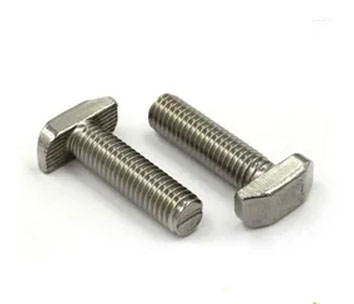
Stainless Hammer Head Bolts & T-Head Bolts: Manufacturer & Distributor
A hammer head bolt has a long, narrow head shaped like the head of a hammer. It drops into a slot or channel, turns under the edges and holds there, so parts can be fixed anywhere along the slot without drilling.
Exotic Alloy manufactures hammer head bolts in Mumbai, India, for building services, façade and solar installers, machine builders and steel fabricators. We stock across India and supply Spain, Europe, the Gulf and Africa. Small heads are cold formed, large T-heads are hot forged, and threads are rolled.
Two families
DIN T-head bolts (DIN 261, 186, 188) slide into machine-table T-slots and foundation slots. Channel hammer head bolts, like the ones in our photo, are inserted through the slot of an anchor or mounting channel and turned 90°; a notch in the thread end shows which way the head points. For the matching nuts and washers see nuts and washers.
- Head
- Rectangular, width = thread size (DIN)
- Fixing
- Turned 90° under channel lips, or slid into a T-slot
- Anti-turn
- Square neck (DIN 186) or nibs (DIN 188)
- Marking
- Notch in the thread end shows head direction
- Grades
- A2-70, A4-50, A4-70; 4.6, 8.8
- Related
- T head screws, square head bolts, anchor fasteners
Hammer Head Bolt Specification
The range we manufacture and supply.
DIN 261 vs DIN 186 vs DIN 188 Hammer Head Bolts
Same head, three ways to stop the bolt turning while the nut is tightened.
| Type | Under the head | Sizes | Typical use |
|---|---|---|---|
| DIN 261 | Plain | M8–M100 × 6 | T-slots whose walls stop the head turning |
| DIN 186 | Square neck | M6–M48 | T-slots, foundations, square holes |
| DIN 188 | Two nibs | M8–M80 × 6 | Foundations and frames where the nibs lock the head |
| Channel bolt | Plain head, notched end | M8–M20 | Anchor channels, mounting rails, solar structures |
Hammer Head Bolt Dimensions
| Thread | Pitch P | m head length nom | n head width nom | k head height nom | As stress area mm² |
|---|---|---|---|---|---|
| M8 | 1.25 | 18 | 8 | 5.5 | 36.6 |
| M10 | 1.5 | 21 | 10 | 7 | 58 |
| M12 | 1.75 | 26 | 12 | 8 | 84.3 |
| M16 | 2 | 30 | 16 | 10.5 | 157 |
| M20 | 2.5 | 36 | 20 | 13 | 245 |
| M24 | 3 | 43 | 24 | 15 | 353 |
| M30 | 3.5 | 54 | 30 | 19 | 561 |
| M36 | 4 | 66 | 36 | 23 | 817 |
| M42 | 4.5 | 80 | 42 | 26 | 1121 |
| M48 | 5 | 88 | 48 | 30 | 1473 |
| M56 | 5.5 | 102 | 56 | 35 | 2030 |
| M64 | 6 | 115 | 64 | 40 | 2676 |
| M72 × 6 | 6 | 128 | 72 | 45 | – |
| M80 × 6 | 6 | 140 | 80 | 50 | – |
| M90 × 6 | 6 | 155 | 90 | 55 | – |
| M100 × 6 | 6 | 170 | 100 | 62 | – |
DIN 261:2010 T-head bolts, mm. Stress area As from ISO 898-1, up to M64.
| Thread | Pitch P | m head length nom | n head width nom | k head height nom |
|---|---|---|---|---|
| M6 | 1 | 16 | 6 | 4.5 |
| M8 | 1.25 | 18 | 8 | 5.5 |
| M10 | 1.5 | 21 | 10 | 7 |
| M12 | 1.75 | 26 | 12 | 8 |
| M16 | 2 | 30 | 16 | 10.5 |
| M20 | 2.5 | 36 | 20 | 13 |
| M24 | 3 | 43 | 24 | 15 |
| M30 | 3.5 | 54 | 30 | 19 |
| M36 | 4 | 66 | 36 | 23 |
| M42 | 4.5 | 80 | 42 | 26 |
| M48 | 5 | 88 | 48 | 30 |
DIN 186:2010 T-head bolts with square neck, mm. Neck dimensions to the standard; ask for a drawing.
| Thread | m head length nom | n head width nom | k head height nom |
|---|---|---|---|
| M8 | 18 | 8 | 5.5 |
| M10 | 21 | 10 | 7 |
| M12 | 26 | 12 | 8 |
| M16 | 30 | 16 | 10.5 |
| M20 | 36 | 20 | 13 |
| M24 | 43 | 24 | 15 |
| M30 | 54 | 30 | 19 |
| M36 | 66 | 36 | 23 |
| M42 | 80 | 42 | 26 |
| M48 | 88 | 48 | 30 |
| M56 | 102 | 56 | 35 |
| M64 | 115 | 64 | 40 |
| M72 × 6 | 128 | 72 | 45 |
| M80 × 6 | 140 | 80 | 50 |
DIN 188:2011 T-head bolts with double nib, mm.
| Channel profile width / depth, mm | Typical bolt threads | Common classes |
|---|---|---|
| 28/15 | M8, M10, M12 | 4.6, 8.8, A4-50, A4-70 |
| 38/17 | M10, M12, M16 | 4.6, 8.8, A4-50, A4-70 |
| 40/22 | M10, M12, M16 | 4.6, 8.8, A4-50, A4-70 |
| 50/30 | M12, M16, M20 | 4.6, 8.8, A4-50, A4-70 |
Typical bolt sizes for common channel profiles. Head length and shape differ between channel makers: send us your channel drawing or part number and we match it.
Installing Hammer Head Bolts
1. Insert
Push the head into the channel slot lengthways, at any point along the channel.
2. Turn 90°
Turn clockwise until the head stops under both lips.
3. Check the notch
The notch in the thread end must lie across the channel.
4. Fixture & washer
Place the part and a washer of the same material as the bolt.
5. Tighten
Tighten the nut to the torque given by the channel maker.
T-slots
DIN T-head bolts slide in from the end of the slot; check the head fits the slot width and depth.
Hammer Head Bolt Property Classes & Loads
The bolt is only one part of the joint: in a channel or T-slot, the lips or slot usually give way first.
| Class | Standard | Rm min MPa | Rp0.2 / Re min MPa | M12 breaking load min, kN | M16 breaking load min, kN |
|---|---|---|---|---|---|
| 4.6 | ISO 898-1 | 400 | 240 | 33.7 | 62.8 |
| 8.8 | ISO 898-1 | 800 | 640 | 67.4 | 125.6 |
| A4-50 | ISO 3506-1 | 500 | 210 | 42.1 | 78.5 |
| A2-70 / A4-70 | ISO 3506-1 | 700 | 450 | 59.0 | 109.9 |
| A4-80 | ISO 3506-1 | 800 | 600 | 67.4 | 125.6 |
Minimum breaking load = stress area × minimum tensile strength (our calculation from ISO 898-1 and ISO 3506-1). These are bolt values, not working loads: use the channel maker’s design loads for the fixing.
Hammer Head Bolt Size & Load Calculator
Pick a size and class to see the head dimensions, the typical channels and the bolt’s own minimum loads.
Bolt
Head sizes from DIN 261 (DIN 186 for M6). Loads are our calculation: stress area × minimum tensile strength or yield strength (ISO 898-1, ISO 3506-1). Bolt values only, not safe working loads.
Result
Hammer Head Bolt Materials & Finishes
| Material | Classes | Finish | Best for |
|---|---|---|---|
| Carbon steel | 4.6, 8.8 | Zinc plated | Dry indoor services and machines |
| Carbon steel | 4.6, 8.8 | Hot-dip galvanised | Outdoor steelwork, solar structures |
| A2 stainless (304) | A2-70 | Plain, passivated | Indoor and mild outdoor |
| A4 stainless (316) | A4-50, A4-70 | Plain, passivated | Coastal, tunnels, car parks, food plants |
How Our Hammer Head Bolts Are Made
Bar & wire
Stainless or carbon steel, certified by heat.
Heading
Cold formed up to medium sizes; large T-heads hot forged.
Head shaping
Head trimmed to the channel or DIN profile; neck or nibs formed.
Threading
Threads rolled; orientation notch pressed into the end.
Heat treatment
Quench and temper for 8.8; stainless as formed.
Finishing
Passivation, zinc plating or hot-dip galvanising.
Where Our Hammer Head Bolts Are Used
Façades & curtain walls
Brackets fixed to cast-in anchor channels.
Solar mounting
Rails and clamps on C-profile structures.
Building services
Pipe, duct and cable-tray supports on mounting channels.
Tunnels & rail
A4 bolts in tunnel and catenary channels.
Machine tools
DIN 261 and DIN 186 bolts in table T-slots.
Foundations
DIN 188 and large T-head bolts for heavy machinery.
Hammer Head Bolt Inspection & Certification
| Check | Method | Applied to |
|---|---|---|
| Head length, width, height | Callipers: m, n, k | Every lot |
| Fit in the channel | Trial in a channel sample | Channel bolts |
| Notch orientation | Visual against the head | Channel bolts |
| Thread | GO / NO-GO ring gauges | Every lot |
| Mechanical | ISO 898-1 / ISO 3506-1 tests | Every heat-treatment or material lot |
| Coating | Thickness gauge | Galvanised lots |
Every shipment includes
- Mill certificate with heat number
- Dimensional report
- Lot number on every box
On request
- EN 10204 3.1 certificate
- PMI report for stainless
- Bolt, nut and washer sets