ISO 7040 Nylock Nuts: Manufacturer & Stockist
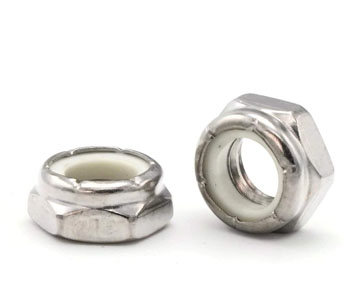
A nylock nut is a hexagon nut with a nylon ring in a collar on top. The bolt forms its own thread in the ring, and the nylon's grip on the thread keeps the nut from working loose under vibration.
Exotic Alloy manufactures and stocks nylock nuts in Mumbai, India, for machine builders, vehicle and trailer makers, HVAC and electrical panel makers, and fastener distributors. We supply across India and stock for buyers in Zimbabwe, Southern and East Africa, the Middle East and South-East Asia.
Regular height, three standards
ISO 7040 is the international metric standard. DIN 982, the German high type, is withdrawn but still ordered, with spanner sizes one step bigger at M10, M12 and M14. Inch nuts follow ASME B18.16.6 style NE. The thin nylon-insert nuts, DIN 985, ISO 10511 and style NTE, are on nylock jam nuts; for plain nuts see hex nuts and for nylon-insert flange nuts hex flange nuts.
- Metric
- ISO 7040 M3–M36; DIN 982 M5–M24
- Inch
- ASME B18.16.6 NE, 1/4–1-1/2
- M10 height
- 11.9 mm max (ISO 7040)
- Insert
- Polyamide, to about 120 °C
- Classes
- 5, 8, 10; NE2, NE5, NE8
- Stainless
- A2-70, A4-70
- Related
- Thin nylock, all-metal lock, washers
Nylock Nut Specification
The range we manufacture and stock.
ISO 7040 Nylock Nut Dimensions
Regular height, metric coarse thread, mm.
| Thread | Pitch P | Spanner s max / min | e min | Height h max / min | Nut body m min | Wrenching mw min | Bearing dw min |
|---|---|---|---|---|---|---|---|
| M3 * | 0.5 | 5.5 / 5.32 | 6.01 | 4.5 / 4.02 | 2.15 | 1.72 | 4.57 |
| M4 * | 0.7 | 7 / 6.78 | 7.66 | 6 / 5.52 | 2.9 | 2.32 | 5.88 |
| M5 * | 0.8 | 8 / 7.78 | 8.79 | 6.8 / 6.22 | 4.4 | 3.52 | 6.88 |
| M6 | 1 | 10 / 9.78 | 11.05 | 8 / 7.42 | 4.9 | 3.92 | 8.88 |
| M8 | 1.25 | 13 / 12.73 | 14.38 | 9.5 / 8.92 | 6.44 | 5.15 | 11.63 |
| M10 | 1.5 | 16 / 15.73 | 17.77 | 11.9 / 11.2 | 8.04 | 6.43 | 14.63 |
| M12 | 1.75 | 18 / 17.73 | 20.03 | 14.9 / 14.2 | 10.37 | 8.3 | 16.63 |
| (M14) | 2 | 21 / 20.67 | 23.36 | 17 / 15.9 | 12.1 | 9.68 | 19.64 |
| M16 | 2 | 24 / 23.67 | 26.75 | 19.1 / 17.8 | 14.1 | 11.28 | 22.49 |
| M20 * | 2.5 | 30 / 29.16 | 32.95 | 22.8 / 20.7 | 16.9 | 13.52 | 27.7 |
| M24 | 3 | 36 / 35 | 39.55 | 27.1 / 25 | 20.2 | 16.16 | 33.25 |
| M30 | 3.5 | 46 / 45 | 50.85 | 32.6 / 30.1 | 24.3 | 19.44 | 42.75 |
| M36 | 4 | 55 / 53.8 | 60.79 | 38.9 / 36.4 | 29.4 | 23.52 | 51.11 |
ISO 7040:2012 Table 1, identical to the 1997 edition and to globalfastener's 2012 listing; spanner s and corners e are those of the ISO 4032 plain nut. h overall height, m height of the metal nut body (the ISO 4032 minimum), mw wrenching height. * ISO 7040:2025, the current edition, keeps these figures except at M3 (h max 4.8), M4 (6.5), M5 (6.95) and M20 (23), and adds the six sizes below. The 2025 values come from globalfastener alone; their s and m match ISO 4032:2023.
Sizes added in ISO 7040:2025
| Thread | Pitch P | Spanner s | Height h max | Nut body m min |
|---|---|---|---|---|
| (M7) | 1 | 11 | 9.2 | 6.14 |
| (M18) | 2.5 | 27 | 21.2 | 15.1 |
| (M22) | 2.5 | 34 | 25 | 18.1 |
| (M27) | 3 | 41 | 29.9 | 22.5 |
| (M33) | 3.5 | 50 | 35.7 | 27.4 |
| (M39) | 4 | 60 | 41.9 | 31.8 |
DIN 982 Nylock Nuts and the ISO Difference
High type, metric coarse thread, mm. Bold: ISO spanner size differs.
| Thread | Pitch P coarse | Spanner s max / min | e min | Height h max / min | Nut body m min | ISO 7040 s / h max |
|---|---|---|---|---|---|---|
| M5 | 0.8 | 8 / 7.78 | 8.79 | 6.3 / 6 | 4.4 | 8 / 6.8 |
| M6 | 1 | 10 / 9.78 | 11.05 | 8 / 7.7 | 4.9 | 10 / 8 |
| M7 | 1 | 11 / 10.73 | 12.12 | 8.5 / 8.2 | 6.14 | – |
| M8 | 1.25 | 13 / 12.73 | 14.38 | 9.5 / 9.14 | 6.44 | 13 / 9.5 |
| M10 | 1.5 | 17 / 16.73 | 18.9 | 11.5 / 11.14 | 8.04 | 16 / 11.9 |
| M12 | 1.75 | 19 / 18.67 | 21.1 | 14 / 13.64 | 10.37 | 18 / 14.9 |
| M14 | 2 | 22 / 21.67 | 24.49 | 16 / 15.3 | 12.1 | 21 / 17 |
| M16 | 2 | 24 / 23.67 | 26.75 | 18 / 17.3 | 14.1 | 24 / 19.1 |
| M18 | 2.5 | 27 / 26.16 | 29.56 | 20 / 19.16 | 15.1 | – |
| M20 | 2.5 | 30 / 29.16 | 32.95 | 22 / 20.7 | 16.9 | 30 / 22.8 |
| M22 | 2.5 | 32 / 31 | 35.03 | 25 / 23.7 | 18.1 | – |
| M24 | 3 | 36 / 35 | 39.55 * | 28 / 26.7 | 20.2 | 36 / 27.1 |
DIN 982:1987 from globalfastener, fasten.it, Intafast and ITA Fasteners, which agree except for misprints. * M24: fasten.it gives e min 39.95 mm; globalfastener, Intafast and the ISO 4032 value for a 36 mm hexagon give 39.55 mm, which we use. Fine-thread DIN 982 nuts, such as M10 x 1.25 and M12 x 1.5, are made to order.
ASME B18.16.6 Style NE Nylon Insert Locknuts
Regular height, UNC and UNF, inches.
| Size | TPI UNC / UNF | Across flats max / min | Corners min | Height max / min | Hex height min | Bearing min |
|---|---|---|---|---|---|---|
| 1/4 | 20 / 28 | .439 / .430 | .488 | .328 / .298 | .225 | .416 |
| 5/16 | 18 / 24 | .502 / .489 | .557 | .359 / .329 | .250 | .475 |
| 3/8 | 16 / 24 | .564 / .551 | .628 | .468 / .438 | .335 | .534 |
| 7/16 | 14 / 20 | .627 / .616 | .698 | .468 / .438 | .324 | .597 |
| 1/2 | 13 / 20 | .752 / .736 | .840 | .609 / .579 | .464 | .712 |
| 9/16 | 12 / 18 | .877 / .861 | .982 | .656 / .626 | .469 | .830 |
| 5/8 | 11 / 18 | .940 / .922 | 1.051 | .765 / .735 | .593 | .890 |
| 3/4 | 10 / 16 | 1.064 / 1.052 | 1.191 | .890 / .860 | .742 | 1.033 |
| 7/8 | 9 / 14 | 1.252 / 1.239 | 1.403 | .999 / .969 | .790 | 1.230 |
| 1 | 8 / 12 | 1.440 / 1.427 | 1.619 | 1.078 / 1.016 | .825 | 1.418 |
| 1-1/8 | 7 / 12 | 1.627 / 1.614 | 1.833 | 1.203 / 1.141 | .930 | 1.605 |
| 1-1/4 | 7 / 12 | 1.815 / 1.801 | 2.046 | 1.422 / 1.360 | 1.125 | 1.793 |
| 1-3/8 | 6 / 12 | 2.008 / 1.973 | 2.259 | 1.609 / 1.547 | 1.282 | 1.962 |
| 1-1/2 | 6 / 12 | 2.197 / 2.159 | 2.473 | 1.640 / 1.578 | 1.313 | 2.148 |
ASME B18.16.6 style NE from globalfastener (2008 and 2017 listings), BoltingSpecialist and JC Fasteners. Grades NE2, NE5 and NE8 go with SAE grade 2, 5 and 8 bolts. Across corners: globalfastener's 2017 listing prints slightly smaller minimums at ten sizes (for example 0.482 against 0.488 in at 1/4); the other sources and its 2008 listing give the values shown. JC Fasteners lists height minimums 0.003 to 0.008 in lower; we use the matching values of the other three.
How Nylock Nuts Lock and How to Fit Them
- Bolt length: clamped parts + washers + nut height h + 2 to 3 thread pitches, so the bolt passes right through the ring.
- Strength: the metal body is a full ISO 4032 nut, so a class 8 nylock nut carries an 8.8 bolt.
- Heat: keep below about 120 °C; above that use an all-metal lock nut.
- Tighten with a spanner on the hex; the ring is not a bearing face.
- Grip falls with each removal: refit only in non-critical joints, never where a joint is safety-critical.
- Keep the ring away from solvents and paint stripper.
Sources differ: some guides ask for 2 pitches of bolt past the nut, others 3; the finder shows both. The insert's upper limit of about 120 °C is given by Würth and AIMS Industrial; lower limits quoted range from −40 °C to −70 °C.
Nylock Nut Finder: Size, Bolt Length & Heat Check
Pick the nut, enter the joint and the service temperature; get the dimensions, the bolt length, a heat check and the order line.
Nut & joint
Dimensions from the tables on this page (ISO 7040:2012 values; 2025 changes are flagged). Bolt length = clamped parts + washers + nut height h max + 2 pitches (shortest) or 3 pitches. Round up to the next stock length. Heat check against about 120 °C for the nylon.
Result
Nylock Nut Materials & Finishes
| Nut body | Class / grade | Finish | Pairs with |
|---|---|---|---|
| Carbon steel | 5 · 8 · 10 (ISO 7040, DIN 982) | Zinc plated, zinc flake, plain | Bolts up to 5.8, 8.8, 10.9 |
| Carbon steel, inch | NE2 · NE5 · NE8 | Zinc plated, plain | SAE grade 2, 5, 8 bolts |
| Stainless A2 (304) | A2-70 | Plain, as in the photo | A2-70 bolts; food plants, outdoors |
| Stainless A4 (316) | A4-70 | Plain | A4-70 bolts; marine and chemical areas |
ISO 7040 gives property classes 5, 8 and 10 from M5 (class as agreed below M5), with stainless grades selectable from ISO 3506-2; the insert is non-metallic, for example polyamide. Coatings follow ISO 4042 (electroplating) or ISO 10683 (zinc flake).
How Our Nylock Nuts Are Made
Material
Steel or stainless wire with heat certificate.
Form
Hex body and collar cold formed.
Tap
Thread tapped through the body.
Treat & plate
Heat treated for class 10; plated before the insert goes in.
Insert
Nylon ring pressed in, collar rolled over.
Test
Thread, height and prevailing torque checked.
Where Our Nylock Nuts Are Used
Machinery
Guards, frames and motor mounts under vibration.
Vehicles & trailers
Body panels, brackets and suspension parts.
HVAC
Fans, blowers and duct supports.
Electrical
Panels, cable trays and busbar supports.
Agriculture
Implements that shake loose plain nuts.
Food equipment
Stainless A2 and A4 nuts on wash-down machines.
Nylock Nut Inspection & Certification
| Check | Method | Applied to |
|---|---|---|
| Thread | GO / NOT GO plug gauges, before the insert | Every lot |
| Spanner, height | Calipers against h max / min and s | Every lot |
| Prevailing torque | Torque on and off a test bolt (ISO 2320 / ASME B18.16.6) | Every lot |
| Proof load | ISO 898-2 / ISO 3506-2 | Every heat-treatment batch |
| Material | Heat certificate, PMI for stainless | Every heat |
| Coating | Thickness gauge | Plated lots |
Every shipment includes
- EN 10204 3.1 certificate
- Lot number on every box
- Packing list by size
On request
- EN 10204 3.2 with third-party inspection
- Prevailing torque test report
- Sets with bolts and washers