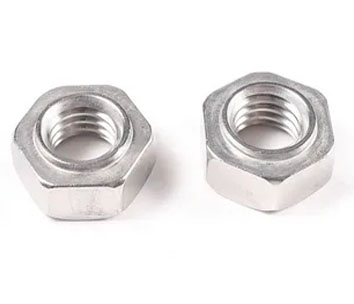
DIN 929 Projection Weld Nuts: Manufacturer & Distributor
A hex weld nut gives thin sheet a strong, permanent thread. It is welded on once, in a few moments, and from then on a bolt can be fitted from the other side with one hand and one spanner.
Exotic Alloy manufactures and distributes hex weld nuts from Mumbai, India, for vehicle and trailer builders, appliance and enclosure makers, furniture and machinery fabricators, and fastener distributors. We supply across India and to Saudi Arabia, the Gulf, Africa and South-East Asia.
How it is built
The weld face carries a round pilot that drops into a hole in the sheet and three small projections on alternate corners. In projection welding the current flows through the projections, which melt and fuse the nut to the sheet. For high-strength bolts there are flanged weld nuts to ISO 21670; for square weld nuts see square weld nuts, for ordinary nuts hex nuts.
- Standard
- DIN 929:2013 (same sizes as 2000)
- Sizes
- M3–M16, fine thread 8–16 mm
- Hole
- = pilot ⌀, 12.5 mm at M10
- Sheet
- 0.63–1.5 mm (M3) to 2–6 mm (M16)
- Bolts
- Property class below 8.8
- Material
- Steel C ≤ 0.25 %, A2, A4
- Related
- Square weld nuts, hex nuts, flange nuts
Hex Weld Nut Specification
The range we manufacture, stock and distribute.
DIN 929 Hex Weld Nut Dimensions
Coarse thread, mm. (M14) is a non-preferred size.
| Size | Pitch P | Spanner s max / min | e min | Height m max / min | Pilot ⌀ max / min | Pilot height h1 max / min | Projection h2 max / min | kg / 1000 |
|---|---|---|---|---|---|---|---|---|
| M3 | 0.5 | 7.5 / 7.28 | 8.15 | 3 / 2.75 | 4.47 / 4.395 | 0.55 / 0.45 | 0.25 / 0.15 | 0.78 |
| M4 | 0.7 | 9 / 8.78 | 9.83 | 3.5 / 3.2 | 5.97 / 5.895 | 0.65 / 0.55 | 0.35 / 0.25 | 1.13 |
| M5 | 0.8 | 10 / 9.78 | 10.95 | 4 / 3.7 | 6.96 / 6.87 | 0.7 / 0.6 | 0.4 / 0.3 | 1.73 |
| M6 | 1 | 11 / 10.73 | 12.02 | 5 / 4.7 | 7.96 / 7.87 | 0.75 / 0.6 | 0.4 / 0.3 | 2.5 |
| M8 | 1.25 | 14 / 13.73 | 15.38 | 6.5 / 6.14 | 10.45 / 10.34 | 0.9 / 0.75 | 0.5 / 0.35 | 5.27 |
| M10 | 1.5 | 17 / 16.73 | 18.74 | 8 / 7.64 | 12.45 / 12.34 | 1.15 / 0.95 | 0.65 / 0.5 | 9.58 |
| M12 | 1.75 | 19 / 18.67 | 20.91 | 10 / 9.64 | 14.75 / 14.64 | 1.4 / 1.2 | 0.8 / 0.6 | 13.7 |
| (M14) | 2 | 22 / 21.67 | 24.27 | 11 / 10.57 | 16.75 / 16.64 | 1.8 / 1.6 | 1 / 0.8 | 21.3 |
| M16 | 2 | 24 / 23.67 | 26.51 | 13 / 12.57 | 18.73 / 18.605 | 1.8 / 1.6 | 1 / 0.8 | 28.5 |
DIN 929:2013 (same values as 2000). s across flats, e across corners, m height of the nut body, pilot ⌀ (tolerance d11), h1 pilot height, h2 projection height before welding, mass of 1000 steel nuts. Checked against four sources and every tolerance against ISO 286.
Weld Nut Hole Size and Sheet Thickness
What to punch, which sheet each size suits, and how the nut compares with an ISO 4032 nut, mm.
| Size | Hole in the sheet nominal / max (H13) | Sheet thickness min – max | Pilot height h1 max | Spanner vs ISO 4032 | Height vs ISO 4032 |
|---|---|---|---|---|---|
| M3 | 4.5 / 4.68 | 0.63 – 1.5 | 0.55 | 7.5 vs 5.5 | 3 vs 2.4 |
| M4 | 6 / 6.18 | 0.75 – 1.5 | 0.65 | 9 vs 7 | 3.5 vs 3.2 |
| M5 | 7 / 7.22 | 0.88 – 2 | 0.7 | 10 vs 8 | 4 vs 4.7 |
| M6 | 8 / 8.22 | 0.88 – 2.5 | 0.75 | 11 vs 10 | 5 vs 5.2 |
| M8 | 10.5 / 10.77 | 1 – 3 | 0.9 | 14 vs 13 | 6.5 vs 6.8 |
| M10 | 12.5 / 12.77 | 1.25 – 4 | 1.15 | 17 vs 16 | 8 vs 8.4 |
| M12 | 14.8 / 15.07 | 1.5 – 5 | 1.4 | 19 vs 18 | 10 vs 10.8 |
| (M14) | 16.8 / 17.07 | 2 – 6 | 1.8 | 22 vs 21 | 11 vs 12.8 |
| M16 | 18.8 / 19.13 | 2 – 6 | 1.8 | 24 vs 24 | 13 vs 14.8 |
The hole equals the pilot diameter. globalfastener and fasten.it give it an H13 tolerance, as shown; Bossard's data sheet calls for H11 (for example 12.50 to 12.61 mm at M10), which fits within H13 and centres the nut more closely. Sheet thickness range from fasten.it and Bossard.
How a Weld Nut Is Projection Welded
- Pilot: centres the nut in the hole, holds it while welding and keeps spatter out of the thread.
- Projections: three, on alternate corners; they concentrate the current so the weld forms there and not in the thread.
- Steel: DIN 929 calls for at most 0.25 % carbon, which welds well; other steels by agreement.
- Welding current, force and time depend on the machine, sheet and coating: set them with trial welds.
Bolt Grade and Bolt Length for Weld Nuts
- Shortest bolt = part + sheet + nut height m. Choose the next standard length; we suggest about two pitches more so the chamfered end clears the nut.
- The finder below does the sum for your joint.
- Bolt grade: DIN 929 weld nuts are for bolts below class 8.8 (fasten.it, Bossard). Some sellers quote 8.8; we follow the standard.
- For class 8.8 to 10.9 bolts use flanged weld nuts to ISO 21670 (M5 to M16), made to order.
Weld Nut Finder: Hole, Sheet & Bolt Length
Pick the size and enter your sheet and part; get the hole, the sheet check, the bolt length and the order line.
Nut & joint
Dimensions from the tables on this page. Hole = pilot diameter, H13 maximum shown. Shortest bolt = part + sheet + nut height m max; suggested = that plus two pitches. Bolt lengths are under the head. Mass is for steel.
Result
Weld Nut Materials & Finishes
| Material | Finish | Weld to | Where |
|---|---|---|---|
| Low-carbon steel, C ≤ 0.25 % | Plain | Steel sheet | Vehicles, appliances, enclosures, machinery |
| Stainless A2 (304) | Plain | Stainless sheet | Food, kitchen and medical equipment, as in the photo |
| Stainless A4 (316) | Plain | Stainless sheet | Outdoor, coastal and chemical equipment |
DIN 929 names steel with at most 0.25 % carbon and allows other steels by agreement. Match the nut to the sheet: steel to steel, stainless to stainless.
How Our Hex Weld Nuts Are Made
Wire
Low-carbon steel or stainless, certified by heat.
Form
Hexagon, pilot and projections cold formed in one piece.
Tap
Thread tapped through.
Gauge
Pilot diameter and projection height checked.
Clean
Degreased, left plain for welding.
Inspect
Thread gauged, lot certified.
Where Our Hex Weld Nuts Are Used
Vehicles
Body panels, brackets and seat frames.
Trailers
Chassis and body fixings.
Enclosures
Cabinets and panels, mounted from one side.
Appliances
Sheet-metal housings and frames.
Furniture
Steel frames for seating and storage.
Machinery
Guards, covers and sheet-metal frames.
Hex Weld Nut Inspection & Certification
| Check | Method | Applied to |
|---|---|---|
| Thread | GO / NOT GO plug gauges | Every lot |
| s, m, pilot ⌀ | Calipers, micrometer | Every lot |
| h1, h2 | Height gauge | Every lot |
| Carbon content | Heat certificate | Every heat |
| Stainless grade | PMI on request | Stainless lots |
| Weld strength | Push-out or torque-out of welded samples | On request |
Every shipment includes
- EN 10204 3.1 certificate
- Lot number on every box
- Packing list by size
On request
- EN 10204 3.2 with third-party inspection
- Trial welds on your sheet
- Bulk packing for automatic feeders