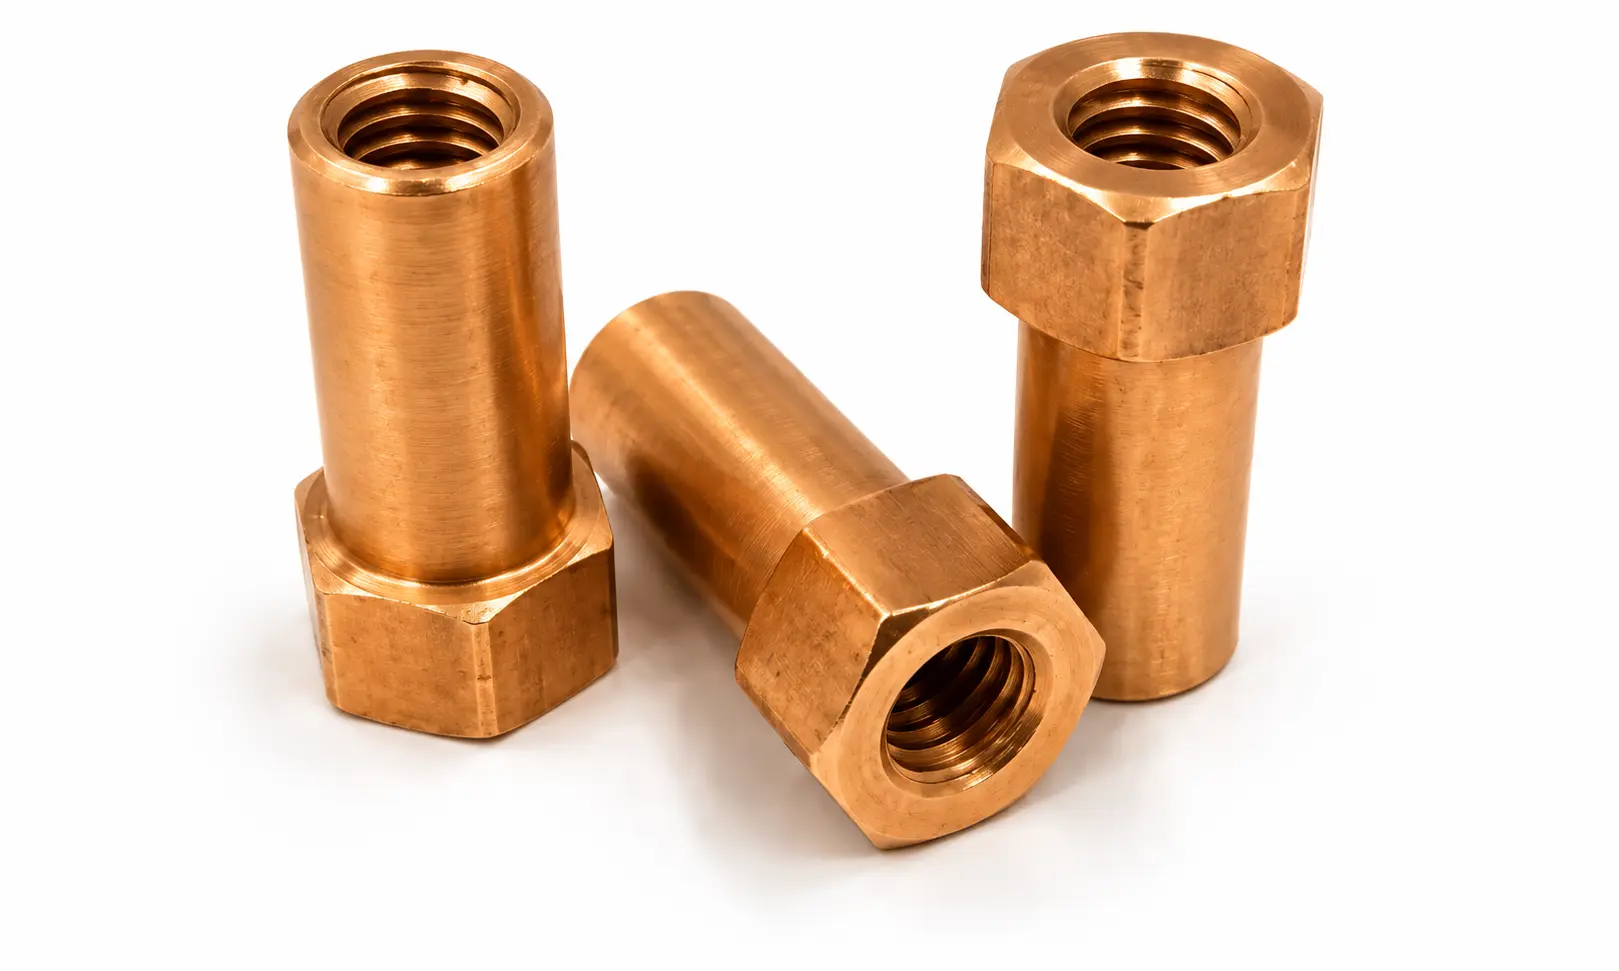
Lead restrictions and weldability. At 3.0–4.0% lead, C54400 is subject to drinking-water lead limits — the US Safe Drinking Water Act caps the weighted average of wetted surfaces at 0.25%, and the European Drinking Water Directive and national acceptance schemes apply equivalent controls — and to RoHS where the part is electrical or electronic. It is also effectively unweldable: CDA rate oxyacetylene, gas shielded arc, coated metal arc, spot and seam welding all Not Recommended and butt welding only Fair, because the lead makes the alloy hot short and causes liquation cracking in the heat-affected zone. Soldering is Excellent and brazing Good. If the part must be welded or will contact drinking water, specify an unleaded grade.
Phosphor bronze is copper and tin, and the tin content decides everything else. These are the oldest engineering alloys in use — copper-tin is bronze in the original sense — and the six unleaded grades on this hub form a clean ladder from 1.25% tin to 10% tin. As tin rises, four things happen together and they are worth reading as one trend.
Strength and spring properties rise sharply. C50500 at 1.0–1.7% tin reaches 517 MPa at spring temper;
C52400 at 9.0–11.0% reaches 883 MPa in strip and
1014 MPa in hard wire, the highest figure on this hub.
Electrical conductivity collapses. C50500 carries
48% IACS and 208 W/m·K, better than many brasses; by C52400 that has fallen to
11% IACS and 50 W/m·K. Tin in solid solution scatters conduction electrons severely, and the drop is roughly fourfold across the range.
The solidus falls and the freezing range widens. C50500 freezes between 1038 and 1077 °C — a 39-degree range; C52400 between 843 and 999 °C, a range of
156 degrees. That wide mushy zone is why the high-tin grades are prone to coring and inverse segregation, and it is the direct reason CDA rate hot forming
Poor on every grade here except C50500.
These are cold-worked alloys. And
thermal expansion rises, from 17.8 to 18.4 × 10⁻⁶/°C — small, but it matters where a phosphor bronze spring works against a steel or brass housing over a temperature range.
The phosphorus in phosphor bronze is there because of how the alloy is melted, and it stays because it is useful. Molten copper-tin readily forms tin oxide, which would leave the casting gassy and the metal dirty. Phosphorus is added as a
deoxidiser: it scavenges oxygen, the products float off, and the melt pours clean. What is left behind is a residue of
0.03–0.35% phosphorus in every grade here —
C54400 is the one exception, registered at 0.01–0.50%.
That residue is not inert. Phosphorus increases strength and hardness, raises the elastic limit, improves wear resistance and significantly improves the fluidity of the melt. It is the reason the alloy is named for it rather than simply being called a tin bronze, and it is why a phosphor bronze outperforms a plain copper-tin alloy of the same tin content as a spring and as a bearing. The range is tight at both ends for a reason: too little and the deoxidation is incomplete, too much and the alloy becomes hot short and the low-melting phosphide network embrittles it.
Phosphor bronze is the classic spring and contact material, and the reasons are specific rather than general. It combines a
high elastic limit,
excellent fatigue strength — CDA publish endurance limits of 152–207 MPa for the spring tempers — good corrosion resistance, low stress relaxation, and the ability to be formed soft and then hardened entirely by cold work. There is no precipitation reaction and no quench and temper:
every temper on this hub is a cold-work temper, running O61 and the OS grain-size anneals at the soft end through H01, H02, H04, H06, H08 and H10 as reduction increases. Across that span tensile strength roughly doubles while elongation falls from 50–70% to 1–3%.
Stress relief after forming is standard practice on this family, and CDA publish the numbers that show why. The HR tempers — HR02, HR04, HR06, HR08, HR10 — are the corresponding cold-worked conditions after a low-temperature stress-relief anneal, and the published data shows a consistent pattern:
the same tensile strength, a somewhat lower 0.2% offset yield, and markedly higher elongation. On
C51900 at extra spring temper, elongation goes from 2% to 9% at an unchanged 765 MPa tensile. The residual tension that drives distortion and stress-corrosion cracking is removed, and the part becomes far more tolerant of handling and assembly.
Specify a stress-relieved temper for formed springs, contacts and clips going into service.Two grades here carry lead, and they exist because the unleaded phosphor bronzes are difficult to machine. Every unleaded grade on this hub rates
20 on the CDA machinability scale — the same as pure copper, and about as poor as engineering metals get. The tough, ductile copper-tin matrix smears and produces long stringy swarf. Lead is essentially insoluble in it, so it sits as discrete soft globules that break the chip mechanically.
C53400, CDA's Phosphor Bronze B-1, carries
0.8–1.2% lead and rates
70.
C54400, Phosphor Bronze B-2, carries
3.0–4.0% lead and rates
80 — the free-cutting phosphor bronze, and the standard bar stock for machined bearings, bushings, thrust washers and valve parts. C54400 is also unusual in carrying a deliberate
1.5–4.5% zinc addition, which makes it a leaded tin-zinc bronze in composition as much as a phosphor bronze.
The lead costs weldability and carries regulatory exposure. CDA rate C54400
Not Recommended for oxyacetylene, gas shielded arc, coated metal arc, spot, seam and butt welding alike — essentially unweldable — where the unleaded grades are rated Good for gas shielded arc welding and
Excellent for soldering, brazing and butt welding. And lead in drinking-water-contact components is restricted under the US Safe Drinking Water Act (0.25% weighted average of wetted surfaces) and under the European Drinking Water Directive, with RoHS restricting it in electrical equipment.
Confirm the regulatory position for your market before committing a design to C53400 or C54400.Phosphor bronze has a broadly good corrosion record, and one specific advantage over brass. With little or no zinc in the unleaded grades there is
no dezincification — the characteristic failure mode of the
brasses simply does not apply. The alloys resist seawater and brackish water, non-oxidising acids, neutral salt solutions, many organic chemicals and industrial and marine atmospheres, and the tin contributes to a protective surface film. They are also
non-sparking and essentially non-magnetic.
The caveats matter and should be designed around. Like every copper alloy, phosphor bronze is susceptible to
stress-corrosion cracking in ammonia, ammonium compounds, amines and nitrites when it carries residual tensile stress — which is precisely the condition a cold-formed spring is in. This is the practical reason stress relief is standard on formed parts, not merely a dimensional-stability measure. Oxidising acids attack it. In a galvanic couple it is cathodic to steel, aluminium and zinc. And where the part will see sustained load at temperature, note that phosphor bronze
relaxes: a spring held under preload above about 100 °C will lose force over time, and the higher-tin grades do better than the lower-tin ones.
How eight grades divide. Six are unleaded and form a tin ladder; two are leaded for machining.
C50500 at 1.0–1.7% tin is the
electrical grade — CDA's Phosphor Bronze 1.25% E — carrying
48% IACS, four times the conductivity of the 10% grade, and it is the only one CDA rate Good for hot forming.
C51100 at 3.5–4.9% and
C51000 at 4.2–5.8% are the
general-purpose spring and contact grades; C51000, Phosphor Bronze 5% A, is the most widely specified phosphor bronze there is and the
ASTM F468 Cu 510 fastener alloy.
C51900 at 5.0–7.0% has the most completely documented temper ladder of any grade here, including every stress-relieved HR condition.
C52100 at 7.0–9.0% (Phosphor Bronze 8% C) and
C52400 at 9.0–11.0% (10% D) are the
high-strength grades — C52400 reaches
1014 MPa in hard wire, the highest figure on this hub — bought for heavy springs, wear plates and bridge expansion plates. Finally the leaded pair:
C53400 (B-1, 0.8–1.2% Pb, machinability 70) and
C54400 (B-2, 3.0–4.0% Pb, machinability 80), the
free-cutting bearing and bushing bar grades.