+91 97734 41022 sales@exoticalloy.com
Material Specification

Nickel Aluminium Bronze C63000

Nickel Aluminium Bronze C63000 Fasteners
Nickel Aluminium Bronze

Nickel Aluminium Bronze C63000 Fasteners

Nickel aluminium bronze C63000 is the general-purpose high-strength wrought grade — copper with 9.0–11.0% aluminium, 4.0–5.5% nickel and 2.0–4.0% iron, manganese to 1.5%. It is the most widely specified wrought nickel aluminium bronze and, for a fastener manufacturer, the most important alloy on this hub.

C63000 is ASTM F468 and F467 Cu 630 — the strongest certified copper-alloy bolting material in the ASTM nonferrous fastener standards. Bolting is specified at 690–896 MPa (100–130 ksi) tensile with 345 MPa minimum yield at 85–100 HRB, against 552–758 MPa for Cu 613 and 345 MPa for Cu 464 naval brass. In drawn and stress relieved rod it reaches 814 MPa typical with 517 MPa yield. The 4.0–5.5% nickel suppresses the gamma-2 eutectoid, so that strength comes without the dealuminification liability of a plain high-aluminium bronze. Note the 5% minimum elongation F468 allows for Cu 630 — this is a strong, relatively unforgiving bolting alloy. It is also covered by AMS 4640 and ASTM B150, B124, B171 and B283. Exotic Alloy supplies C63000 rod, bar, shapes, forgings, fasteners and machined components.

Request a Quote
Product Range

Nickel Aluminium Bronze C63000 Fasteners Available

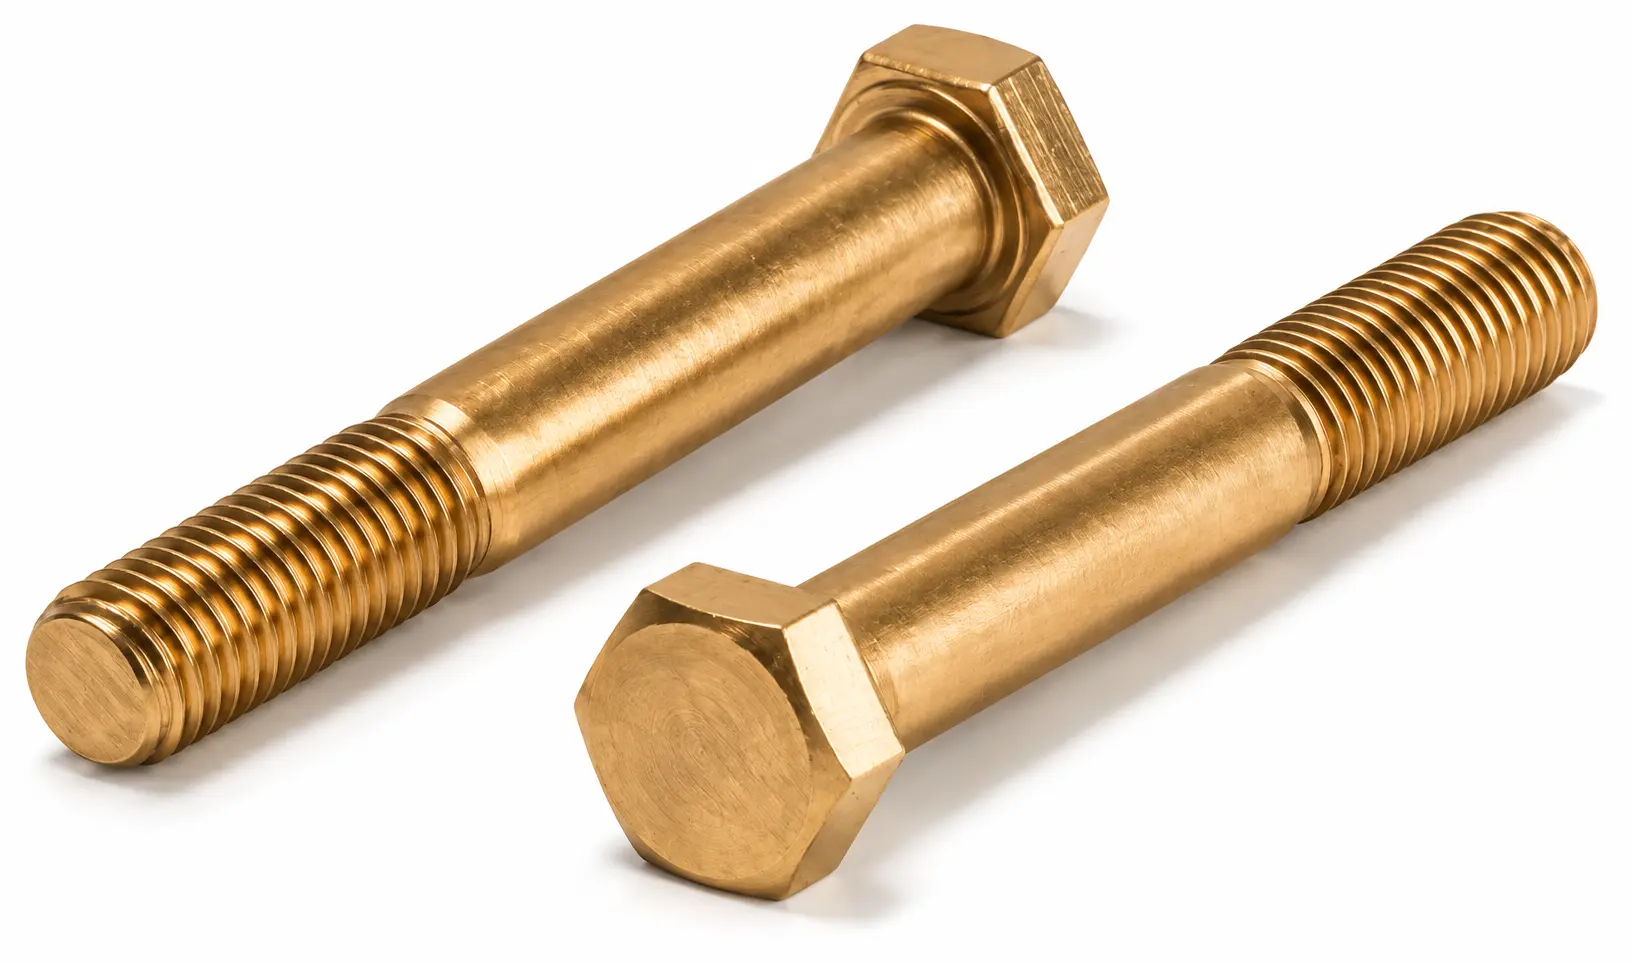
Nickel Aluminium Bronze C63000 Hex Bolts
Nickel Aluminium Bronze C63000
Hex Bolts
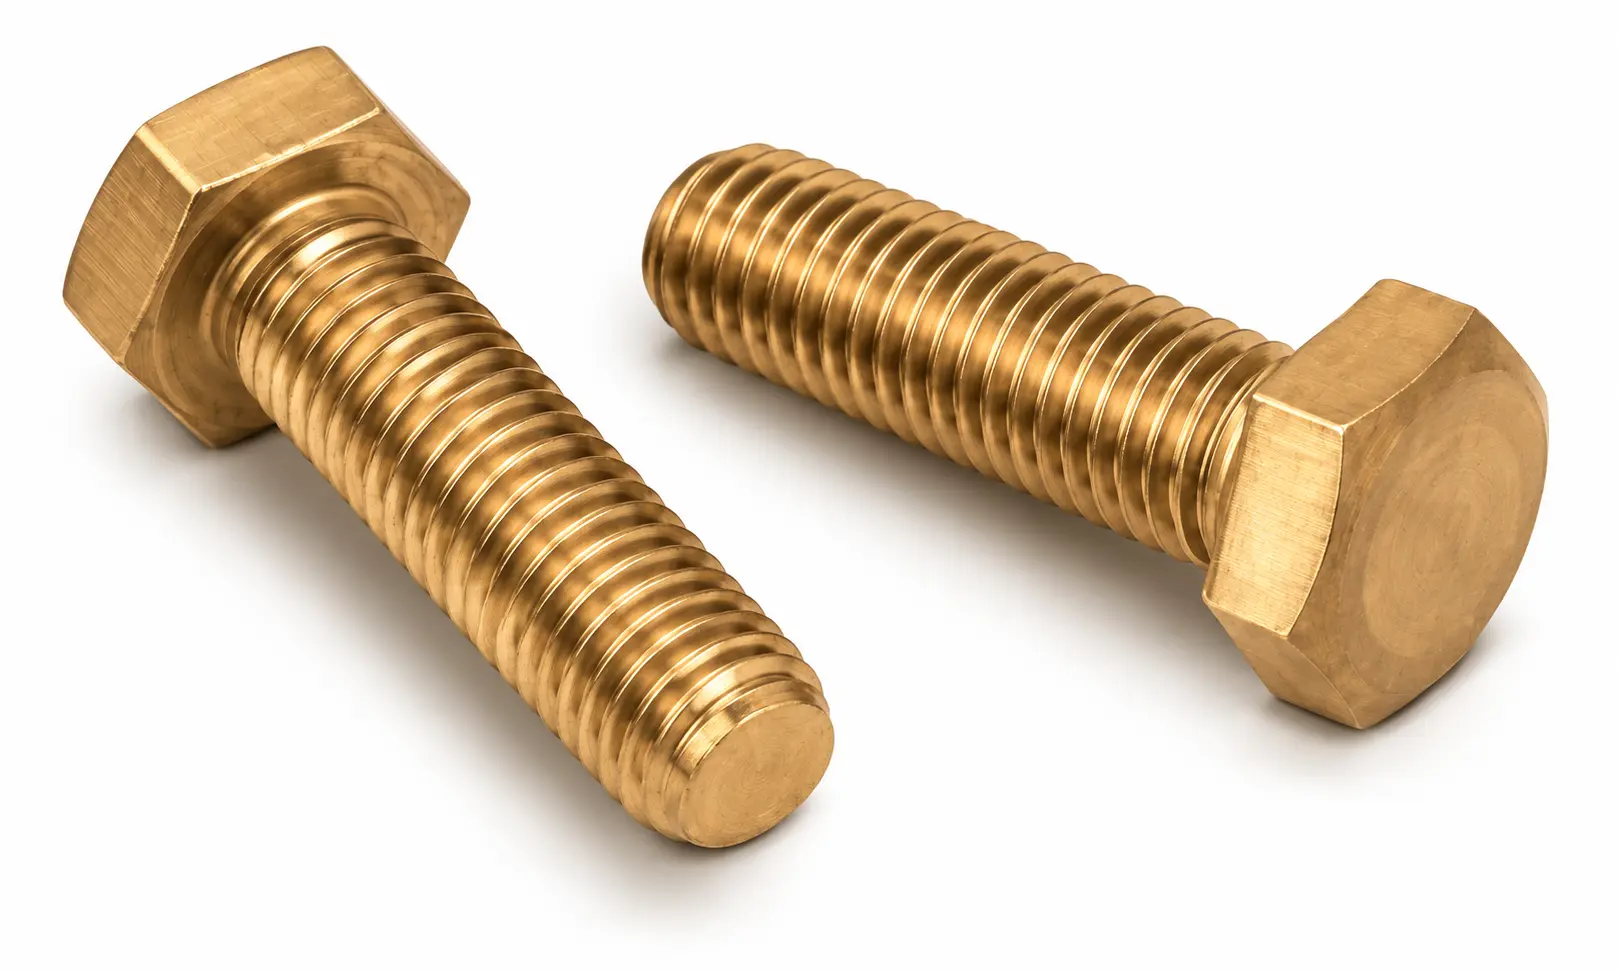
Nickel Aluminium Bronze C63000 Heavy Hex Bolts
Nickel Aluminium Bronze C63000
Heavy Hex Bolts
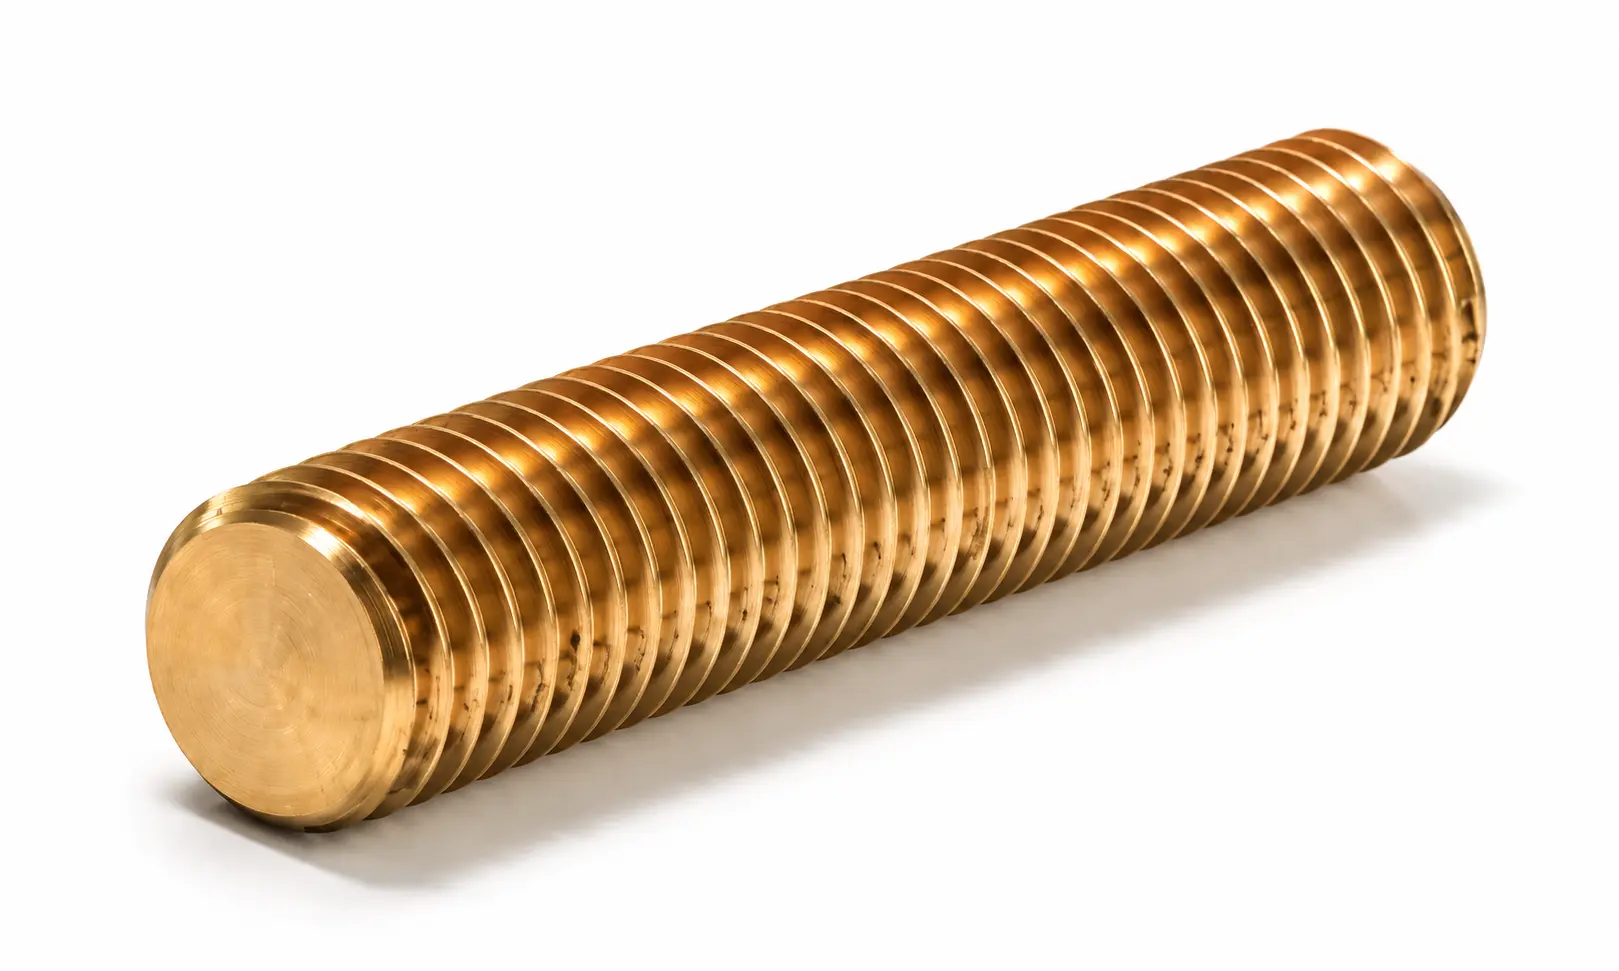
Nickel Aluminium Bronze C63000 Stud Bolts
Nickel Aluminium Bronze C63000
Stud Bolts
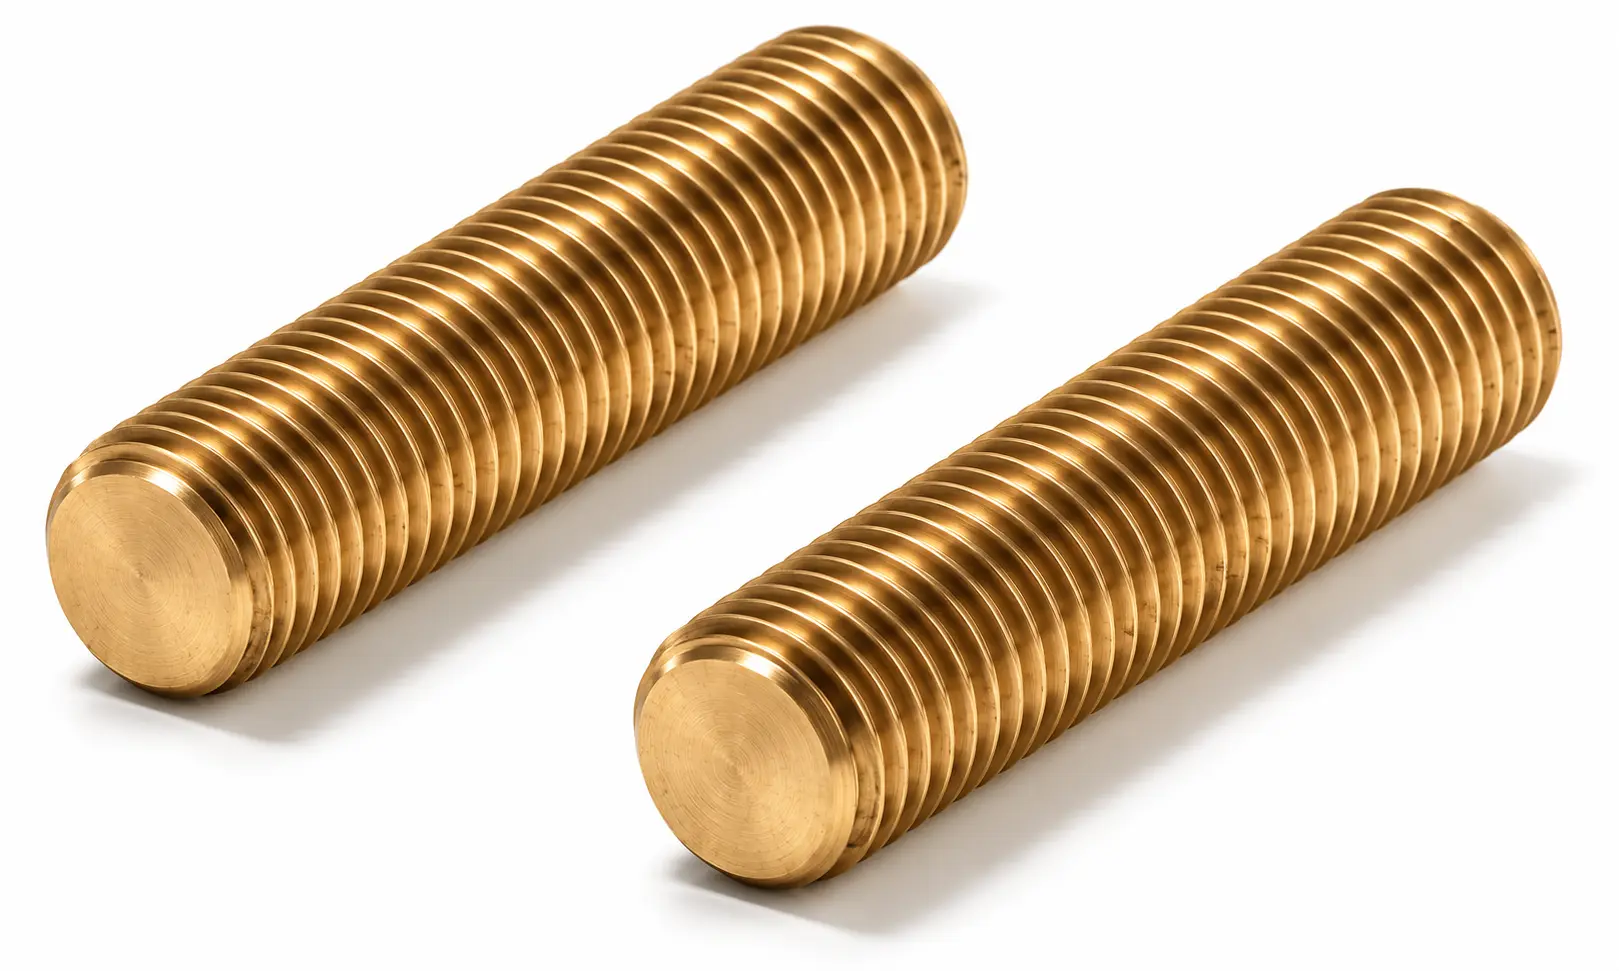
Nickel Aluminium Bronze C63000 Threaded Rods
Nickel Aluminium Bronze C63000
Threaded Rods
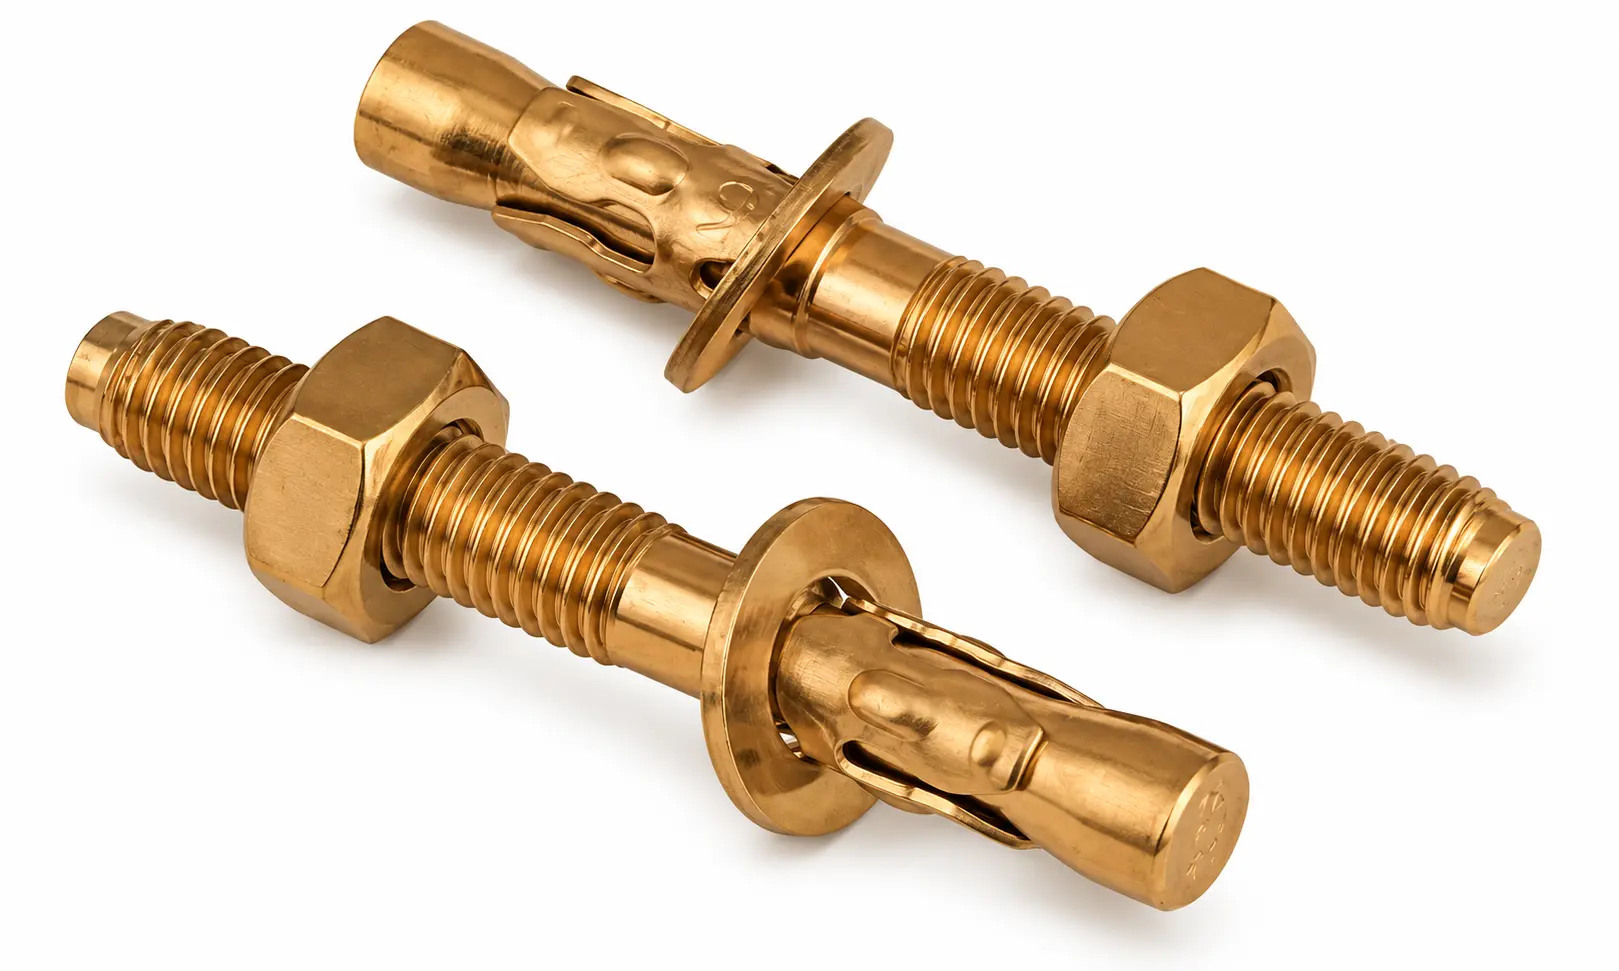
Nickel Aluminium Bronze C63000 Anchor Bolts
Nickel Aluminium Bronze C63000
Anchor Bolts
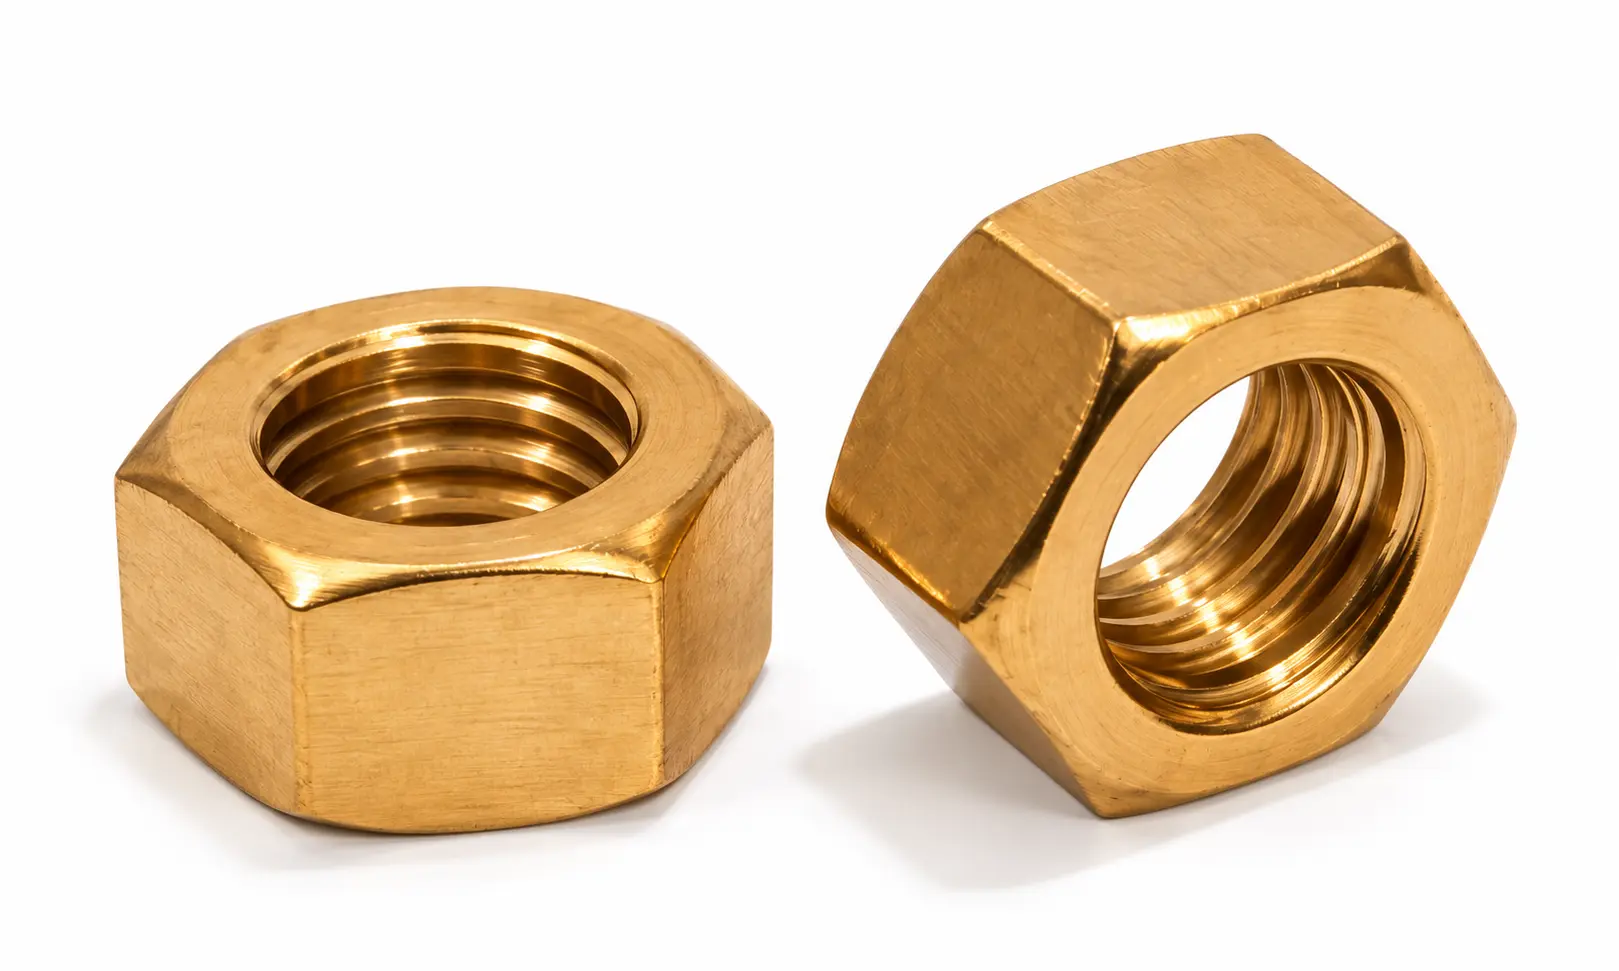
Nickel Aluminium Bronze C63000 Hex Nuts
Nickel Aluminium Bronze C63000
Hex Nuts
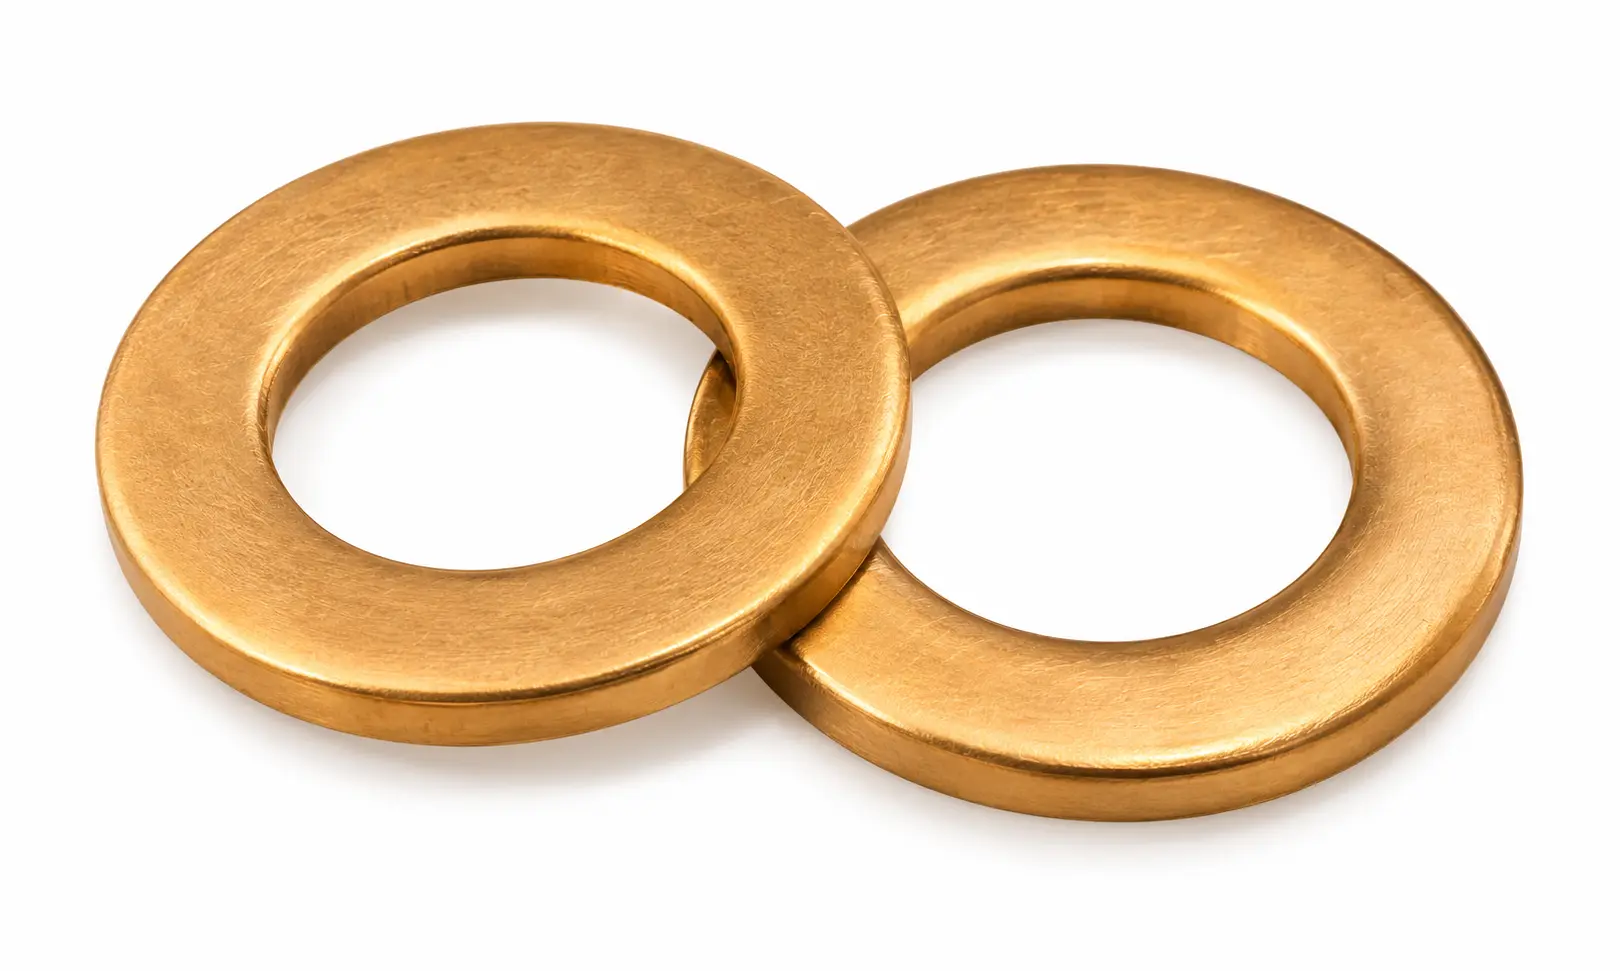
Nickel Aluminium Bronze C63000 Washers
Nickel Aluminium Bronze C63000
Washers
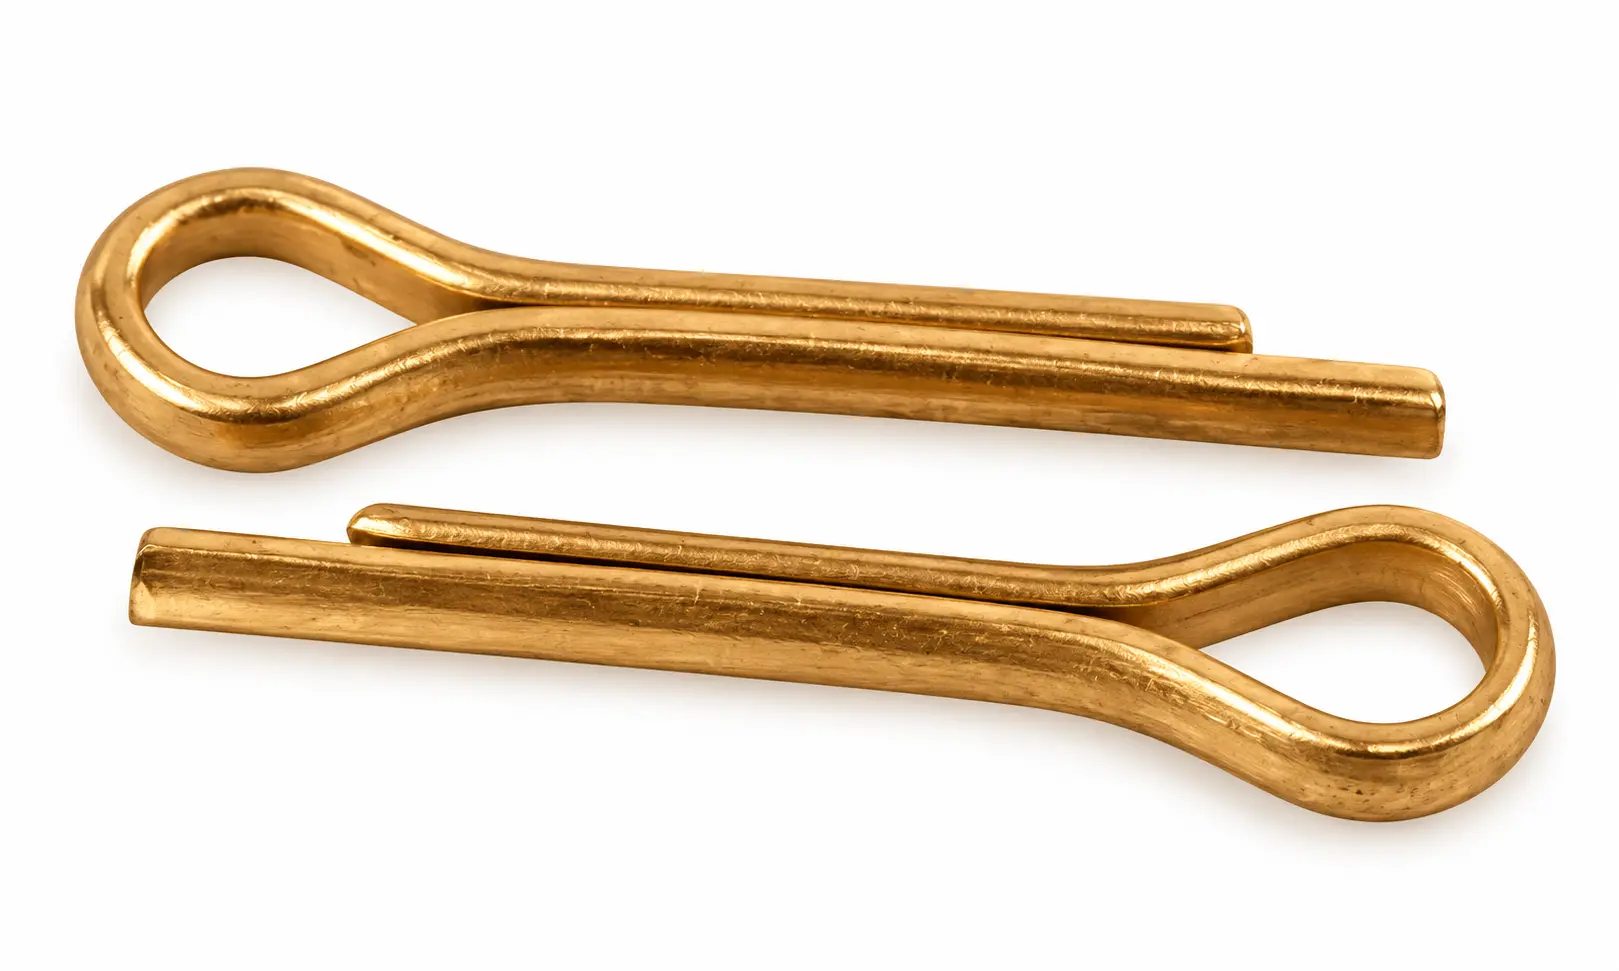
Nickel Aluminium Bronze C63000 Cotter Pins
Nickel Aluminium Bronze C63000
Cotter Pins
Nickel Aluminium Bronze C63000 Springs
Nickel Aluminium Bronze C63000
Springs
Nickel Aluminium Bronze C63000 Circlips
Nickel Aluminium Bronze C63000
Circlips
Nickel Aluminium Bronze C63000 Coated Fasteners
Nickel Aluminium Bronze C63000
Coated Fasteners
Nickel Aluminium Bronze C63000 Custom Spacers
Nickel Aluminium Bronze C63000
Custom Spacers
Technical Data

Nickel Aluminium Bronze C63000 Specifications

Chemical Composition — Nickel Aluminium Bronze C63000 (wt. %)
ElementMinimum %Maximum %
Copper (Cu) *Remainder—
Aluminium (Al)9.011.0
Nickel (Ni) **4.05.5
Iron (Fe)2.04.0
Manganese (Mn)—1.5
Zinc (Zn)—0.30
Silicon (Si)—0.25
Tin (Sn)—0.20
Copper + sum of named elements99.5—
Mechanical Properties — Nickel Aluminium Bronze C63000
ConditionUTS (MPa)YS 0.5% EUL (MPa)Elongation (%)Hardness
Bar 75 mm, as hot extruded M306213451596 HRB
Bar 50 mm, drawn and stress relieved HR506904141596 HRB
Bar 25 mm, drawn and stress relieved HR507584271597 HRB
Rod 100 mm, as hot extruded M306904141596 HRB
Rod 75 mm, drawn and stress relieved HR507724272096 HRB
Rod 50 mm, drawn and stress relieved HR507934481896 HRB
Rod 25 mm, drawn and stress relieved HR508145171598 HRB
ASTM F468 Cu 630 bolting, machined specimen690–896345 min5 min85–100 HRB
Physical Properties
Density7.58 g/cm³
Melting Range1035–1054 °C (1895–1930 °F)
Electrical Conductivity7% IACS at 20 °C
Thermal Conductivity39 W/m·K at 20 °C
Coefficient of Thermal Expansion16.2 × 10⁻⁶ /°C
Specific Heat Capacity377 J/kg·K at 20 °C
Modulus of Elasticity121 GPa
Modulus of Rigidity44 GPa
StructureAlpha + kappa — nickel suppresses gamma-2; dealuminification resistant
Machinability Rating30 (C36000 = 100)
Forgeability Rating75
Capacity for Cold WorkingPoor
Capacity for Hot FormingGood
Gas Shielded Arc WeldingGood
Oxyacetylene WeldingNot Recommended
Annealing Temperature593–704 °C (1100–1300 °F)
Hot Working Temperature788–927 °C (1450–1700 °F)
Magnetic ResponseNon-magnetic
Spark BehaviourNon-sparking
Equivalent Grades & Standards
UNSCDA NumberCDA Alloy NameCommon Name
C63000 CDA 630 Aluminum Bronze ASTM F468 Cu 630, AMS 4640, Nickel Aluminium Bronze C63000, CDA 630

Key Specifications: SAE J461 / SAE J463 / ASTM B124/B124M / AMS 4640 / ASTM F468 / MIL-B-16166 / ASME SB283 / ASTM B283/B283M / ASTM F467 / ASTM B171/B171M / ASME SB171 / ASTM B150/B150M / ASME SB150.

*The copper value includes silver. The nickel value includes cobalt.

ASTM F468 additionally specifies a copper minimum of 78.0% for Cu 630, where CDA give copper as the remainder. The final mechanical row is the F468 fastener requirement, which is a specified range and minimum rather than a typical value. CDA also publish a compressive strength of 1034 MPa at 0.1 in/in set and a fatigue strength of 255 MPa for 25 mm HR50 bar.

Note on fastener standards: C63000 is the strongest certified copper-alloy bolting material in the ASTM nonferrous fastener standards. ASTM F468 and F467 list C63000 as Cu 630, mechanical property marking F 468H, specified at 690–896 MPa (100–130 ksi) tensile with 345 MPa minimum yield at 85–100 HRB in all diameters, with 5% minimum elongation. Set that against the other certified copper alloys: Cu 613 at 552–758 MPa, Cu 614 at 517–758 MPa, and Cu 464 naval brass at 345 MPa with 103 MPa minimum yield. A Cu 630 bolt is in the strength class of a carbon steel structural bolt while being non-sparking, non-magnetic and better in seawater than any of them.

The trade is ductility: F468 requires only 5% minimum elongation for Cu 630 against 30% for Cu 613 and Cu 614, so where a joint needs to yield and redistribute load rather than simply hold, the lower-aluminium grades remain the better answer. C63000 is also covered by AMS 4640 and ASTM B150, B124, B171 and B283. The other grades on this hub are supplied to their mill and casting product standards — ASTM B150 and B315 for wrought rod, bar, shapes and tube, AMS 4590 for C63020 extrusions, and ASTM B148, B271, B505, B763 and B806 plus MIL-B-24480 for the castings — with thread conformance to the relevant ASME or ISO standard and acceptance criteria agreed on the order.

Every nickel aluminium bronze order ships with EN 10204 3.1 certification giving the heat analysis, the heat-treated condition, and the mechanical test results for the product form and section supplied. Aluminium, nickel, iron and manganese are reported explicitly, and the iron-to-nickel relationship is checked and stated — on C63200 and C95800 the specifications require that iron shall not exceed nickel, and a heat that meets every individual element range can still fail on that comparison. Heat-treatment certification to the specified cycle, hardness survey across section, microstructural examination for gamma-2 and for kappa phase distribution, dealuminification testing, impact testing and positive material identification can all be added at order stage.

Machining: nickel aluminium bronze is tougher and more work hardening than plain aluminium bronze, and the kappa phases that give it its wear resistance also abrade tooling. CDA machinability ratings here are low: 30 for the wrought grades C63000 and C63200, 50 for the cast C95500, and only 20 for C95800 — the propeller alloy is the hardest of the group to cut. For comparison C36000 free-cutting brass is the 100 on that scale, and no leaded nickel aluminium bronze exists because lead and aluminium together make the alloy hot short.

What works: rigid setups and heavy, continuous cuts, because the alloy work hardens severely the moment a tool rubs or dwells; positive rake on a keen, well-supported edge; low surface speed with generous feed, never the reverse; carbide as standard, with ceramic or CBN on the harder heat-treated conditions; and flood coolant throughout. Take the cut under the previously work-hardened layer rather than skimming it. Expect tool life well below brass practice and plan the sequence so that finishing passes are not interrupted. Where a part is to be both heat treated and machined, rough machine, heat treat, then finish — the quench will move the part.

Heat treatment is where nickel aluminium bronze is most often got wrong, and the two cast grades here behave differently.

C95500 is quench hardenable. CDA publish the full cycle: solution treat at 871–913 °C (1600–1675 °F) for one hour, water quench, then temper anneal at 621–663 °C (1150–1225 °F) for one hour — the TQ50 condition. On sand castings that lifts the specified minimum tensile from 621 to 758 MPa and Brinell from 190 to 200, with typical values reaching 827 MPa and 230 HB, at the cost of dropping minimum elongation from 6% to 5%.

C95800 is not. CDA register a stress relief at 316 °C (600 °F) and no solution treatment cycle, and publish no TQ50 properties for it. C95800 is used in the as-cast condition, and where a thermal treatment is required — typically a temper anneal after welding or on heavy sections for naval work — the requirement comes from the governing specification, MIL-B-24480 or the purchaser's own, rather than from the CDA record. Do not assume the C95400 or C95500 cycle applies to it.

On the wrought side, C63000 and C63200 are supplied hot worked and then either light annealed (O50) or drawn and stress relieved (HR50), with annealing ranges of 593–704 °C and 621–704 °C respectively. C63020 is different again: AMS 4590 specifies it as martensitic, solution heat treated and tempered extrusions, which is the highest-strength condition available in a wrought nickel aluminium bronze. On every grade here, specify the condition on the order — it governs strength, and on the alpha-beta grades it governs corrosion behaviour too.

Welding: nickel aluminium bronze welds well by gas shielded arc processes and badly by everything else, for the same reason as plain aluminium bronze — the refractory alumina film. CDA rate gas shielded arc welding (GTAW/TIG and GMAW/MIG) as Good across the family and Excellent for C63200, and coated metal arc welding as Good. Oxyacetylene welding is Not Recommended on every grade here, because the oxide cannot be reduced by the flame, and brazing is only Fair.

The heat-affected zone is the real issue on this family. Weld thermal cycles can re-introduce the very phases the nickel is there to suppress: slow cooling through the eutectoid range in the HAZ of a high-aluminium heat can form gamma-2 locally and leave a narrow band that dealuminifies in service while the parent metal is untouched. Control interpass temperature, avoid excessive heat input, and temper anneal after welding where the part will be immersed — for C95800 naval work this is normally a requirement of MIL-B-24480 rather than an option. Clean back to bright metal immediately before welding, use argon or argon-helium with good coverage front and back, and qualify the procedure on the alloy and section rather than on a generic aluminium bronze procedure. C95800 and C63200 are both widely used as weld-repair and overlay consumables for propellers and seawater castings.

Nickel is the whole point of this family, and what it does is chemical rather than simply strengthening. A plain aluminium bronze above about 9.4% aluminium carries a beta phase at temperature, and on slow cooling through roughly 565 °C that beta decomposes to alpha plus gamma-2 (γ₂, Cu₉Al₄) — a hard, brittle intermetallic that corrodes preferentially and is the direct cause of dealuminification. Adding 4% nickel or more suppresses that eutectoid decomposition outright. The gamma-2 does not form, and the alloy keeps the strength of a high-aluminium bronze without the corrosion liability that normally comes with it.

What forms instead is a family of iron- and nickel-rich kappa (κ) phases — conventionally κI to κIV, differing in size, composition and where they nucleate. These are dispersed, relatively noble intermetallics. They raise strength, hardness and wear resistance, they pin the grain structure at temperature, and crucially they do not set up the galvanic couple that destroys a gamma-2-bearing alloy in seawater. That single substitution — kappa in place of gamma-2 — is why nickel aluminium bronze, and not plain aluminium bronze, is the standard material for ship propellers, seawater pumps, valves and offshore hardware.

The iron-to-nickel rule follows directly from this, and it is written into the specifications. Both C63200 and C95800 carry the explicit requirement that the iron content shall not exceed the nickel content. Iron and nickel are both kappa formers, but an excess of iron over nickel leaves too little nickel in solution to do the eutectoid-suppressing job, and the corrosion resistance falls away. A heat that meets every individual element range and still has Fe > Ni is non-conforming. Check it on the certificate; it is the single most commonly overlooked acceptance criterion on this family.

Nickel aluminium bronze is the benchmark copper alloy for seawater, and the case for it is unusually broad. The alumina-rich surface film is tenacious and self-healing, and the nickel-modified structure removes the dealuminification weakness that limits plain aluminium bronze. The result is a material that handles conditions no other copper alloy manages together: high-velocity and turbulent seawater without impingement attack; cavitation at propeller blade tips and pump inlets, where it outperforms stainless steels on an erosion-rate basis; crevice and pitting conditions that would attack austenitic stainless; and long-term biofouling resistance from the copper matrix, which keeps hulls and intakes clearer than passive alloys do.

It also behaves well where it matters practically. It is non-sparking and essentially non-magnetic, which is why it appears in minehunter and naval fittings and in safety tools. It keeps useful strength and toughness at cryogenic temperature — CDA list cryogenic valve parts among the uses for C63020 — and it does not undergo a ductile-to-brittle transition. And it retains strength at elevated temperature better than brasses or tin bronzes.

The limits should be stated plainly. Oxidising acids, notably nitric, attack it. Stagnant, sulphide-polluted seawater is its worst case: the protective film does not form properly in sulphide-bearing water, and a layup period in a polluted harbour can do more damage than years of service at speed. Ammonia and amines can still cause stress-corrosion cracking. And in a galvanic couple it is cathodic to steel, so steel fasteners in a nickel aluminium bronze component will be attacked — match the materials or isolate them.

Heat treatment is where nickel aluminium bronze is most often got wrong, and the two cast grades here behave differently.

C95500 is quench hardenable. CDA publish the full cycle: solution treat at 871–913 °C (1600–1675 °F) for one hour, water quench, then temper anneal at 621–663 °C (1150–1225 °F) for one hour — the TQ50 condition. On sand castings that lifts the specified minimum tensile from 621 to 758 MPa and Brinell from 190 to 200, with typical values reaching 827 MPa and 230 HB, at the cost of dropping minimum elongation from 6% to 5%.

C95800 is not. CDA register a stress relief at 316 °C (600 °F) and no solution treatment cycle, and publish no TQ50 properties for it. C95800 is used in the as-cast condition, and where a thermal treatment is required — typically a temper anneal after welding or on heavy sections for naval work — the requirement comes from the governing specification, MIL-B-24480 or the purchaser's own, rather than from the CDA record. Do not assume the C95400 or C95500 cycle applies to it.

On the wrought side, C63000 and C63200 are supplied hot worked and then either light annealed (O50) or drawn and stress relieved (HR50), with annealing ranges of 593–704 °C and 621–704 °C respectively. C63020 is different again: AMS 4590 specifies it as martensitic, solution heat treated and tempered extrusions, which is the highest-strength condition available in a wrought nickel aluminium bronze. On every grade here, specify the condition on the order — it governs strength, and on the alpha-beta grades it governs corrosion behaviour too.

How these grades divide. On the wrought side, C63000 at 9.0–11.0% aluminium and 4.0–5.5% nickel is the general-purpose high-strength grade and the ASTM F468 Cu 630 fastener alloy, reaching 814 MPa in drawn and stress relieved rod. C63200 drops the aluminium to 8.7–9.5% and adds 1.2–2.0% manganese: slightly lower strength, noticeably better ductility at 20–25% elongation, Excellent weldability, and the Fe ≤ Ni rule — it is the grade for welded seawater fabrications and plate. C63020 is the martensitic, solution treated and tempered extrusion alloy of AMS 4590, for heavily loaded bearings, bushings and valve balls — though CDA register composition and specifications only, with no published properties.

On the cast side, C95500 at 10.0–11.5% aluminium is the quench-hardenable high-strength casting, reaching 758 MPa minimum in the TQ50 condition, and C95800 at 8.5–9.5% is the standard marine propeller alloy — lower strength, far better ductility at 15–25% elongation, the Fe ≤ Ni rule, and MIL-B-24480 coverage. For completeness the hub also lists C95400, which is frequently bought alongside these but is not a nickel aluminium bronze — CDA class it as a plain copper-aluminium-iron casting alloy with nickel only as a 1.5% maximum limit, and it is documented on the aluminium bronze hub.
Key Characteristics

  • The general-purpose high-strength wrought nickel aluminium bronze.
  • 9.0–11.0% Al with 4.0–5.5% Ni and 2.0–4.0% Fe.
  • ASTM F468 / F467 Cu 630 — the strongest certified copper-alloy bolting.
  • Bolting specified at 690–896 MPa with 345 MPa minimum yield.
  • 814 MPa typical in 25 mm drawn and stress relieved rod.
  • Nickel suppresses gamma-2 — strength without dealuminification risk.
  • Only 5% minimum elongation under F468 — strong but unforgiving.
  • Also covered by AMS 4640, ASTM B150, B124, B171 and B283.

Typical Applications

  • Certified marine and offshore bolting to ASTM F468.
  • High-strength studs, nuts and threaded members.
  • Pump and valve shafts and stems.
  • Forged marine and offshore hardware.
  • Seawater system fasteners and fittings.
  • Non-sparking high-strength tools and hardware.
  • Hydraulic and heavy equipment components.
  • Tube sheets and condenser hardware.