+91 97734 41022 sales@exoticalloy.com
Material Specification

Aluminium Bronze C95400

Aluminium Bronze C95400 Fasteners
Cast Aluminium Bronze

Aluminium Bronze C95400 Fasteners

C95400 is the standard general-purpose aluminium bronze casting alloy — copper 83.0% minimum with 10.0–11.5% aluminium, 3.0–5.0% iron and nickel to 1.5%. It is the cast counterpart of C62400 and by a wide margin the most commonly specified aluminium bronze casting, listed under ASTM B148, B505, B271, B763, B66, B806 and B30.

Its defining feature is that it is quench hardenable. In the as-cast M01 condition it is specified at 517 MPa with 207 MPa yield, 12% elongation and 150 HB. Solution treated at 871–913 °C, water quenched and temper annealed at 621–663 °C — the TQ50 condition — the same alloy is specified at 621 MPa and 190 HB, with typical values of 724 MPa and 195 HB, at the cost of halving elongation to 6%. That treatment also controls the gamma-2 phase and so governs dealuminification resistance, which is why the heat-treated condition should be stated on the order for immersed service. C95400 is also the easiest alloy on this hub to machine, at a rating of 60. Exotic Alloy supplies C95400 castings, cast bar and machined cast components.

Request a Quote
Product Range

Aluminium Bronze C95400 Fasteners Available

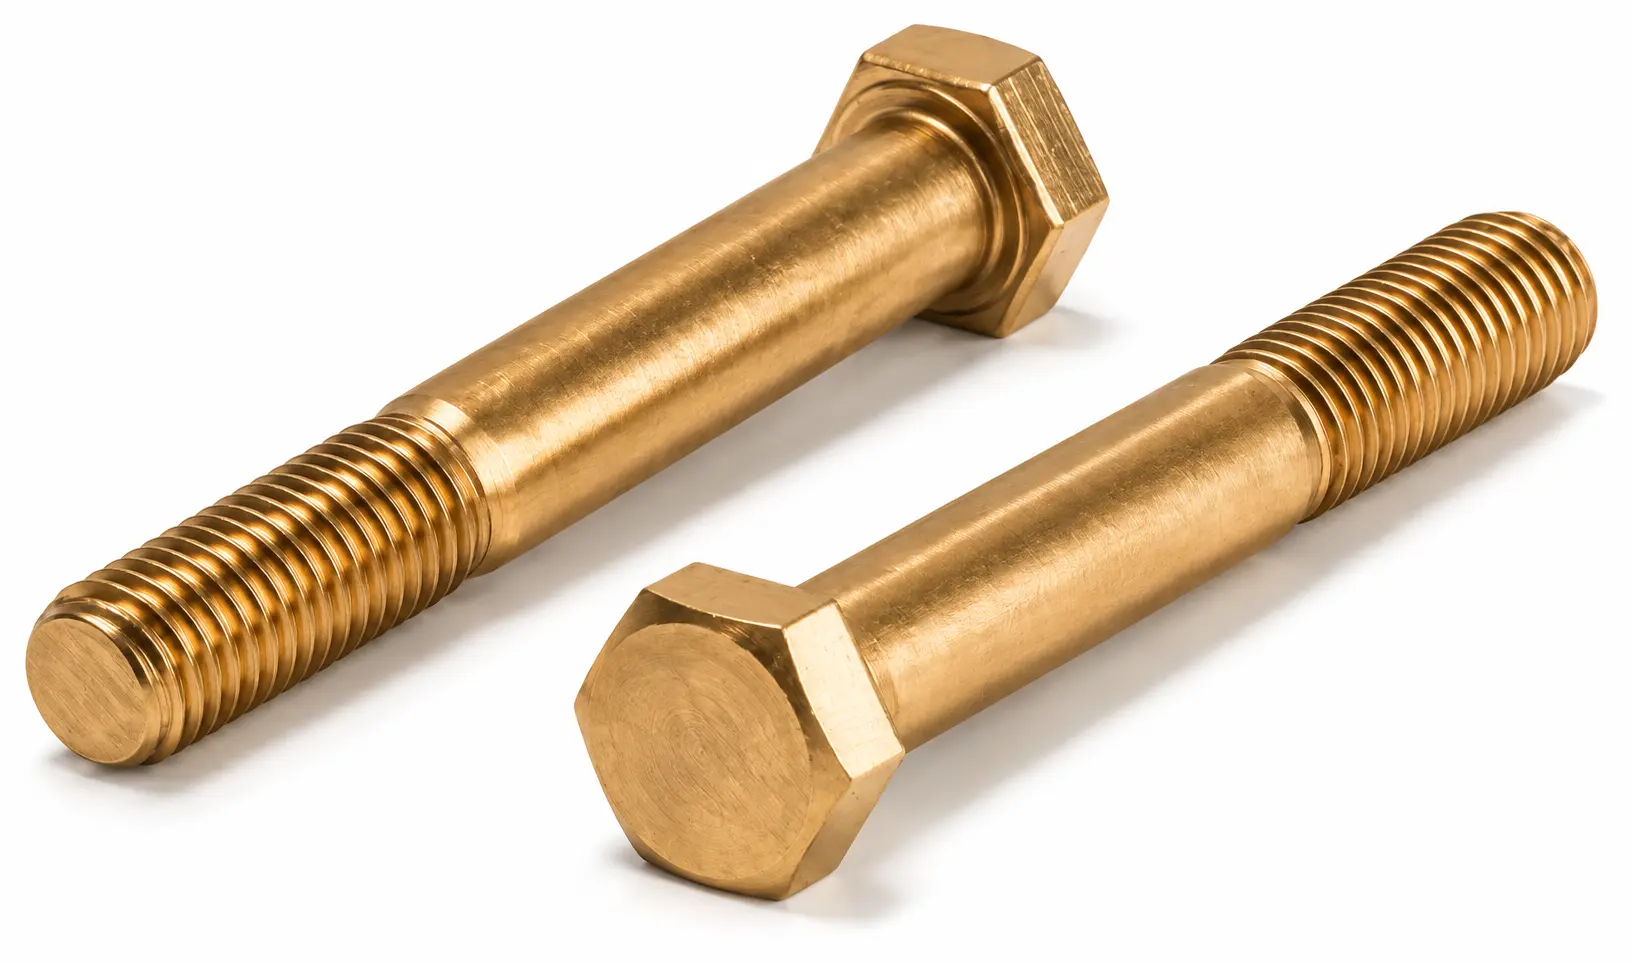
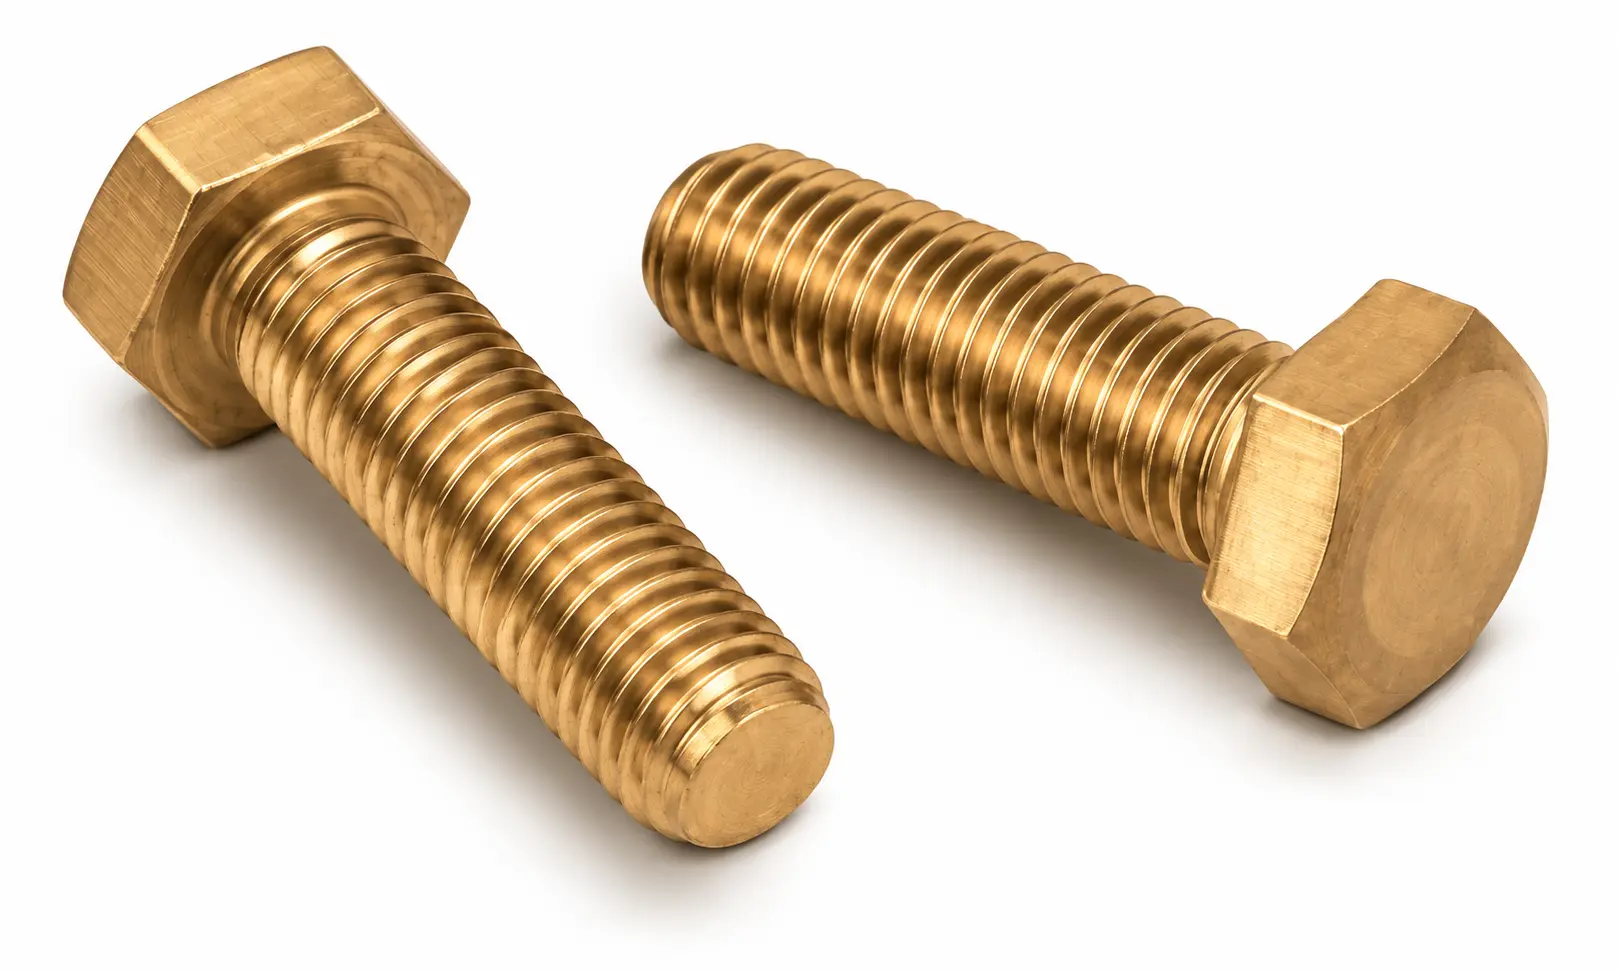
Aluminium Bronze C95400 Hex Bolts
Aluminium Bronze C95400
Hex Bolts
Aluminium Bronze C95400 Heavy Hex Bolts
Aluminium Bronze C95400
Heavy Hex Bolts
Aluminium Bronze C95400 Stud Bolts
Aluminium Bronze C95400
Stud Bolts
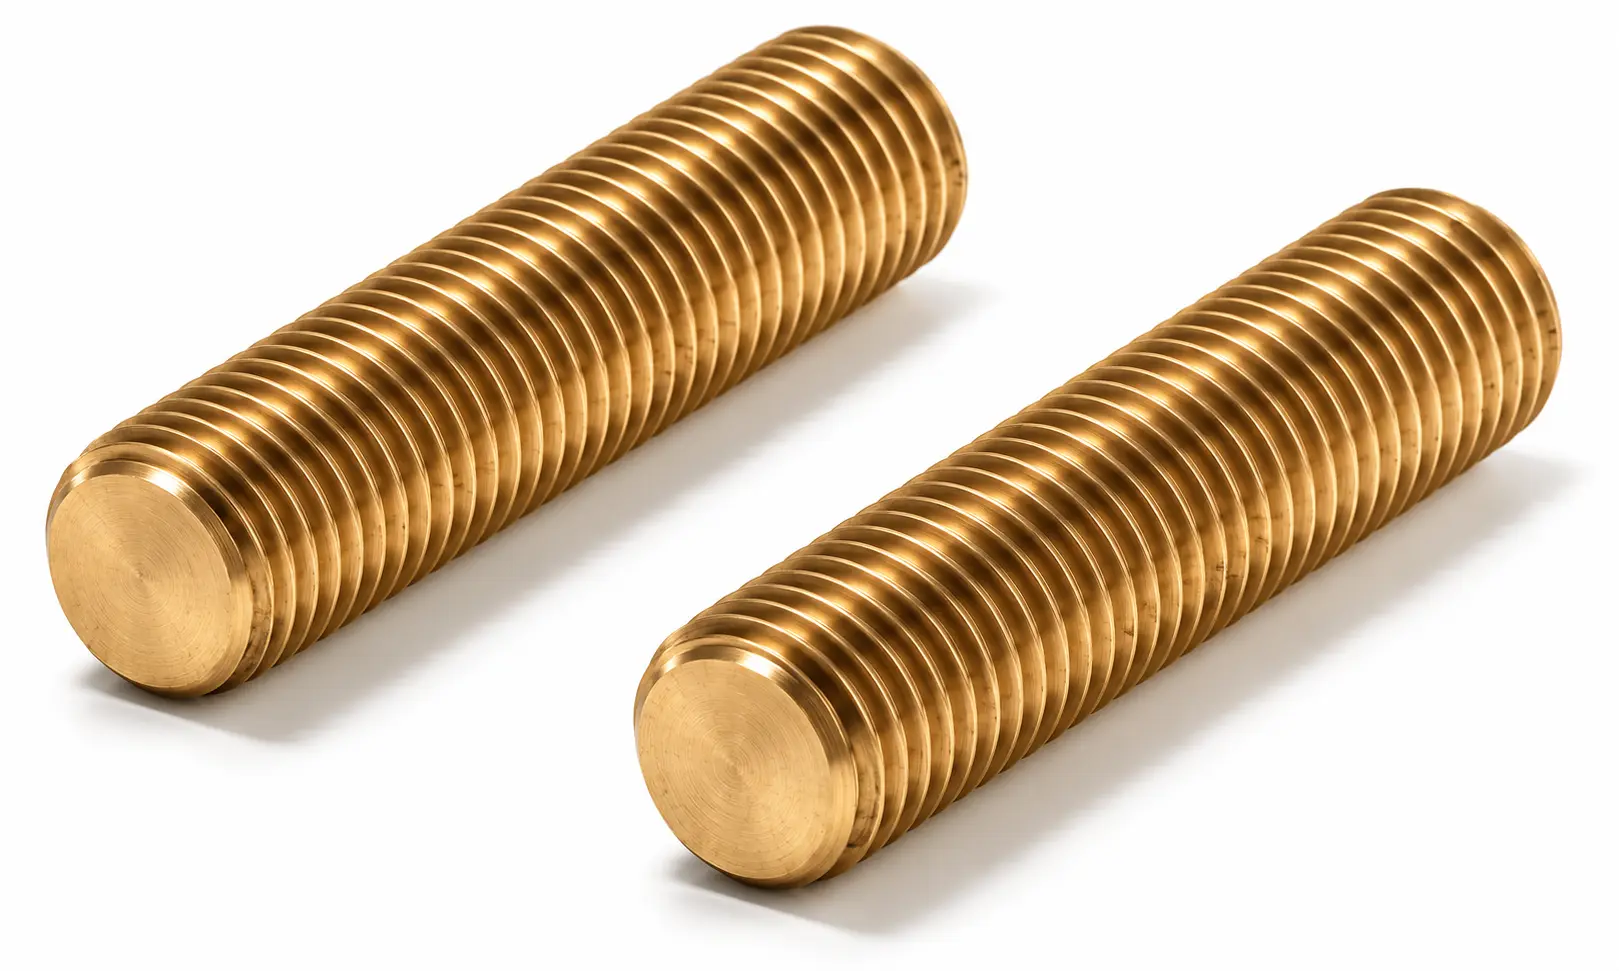
Aluminium Bronze C95400 Threaded Rods
Aluminium Bronze C95400
Threaded Rods
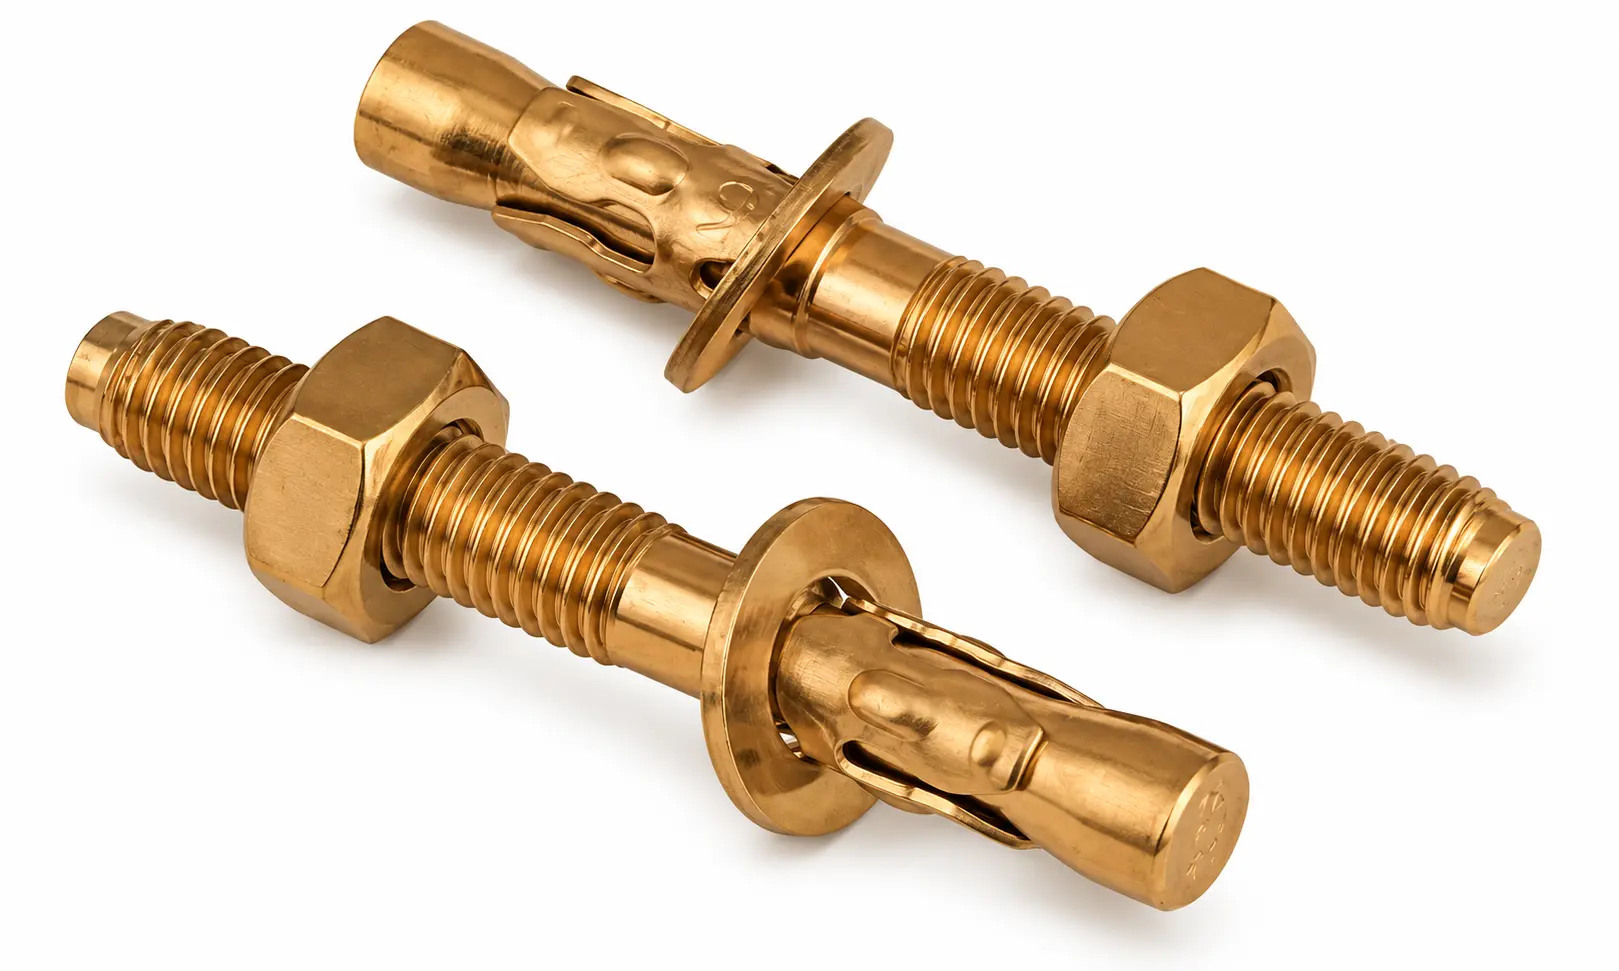
Aluminium Bronze C95400 Anchor Bolts
Aluminium Bronze C95400
Anchor Bolts
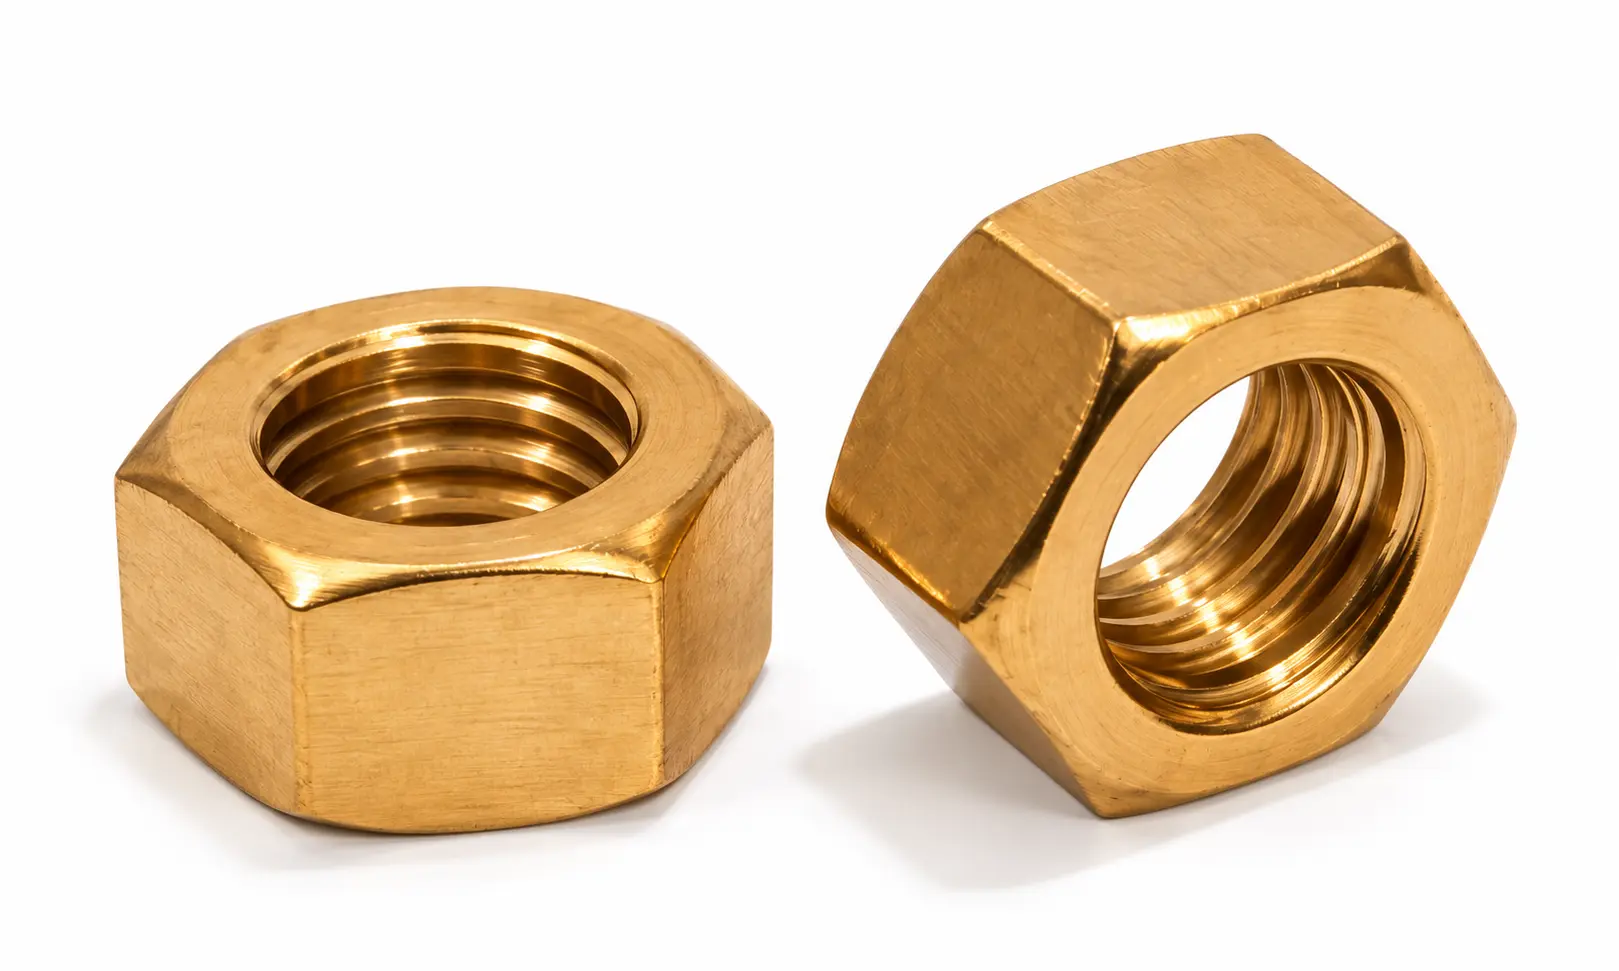
Aluminium Bronze C95400 Hex Nuts
Aluminium Bronze C95400
Hex Nuts
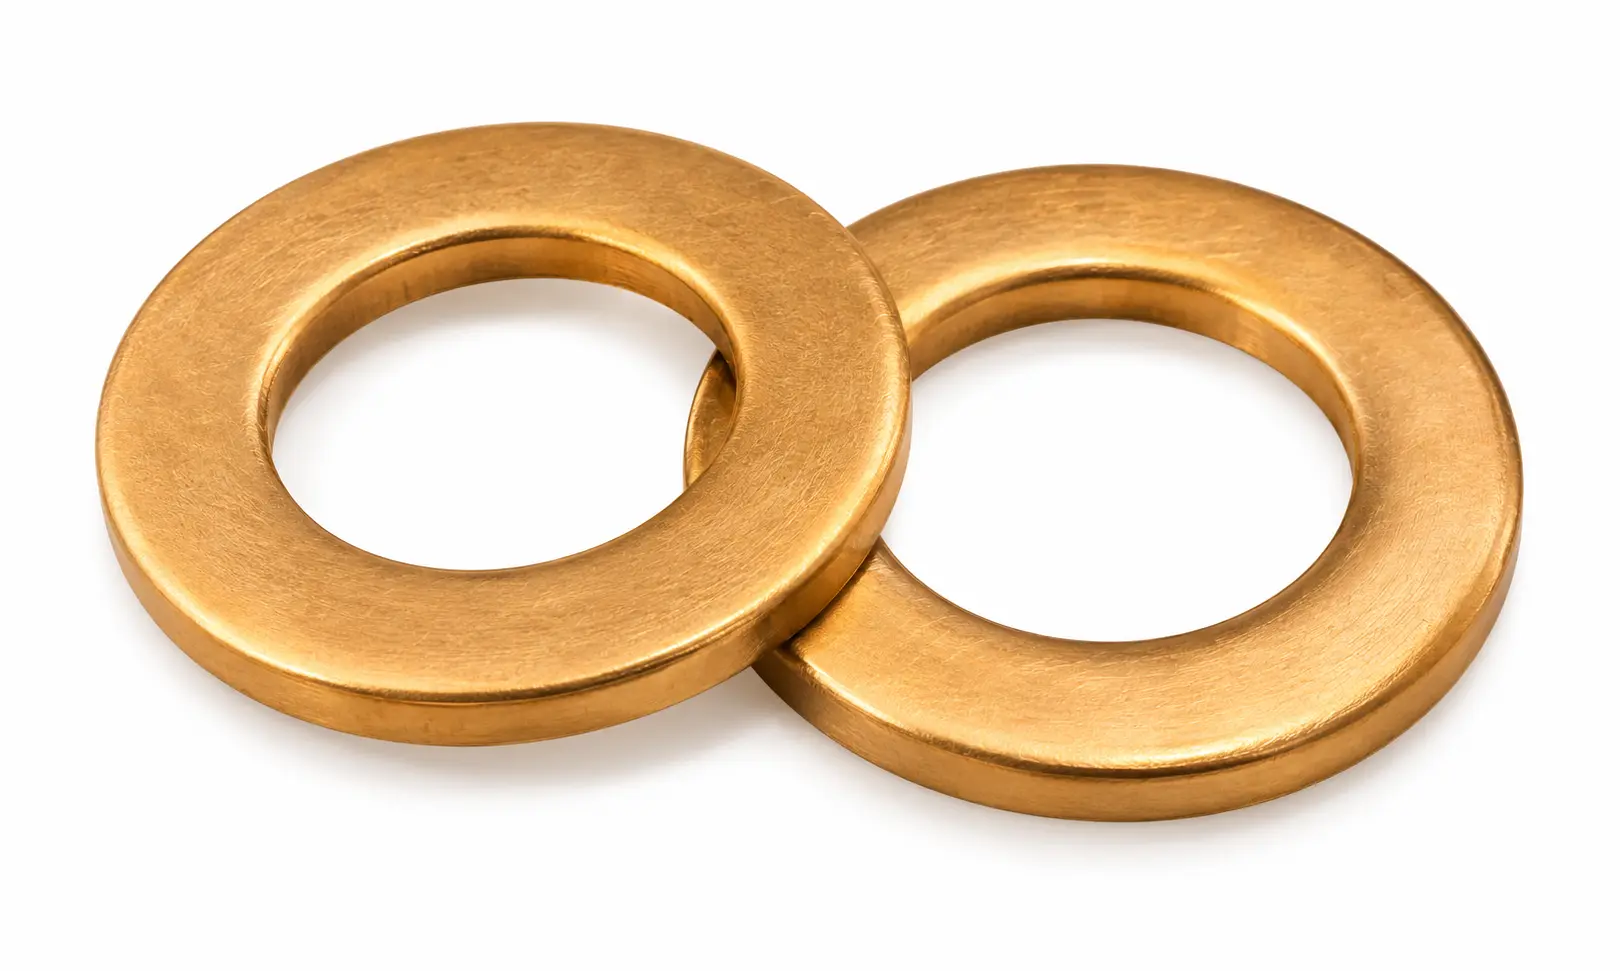
Aluminium Bronze C95400 Washers
Aluminium Bronze C95400
Washers
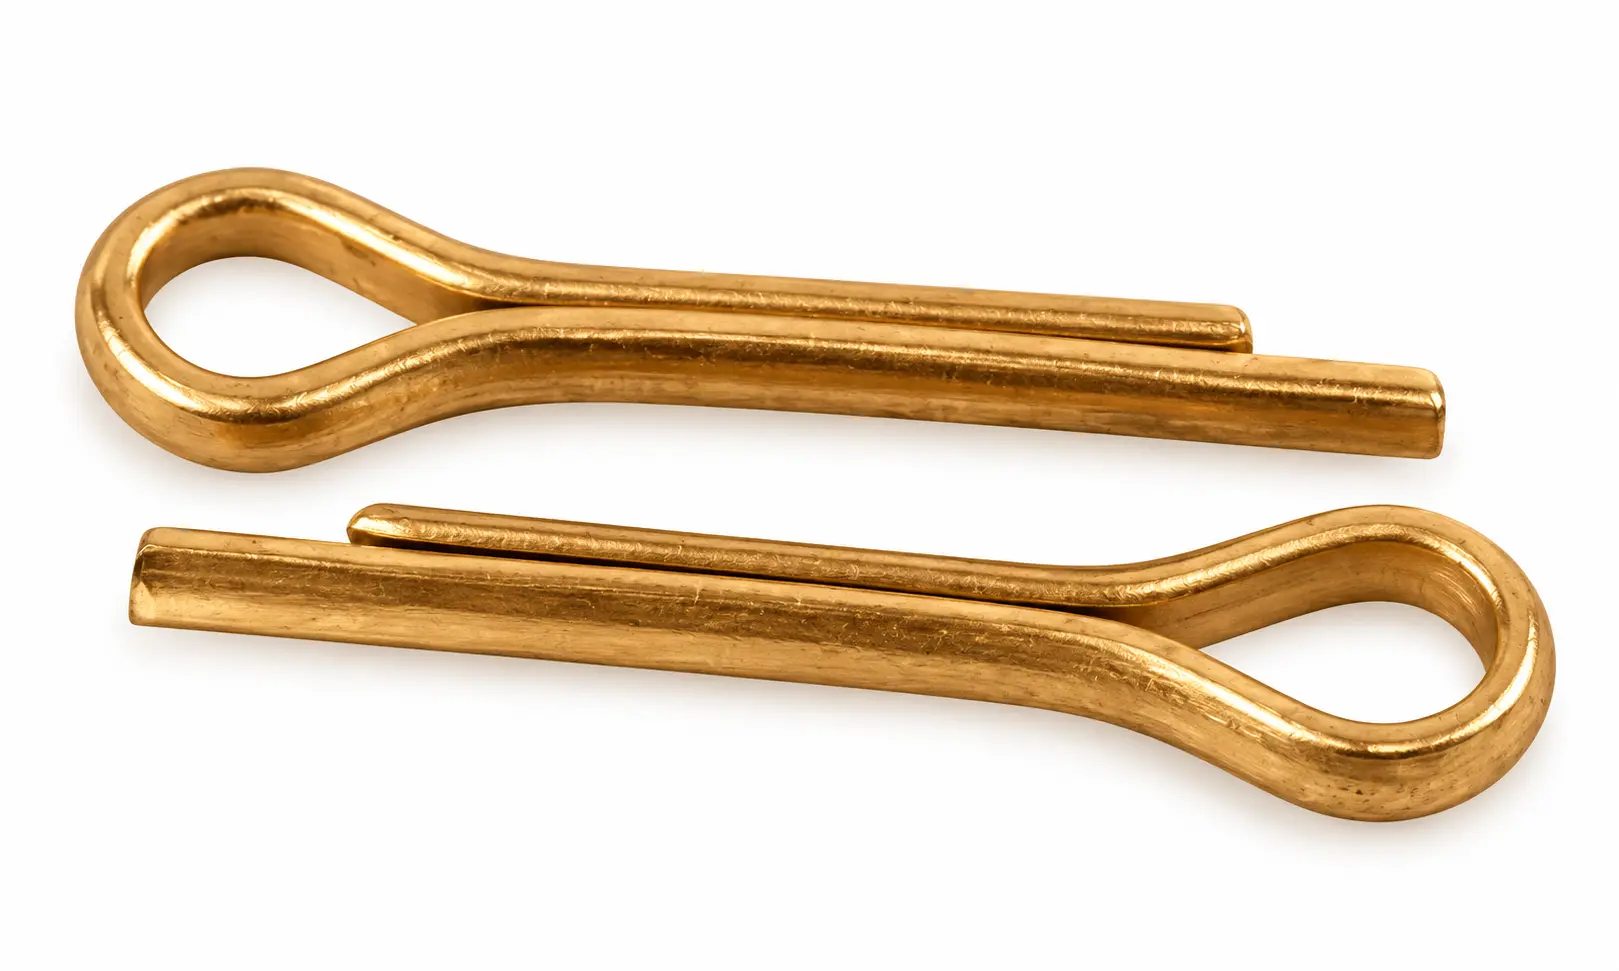
Aluminium Bronze C95400 Cotter Pins
Aluminium Bronze C95400
Cotter Pins
Aluminium Bronze C95400 Springs
Aluminium Bronze C95400
Springs
Aluminium Bronze C95400 Circlips
Aluminium Bronze C95400
Circlips
Aluminium Bronze C95400 Coated Fasteners
Aluminium Bronze C95400
Coated Fasteners
Aluminium Bronze C95400 Custom Spacers
Aluminium Bronze C95400
Custom Spacers
Technical Data

Aluminium Bronze C95400 Specifications

Chemical Composition — Aluminium Bronze C95400 (wt. %)
ElementMinimum %Maximum %
Copper (Cu) *83.0—
Aluminium (Al)10.011.5
Iron (Fe)3.05.0
Nickel (Ni) **—1.5
Manganese (Mn)—0.50
Copper + sum of named elements99.5—
Mechanical Properties — Aluminium Bronze C95400
ConditionUTS (MPa)YS 0.5% EUL (MPa)Elongation (%)Hardness
Sand cast M01 — minimum51720712150 HB
Sand cast M01 — typical58624118170 HB
Sand cast TQ50 — minimum621—6190 HB
Sand cast TQ50 — typical7243728195 HB
Centrifugal cast M02 — minimum51720712150 HB
Centrifugal cast TQ50 — minimum621—6190 HB
Continuous cast M07 — minimum58622112—
Continuous cast TQ50 — minimum655—10—
Permanent mould cast M05 — minimum69027610—
Permanent mould cast M05 — typical72431711—
Physical Properties
Density7.45 g/cm³
Melting Range1027–1038 °C (1880–1900 °F)
Electrical Conductivity13% IACS at 20 °C
Thermal Conductivity59 W/m·K at 20 °C
Coefficient of Thermal Expansion16.2 × 10⁻⁶ /°C
Specific Heat Capacity419 J/kg·K at 20 °C
Modulus of Elasticity107 GPa
StructureCast alpha-beta — quench hardenable to the TQ50 condition
Machinability Rating60 (C36000 = 100)
Gas Shielded Arc WeldingGood
Oxyacetylene WeldingNot Recommended
Annealing Temperature621–663 °C (1150–1225 °F)
Stress Relief Temperature316 °C (600 °F)
Solution Treatment871–913 °C (1600–1675 °F), 1 hour, water quench
Magnetic ResponseNon-magnetic
Spark BehaviourNon-sparking
Equivalent Grades & Standards
UNSCDA NumberCDA Alloy NameCommon Name
C95400 CDA 954 Not registered by CDA ASTM B148 C95400, Cast Aluminium Bronze, CDA 954

Key Specifications: SAE J461 / ASTM B271/B271M / SAE J462 / ASME SB271 / ASTM B505/B505M / ASTM B806 / ASTM B148 / ASTM B763/B763M / ASME SB148 / ASTM B66 / ASTM B30 / MIL-C-11866.

*In determining the copper minimum, copper may be calculated as Cu + Ni. **The nickel value includes cobalt.

Sand cast typical figures also include a shear strength of 324 MPa, compressive strength of 690 MPa at 0.1 in/in set, creep strength of 51 MPa, fatigue strength of 193 MPa and a proportional limit of 117 MPa. In the TQ50 condition the typical shear strength is 345 MPa, Izod 11 ft-lb, Charpy V-notch 7 ft-lb, compressive strength 827 MPa and fatigue strength 241 MPa. CDA publish no yield figure for the specified-minimum TQ50 rows; the 372 MPa value shown is the sand cast typical.

Note on fastener standards: Two aluminium bronzes on this hub are covered by the ASTM nonferrous fastener standards, and they are the strongest brass or bronze grades in those standards. ASTM F468 and F467 list C61300 as Cu 613, mechanical property marking F 468F, and C61400 as Cu 614, marking F 468G. Cu 613 bolting is specified at 552–758 MPa (80–110 ksi) tensile with 345 MPa minimum yield in sizes to 13 mm, and Cu 614 at 517–758 MPa with 241 MPa minimum yield in all sizes, both at 70–95 HRB and 30% minimum elongation. For comparison, a naval brass bolt to Cu 464 is specified at 345 MPa with 103 MPa minimum yield: an aluminium bronze bolt carries roughly two to three times the yield of a brass one and resists seawater better.

That combination — high strength, seawater resistance, non-sparking and non-magnetic behaviour, and no beryllium handling regime — makes Cu 613 and Cu 614 the default certified copper-alloy bolting for marine, offshore, desalination and chemical plant duty. The other six grades here are supplied to their mill product standards — ASTM B150 for rod, bar and shapes, B169 for plate, sheet, strip and rolled bar, B124 and B283 for forgings, B111 and B315 for tube, B148 and B505 for castings — with thread conformance to the relevant ASME or ISO standard and acceptance criteria agreed on the order.

Every aluminium bronze order ships with EN 10204 3.1 certification giving the heat analysis, the temper or heat-treated condition, and the mechanical test results for the product form and section supplied. Aluminium, iron and nickel are reported explicitly — aluminium sets the phase structure and therefore the heat-treatability and dealuminification behaviour, while iron and nickel control grain size and eutectoid suppression. Heat-treatment certification to the specified cycle, hardness survey, microstructural examination for gamma-2 and continuous beta, dealuminification testing and positive material identification can all be added at order stage.

Machining: aluminium bronze is tough, strongly work hardening and abrasive, and it is the most demanding of the common copper alloys to cut. CDA machinability ratings on this hub run from 20 for the single-phase alpha grades C61000, C61400 and C62500, through 30 for C61300, to 50 for the forging grades C62300 and C62400 and 60 for the cast C95400, which is the easiest of the family. None of them approaches a leaded brass — C36000 is the 100 on that scale — and no leaded aluminium bronze exists, because lead and aluminium together make the alloy hot short.

What works: rigid setups and heavy, uninterrupted cuts, because the alloy work hardens severely if the tool dwells or rubs; positive rake with a keen, well-supported edge; reduced surface speed with generous feed rather than the reverse; carbide tooling as standard, and flood coolant throughout. The alumina film and the hard phases in the high-aluminium grades abrade tooling, so expect tool life well below brass practice. The alpha grades produce continuous stringy swarf and need chip breakers. Drilling and tapping call for sharp, frequently regrounds tools and firm feed to stay under the work-hardened layer.

Heat treatment splits this family in two, and the aluminium content tells you which half a grade is in.

The alpha grades — C61000, C61300 and C61400, at 6–8.5% aluminium — are not hardenable. Strength comes from cold work, and the temper designations record it: O60 and O61 soft annealed, M20 and M30 as hot rolled or extruded, then H01, H02, H04 and above as cold reduction increases. Annealing is in the 605–900 °C range depending on grade and product, and HR50 drawn-and-stress-relieved is a common supply condition for rod, giving the cold-worked strength with the residual stress removed.

The alpha-beta grades — C61900, C62300, C62400, C62500 and the cast C95400, at 8.5–13.5% aluminium — are quench hardenable, like a steel. The part is solution treated in the beta field, water quenched to suppress the eutectoid decomposition to brittle gamma-2, and then temper annealed to develop the final structure. For C95400 CDA publish the cycle explicitly: solution treat at 871–913 °C (1600–1675 °F) for one hour, water quench, then temper anneal at 621–663 °C (1150–1225 °F) for one hour. That is the TQ50 condition, and on C95400 it lifts the specified minimum tensile from 517 to 621 MPa and Brinell from 150 to 190 while halving elongation. C61900 strip is supplied in treated tempers on the same principle — HT04 and HT08 are the hard and spring tempers after treatment, reaching 931 and 1000 MPa.

Stress relief at around 316 °C (600 °F) is specified for C95400 castings and is worth applying to any heavily cold-worked, welded or intricately machined aluminium bronze part. Specify the heat-treated condition explicitly on the order: on the alpha-beta grades it governs not only strength but dealuminification resistance, and a slow-cooled part can meet the composition limits and still be wrong for immersed service.


Everything about an aluminium bronze follows from its aluminium content, because aluminium decides the phase structure. Below roughly 8% aluminium the alloy is single-phase alpha: face-centred cubic, ductile, cold formable, readily welded, and not hardenable by heat treatment — strength comes from cold work alone. Above roughly 9.4% aluminium a second beta phase is stable at temperature and the alloy becomes alpha-beta. That changes the alloy fundamentally: it becomes much stronger, it hot forges and extrudes superbly, and — uniquely among the common copper alloys — it can be quenched and tempered like a steel.

The catch is the eutectoid. On slow cooling through about 565 °C the beta phase decomposes to alpha plus gamma-2 (γ₂, Cu₉Al₄), a hard, brittle intermetallic that embrittles the alloy and, worse, corrodes preferentially. Rapid cooling from the beta field suppresses the eutectoid and produces a hard martensitic beta; a subsequent temper anneal then develops a controlled, fine alpha-plus-precipitate structure with good strength and good corrosion behaviour. This is why the high-aluminium grades are supplied quenched and temper-annealed rather than slow cooled, and why heat-treatment control is a genuine quality issue on this family rather than a formality.

On this hub the division is clean. C61000, C61300 and C61400 sit at 6–8.5% aluminium and are single-phase alpha — formable, weldable, dealuminification-resistant, the grades to specify for tube, plate and fasteners. C61900, C62300, C62400, C62500 and the cast C95400 run from 8.5% to 13.5% aluminium and are alpha-beta — stronger, hot worked, heat treatable, and progressively harder, more wear resistant and less ductile as the aluminium rises.

Aluminium bronze owes its corrosion resistance to an aluminium oxide film, not a copper one, and that is what separates it from every other copper alloy. The 6–13% aluminium forms a thin, tenacious, self-healing alumina-rich surface layer that is far more stable than the cuprous oxide film on a brass or a tin bronze. The practical consequences are large: outstanding resistance in seawater and brackish water, including at high flow velocity where a brass would be stripped by impingement; good resistance to non-oxidising acids — dilute sulphuric, hydrochloric and phosphoric — and to many organic acids, alkalis and process chemicals; excellent erosion, cavitation and impingement resistance, which is why pump impellers and valve trim are made from it; and high resistance to biofouling from the copper matrix.

It is also non-sparking and essentially non-magnetic, which puts aluminium bronze alongside beryllium copper as a safety-tool and magnetically-sensitive-environment material — without beryllium's particulate controls. And it retains useful strength at elevated temperature, where most copper alloys soften quickly.

The limits are worth stating plainly. Oxidising acids, notably nitric acid, attack it. Ammonia and ammonium compounds can cause stress-corrosion cracking, as they do in brass. Sulphide-polluted stagnant seawater degrades the protective film. And the alpha-beta grades are susceptible to dealuminification if the structure is wrong — see below.

Dealuminification is the aluminium bronze analogue of dezincification, and it is the one failure mode to design against. Aluminium is selectively leached out of the alloy, leaving a porous, weak, copper-rich residue that keeps the original shape of the part — exactly the deceptive failure that makes dezincification dangerous in brass. A dealuminified pump casing or valve body can look sound and have almost no remaining strength.

It is a structural problem, not simply a compositional one. Attack concentrates on the gamma-2 phase formed when an alpha-beta alloy is cooled slowly through the eutectoid, and on continuous beta networks. There are three defences. Stay single phase — below about 8% aluminium the alloy is alpha and the problem largely disappears, which is why C61300 and C61400 are the grades specified for long-life seawater tube and fastening. Control the heat treatment — quench from the beta field and temper anneal, so that the gamma-2 is suppressed and the structure is fine and discontinuous; this is the route used for C95400 castings in the TQ50 condition. Add nickel — at about 4% and above, nickel suppresses the eutectoid decomposition outright, which is the whole reason the nickel aluminium bronzes exist as a separate family for critical seawater service. Where a part will spend its life immersed, state the required structure and heat-treated condition on the order rather than relying on the composition limits alone.

How eight grades divide. Read the aluminium figure first. The single-phase alpha grades at 6–8.5% aluminium are the formable, weldable, corrosion-first choices: C61000 is the simplest and most conductive at 15% IACS, C61300 adds 0.20–0.50% tin for improved corrosion resistance and is the ASTM F468 Cu 613 fastener grade, and C61400 is the iron-bearing workhorse for condenser tube, plate and heat exchangers and the ASTM F468 Cu 614 fastener grade. The alpha-beta grades trade formability for strength and wear resistance as aluminium climbs: C61900 at 8.5–10% is a heat-treatable strip and spring alloy reaching 1048 MPa, the strongest figure on this hub; C62300 at 8.5–10% and C62400 at 10–11.5% are the forging grades, with the best machinability of the wrought family at 50; and C62500 at 12.5–13.5% is a hard, essentially non-ductile wear and die material. Finally C95400 is the cast member of the family — the standard general-purpose aluminium bronze casting alloy, quench hardenable to 621 MPa minimum, and the easiest here to machine at 60.
Key Characteristics

  • The standard general-purpose aluminium bronze casting alloy.
  • Copper 83.0% min with 10.0–11.5% Al and 3.0–5.0% Fe.
  • A CAST alloy — every other grade on this hub is wrought.
  • Quench hardenable: 517 MPa as cast, 621 MPa minimum at TQ50.
  • Solution treat 871–913 °C, water quench, temper anneal 621–663 °C.
  • Hardness 150 HB as cast rising to 190 HB minimum heat treated.
  • Machinability 60 — the easiest alloy on this hub.
  • Listed under ASTM B148, B505, B271, B763, B66, B806 and B30.

Typical Applications

  • Pump casings, impellers and wear rings.
  • Valve bodies, seats and trim.
  • Bearings, bushings and wear plates.
  • Resistance welding gun components and electrode holders.
  • Large hold-down screws and cast fasteners.
  • Gears, worm wheels and nuts.
  • Marine propellers and shafting components.
  • Chemical and process plant castings.