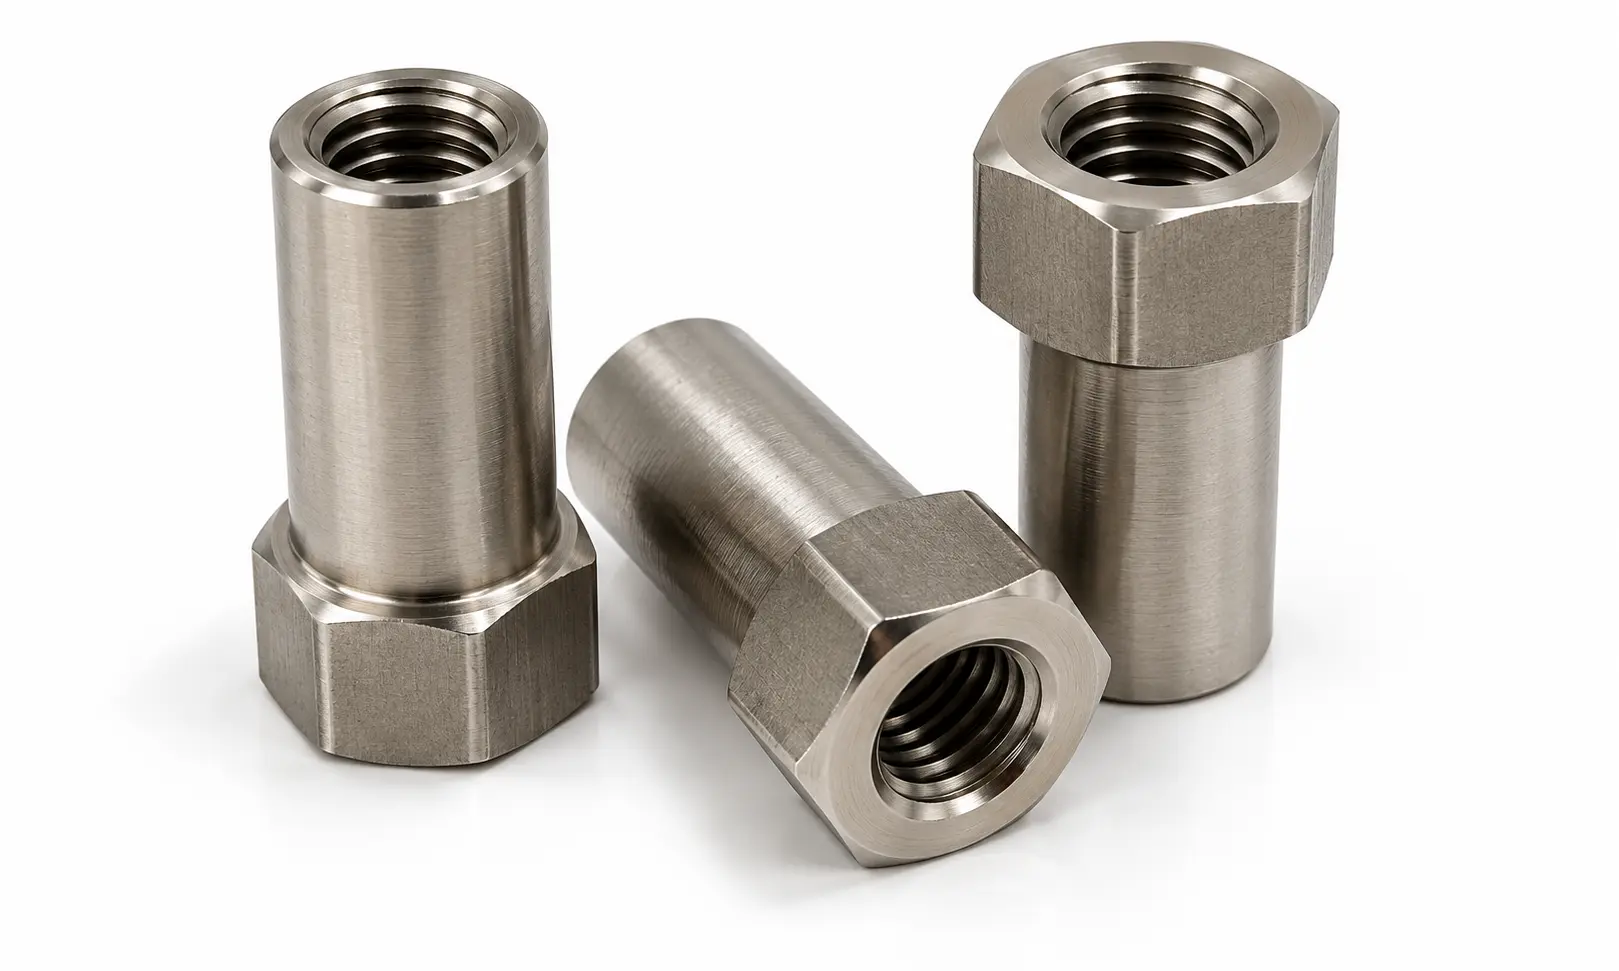
Zirconium's distinguishing feature is that it resists acids and alkalis alike. Most corrosion-resistant metals are good on one side of the pH scale: tantalum is outstanding in acid and is destroyed by caustic, while most stainless and nickel alloys struggle in reducing acid. Zirconium does both, and that is why it is specified. ATI's corrosion data show rates below 1 mpy in
hydrochloric acid at every concentration to 37% and temperatures to 225 °C; below 1 mpy in
nitric acid from 10 to 70% up to 260 °C; below 1 mpy in
sulfuric acid to 75% at ambient; and below 2 mpy in
sodium hydroxide from 5% to 50% up to about 150 °C and in potassium hydroxide to 50% at boiling. It is essentially inert to the organic acids — acetic, formic, lactic, hydroxyacetic — at all concentrations to boiling and beyond, including the acetic acid streams carrying iodide, bromide and ferric contamination that defeat most alternatives. Protection comes from a tightly adherent zirconium oxide film that forms spontaneously in air and can be deliberately thickened by a heat treatment, which improves erosion resistance in high-velocity systems and gives an excellent bearing surface.
At 1.0 to 2.0% tin the addition is a solid-solution strengthener and does not change zirconium's corrosion behaviour in any practically significant way; R60704 is treated as corrosion-equivalent to unalloyed zirconium, and the exclusions below apply unchanged. Note that ATI's published corrosion rate data cover the 702 and 705 grades, so where R60704 is being considered for a borderline duty it should be qualified against the actual process stream.
Zirconium has a short but absolute exclusion list, and the items on it are not obvious. Hydrofluoric acid attacks it at any concentration, even at room temperature (>50 mpy), and as with tantalum the real hazard is
trace fluoride rather than deliberate HF: ATI's data show 90% nitric acid, normally a duty zirconium handles at under 1 mpy, jumping to over 50 mpy with just
200 ppm of HF present.
Oxidising chloride salts are the second exclusion and the one that catches people out:
ferric chloride and cupric chloride attack zirconium at over 50 mpy at all concentrations from room temperature to boiling, which rules out the ferric-chloride-bearing streams common in etching, pickling and some leaching duties.
Aqua regia attacks it. So does
concentrated sulfuric acid above roughly 70% — the transition is sharp and temperature-sensitive, from under 1 mpy at 75% and 20 °C to over 50 mpy at 77.5% and 100 °C — and
phosphoric acid above about 55% at elevated temperature.
The wet-versus-dry chlorine behaviour is the inverse of titanium's, and the two are routinely confused. Zirconium handles
dry chlorine gas at under 5 mpy but is destroyed by
wet chlorine — chlorine gas with more than 0.13% water, or chlorine-saturated water — at over 50 mpy. Titanium is exactly the opposite: it needs moisture to maintain its oxide and reacts violently with dry chlorine. Substituting one for the other in a chlorine service on the assumption that both are “corrosion-resistant reactive metals” is a serious error.
Zirconium is susceptible to stress-corrosion cracking in a specific and well-documented set of environments, and a tightened fastener supplies exactly the sustained tensile stress that SCC requires. The environments to watch are
ferric and cupric chloride solutions, which both corrode and crack it;
concentrated nitric acid above about 70%, where ATI's own data note SCC observed even though the general corrosion rate stays below 1 mpy — a dangerous combination, because the metal looks untouched right up until it cracks;
methanol-halide mixtures; and
hydrochloric acid carrying ferric chloride, where 100 ppm of FeCl₃ in 10% HCl produced SCC at a general rate still under 1 mpy. The practical implications are that a corrosion-rate chart alone is not sufficient to qualify zirconium for a duty, that residual stress from forming and welding should be removed by a stress-relief anneal, and that oxidising-chloride contamination must be assessed even when it is present only in traces.
Hydrogen embrittlement is zirconium's other failure mode. Zirconium absorbs hydrogen readily and precipitates it as brittle zirconium hydride platelets, which cut ductility and can cause delayed cracking. As with tantalum, the metal does not have to be corroding to pick hydrogen up — it only needs to be
cathodic. Couple zirconium electrically to a less noble metal in an acidic electrolyte, or apply cathodic polarisation, and atomic hydrogen is evolved on its surface and diffuses in. A zirconium bolt clamping a carbon steel or stainless flange in acid service is precisely that configuration. The mitigations are the same three:
electrical isolation with non-conducting gaskets, sleeves and washers;
anodic protection; or an
oxidising addition to the stream to depolarise the cathode reaction. A thickened oxide film produced by heat treatment also slows hydrogen ingress. Hydrogen is held to 0.005% maximum in the as-supplied material by ASTM B551 precisely because the starting level matters.
Zirconium galls, and it is galvanically noble. Like titanium, zirconium has a thin oxide over an adhesive metal, so a zirconium thread run against another zirconium thread will cold-weld and seize, often badly enough that the fastener must be cut off. Every zirconium bolted joint needs one of three mitigations: an anti-seize compound or dry-film lubricant such as molybdenum disulphide; a thickened oxide film produced by heat treatment, which ATI note serves as an excellent bearing surface and is the approach specific to this metal; or a nut in a dissimilar material. Separately, zirconium sits well above carbon steel, aluminium and zinc on the galvanic series, so a zirconium fastener will not itself corrode in a less noble assembly but will drive corrosion of the structure around it — and, as above, will take up hydrogen while doing so. Insulating washers and sleeves address both problems at once.
Zirconium fines are pyrophoric, and this is a genuine machine-shop hazard rather than a formality. Fine turnings, grinding dust and powder ignite readily in air — sometimes spontaneously — and burn at very high temperature. A zirconium fire
must not be fought with water, which decomposes and feeds it hydrogen and oxygen, nor with carbon dioxide or halogenated agents; only a Class D agent such as dry powdered graphite, sodium chloride or limestone is appropriate. Machining is therefore done with heavy flood coolant that keeps chips wet and cool, swarf is collected wet, kept submerged or damp, and stored in covered containers away from the shop, and grinding is kept wet throughout. Exotic Alloy handles all zirconium machining and grinding under these controls. The bulk metal in a finished fastener presents no fire risk whatever — the hazard is entirely in the fines generated making it.
A note on hafnium, because it causes confusion. Hafnium occurs with zirconium in nature and is chemically almost inseparable from it, so the commercial grades on this hub simply permit it: ASTM B551 allows
up to 4.5% hafnium in all five grades, and the zirconium content is specified as a combined “zirconium + hafnium” minimum rather than as zirconium alone. ATI state plainly that the presence of hafnium at these levels does not significantly influence the physical, mechanical or corrosion properties, so for every chemical-process and fastener application it is simply irrelevant.
It matters in exactly one place: nuclear service. Hafnium has a thermal neutron absorption cross-section around 600 times that of zirconium, so reactor-grade zirconium has the hafnium painstakingly removed to the order of 0.010% and is bought under an entirely separate set of nuclear specifications and UNS numbers.
None of the five grades here is a nuclear grade, and none should be offered for reactor core duty.
Which grades exist in which product form is not uniform, and it governs what can actually be made. ASTM B551 covers five grades of strip, sheet and plate — R60700, R60702, R60704, R60705 and R60706.
ASTM B550, the bar and wire specification, covers only three: R60702, R60704 and R60705.
R60700 and
R60706 are flat-product grades and are not covered by the bar and wire standard, which is the practical constraint on making conventional turned or headed fasteners in them — parts in those two grades are normally produced from plate, or supplied to B550 chemistry and property requirements by specific agreement between purchaser and manufacturer. Separately, only
R60702 and R60705 carry ASME Boiler and Pressure Vessel Code allowable stresses (Section II Part D, under SB-493, SB-523, SB-550, SB-551 and SB-658); R60700, R60704 and R60706 are not ASME code-listed materials and must not be specified for code pressure-retaining duty. Tell us the service and we will confirm form availability before you commit a drawing to a grade.
How these five grades divide. They separate on two axes — alloy addition and oxygen content — and ASTM B551's bend test radius is the clearest single indicator of where each one sits.
R60702 is unalloyed zirconium and the workhorse: 380 MPa tensile minimum, ASME code-listed in every product form, and the default for chemical process duty.
R60700 is the same metal with oxygen cut to 0.10% and is the odd one out in the standard — it is the only grade specified by
maximum strength rather than minimum, capped at 380 MPa tensile and 305 MPa yield, with the highest minimum elongation at 20%. You buy it to guarantee softness and formability, not strength.
R60704 adds 1.0–2.0% tin with a raised iron-plus-chromium range for a modest strength gain to 415 MPa.
R60705 adds 2.0–3.0% niobium and is much the strongest at 550 MPa tensile and 380 MPa yield, while also bending tighter than the unalloyed grades at 3T — the niobium improves strength and formability together.
R60706 is chemically the same Zr-2.5Nb alloy as R60705 with oxygen reduced from 0.18% to 0.16%, trading specified strength down to 510/345 MPa in exchange for the tightest bend radius in the standard at 2.5T.