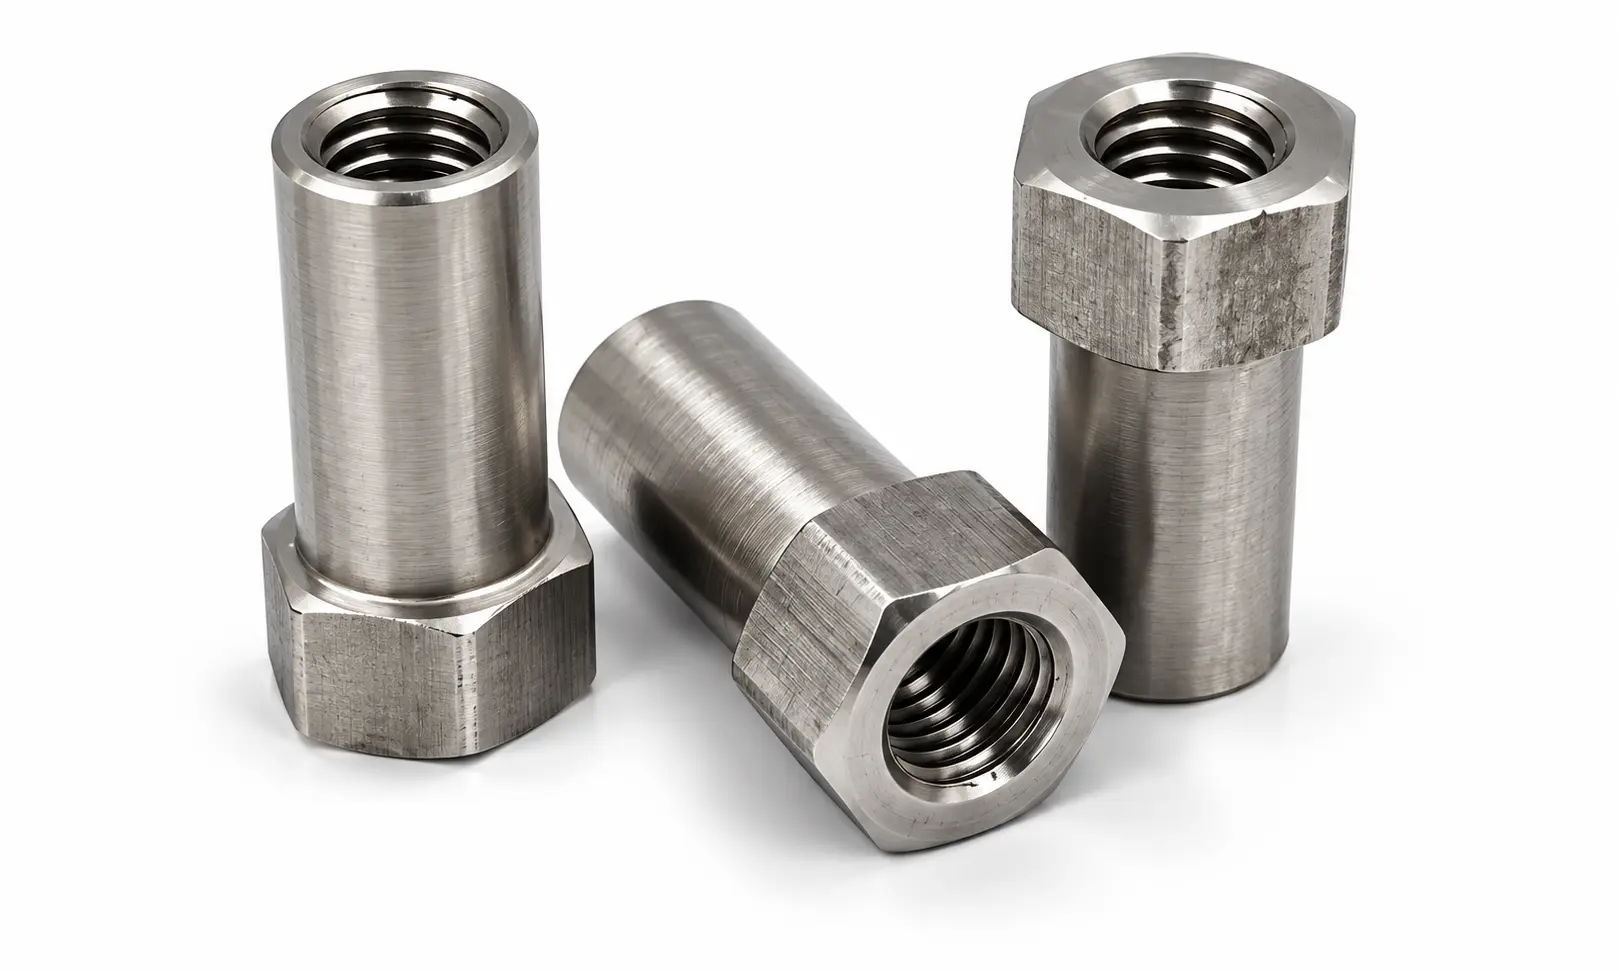
Ta-10W has excellent corrosion resistance in many media, and in general acid service it behaves broadly as tantalum does — but it is important to be clear that this is not the grade normally bought for chemical duty. At 10% tungsten the alloy is a structural and elevated-temperature material; where the requirement is pure corrosion performance in process plant, unalloyed
R05200 or
Ta-2.5W is specified, and where cost per unit volume governs,
Ta-40Nb.
Tantalum is the most corrosion-resistant metal in commercial use, and that single property is the reason anyone pays for it. A dense, self-healing, tightly adherent Ta₂O₅ film makes it effectively inert to almost every mineral and organic acid at the concentrations and temperatures found in industrial process plant — its behaviour is routinely compared to glass rather than to other metals. It resists hydrochloric acid at all concentrations and well above the boiling point, sulfuric acid to high concentration and temperature, nitric acid, phosphoric, hydrobromic, chromic, perchloric, and the organics including formic and acetic acid. It resists wet chlorine, bromine and iodine, aqua regia, ferric and cupric chloride, and most salt solutions. These are duties in which every stainless steel, most nickel alloys and in many cases zirconium and titanium all fail; tantalum is specified precisely where the process has already defeated those cheaper options.
Four absolute exclusions apply to every grade on this page, and no alloying addition changes them. First,
hydrofluoric acid at any concentration or temperature attacks tantalum rapidly, and a nitric-plus-hydrofluoric mixture will dissolve it completely — HF is in fact the standard reagent for machining and pickling tantalum. Second,
any fluoride-bearing acidic solution behaves the same way, which matters because fluoride is a frequent trace contaminant rather than a deliberate ingredient; a process stream that is nominally pure sulfuric acid but carries fluoride will destroy a tantalum component. Third,
free sulfur trioxide — oleum and hot fuming sulfuric acid — attacks it, and plain concentrated sulfuric acid becomes aggressive above roughly 175–200 °C, where corrosion rate rises sharply and hydrogen pickup begins. Fourth,
strong alkalis attack tantalum even at room temperature, and molten sodium or potassium hydroxide attacks it rapidly; tantalum is an acid-service metal and must not be used on the alkaline side. Alkaline peroxide and fused alkaline salts are likewise excluded.
Hydrogen embrittlement is the single most important practical fact about tantalum in service, and it is what actually fails tantalum equipment — not wall loss. Tantalum absorbs atomic hydrogen readily and becomes brittle as it does so; embrittlement is significant by the time hydrogen reaches roughly 100 ppm, and the damage is permanent. The danger is that tantalum does not need to be corroding to pick hydrogen up. It only needs to be
cathodic. Couple tantalum electrically to a less noble metal — carbon or stainless steel, a steel flange, a graphite gasket, a steel bolt — in an acidic electrolyte and the tantalum becomes the cathode of a galvanic cell, atomic hydrogen is evolved on its surface, and it diffuses straight into the metal. The same thing happens under any applied cathodic polarisation. The component then cracks or blisters with no measurable thinning and no warning.
For a tantalum fastener this is a design rule, not a footnote. A tantalum bolt clamping a less noble flange in acid service is exactly the configuration that embrittles, and the bolt is the part you cannot afford to lose. Three mitigations are used, and at least one is mandatory:
electrical isolation — non-conducting gaskets, sleeves and washers so no galvanic circuit exists, which is why tantalum-lined vessels are built with insulating joints;
anodic protection by impressed current, holding the tantalum anodic so no hydrogen is evolved on it; or
an oxidising addition to the process stream — nitric acid, ferric or cupric ions — which depolarises the cathode reaction. Graphite is a particular trap: it is noble, conductive and common as a gasket material, and a graphite gasket wetted by acid against a tantalum face is a working galvanic cell. Tell Exotic Alloy the mating material and the electrolyte and we will advise on the isolation detail.
Tantalum cannot be used hot in air, and this is a separate limit from hydrogen embrittlement. Above roughly 260–300 °C tantalum oxidises rapidly in air or any oxidising atmosphere, and the oxide that forms is not protective — it grows, spalls and consumes the section. Over the same range the metal also absorbs oxygen, nitrogen and hydrogen directly from the atmosphere, all of which embrittle it. The consequence is that tantalum’s very high melting point is only usable under
vacuum or an inert atmosphere: as a furnace element, heat shield, crucible or liner it performs superbly to well over 2000 °C, and in open air it is finished at 260 °C. Where oxidising service above that temperature is unavoidable the alloy must be coated — silicide and tin-aluminium coating systems are used on
Ta-10W for rocket nozzle work — and coating life, not alloy strength, then governs the design.
Coatings for oxidising high-temperature service. Because the 260 °C air limit would otherwise make the alloy’s hot strength unusable outside vacuum, Ta-10W is the tantalum grade for which protective coating systems have actually been developed and characterised. Silicide coatings, silicon-aluminium and silicon-manganese modifications, and 50 tin-50 aluminium systems have all been cyclic-life tested on this alloy; the tin-aluminium system gives by far the longest life, exceeding 425 hours at 1800 °F and 225 hours at 2500 °F, where the plain silicide systems manage a few hours at the same temperatures. Coating life, and the behaviour of a defected coating, then governs component life rather than the alloy itself — defected silicide coatings survive under five hours at 2700 °F.
Tantalum is expensive, and specifying it well means using as little as possible. It is a conflict-mineral-regulated, supply-constrained metal carried at a price well above nickel alloys and titanium, and process plant reflects that: vessels and columns are built as steel pressure shells with a loose tantalum liner or an explosion-bonded tantalum clad layer, not in solid tantalum, and tantalum is also the standard patch material for repairing glass-lined equipment. Solid tantalum is reserved for the parts that cannot be clad — bayonet heaters, thermowells, spargers, rupture discs, small-bore piping, and the fasteners, which is where Exotic Alloy comes in. A tantalum fastener is specified because the alternatives have already been tried and dissolved, so it is worth getting the isolation and the certification right rather than economising on them.
How these five grades divide. The two unalloyed grades are chemically almost identical and are chosen on
production route:
R05200 is electron-beam or vacuum-arc melted with oxygen held to 0.015%, while
R05400 is consolidated by powder metallurgy and allowed double the oxygen at 0.030%. They carry the same ASTM mechanical minimums, so R05200 is specified where the lower interstitial ceiling or the melted structure matters and R05400 where availability and cost govern.
R05252 (Ta-2.5W) adds a modest tungsten solid-solution addition that raises specified tensile strength from 207 to 276 MPa while leaving corrosion resistance and formability essentially intact — it is the usual upgrade when unalloyed tantalum is corrosion-adequate but not strong enough.
R05255 (Ta-10W) more than doubles that again to 482 MPa specified and 550–655 MPa typical, and holds useful strength to beyond 2000 °C in vacuum; it is the structural and aerospace grade, bought for strength rather than for chemical duty.
R05240 (Ta-40Nb) goes the other way: diluting with 40% niobium cuts density by roughly a quarter and cuts cost substantially while keeping much of tantalum’s acid resistance, which makes it the economic choice for bulk acid service where the very last increment of corrosion performance is not required.