+91 97734 41022 sales@exoticalloy.com
Material Specification

Nickel Silver C75700

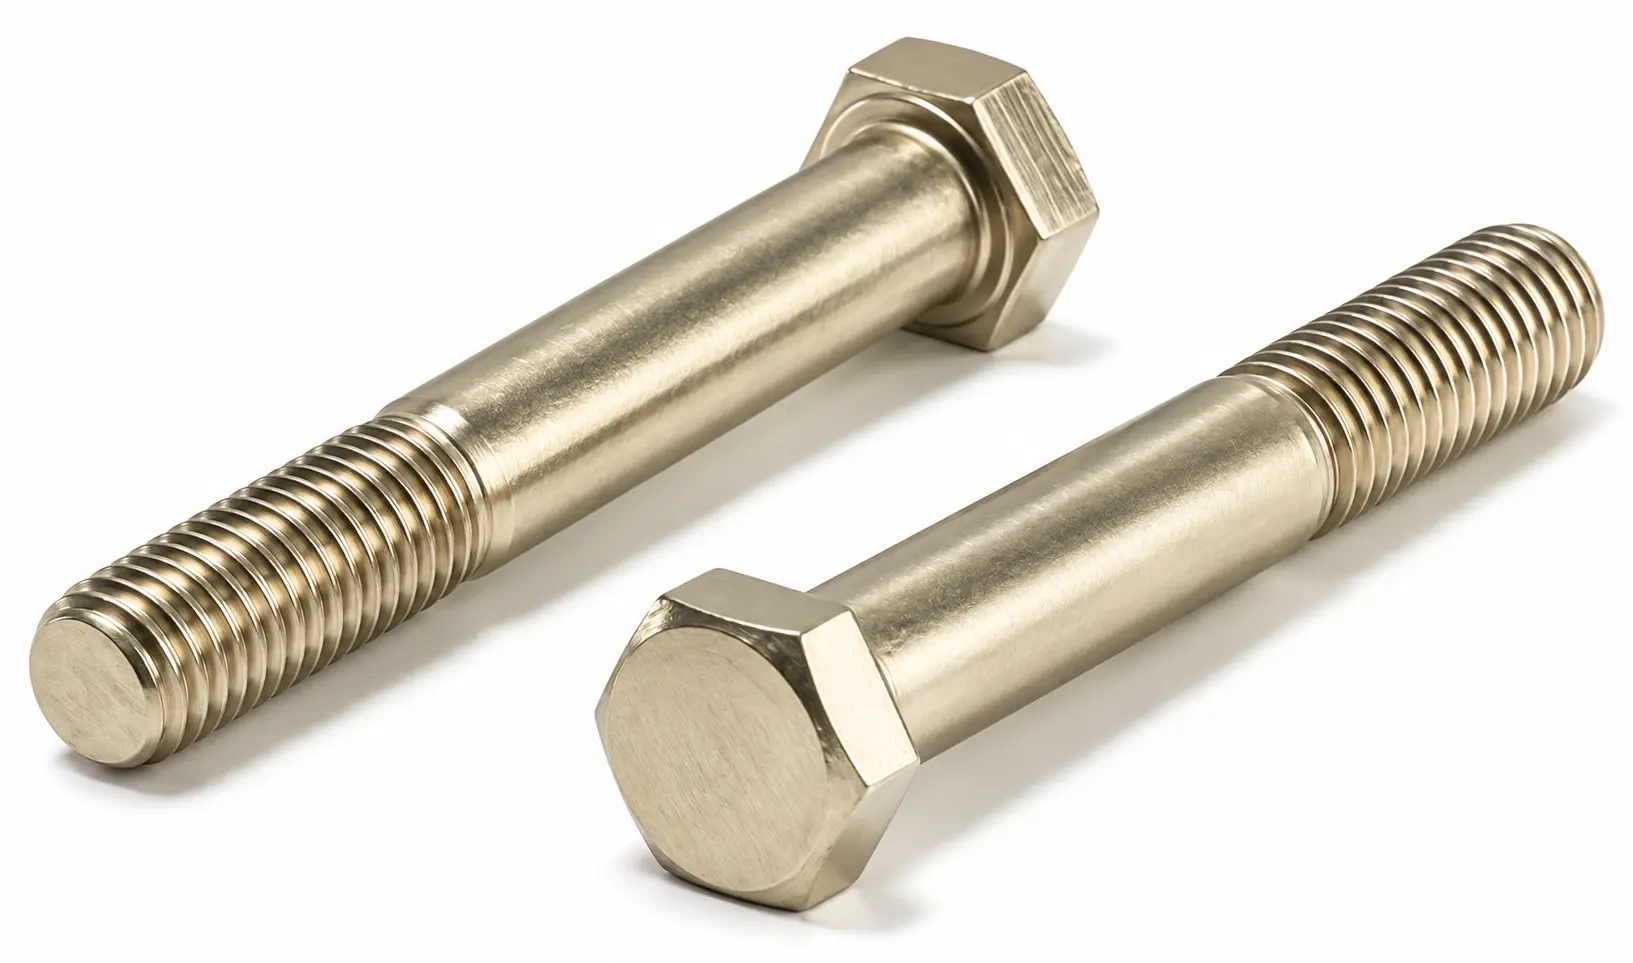
Nickel Silver C75700 Fasteners
65-12 Nickel Silver — Economical Mid-Nickel Grade

Nickel Silver C75700 Fasteners

Nickel Silver C75700 is the 65-12 grade — copper 63.5–66.5% with nickel at 11.0–13.0% and the balance zinc. It is one step up from C74500's 10% nickel, giving a slightly whiter colour for a small cost increase, and it is widely used where appearance matters but a full 18% nickel cannot be justified.

Properties are characteristic of the 65-series: 359 MPa annealed rising to 641 MPa at extra hard, with excellent cold formability through the whole range and the family's usual Excellent soldering and brazing. Lead is held to 0.05%. As with every nickel silver, hot forming is rated Poor — these alloys are hot-short and must be worked cold. Exotic Alloy supplies C75700 strip, wire and formed components.

Request a Quote
Product Range

Nickel Silver C75700 Fasteners Available

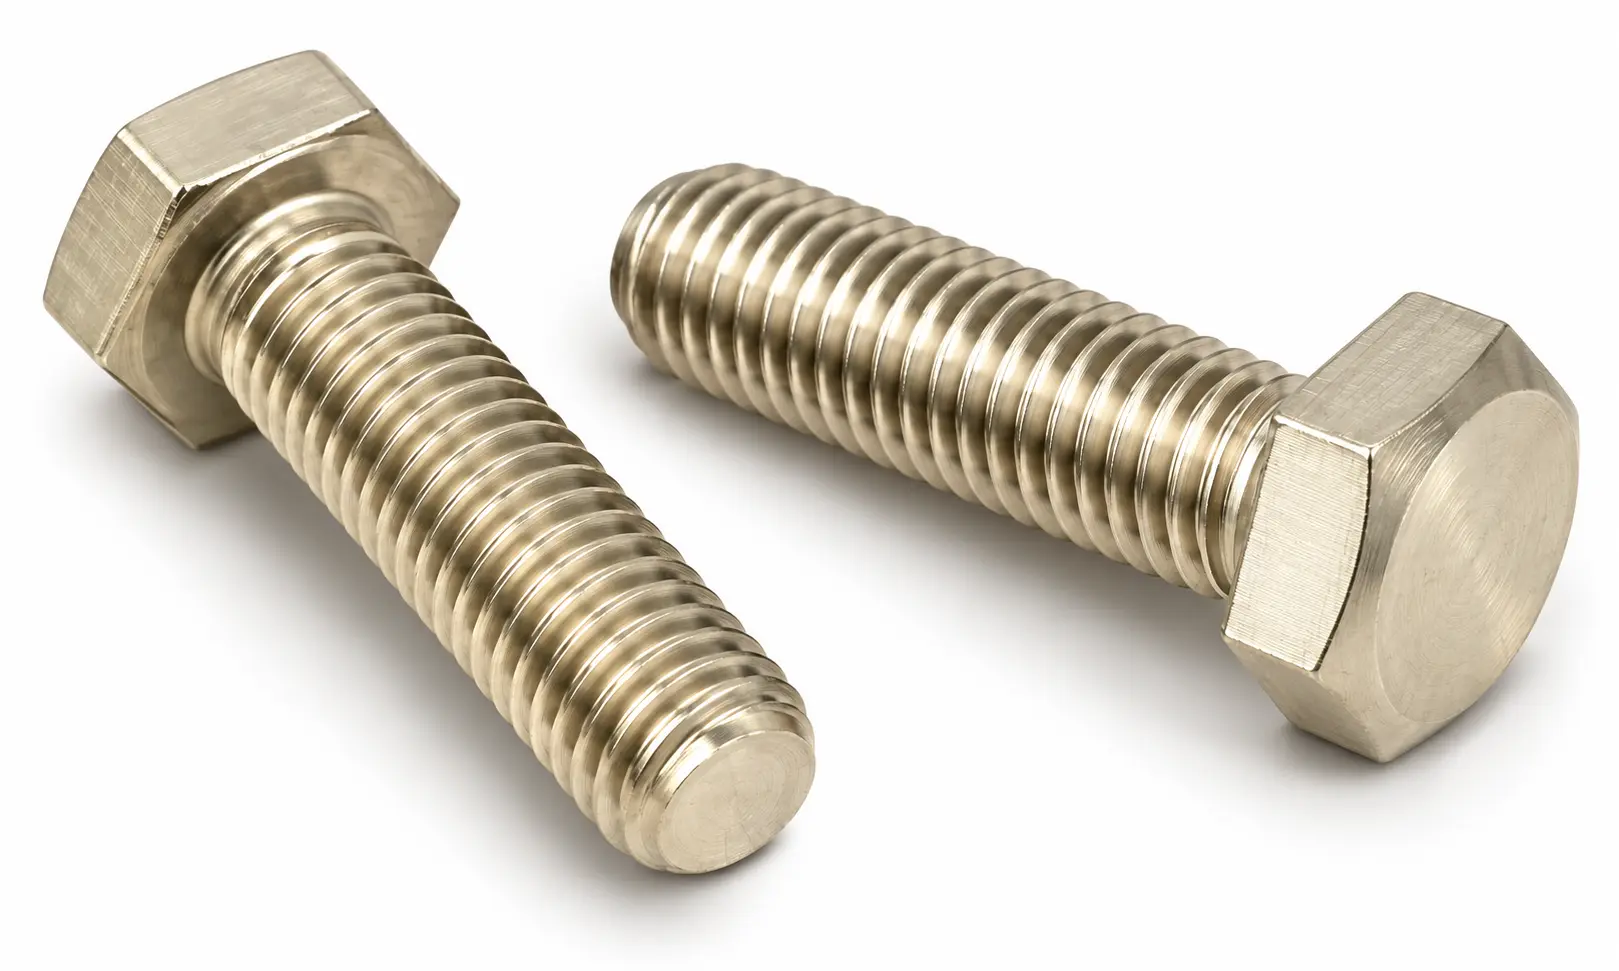
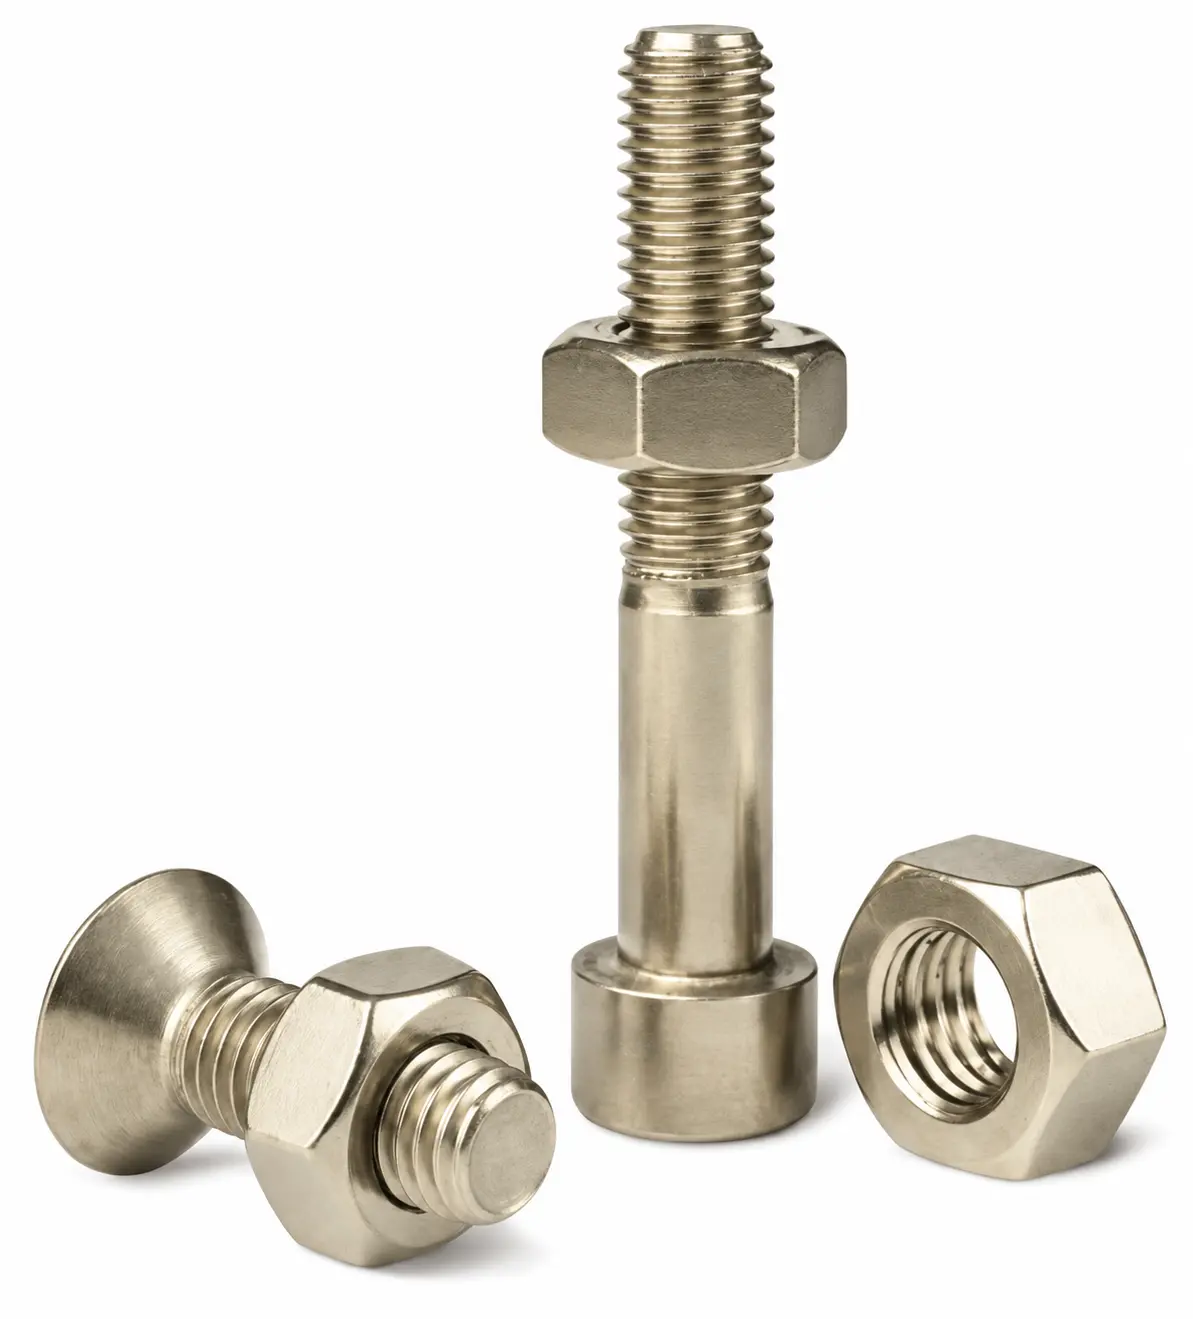
Nickel Silver C75700 Hex Bolts
Nickel Silver C75700
Hex Bolts
Nickel Silver C75700 Heavy Hex Bolts
Nickel Silver C75700
Heavy Hex Bolts
Nickel Silver C75700 Stud Bolts
Nickel Silver C75700
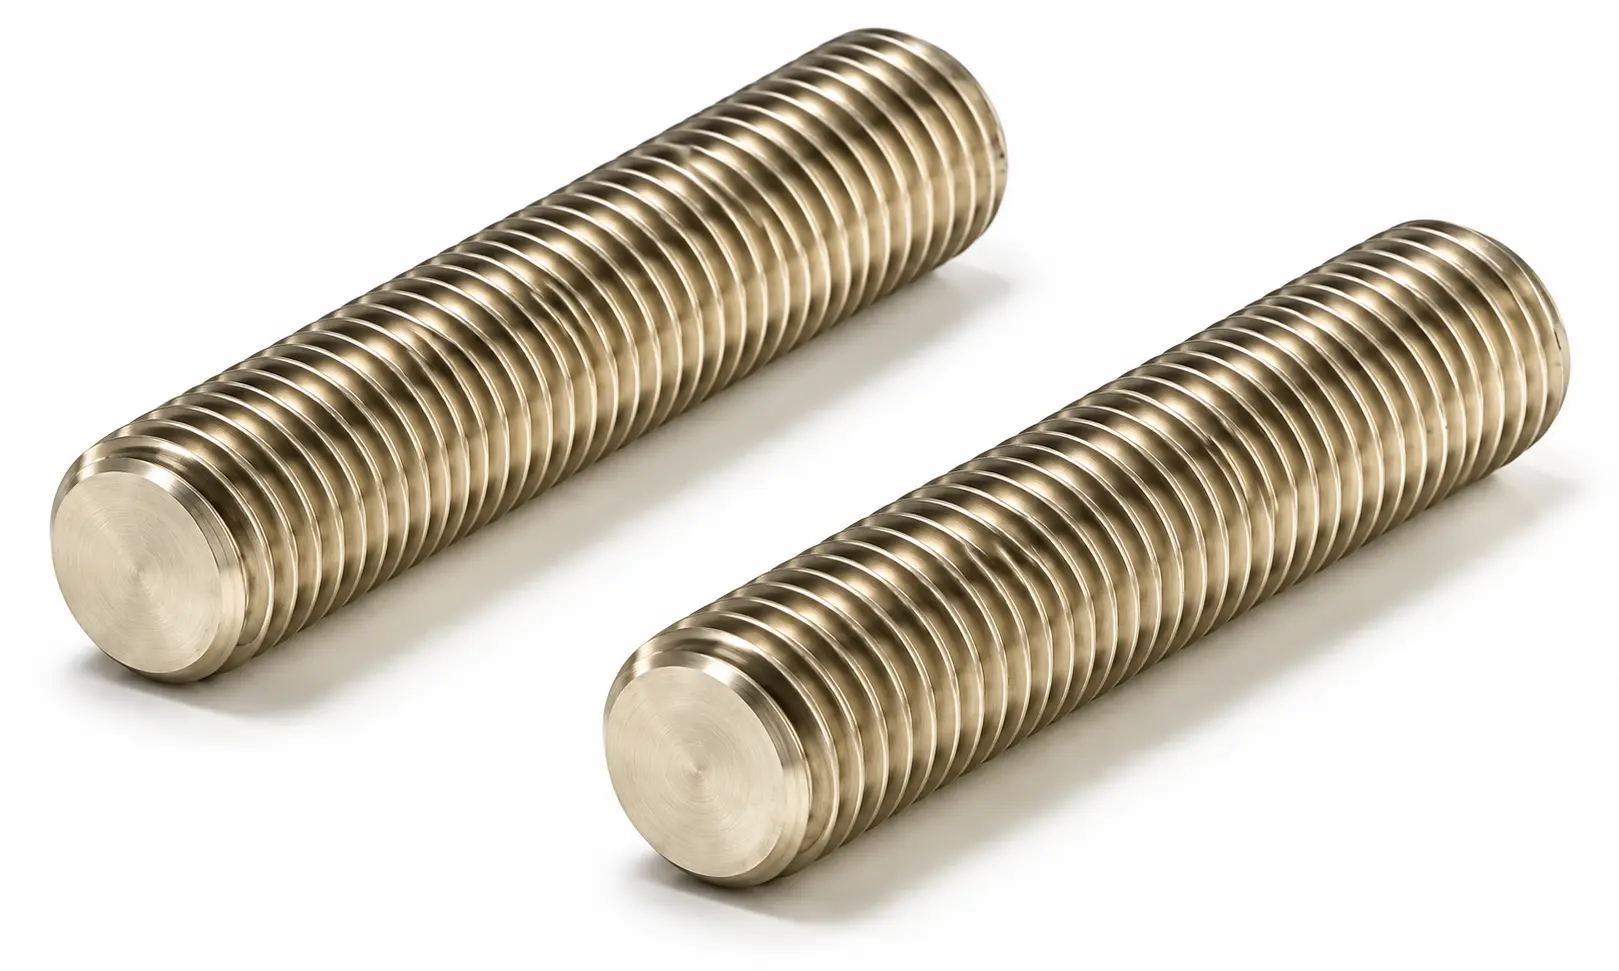
Stud Bolts
Nickel Silver C75700 Threaded Rods
Nickel Silver C75700
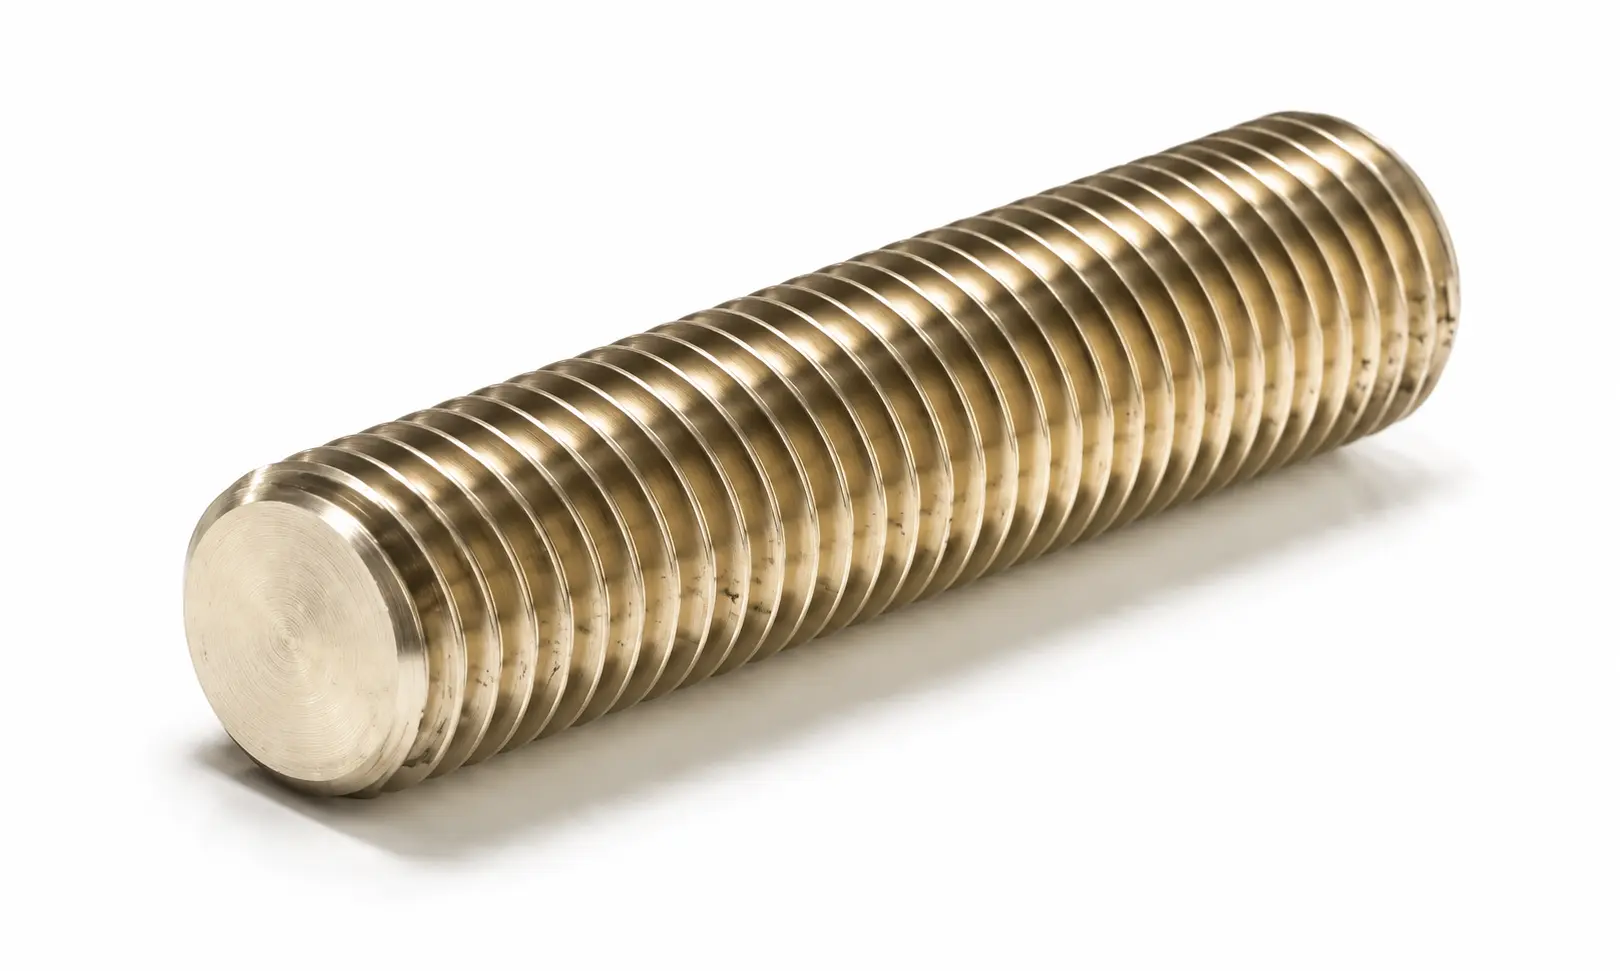
Threaded Rods
Nickel Silver C75700 Anchor Bolts
Nickel Silver C75700
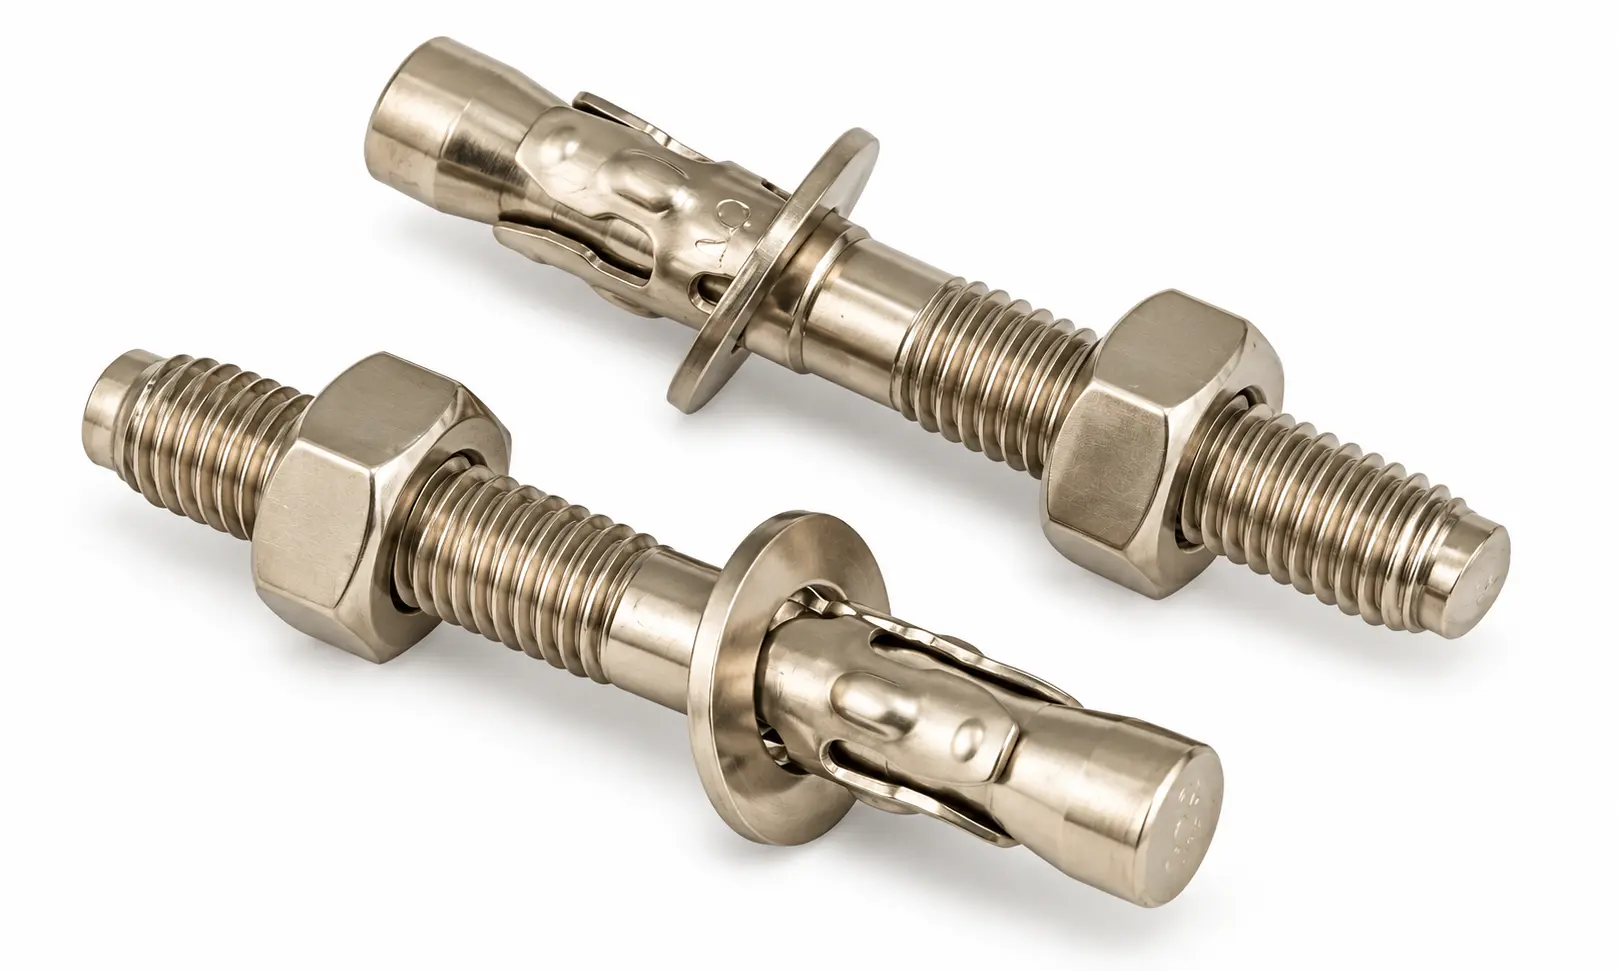
Anchor Bolts
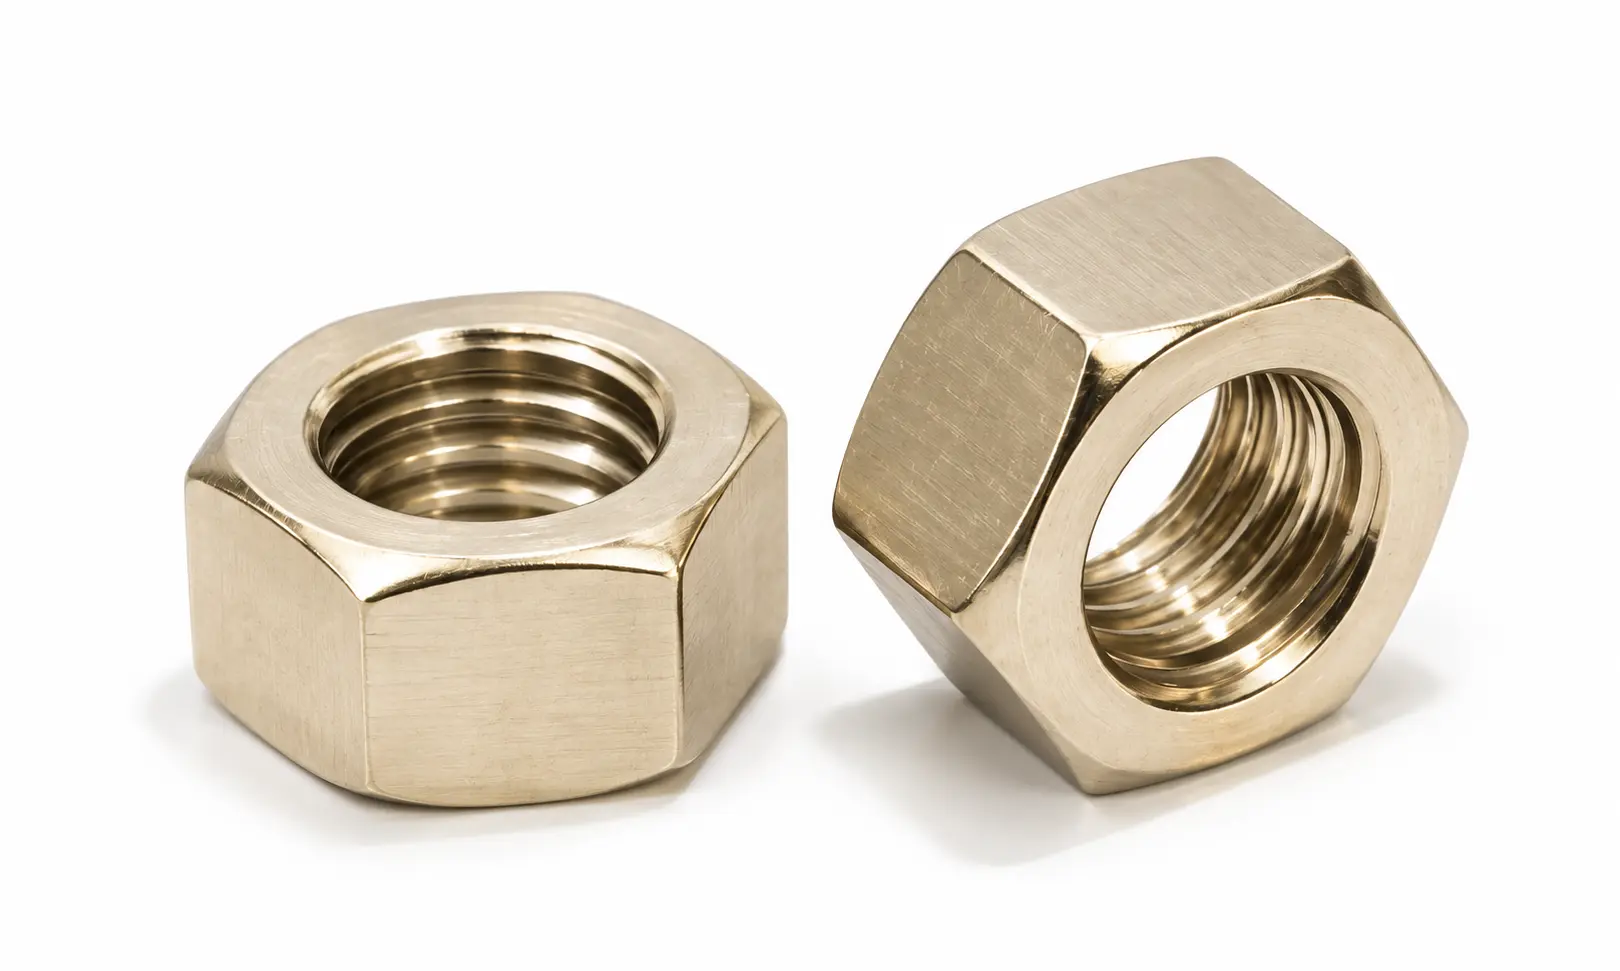
Nickel Silver C75700 Hex Nuts
Nickel Silver C75700
Hex Nuts
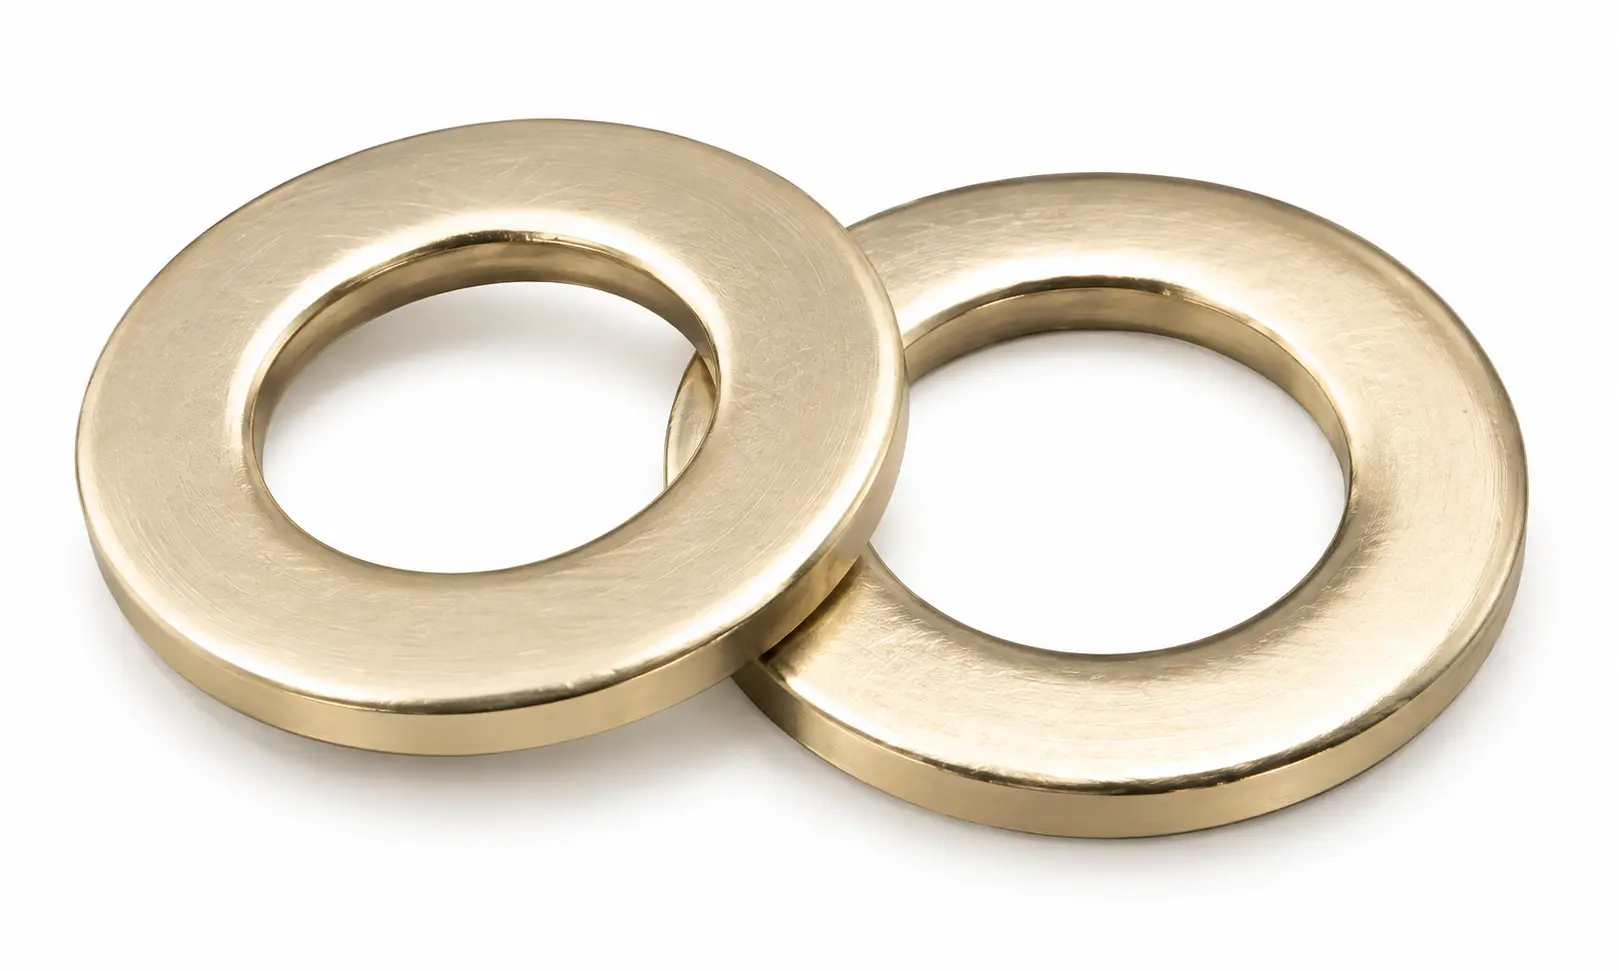
Nickel Silver C75700 Washers
Nickel Silver C75700
Washers
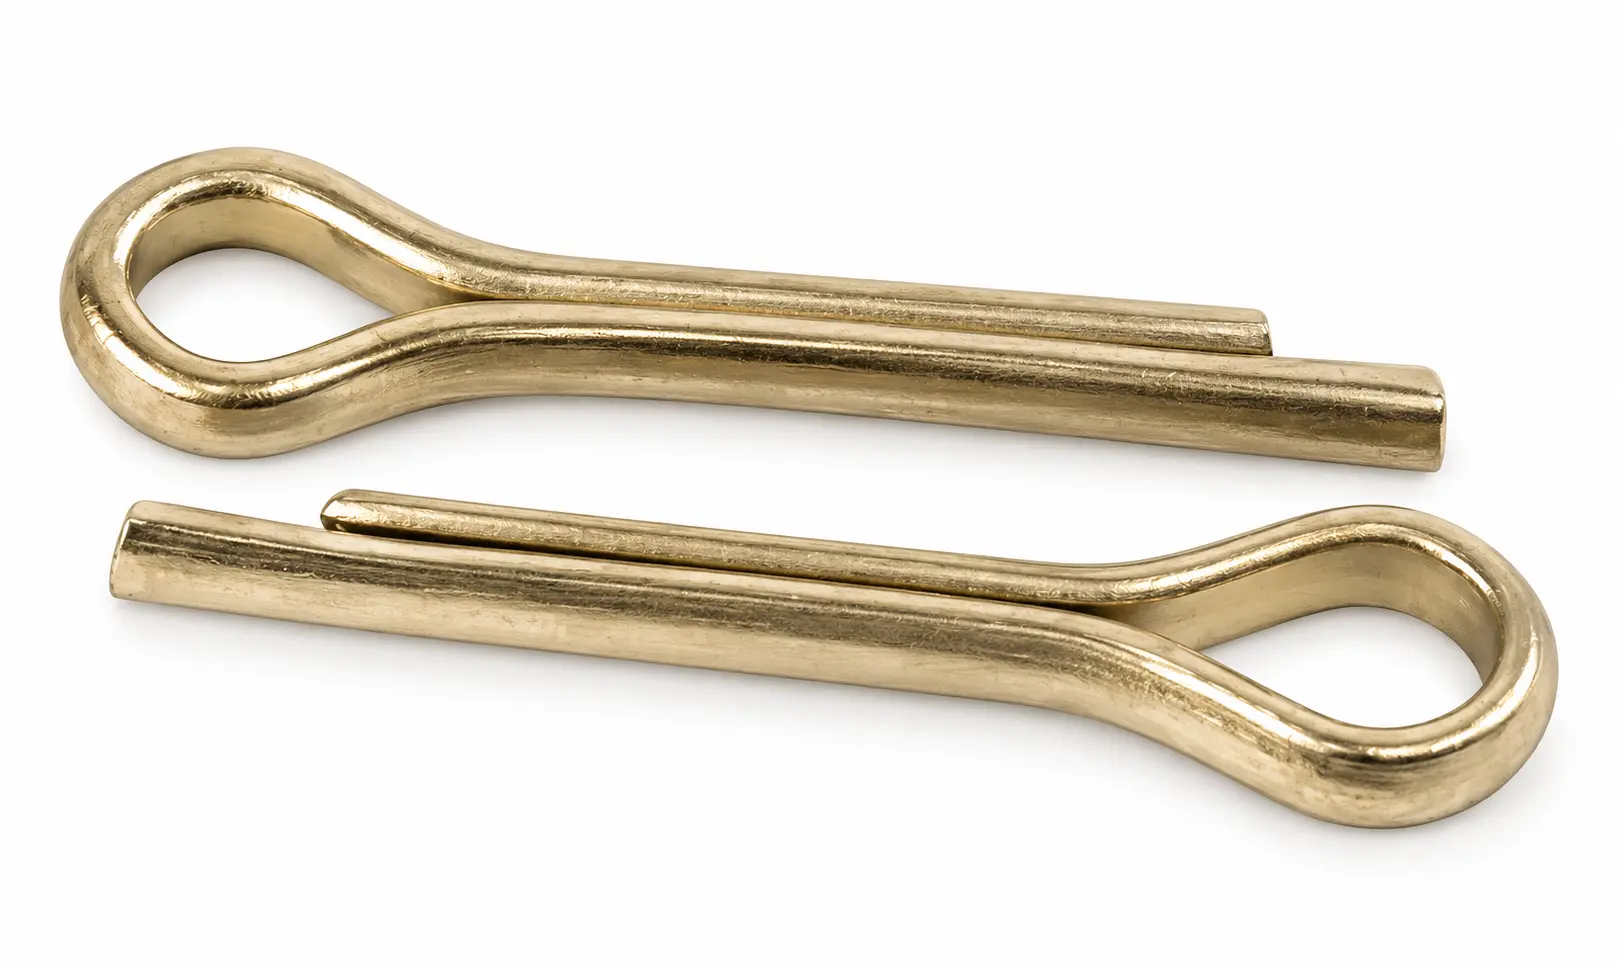
Nickel Silver C75700 Cotter Pins
Nickel Silver C75700
Cotter Pins
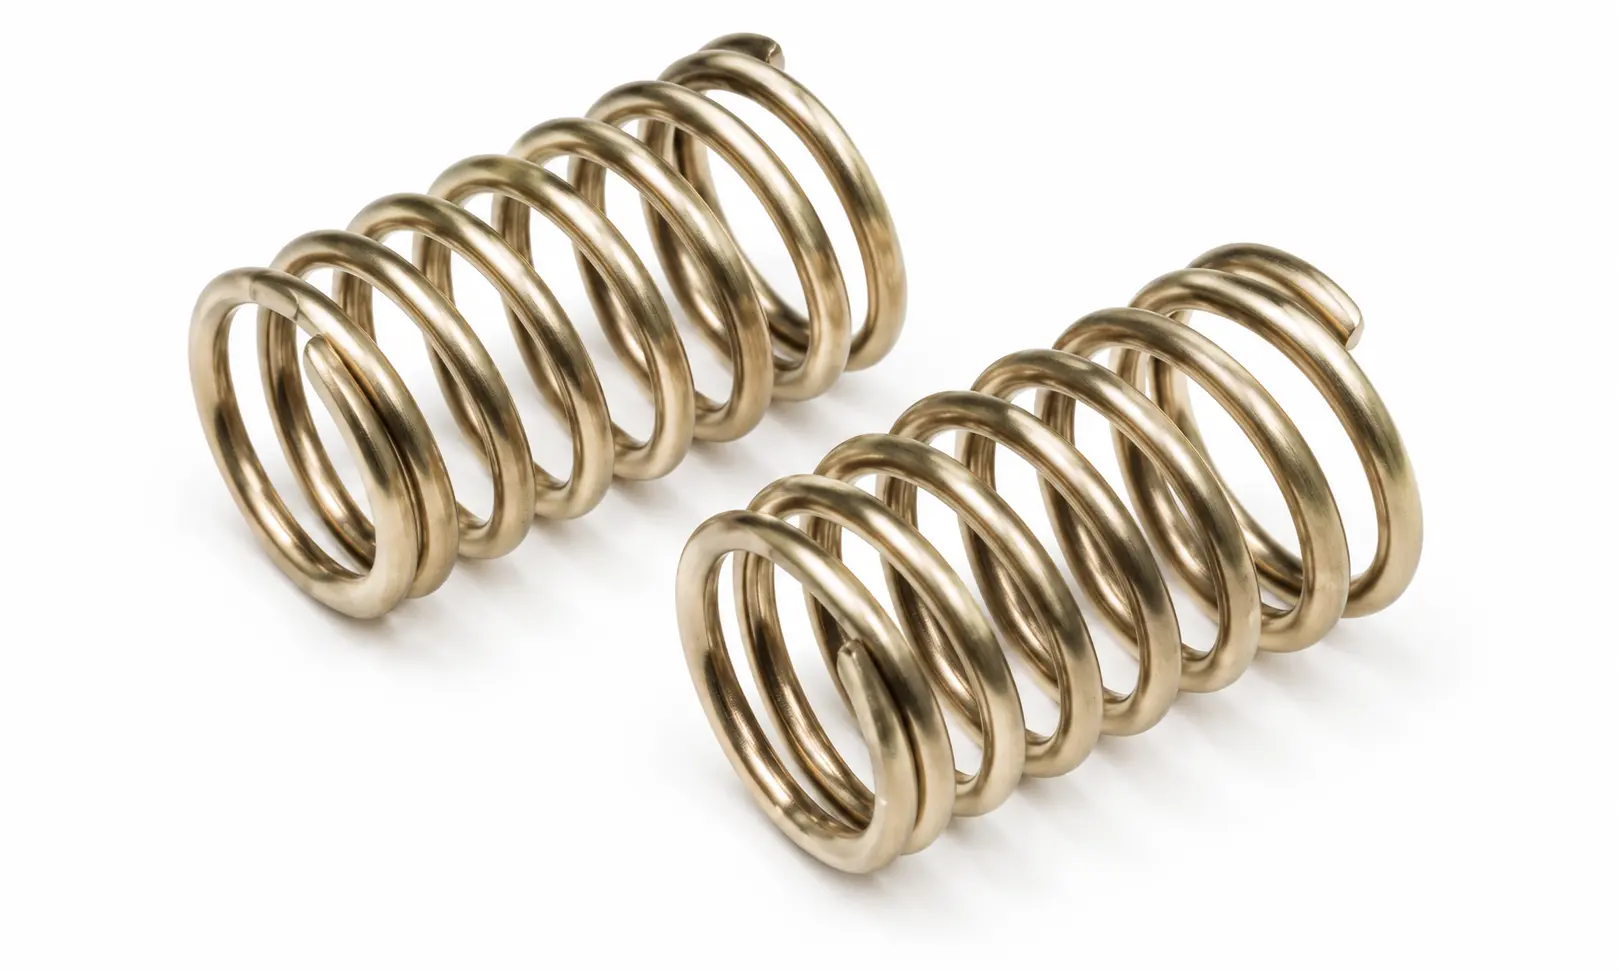
Nickel Silver C75700 Springs
Nickel Silver C75700
Springs
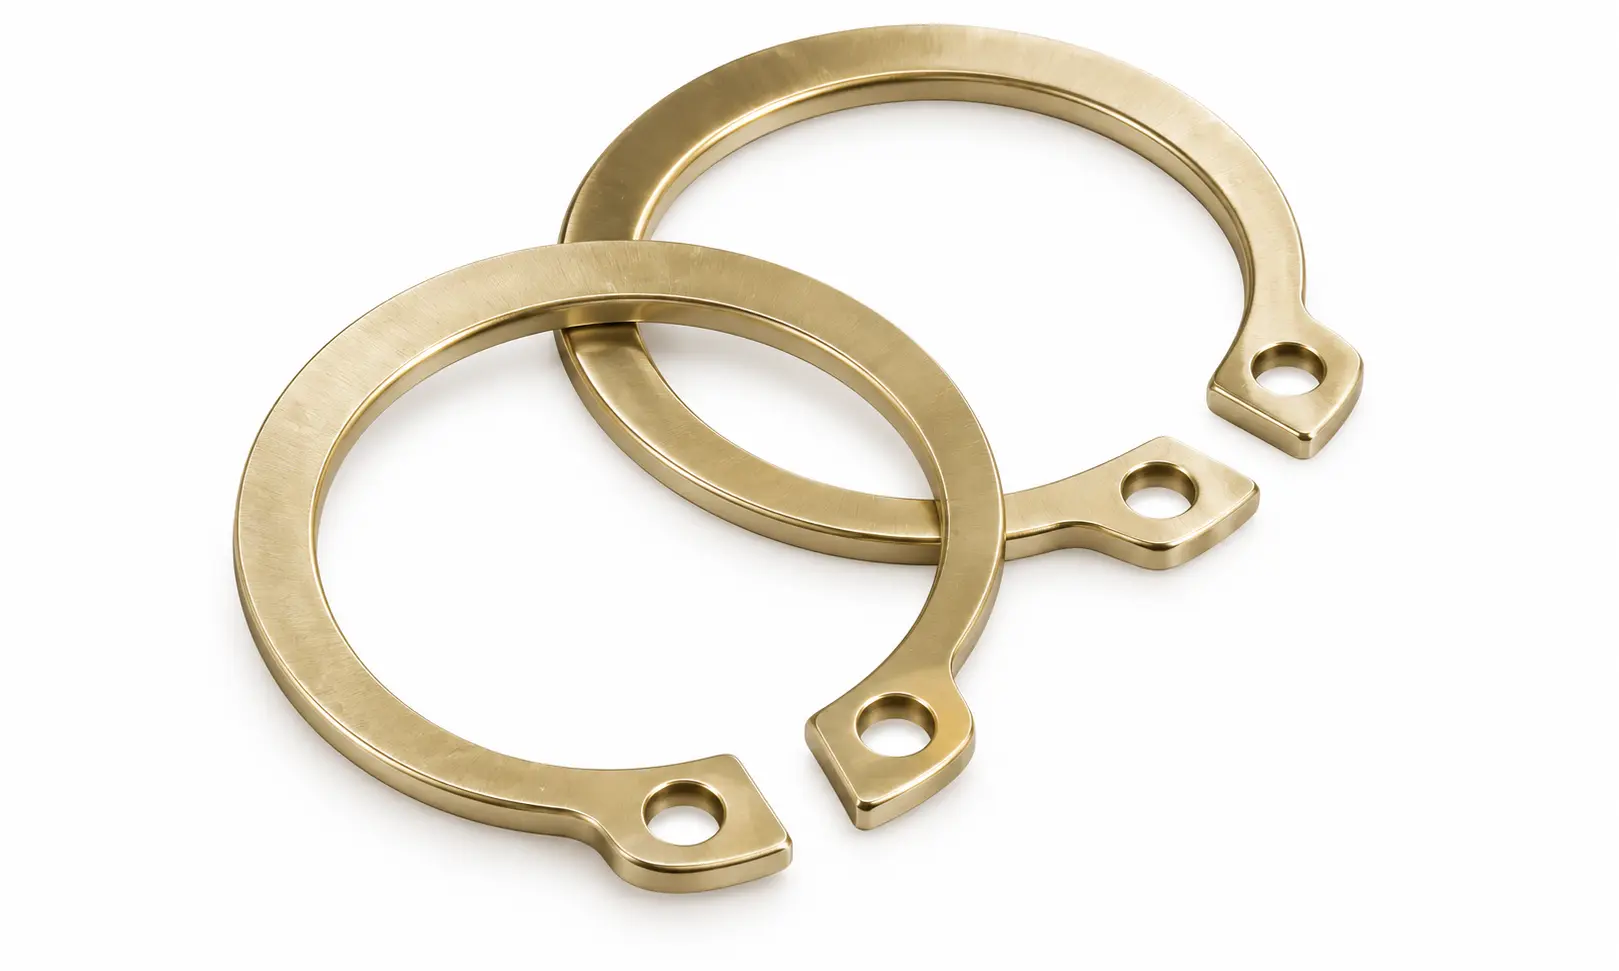
Nickel Silver C75700 Circlips
Nickel Silver C75700
Circlips
Nickel Silver C75700 Coated Fasteners
Nickel Silver C75700
Coated Fasteners
Nickel Silver C75700 Custom Spacers
Nickel Silver C75700
Custom Spacers
Technical Data

Nickel Silver C75700 Specifications

Chemical Composition — Nickel Silver C75700 (wt. %)
ElementMinimum %Maximum %
Copper (Cu), including silver63.566.5
Nickel (Ni), including cobalt11.013.0
Zinc (Zn)Remainder—
Lead (Pb)—0.05
Iron (Fe)—0.25
Manganese (Mn)—0.50
Copper + sum of named elements99.5—
Mechanical Properties — Nickel Silver C75700
ConditionUTS (MPa)YS 0.5% EUL (MPa)Elongation (%)Hardness
Flat, 0.070 mm grain OS0703591244869 HRF
Flat, 0.050 mm grain OS0503721314573 HRF
Flat, 0.035 mm grain OS0353861454278 HRF
Flat, 0.025 mm grain OS0254071653882 HRF
Flat, 0.015 mm grain OS0154211933588 HRF
Flat, 1/8 hard H004142413260 HRB
Flat, 1/4 hard H014483102370 HRB
Flat, 1/2 hard H025034141180 HRB
Flat, hard H04586517489 HRB
Flat, extra hard H06641545292 HRB
Physical Properties
Density8.69 g/cm³
Melting Point1038 °C (1900 °F) liquidus
Electrical Conductivity8% IACS at 20 °C
Thermal Conductivity40 W/m·K at 20 °C
Coefficient of Thermal Expansion16.2 × 10⁻⁶ /°C
Specific Heat Capacity377 J/kg·K at 20 °C
Modulus of Elasticity124 GPa
Modulus of Rigidity47 GPa
Machinability Rating20 (C36000 = 100)
Capacity for Cold WorkingExcellent
Capacity for Hot FormingPoor — cold-worked alloy
Hardenable by Heat TreatmentNo — strength from cold work only
Magnetic ResponseNon-magnetic
Equivalent Grades & Standards
UNSEN / CEN DesignationNominal CompositionCommon Name
C75700 — Cu-65Ni12Zn23 Nickel Silver 65-12, CDA 757

Key Specifications: ASTM B122/B122M (Copper-Nickel-Zinc Alloy [Nickel Silver] and Copper-Nickel Plate, Sheet, Strip & Rolled Bar) / ASTM B151/B151M (Copper-Nickel-Zinc Alloy [Nickel Silver] and Copper-Nickel Rod & Bar) / ASTM B206 (Copper-Nickel-Zinc Alloy Wire) / SAE J461 and J463 (Wrought and Cast Copper Alloys).

Note on fastener standards: No nickel silver is covered by the ASTM nonferrous fastener standards. ASTM F468 and F467 carry a long list of copper materials — C11000, C26000, C27000, C46200, C46400, C51000, C61300, C61400, C63000, C64200, C65100, C65500, C66100, C67500, C71000 and C71500 — but none of the C73xxx to C79xxx nickel silvers appears among them. Fasteners and fixings in these alloys are manufactured from material certified to ASTM B122, B151 or B206 as applicable, with thread conformance to the relevant ASME or ISO standard and acceptance criteria agreed on the order.

In practice nickel silvers are rarely specified as structural fasteners in any case. They are chosen for appearance, spring properties, tarnish resistance, formability and acoustic behaviour — decorative screws and fittings, instrument hardware, contact springs, clips and pins — rather than for load. Where a copper-alloy fastener with a standard behind it is needed, the silicon and aluminium bronzes on the F468 list are the covered options, or C71500 where a copper-nickel is wanted.

Every nickel silver order ships with EN 10204 3.1 certification giving the heat analysis, the temper, and the mechanical test results for the product form and section supplied. Nickel and zinc are reported explicitly because the nickel-to-copper ratio governs colour and the zinc content governs dezincification susceptibility. Lead content is certified on the leaded grades, where it matters both for machinability and for regulatory compliance. Positive material identification, stress-relief treatment and colour matching against a supplied sample can all be added at order stage.

Machining: the unleaded nickel silvers carry a CDA machinability rating of 20 — the same as pure copper, where free-cutting brass C36000 is 100. They are tough and gummy, work harden ahead of the tool and produce long continuous swarf with a strong tendency to build up on the cutting edge. C77000 is marginally better at 30. Sharp positive-rake tooling, rigid setups, a positive feed that keeps the tool cutting rather than rubbing, and generous lubricant are all required.

Where machining dominates, change grade. The two leaded nickel silvers exist for precisely this reason: C78200 with 1.5–2.5% lead reaches a machinability rating of 60 — three times the unleaded grades — and C79200 with 0.8–1.4% lead is the other free-machining option. The lead is nearly insoluble in the matrix and sits as discrete particles that break the chip mechanically. The cost is joining performance and, increasingly, regulatory acceptability — see the notes on those pages.

Joining: the unleaded grades solder and braze Excellently and take oxyacetylene and butt welding Well, but CDA rate gas-shielded arc welding only Fair and coated metal arc welding Not Recommended. Zinc volatilisation in the arc is the problem, and it is also a fume hazard — zinc oxide fume causes metal fume fever, so adequate extraction is required whenever these alloys are heated to welding or brazing temperature. Soldering and brazing are the preferred routes, which suits the decorative and instrument work the family is used for.

Heat treatment: nickel silvers are not hardenable by heat treatment. They are single-phase alpha solid solutions with no precipitation reaction to exploit, so strength comes from cold work alone and the temper designation records the degree of reduction — OS grain-size tempers and O annealed conditions at the soft end, then H00, H01, H02, H04, H06 and H08 as cold work increases. Across that range tensile strength roughly doubles while elongation collapses from around 40% to under 5%.

Stress-relief annealing deserves particular attention on these alloys. Because they contain 17–27% zinc they are susceptible to ammonia stress-corrosion cracking, and residual tensile stress from cold work is one of the three ingredients that mechanism needs. A low-temperature stress relief after forming removes that stress while retaining most of the cold-worked strength, and is worth specifying as standard for components going into service rather than treating as optional. Full annealing is carried out in the region of 538–816 °C depending on grade and the grain size required.

Nickel silver contains no silver whatsoever. The name is purely descriptive — these are copper-nickel-zinc alloys, and the nickel bleaches the natural red of copper to a silver-white that closely resembles sterling. They are also sold as German silver, alpaca, maillechort and nickel brass, and the historical trade abbreviation EPNS — electroplated nickel silver — refers to cutlery made by silver-plating a nickel silver base, where the base metal's own colour means a worn plating does not reveal an obviously different metal underneath. That single property, a silver appearance at a fraction of the cost, is the commercial foundation of the whole family.

Colour tracks the nickel-to-copper ratio, and so does price. At the bottom of the range C74500 with 10% nickel retains a distinctly warm, pale-yellow cast. By C75200 at 18% nickel the alloy reads as convincingly silver-white, which is why that grade is the classic. C77000 holds the same 18% nickel against only 55% copper, giving both the whitest colour and the highest strength in the family. If appearance is a specified requirement, state the grade — the difference between 10% and 18% nickel is plainly visible side by side.

These alloys contain 17–27% zinc, and that changes the corrosion rules completely compared with the copper-nickels. It is worth being blunt about this, because the C7xxxx UNS numbering invites the assumption that nickel silvers behave like C70600 and C71500. They do not.

Dezincification applies. In the copper-nickels there is no zinc to lose; here there is a great deal, and in stagnant or slightly acidic chloride waters the zinc can be selectively leached out, leaving a porous, mechanically worthless copper residue that retains the original shape. The nickel content improves resistance substantially over plain brass, but it does not eliminate the mechanism. Ammonia stress-corrosion cracking — the classic ‘season cracking’ of brass — also applies, and a cold-worked or tightened nickel silver component carrying residual tensile stress will crack in moist ammonia, ammonium compounds, amines or nitrites. A stress-relief anneal after cold work is genuinely important on these alloys, not a refinement.

Nickel silvers are not seawater alloys. They carry none of the deliberate iron addition that builds the protective film in the marine copper-nickels, and they should not be specified for seawater piping, condenser tube or any flowing-seawater duty. Their corrosion credentials are for atmospheric exposure, indoor and decorative service, food contact and freshwater — duties in which they perform well and tarnish slowly.

Every grade in this family is rated Poor for hot forming, and that is the governing manufacturing fact. Nickel silvers are hot-short: the zinc volatilises and the alloys crack rather than flow at forging temperature. They are therefore cold-worked materials, and CDA rate most of them Excellent for cold working to match. Components are blanked, drawn, spun, stamped, cold headed, swaged and roll-threaded from strip, rod or wire, with interstage annealing where the work is severe, and the final temper set by the last cold reduction. Annealing is carried out in the region of 538–816 °C depending on grade. Hot forging, hot extrusion and hot rolling are not practical routes for these alloys — design the part for cold forming from the outset.

How the eight divide. Six are unleaded and two are leaded free-machining grades. Among the unleaded, the key variable is the nickel-to-copper ratio, which sets both colour and strength. C74500 (65-10) has the least nickel and the warmest colour; C75700 (65-12) and C75400 (65-15) step up through the middle; C75200 (65-18) is the classic German silver and the industry reference. C73500 is the high-copper, low-zinc member at 72% copper, giving the best corrosion resistance of the group and the standard coinage composition. C77000 (55-18) holds the same 18% nickel at much lower copper, producing the whitest colour and much the highest strength — up to 1000 MPa as hard-drawn wire — which makes it the spring and contact grade. The leaded pair, C78200 and C79200, trade weldability for free-machining behaviour and are chosen for turned and screw-machined parts.
Key Characteristics

  • The 65-12 grade — nickel 11.0–13.0%.
  • One step whiter than C74500 for a small cost increase.
  • 359 MPa annealed rising to 641 MPa at extra hard.
  • Excellent cold formability across the full temper range.
  • Lead held to 0.05%.
  • Solders and brazes Excellently.
  • Poor hot forming — hot-short, must be worked cold.
  • Contains no silver.

Typical Applications

  • Decorative hardware, trim and fittings.
  • Zips, slide fasteners and clasps.
  • Hollowware, giftware and trophies.
  • Optical frames and instrument components.
  • Springs, clips and electrical contacts.
  • Nameplates, badges and signage.
  • Formed and drawn consumer parts.
  • Plated base-metal components.