+91 97734 41022 sales@exoticalloy.com
Material Specification

Beryllium Copper C17300

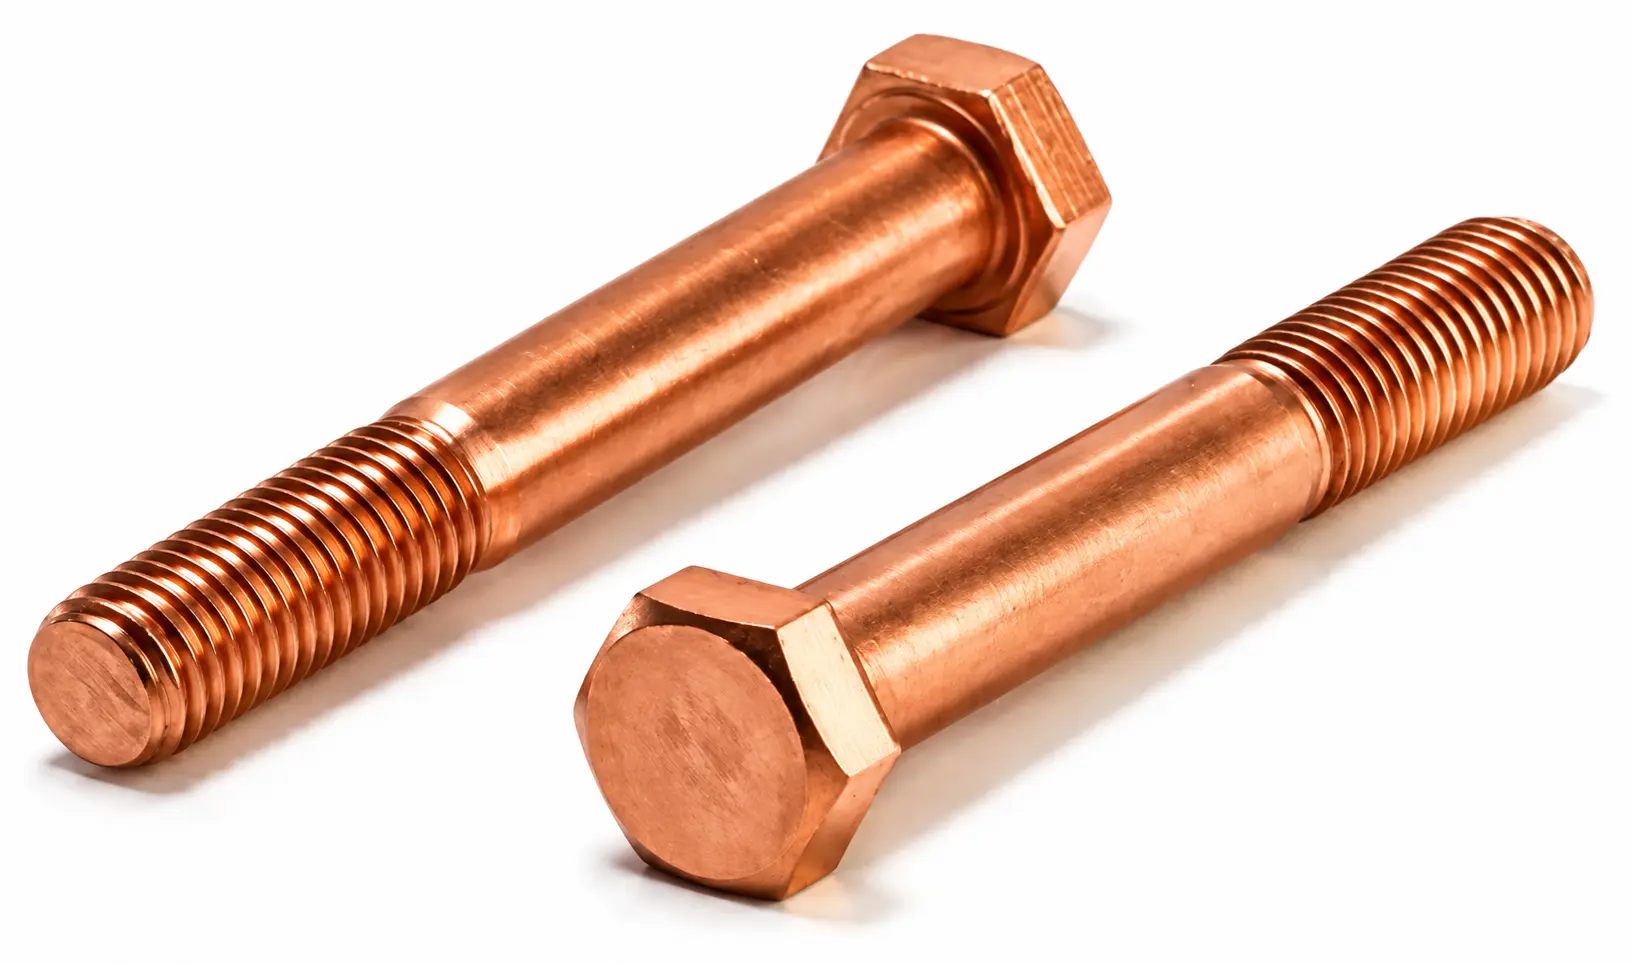
Beryllium Copper C17300 Fasteners
Free-Machining Beryllium Copper — Leaded C17200

Beryllium Copper C17300 Fasteners

Beryllium Copper C17300 is the free-machining version of C17200. The beryllium, cobalt, aluminium and silicon limits are identical — beryllium 1.80–2.00% — with one addition: 0.20–0.6% lead. Lead is nearly insoluble in copper and sits as discrete soft particles that break the chip mechanically and lubricate the cutting edge.

The effect on machining is decisive — CDA machinability rises from 20 to 50, two and a half times better — and the strength is essentially untouched, with precipitation-hardened wire reaching 1462 MPa, marginally above C17200. There are two real costs. Forgeability falls to zero: the lead makes the alloy hot-short, so forging is not a route for this grade. And lead brings regulatory restrictions in drinking-water contact and electronics applications. Where a part is turned, drilled, slotted or threaded from bar, C17300 is the correct choice; where it is forged or where lead is unacceptable, use C17200. Exotic Alloy supplies C17300 under full beryllium particulate controls.

Request a Quote
Product Range

Beryllium Copper C17300 Fasteners Available

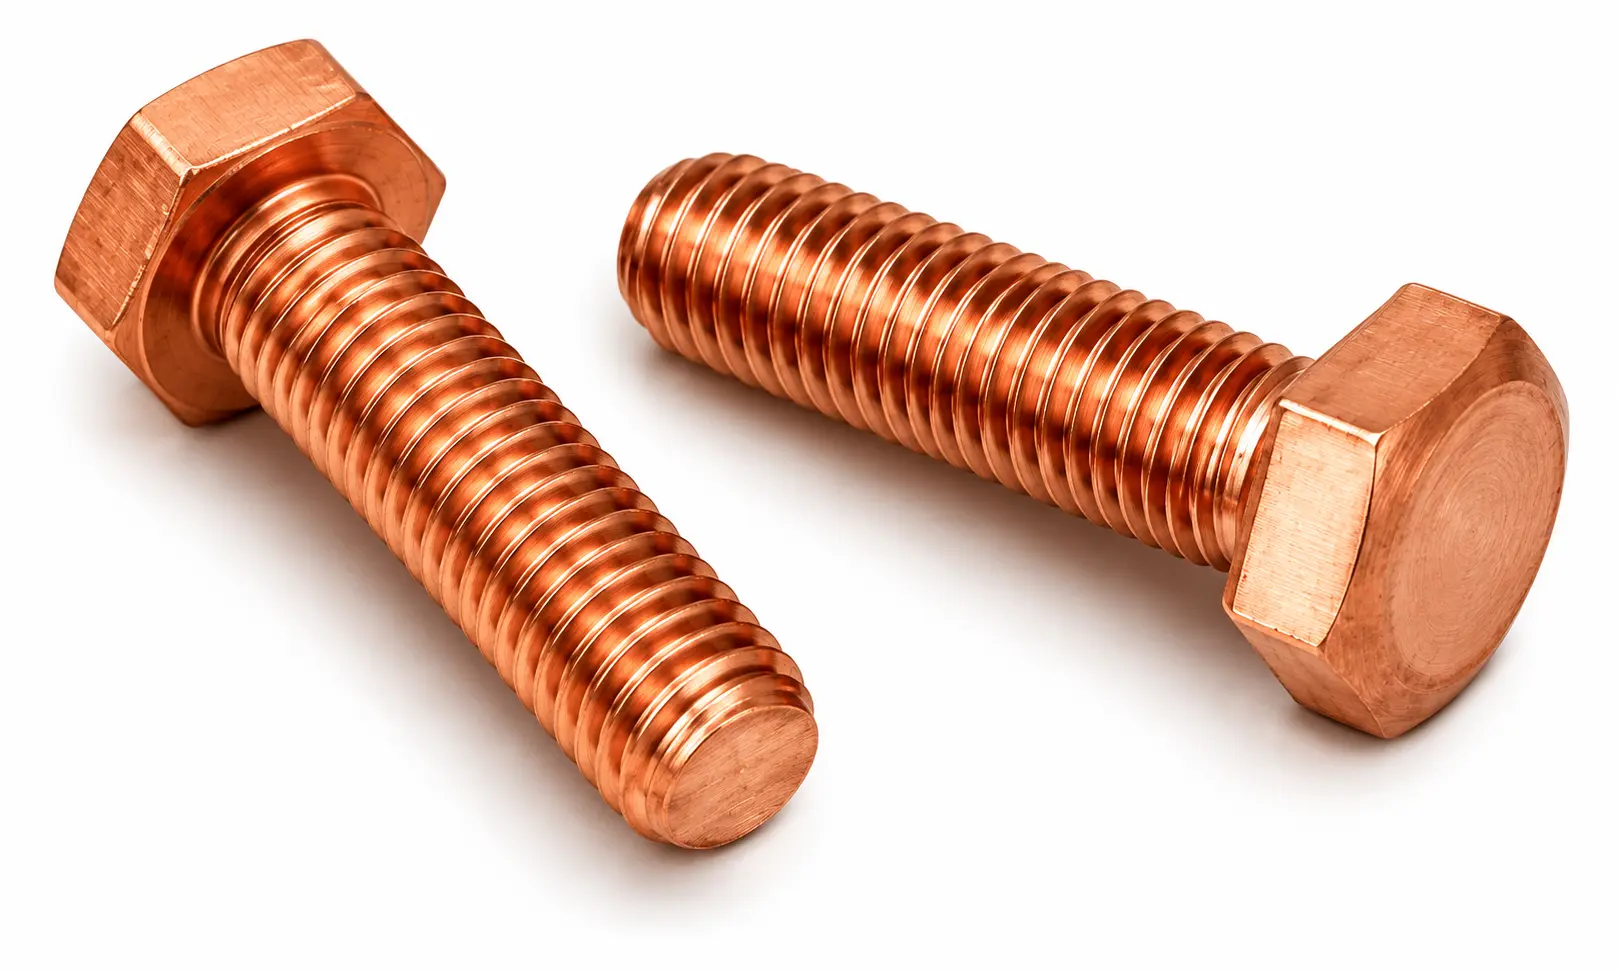
Beryllium Copper C17300 Hex Bolts
Beryllium Copper C17300
Hex Bolts
Beryllium Copper C17300 Heavy Hex Bolts
Beryllium Copper C17300
Heavy Hex Bolts
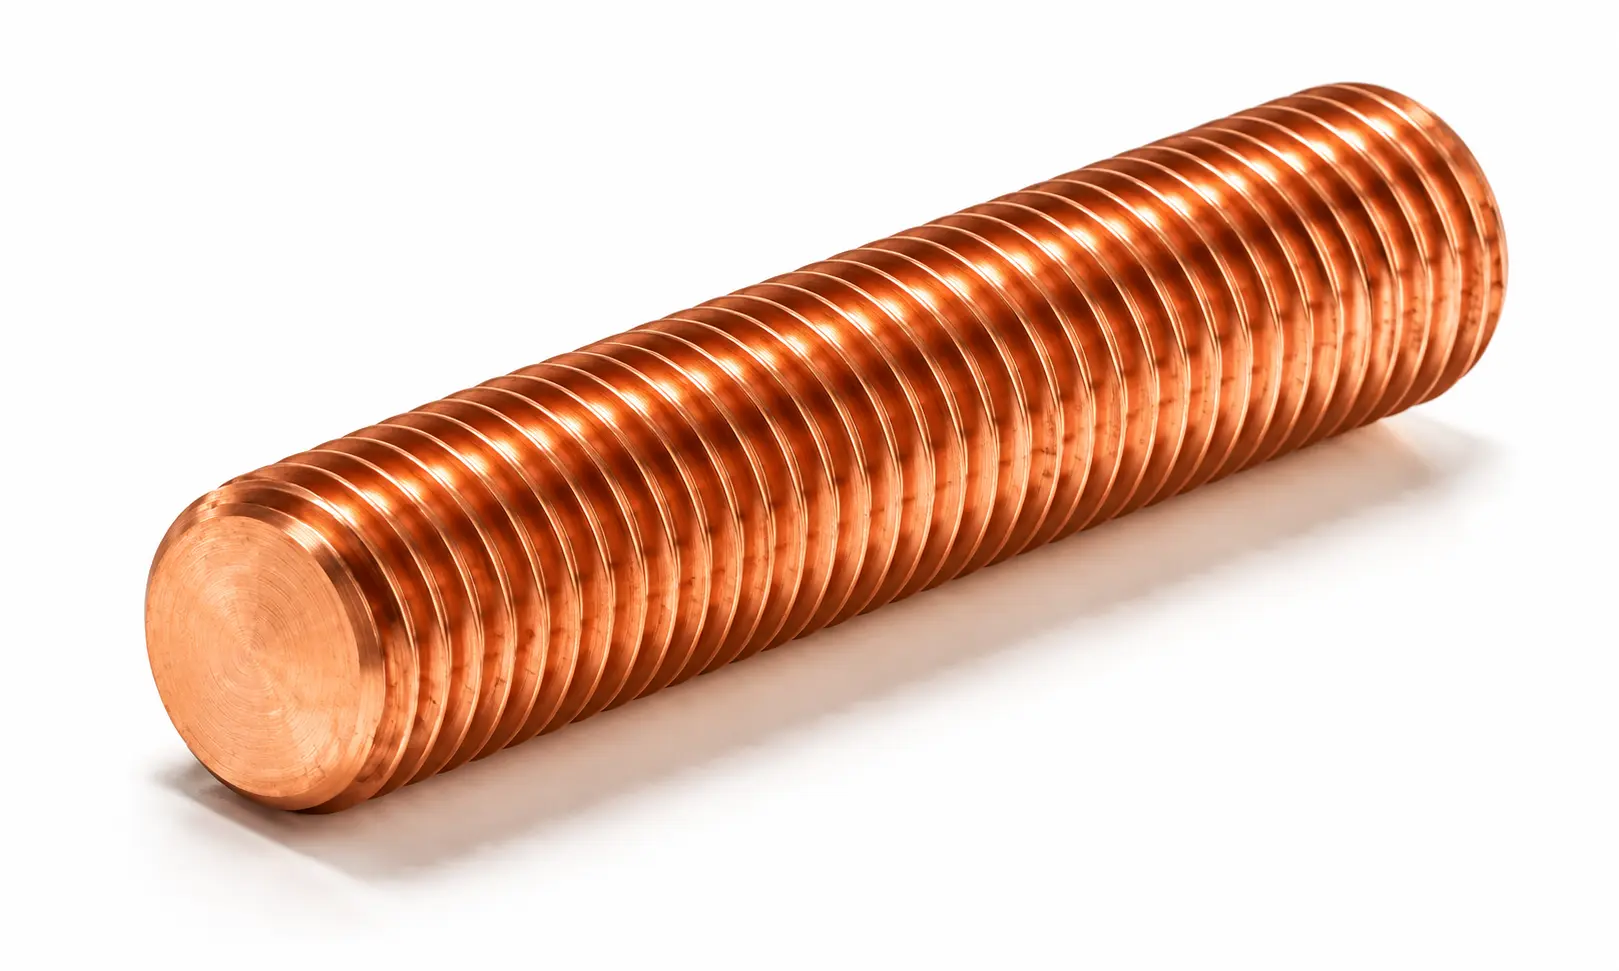
Beryllium Copper C17300 Stud Bolts
Beryllium Copper C17300
Stud Bolts
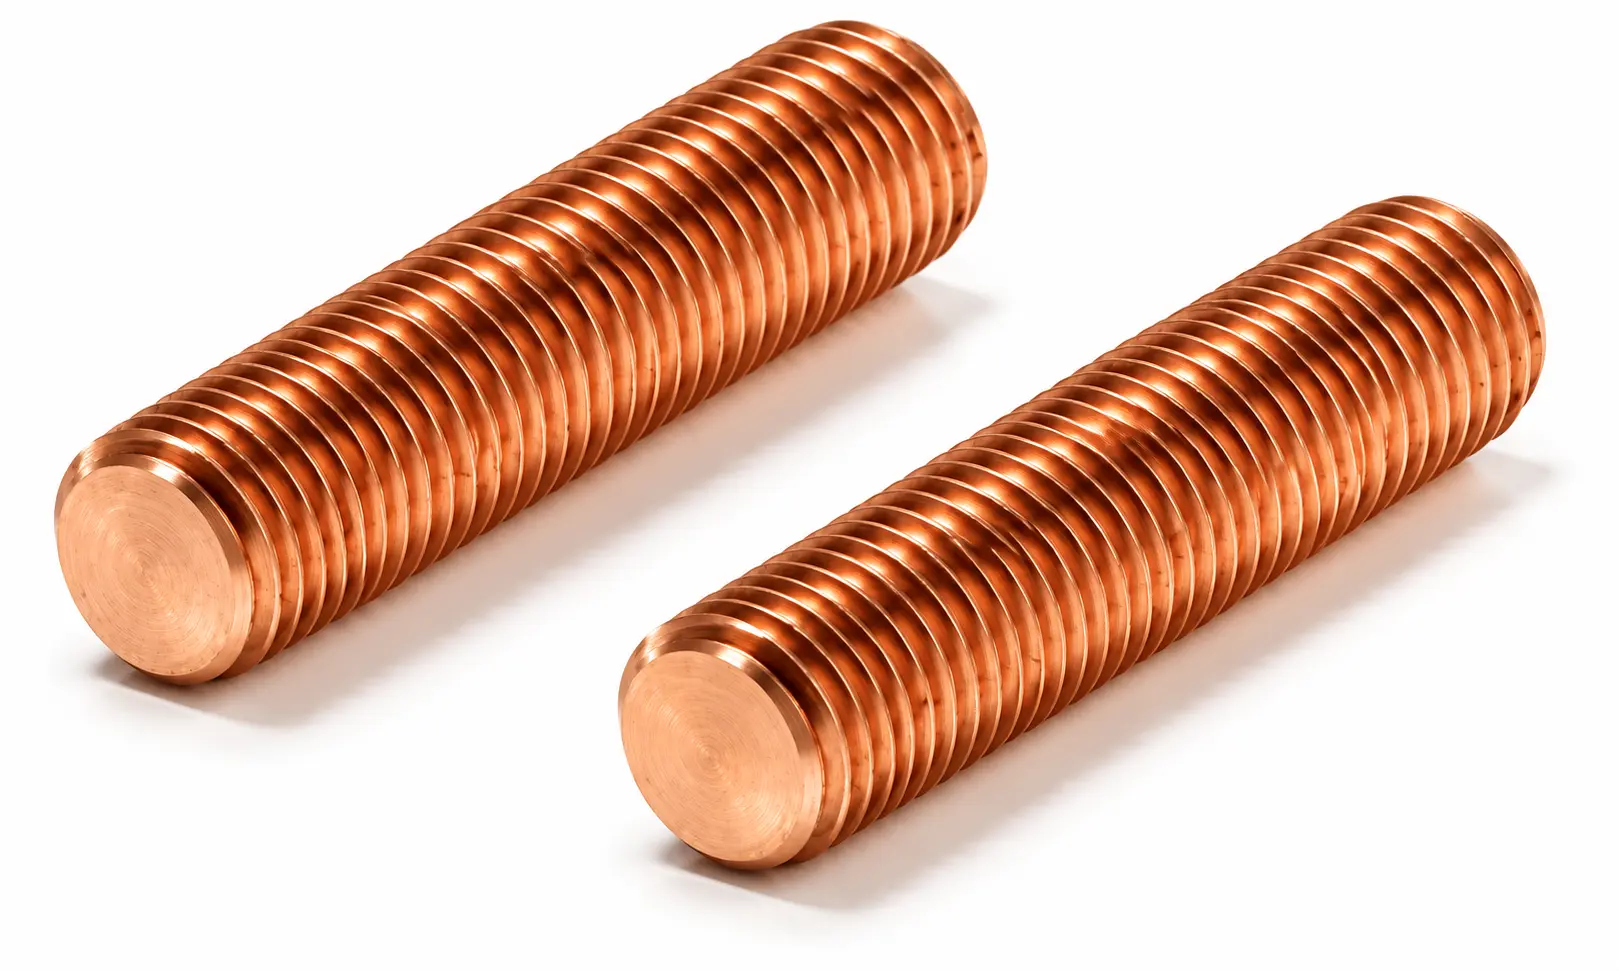
Beryllium Copper C17300 Threaded Rods
Beryllium Copper C17300
Threaded Rods
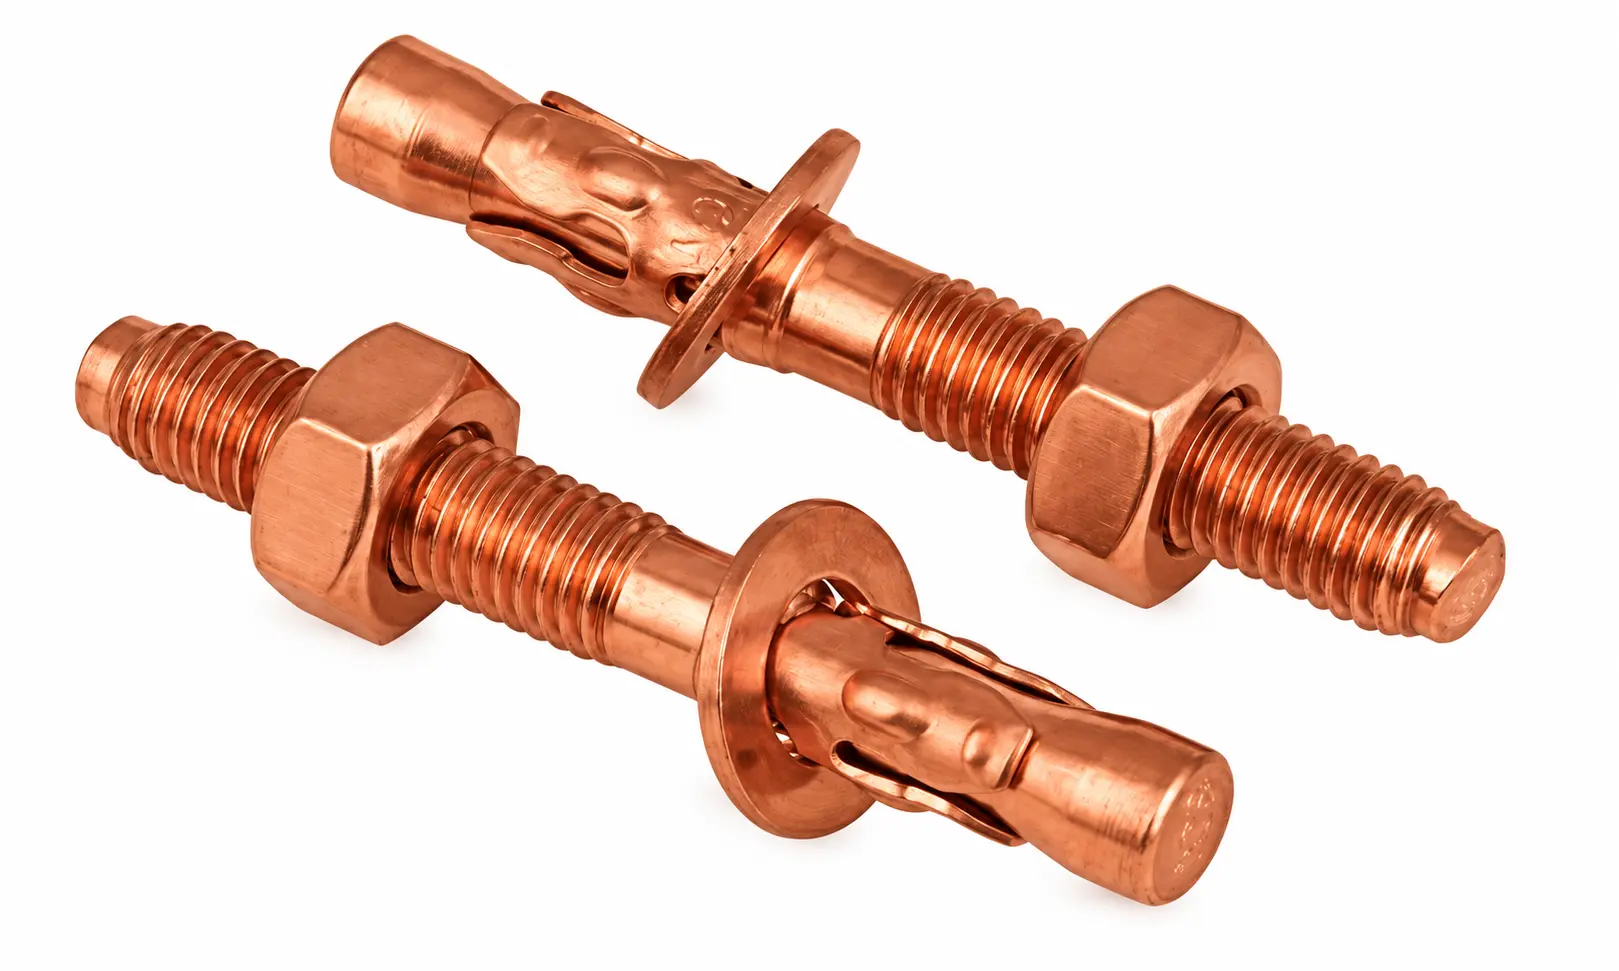
Beryllium Copper C17300 Anchor Bolts
Beryllium Copper C17300
Anchor Bolts
Beryllium Copper C17300 Hex Nuts
Beryllium Copper C17300
Hex Nuts
Beryllium Copper C17300 Washers
Beryllium Copper C17300
Washers
Beryllium Copper C17300 Cotter Pins
Beryllium Copper C17300
Cotter Pins
Beryllium Copper C17300 Springs
Beryllium Copper C17300
Springs
Beryllium Copper C17300 Circlips
Beryllium Copper C17300
Circlips
Beryllium Copper C17300 Coated Fasteners
Beryllium Copper C17300
Coated Fasteners
Beryllium Copper C17300 Custom Spacers
Beryllium Copper C17300
Custom Spacers
Technical Data

Beryllium Copper C17300 Specifications

Chemical Composition — Beryllium Copper C17300 (wt. %)
ElementMinimum %Maximum %
Copper (Cu), including silverRemainder—
Beryllium (Be)1.802.00
Lead (Pb)0.200.6
Cobalt (Co)0.20—
Aluminium (Al)—0.20
Silicon (Si)—0.20
Nickel + Cobalt0.20—
Nickel + Iron + Cobalt—0.6
Copper + sum of named elements99.5—
Mechanical Properties — Beryllium Copper C17300
ConditionUTS (MPa)YS 0.2% (MPa)Elongation (%)Hardness
Rod, solution treated TB004691724862 HRB
Rod 28 mm, sol. treated + hard TD046896211595 HRB
Rod 9.5 mm, sol. treated + hard TD047726211595 HRB
Rod, precipitation hardened TF001255896639 HRC
Rod 28 mm, hard + precip. treated TH0413101207341 HRC
Rod 25 mm, hard + precip. treated TH04134512275—
Wire, solution treated TB0046919335—
Wire, sol. treated + 1/4 hard TD0170356510—
Wire, sol. treated + 1/2 hard TD028416895—
Wire, sol. treated + 3/4 hard TD039798272—
Wire, sol. treated + hard TD0410488621—
Wire, precipitation hardened TF00122711033—
Wire, 1/4 hard + precip. treated TH01131012072—
Wire, 1/2 hard + precip. treated TH02137912761—
Wire, 3/4 hard + precip. treated TH03144813101—
Wire, hard + precip. treated TH04146213451—
Physical Properties
Density8.26 g/cm³ (0.298 lb/in³)
Melting Point — Liquidus982 °C (1800 °F)
Melting Point — Solidus866 °C (1590 °F)
Electrical Conductivity22% IACS at 20 °C, precipitation hardened
Thermal Conductivity107 W/m·K at 20 °C (actual 107–130)
Coefficient of Thermal Expansion17.8 × 10⁻⁶ /°C (20–300 °C)
Specific Heat Capacity419 J/kg·K at 20 °C
Modulus of Elasticity128 GPa
Modulus of Rigidity50 GPa
Solution Treatment774–802 °C (1425–1475 °F), water quench
Precipitation Treatment316 °C (600 °F), air
Stress Relief204 °C (400 °F)
Hot Working Temperature649–816 °C (1200–1500 °F)
Hardenable by Heat TreatmentYes — precipitation hardening
Magnetic ResponseNon-magnetic; non-sparking
Forgeability Rating0 — lead makes the alloy hot-short
Machinability Rating50 (C36000 = 100)
Equivalent Grades & Standards
UNSEN / CEN DesignationNominal CompositionCommon Name
C17300 — Cu-1.9Be-0.4Pb Leaded Beryllium Copper, Alloy 25 free-machining, CDA 173

Key Specifications: ASTM B194 (Copper Beryllium Alloy Plate, Sheet, Strip & Rolled Bar) / ASTM B196/B196M (Copper Beryllium Alloy Rod & Bar) / ASTM B197 (Copper Beryllium Alloy Wire) / AMS 4530, 4532, 4533, 4534, 4650 and 4651 / MIL-C-21657 / SAE J461 and J463.

A note on the lead. The lead that makes this grade free machining also restricts where it can be used. Lead content is regulated in drinking-water contact components in most jurisdictions, and under RoHS in electrical and electronic equipment, where copper-alloy exemptions have been progressively narrowed. Confirm the regulatory position for your market before committing a design; where lead is unacceptable, C17200 gives the same strength at a machinability rating of 20.

Note on fastener standards: Beryllium copper is not covered by the ASTM nonferrous fastener standards. ASTM F468 and F467 carry C11000, C26000, C27000, C46200, C46400, C51000, C61300, C61400, C63000, C64200, C65100, C65500, C66100, C67500, C71000 and C71500 — no beryllium copper appears among them. Fasteners in these alloys are manufactured from material certified to ASTM B194, B196, B197, B441, B534 or the applicable AMS specification, with thread conformance to the relevant ASME or ISO standard and acceptance criteria agreed on the order.

That said, beryllium copper makes a genuinely exceptional fastener where its properties are needed, and CDA list fasteners explicitly among the typical uses for C17500. At up to 1448 MPa, C17200 is stronger than an ASTM A325 structural steel bolt at 830 MPa and comparable with property class 12.9 — the only copper alloy of which that is true — while remaining non-magnetic, non-sparking, corrosion resistant and electrically conductive. For downhole tooling, hazardous-area equipment, subsea instrumentation and non-magnetic assemblies, that combination has no substitute.

Every beryllium copper order ships with EN 10204 3.1 certification giving the heat analysis, the temper and heat-treatment condition, and the mechanical test results for that temper and section. Beryllium content is certified explicitly, both because it determines the strength and conductivity class and because it determines the regulatory handling regime downstream. Electrical conductivity testing to ASTM B193, hardness survey, and solution treatment and ageing to a specified temper can all be added at order stage. Safety data sheets accompany every shipment.

Form soft, age hard — that is the whole fabrication strategy. Blanking, drawing, deep forming, coiling, bending and cold heading are all carried out in the solution-treated TB00 condition or a low TD temper, where the alloy is ductile and compliant. The finished part is then precipitation hardened. Designers who try to form an already-aged temper find the material unforgiving; designers who form soft and age afterwards get both the geometry and the strength. Allow for the small but real dimensional change that occurs during ageing on precision parts.

Machining: the unleaded high-strength grade C17200 carries a CDA machinability rating of only 20 — the same as pure copper. The high-conductivity C17500 is better at 40, and the leaded C17300 reaches 50, which is why that grade exists. Machining is normally done before ageing, both because the soft condition cuts more easily and because the aged material is hard on tooling. All machining must be performed under the beryllium particulate controls set out below — wet methods, local exhaust ventilation, HEPA cleaning.

Joining: CDA rate the high-strength grades Good for soldering, brazing, gas-shielded arc welding, coated metal arc welding and spot welding, Fair for seam and butt welding, and Not Recommended for oxyacetylene welding. The high-conductivity grades drop to Fair for arc welding because the higher thermal conductivity carries heat away from the joint. Two cautions: any welding or brazing cycle will locally over-age or re-solution the precipitate structure, so a welded assembly should be re-heat-treated or designed on softened heat-affected-zone properties; and welding and brazing generate beryllium fume, which demands the full extraction controls.

C17300 specifically: this is the grade to specify when machining dominates. At a rating of 50 against C17200's 20 it cuts two and a half times better, giving short broken chips, clean threads and good tool life on screw-machine work. The penalties are that forgeability falls to zero — the lead makes the alloy hot-short, so forging is not available — and that lead further limits welding, which was already restricted. Machine before ageing, and under the full beryllium particulate controls.

Heat treatment is the entire point of this alloy, and the cycle has three stages.

Solution treatment is carried out at 774–802 °C (1425–1475 °F) per CDA, followed by a water quench, to dissolve the beryllium and freeze it in supersaturated solid solution. The resulting TB00 condition is soft — around 483 MPa at 45% elongation — and is the right state for forming.

Cold working between solution treatment and ageing is optional, producing the TD tempers on its own and the much stronger TH tempers when followed by ageing.

Precipitation treatment (ageing) is carried out at approximately 316 °C (600 °F) in air, typically for a few hours. CDA also give a stress relief temperature of 204 °C (400 °F), and a hot working range of 649–816 °C.

Over-ageing softens the alloy permanently. Holding it above the ageing temperature — in a welding cycle, a brazing operation or in sustained hot service — coarsens the precipitate and the material does not recover on cooling. Only a full re-solution-treat, quench and re-age will restore it. This also sets the practical service ceiling: beryllium coppers are not elevated-temperature materials, and sustained service much above the ageing temperature should be treated as a design problem.

Beryllium copper is the strongest copper alloy there is, and the mechanism is precipitation hardening. Beryllium has appreciable solubility in copper at high temperature and very little at low temperature, so the alloy can be solution treated to take the beryllium into solution, quenched to hold it there in supersaturation, and then aged to precipitate it as an extremely fine coherent dispersion. The resulting strengths are in a different class from any other copper: C17200 reaches 1448 MPa as precipitation-hardened wire — comparable with a quenched and tempered alloy steel, and nearly three times what the best chromium copper manages.

The commercially useful consequence is that the alloy is soft when you form it and hard when you use it. In the solution-treated condition C17200 is around 483 MPa with 45% elongation — readily blanked, drawn, formed, coiled and cold headed. The part is then aged, typically a few hours at 315 °C, and comes out at two to three times the strength with the formed geometry intact. No other copper alloy offers that combination, and it is why beryllium copper dominates precision springs, contacts and formed electrical components.

Beryllium coppers split into two distinct families, and the split is between strength and conductivity. The high-strength grades — C17200 and its free-machining variant C17300 — carry 1.80–2.00% beryllium and reach 1380–1450 MPa, but at only 22% IACS conductivity. The high-conductivity grades — C17500 with cobalt and C17510 with nickel — carry only 0.2–0.7% beryllium and peak around 793 MPa, but deliver 45–48% IACS, more than double, with thermal conductivity roughly twice as high at 208 against 107 W/m·K.

The choice follows directly from the duty. A spring contact that must carry force is a high-strength application; a current-carrying component, a resistance welding electrode or a die-casting plunger tip that must shed heat is a high-conductivity one. The cobalt and nickel in the low-beryllium grades do the same job as the beryllium does in C17200 — they form the precipitate — but with far less beryllium in solution to scatter conduction electrons.

The temper designation on a beryllium copper records a thermal and a mechanical history, and both matter. The modern system runs: TB00, solution heat treated — the soft, formable, supersaturated condition; TD01 to TD04, solution treated and then cold worked to quarter, half, three-quarter or full hard, with the beryllium still in solution; TF00, precipitation hardened directly from solution treatment; and TH01 to TH04, cold worked and then precipitation hardened, which stacks both mechanisms and gives the highest properties in the alloy. The older designations map across directly — A, 1/4H, 1/2H, H for the pre-age conditions and AT, 1/4HT, 1/2HT, HT for the aged ones.

The TM mill-hardened tempers deserve separate mention, because they solve a real production problem. TM00, TM01, TM02, TM04, TM05, TM06 and TM08 are supplied already aged by the mill to a guaranteed strength and formability combination. The user forms the part and uses it with no heat treatment at all. That removes the ageing furnace, the distortion risk and the handling step from the production route, at the cost of a lower peak strength than a user-aged TH temper would reach. For high-volume stamped contacts and connectors the mill-hardened tempers are usually the right commercial answer.

Non-sparking and non-magnetic behaviour is one of the two things beryllium copper is uniquely bought for. Struck against steel or stone, beryllium copper does not throw the incendive sparks that a ferrous tool does, and it is essentially non-magnetic. That combination makes it the standard material for safety tools in explosive atmospheres — oil and gas installations, refineries, chemical plant, munitions handling, grain and dust environments — and for tooling and instruments that must work near sensitive magnetic equipment, including mine countermeasures and magnetic resonance environments. CDA list navigational instruments among the typical uses for C17200 for exactly this reason, and the dedicated military specification MIL-C-21657, ‘Copper-Beryllium Alloy, Low Magnetic Effect (for Special Purpose Tools and Equipment)’, exists to cover it.

It is worth being precise about the claim: non-sparking tools reduce the risk of ignition, they do not eliminate it. A tool can still ignite an atmosphere through friction heating or by striking certain materials. Non-sparking tooling is one layer of control in a hazardous area, not a substitute for the others.

Corrosion behaviour is broadly that of copper, with some genuine advantages. Beryllium coppers resist fresh and salt water, atmospheric exposure, non-oxidising acids free of dissolved oxygen, and neutral and alkaline salt solutions. CDA list corrosion resistance as a reason for use across almost every application they record for these alloys. Unlike the brasses and nickel silvers there is no zinc, so dezincification does not apply, and beryllium coppers are notably more resistant to stress-corrosion cracking than those families — a real advantage for springs, which are by definition held under sustained stress.

The copper family's limits still hold: attack by oxidising acids (nitric rapidly, sulfuric or hydrochloric once oxygen or ferric iron is present), by oxidising salts such as ferric and cupric chloride, and by sulfides and hydrogen sulfide. Ammonia and amines warrant caution for stressed components as with any copper alloy. Beryllium coppers are also widely used in sour service downhole tooling, where their resistance to hydrogen embrittlement and sulfide stress cracking relative to high-strength steels at comparable strength is a significant part of the case for them.

How the four divide. Two axes: beryllium content and lead. C17200 is the reference high-strength grade at 1.80–2.00% beryllium, reaching 1448 MPa at 22% IACS — the alloy for springs, contacts, non-sparking tools and downhole hardware. C17300 is the same alloy with 0.20–0.6% lead added, lifting machinability from 20 to 50 for screw-machine work at the cost of forgeability and some joining performance. C17500 swaps most of the beryllium for 2.4–2.7% cobalt, giving 45% IACS and 208 W/m·K at up to 793 MPa — the grade for current-carrying and heat-shedding duty, resistance welding hardware and die-casting plunger tips. C17510 does the same job with 1.4–2.2% nickel instead of cobalt, reaching 48% IACS in the HT temper. Choose on conductivity first, then on whether you need free machining.

Beryllium is a recognised occupational health hazard, and it must be managed properly. Here is the position stated plainly.

Solid beryllium copper is safe to handle. Finished bar, strip, wire, fasteners and components present no beryllium hazard in normal handling, installation or service. There is no risk from touching the metal, and no risk to the end user of a finished part. The hazard is entirely one of inhaling airborne beryllium particulate — dust, fume or mist — and it arises only where a process generates it: machining, grinding, sanding, abrasive blasting, welding, brazing, melting and similar operations.

What the hazard is. Inhaled beryllium particulate can cause beryllium sensitisation, an immune response, in a minority of exposed people. Sensitised individuals may go on to develop Chronic Beryllium Disease (CBD), an irreversible granulomatous lung disease. Very high short-term exposures can cause acute beryllium disease, and beryllium is classified by IARC as a Group 1 human carcinogen for lung cancer. These are serious outcomes and the reason the controls below are not optional.

The regulatory limits. Under the OSHA beryllium standard, 29 CFR 1910.1024, the permissible exposure limit is 0.2 µg/m³ as an 8-hour time-weighted average, with a short-term exposure limit of 2.0 µg/m³ over 15 minutes and an action level of 0.1 µg/m³. The standard excludes materials containing less than 0.1% beryllium by weight where objective data show exposures stay below the action level — every grade on this hub is well above that threshold, from 0.2% in C17510 to 2.00% in C17200, so the standard applies in full. Other jurisdictions set their own limits; check the rules for your location.

The controls that matter. Local exhaust ventilation captured at the point of generation; wet machining and wet grinding methods; no dry grinding, dry sanding or abrasive blasting; enclosure of dusty operations where practicable; cleaning by HEPA vacuum or wet methods only — never compressed air or dry sweeping, which simply re-suspend the particulate; separate work clothing that does not go home; washing facilities; exposure assessment and medical surveillance where required. Exotic Alloy operates these controls on all beryllium copper work. If you are machining beryllium copper in your own facility, obtain the supplier safety data sheet and implement the controls before starting.
Key Characteristics

  • The free-machining version of C17200 — 0.20–0.6% lead added.
  • Machinability 50 against 20 for C17200.
  • Beryllium 1.80–2.00% — identical to C17200.
  • Reaches 1462 MPa as precipitation-hardened wire.
  • Forgeability rating 0 — lead makes it hot-short.
  • Lead restricted in drinking-water and RoHS applications.
  • Non-magnetic and non-sparking as C17200.
  • 22% IACS electrical conductivity.

Typical Applications

  • Turned and screw-machined high-strength components.
  • Threaded fasteners, studs and adaptors from bar.
  • Non-sparking machined safety tools and fittings.
  • Downhole and oilfield machined tooling.
  • Precision machined instrument components.
  • Bushings, bearings and wear components.
  • Valve and pump machined parts.
  • High-volume turned electrical hardware.