+91 97734 41022 sales@exoticalloy.com
Material Specification

Aluminium 5083

Aluminium 5083 Fasteners
High-Magnesium Marine Alloy — Strongest Non-Heat-Treatable

Aluminium 5083 Fasteners

Aluminium 5083 is the highest-strength aluminium alloy available without heat treatment. Its composition is 4.0–4.9% magnesium with 0.40–1.0% manganese and 0.05–0.25% chromium. ASTM B209M specifies 275–350 MPa tensile with 125 MPa yield for 5083-O, rising to 305–385 MPa at H32 — strength comparable to a 6xxx alloy, achieved entirely by solid-solution strengthening and cold work.

5083 is the premier marine structural alloy: exceptional resistance to seawater and industrial atmospheres, excellent weldability with 5183 or 5356 filler, and it retains its strength remarkably well in the as-welded condition because there is no heat treatment to destroy. It is also a standard cryogenic material, with strength and toughness that increase as temperature falls, used down to liquid-helium temperatures. The one critical limitation is the mirror image of that: at above 3% magnesium 5083 sensitises in sustained service above about 65 °C, becoming susceptible to intergranular corrosion and cracking. Exotic Alloy supplies 5083 marine fasteners and fabricated components.

Request a Quote
Product Range

Aluminium 5083 Fasteners Available

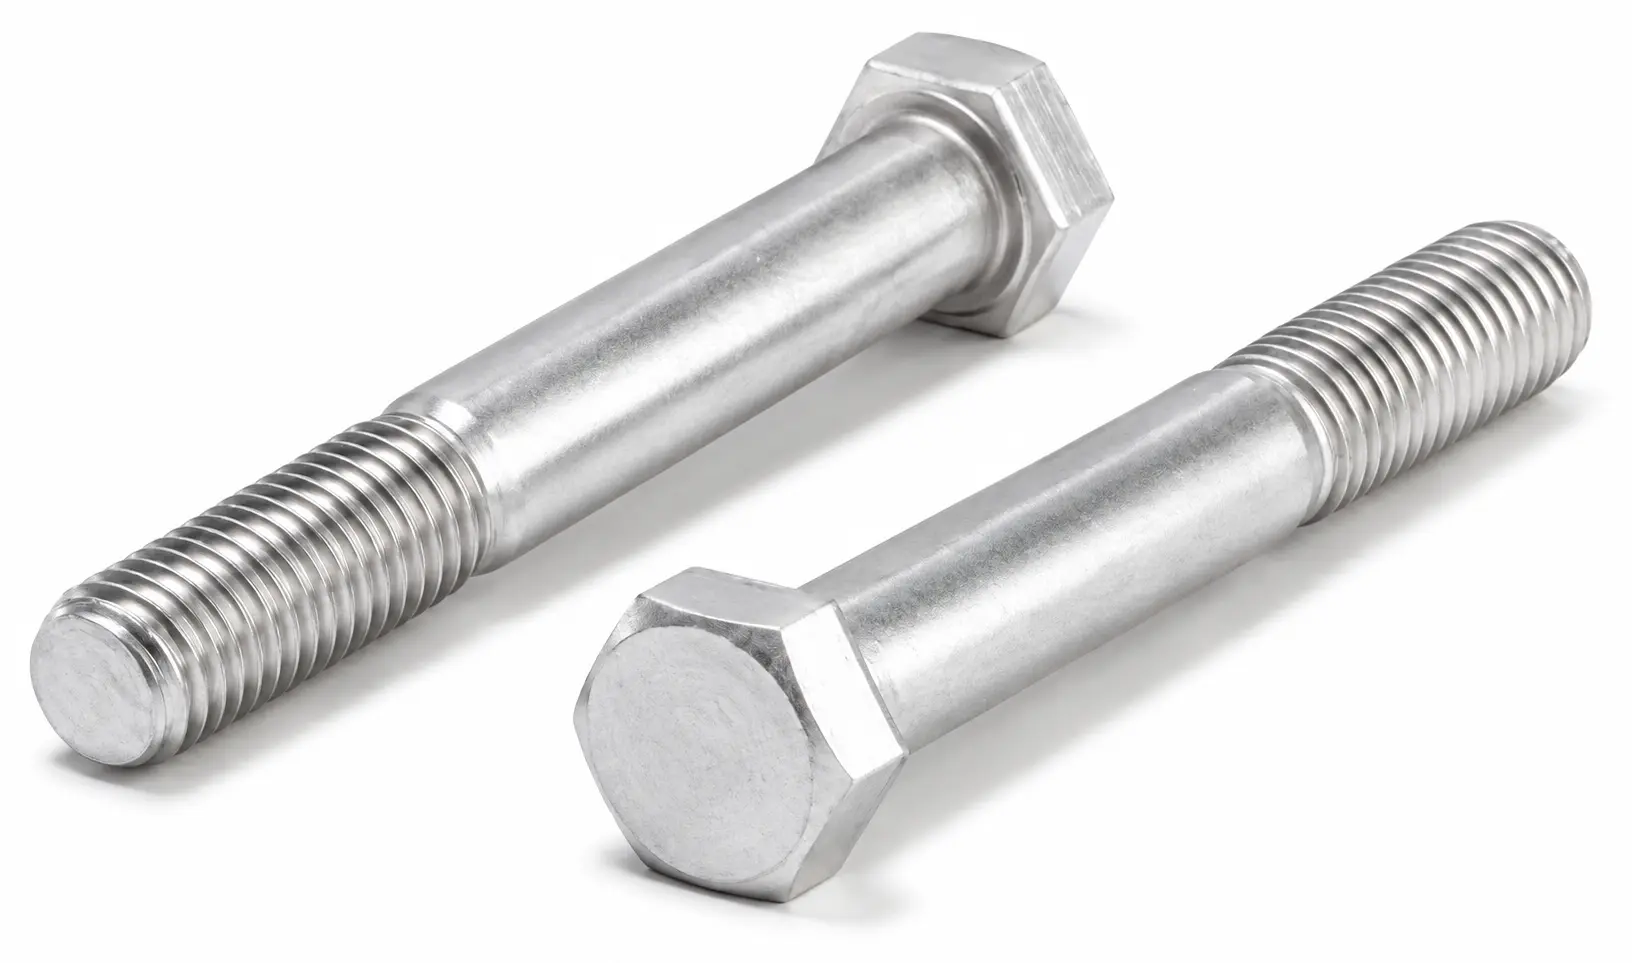
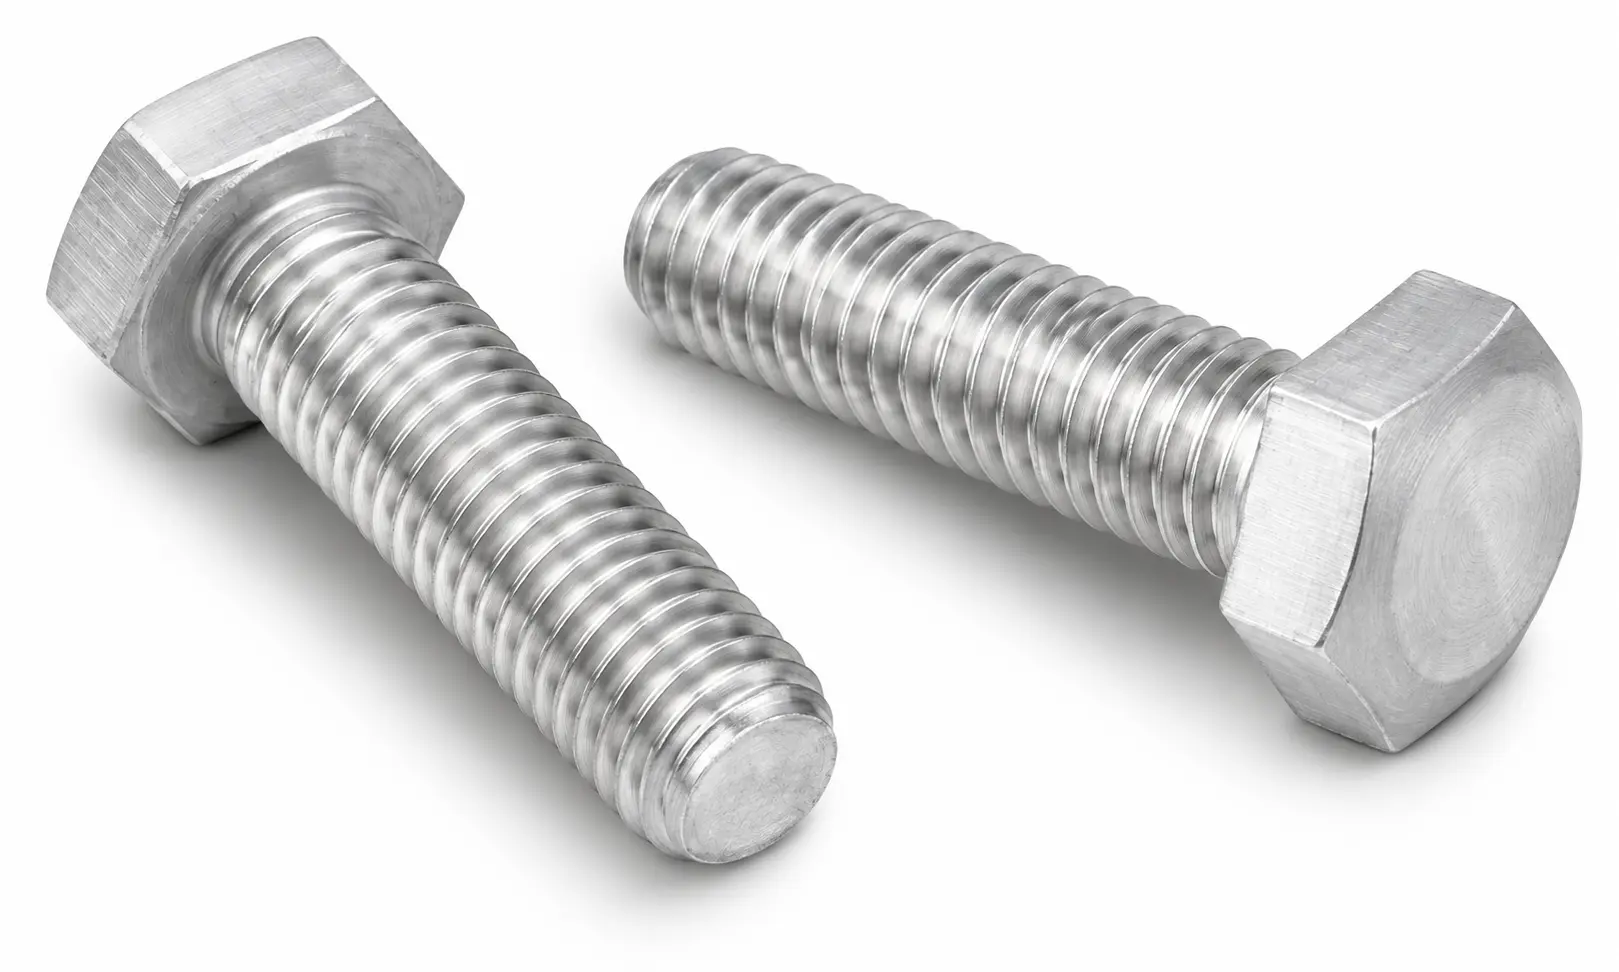
Aluminium 5083 Hex Bolts
Aluminium 5083
Hex Bolts
Aluminium 5083 Heavy Hex Bolts
Aluminium 5083
Heavy Hex Bolts
Aluminium 5083 Stud Bolts
Aluminium 5083
Stud Bolts
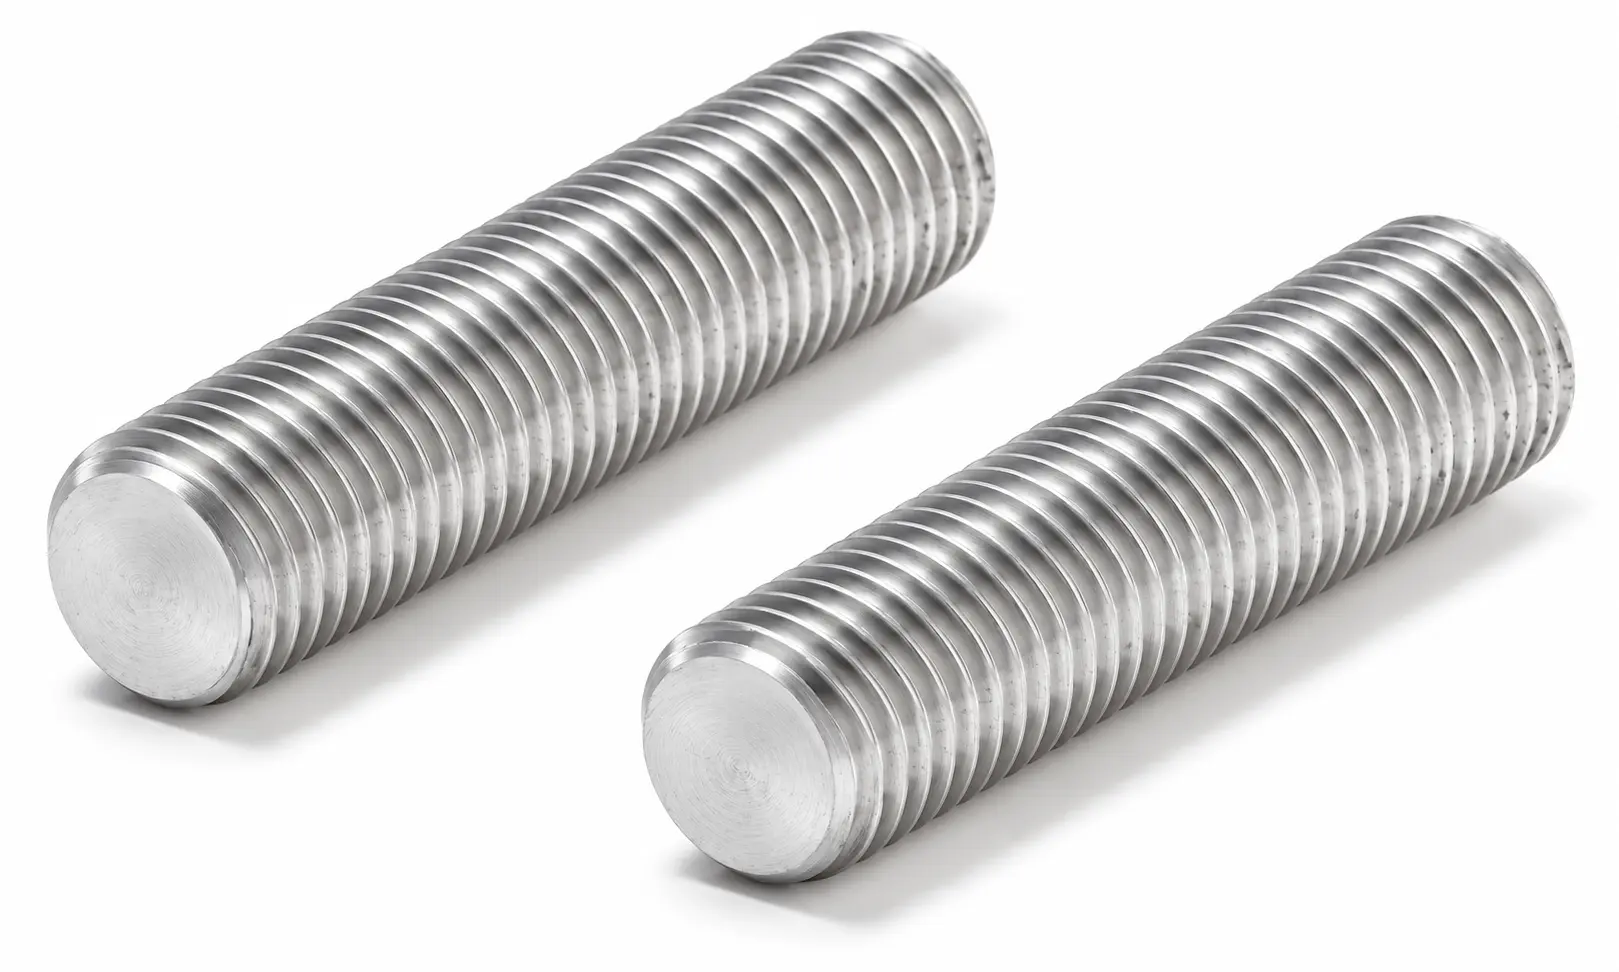
Aluminium 5083 Threaded Rods
Aluminium 5083
Threaded Rods
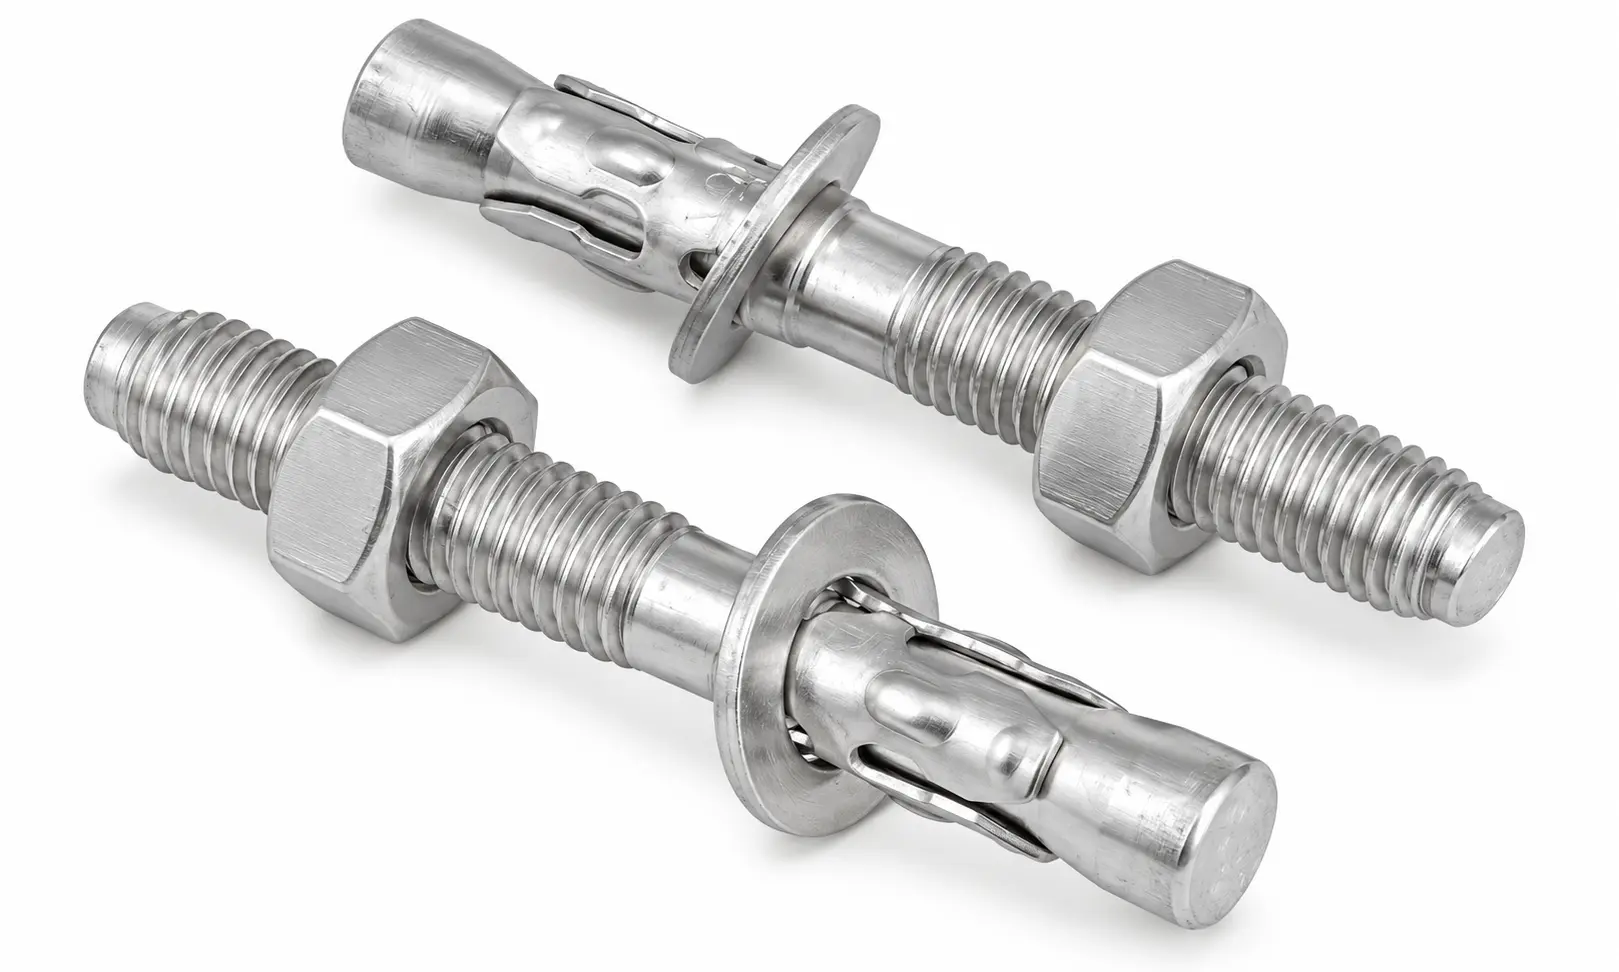
Aluminium 5083 Anchor Bolts
Aluminium 5083
Anchor Bolts
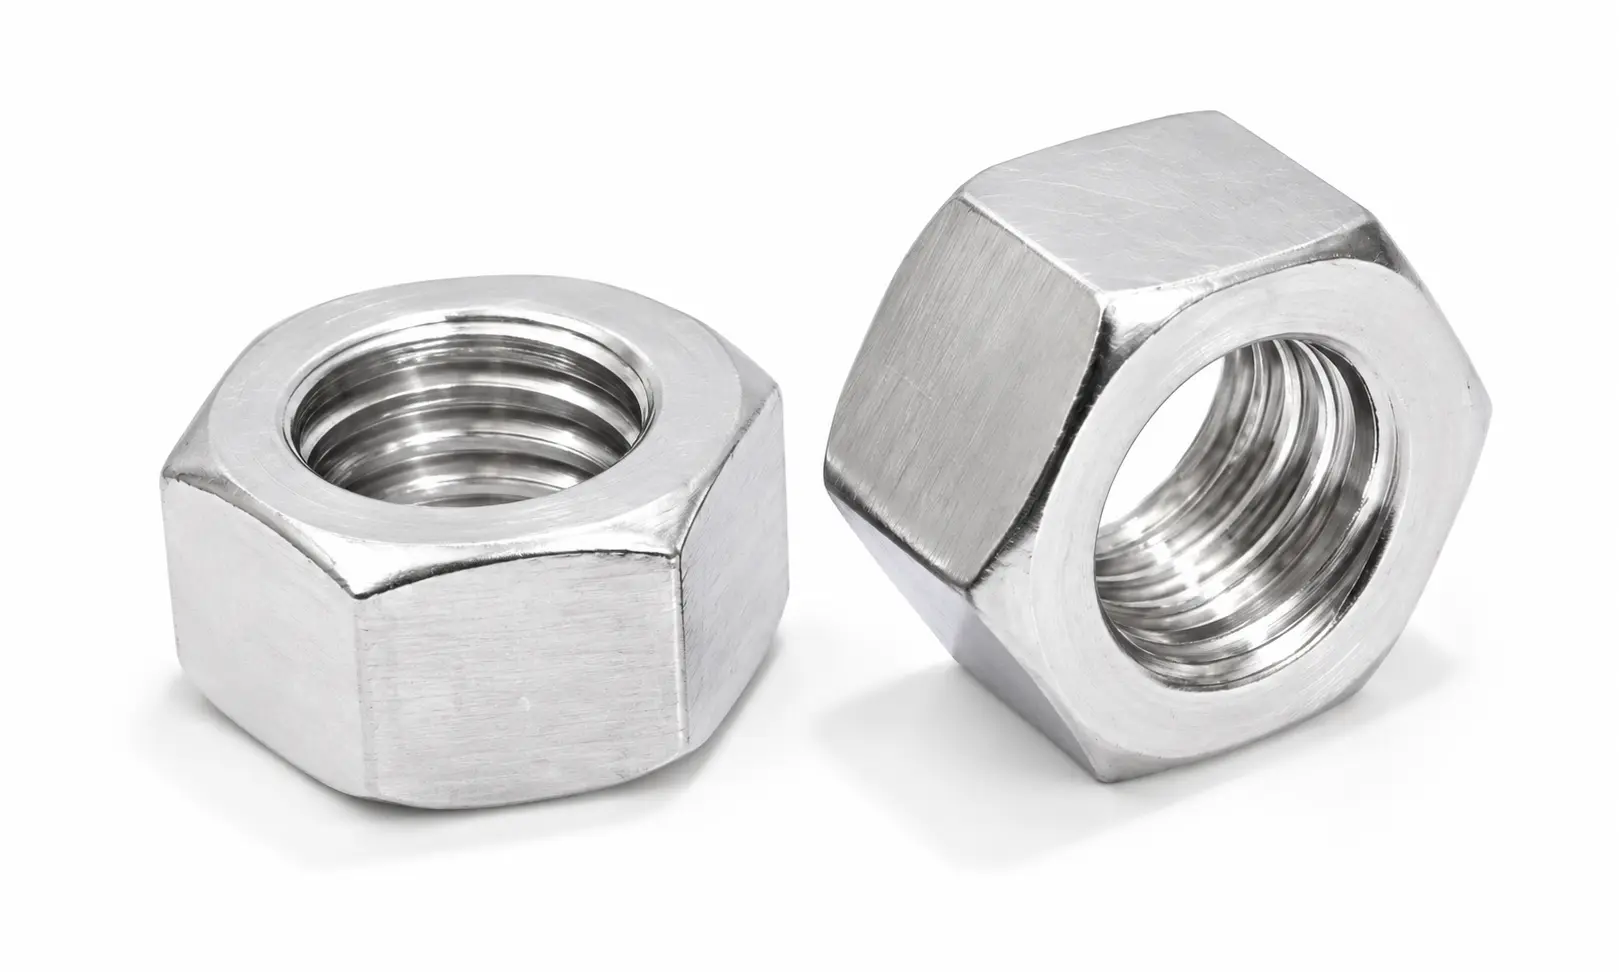
Aluminium 5083 Hex Nuts
Aluminium 5083
Hex Nuts
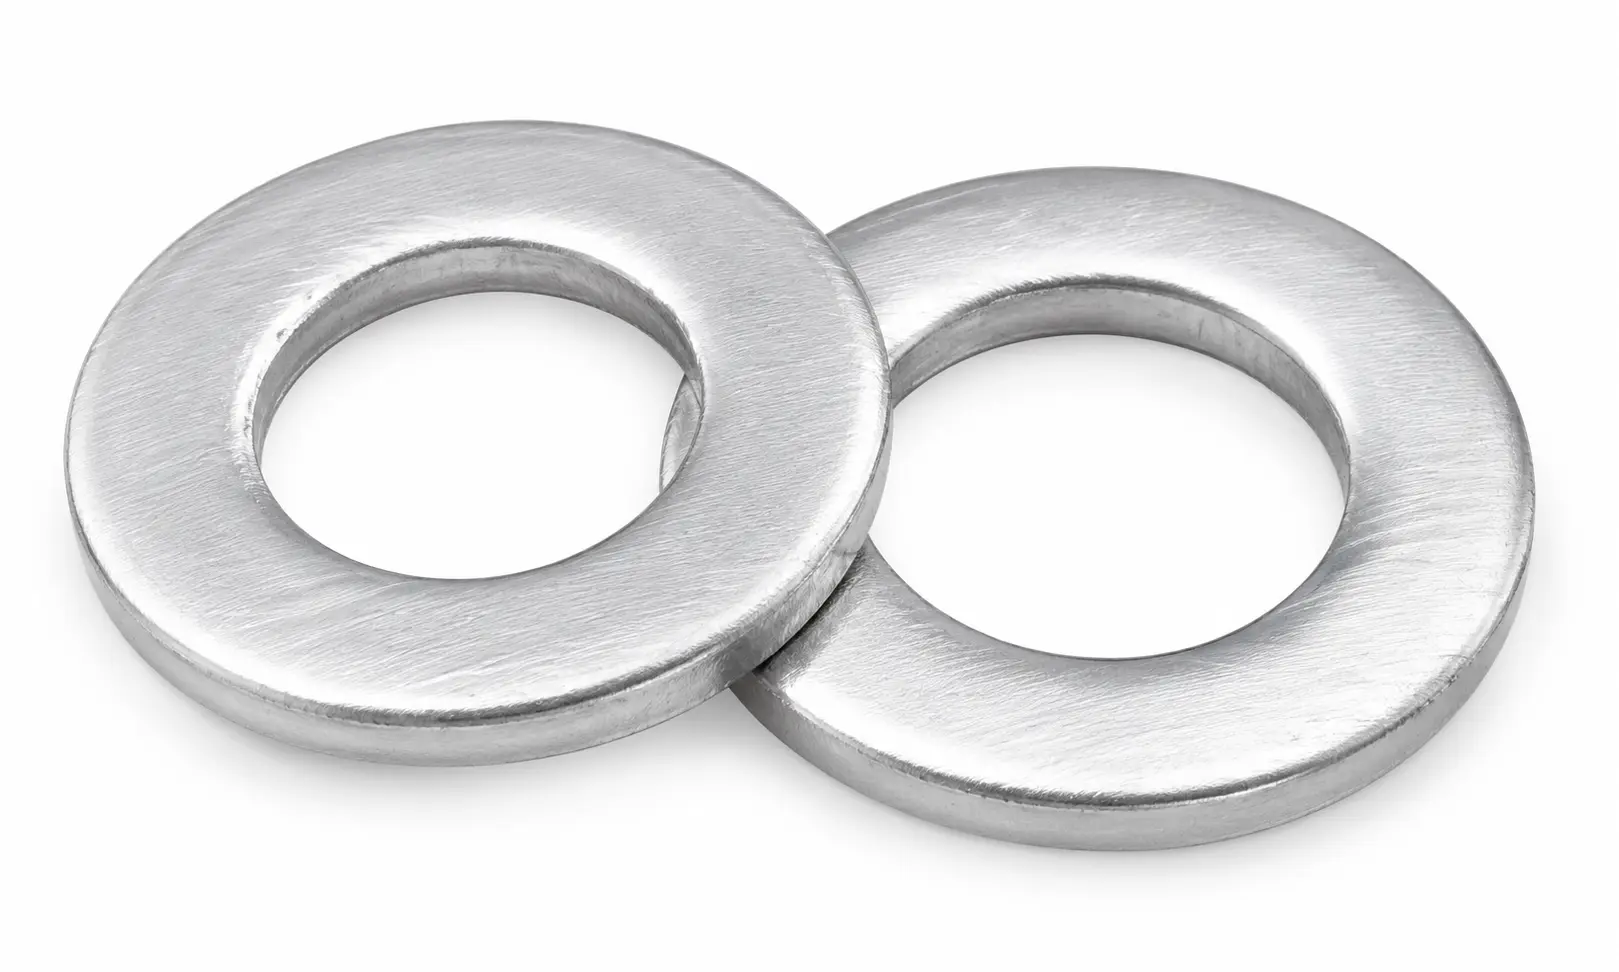
Aluminium 5083 Washers
Aluminium 5083
Washers
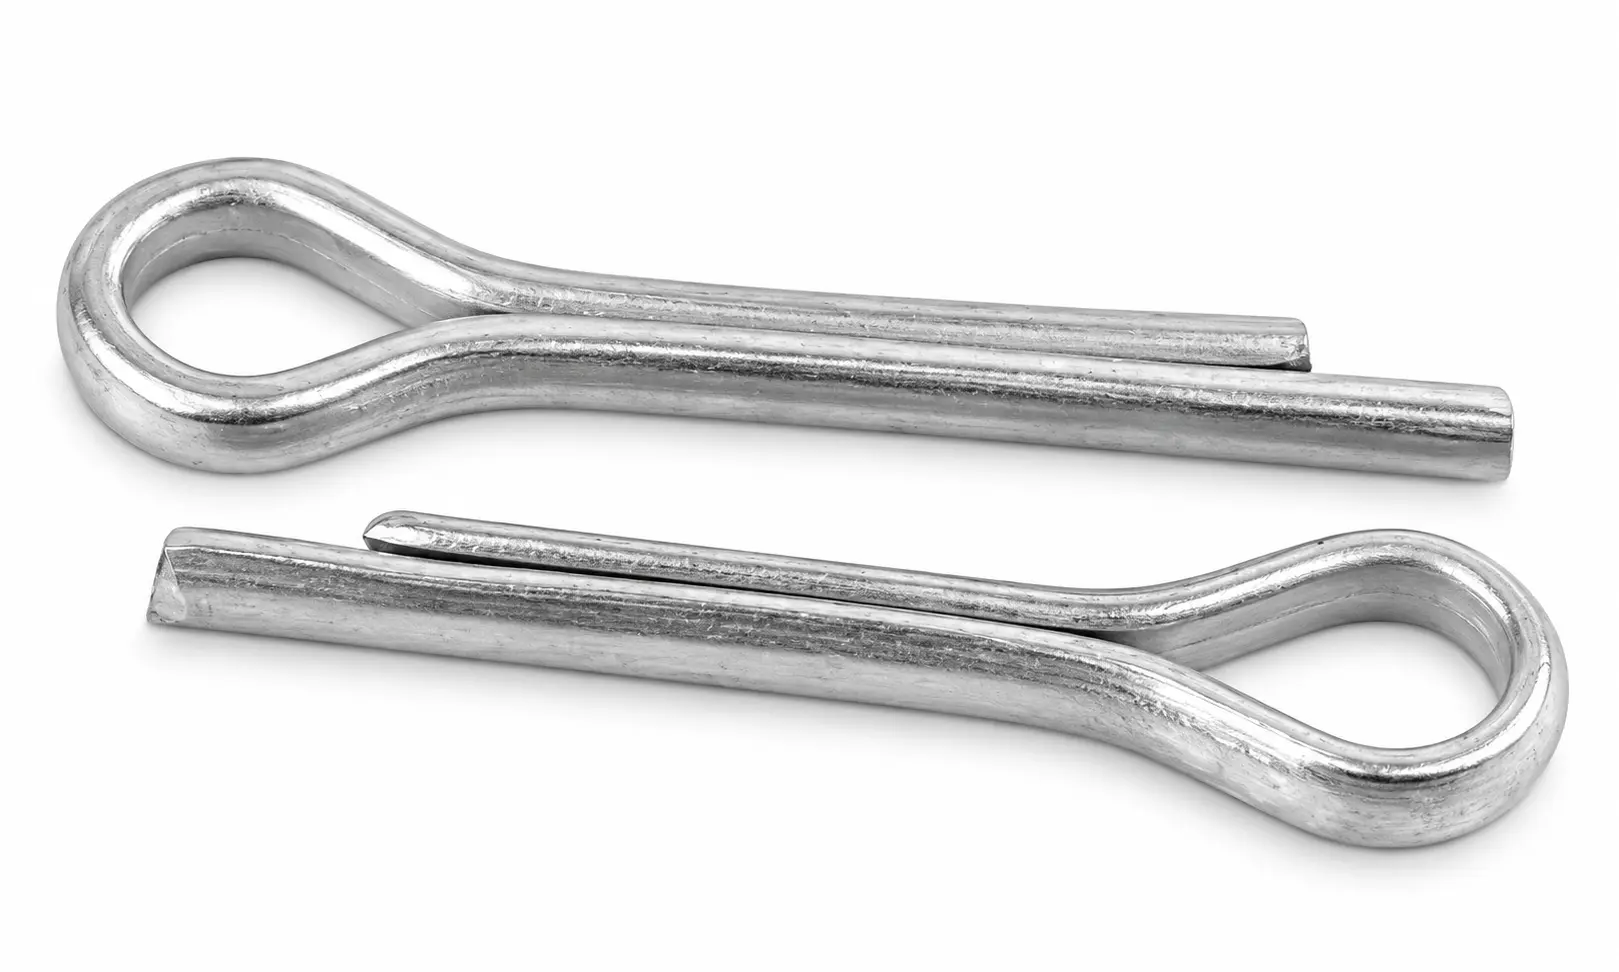
Aluminium 5083 Cotter Pins
Aluminium 5083
Cotter Pins
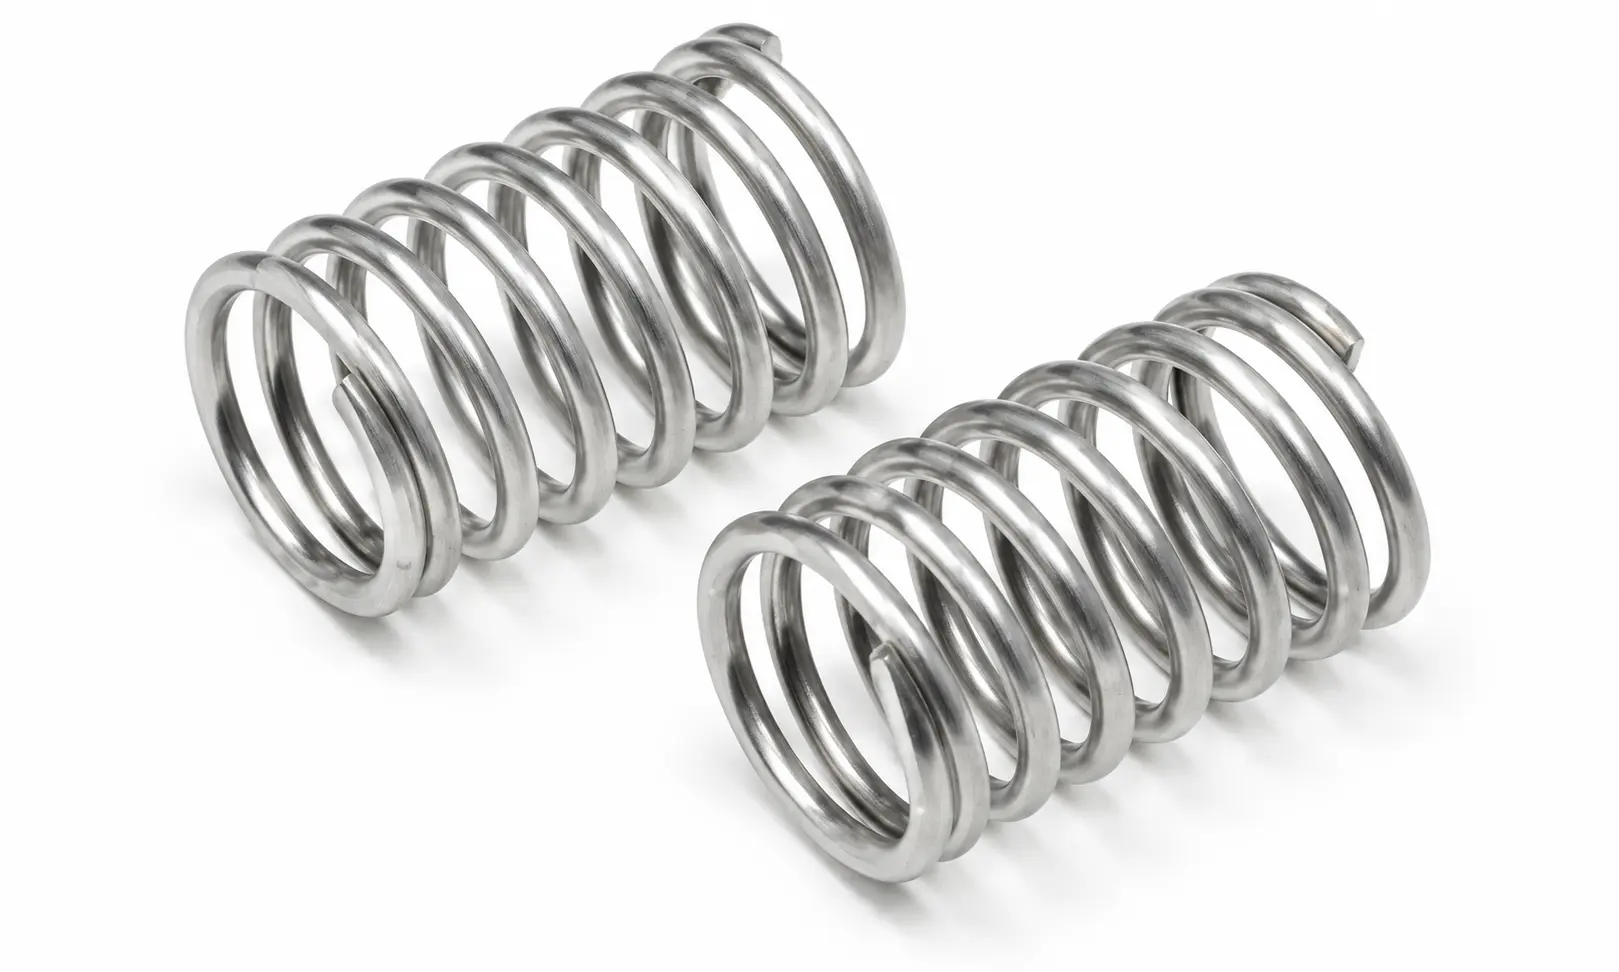
Aluminium 5083 Springs
Aluminium 5083
Springs
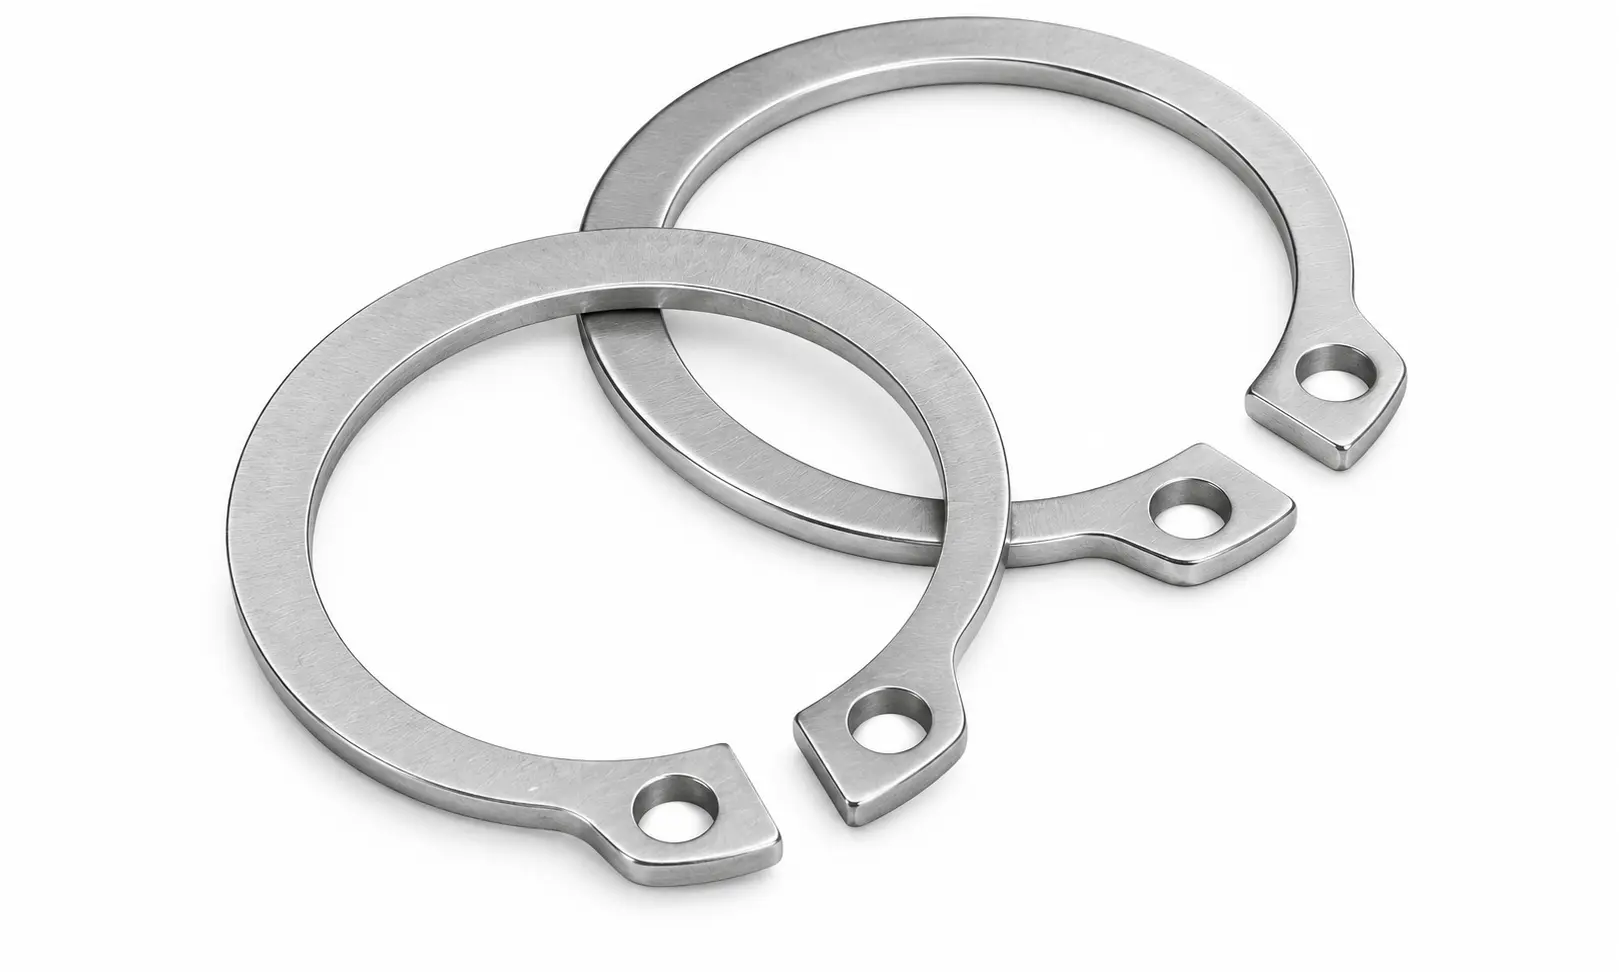
Aluminium 5083 Circlips
Aluminium 5083
Circlips
Aluminium 5083 Coated Fasteners
Aluminium 5083
Coated Fasteners
Aluminium 5083 Custom Spacers
Aluminium 5083
Custom Spacers
Technical Data

Aluminium 5083 Specifications

Chemical Composition — Aluminium 5083 (wt. %)
ElementMinimum %Maximum %
Silicon (Si)—0.40
Iron (Fe)—0.40
Copper (Cu)—0.10
Manganese (Mn)0.401.0
Magnesium (Mg)4.04.9
Chromium (Cr)0.050.25
Zinc (Zn)—0.25
Titanium (Ti)—0.15
Other elements, each—0.05
Other elements, total—0.15
Aluminium (Al)Remainder—
Mechanical Properties — Aluminium 5083
ConditionUTS (MPa)YS 0.2% (MPa)Elongation (%)Hardness
Sheet & plate 1.20–40 mm, O (B209M)275–350125–20016—
Plate 40–80 mm, O (B209M)270–345115–20014—
Plate 6.30–12.50 mm, H112 (B209M)275 min12512—
Plate 12.50–40 mm, H112 (B209M)275 min12510—
Plate 5.00–12.50 mm, H32 (B209M)305–38521512—
Plate 40–80 mm, H32 (B209M)285–38520010—
Physical Properties
Density2.66 g/cm³
Alloy Series5xxx — aluminium-magnesium
Principal Alloying AdditionMagnesium
Heat TreatableNo — strain hardened only
Modulus of Elasticity69 GPa (nominal, wrought aluminium)
Coefficient of Thermal Expansionapprox. 23.6 × 10⁻⁶ /°C (20–100 °C)
Melting Point of Pure Aluminium660 °C — alloys melt over a lower range
Crystal StructureFace-centred cubic (FCC) — no ductile-to-brittle transition
Magnetic ResponseNon-magnetic; non-sparking
Maximum Sustained Service Temperature65 °C — sensitisation limit
Cryogenic ServiceSuitable to liquid-helium temperature; toughness increases as temperature falls
Conductivity NoteElectrical and thermal conductivity in aluminium are strongly temper- and alloy-dependent; certified values for the supplied temper are available on request.
Equivalent Grades & Standards
UNSEN / ISO DesignationPrincipal AdditionCommon Name
A95083 EN AW-5083 / AlMg4.5Mn0.7 Magnesium Aluminium 5083

Key Specifications: ASTM B209/B209M (Sheet & Plate) / ASTM B211 (Rolled or Cold-Finished Bar, Rod & Wire) / ASTM B221 (Extruded Bars, Rods, Wire, Profiles & Tubes) / EN 485-2 / EN 573-3 (Chemical Composition) / Aluminum Association Teal Sheets. ASTM B928 (High-Magnesium Sheet & Plate for Marine Service) / ASTM G66 and G67 (Exfoliation and Intergranular Corrosion Testing).

For marine service specify the H116 or H321 tempers, which are produced and tested specifically for exfoliation resistance under ASTM B928 with mandatory G66 and G67 testing.

Note on fastener standards: ASTM F468 and F467 cover only aluminium alloys 2024-T4, 6061-T6 and 7075-T73. Fasteners in this alloy are manufactured to the composition and temper requirements of the mill product standards above, with thread conformance to the applicable ASME or ISO standard and acceptance criteria agreed on the order.

Every aluminium order ships with EN 10204 3.1 certification giving the heat analysis against the Aluminum Association composition limits, the temper, and the mechanical test results for the product form, section and orientation supplied. Because temper governs properties in this material, the certificate states the temper explicitly and the test results correspond to it. Positive material identification, conductivity testing as a temper check, anodising, chromate conversion coating and exfoliation testing to ASTM G66 or G67 can all be added at order stage.

Machining: aluminium cuts fast but not always cleanly, and the behaviour varies sharply by series. The soft 1xxx, 3xxx and 5xxx alloys and the annealed tempers are gummy — they smear, build up on the cutting edge and tear rather than shear, giving poor finish and oversize holes. The harder heat-treated tempers of the 2xxx, 6xxx and 7xxx series machine very well by comparison, with 2024-T351, 6061-T6 and 7075-T651 all being everyday CNC materials. The outright free-machining choice is 2011, whose bismuth and lead additions break the chip mechanically and make it the standard screw-machine aluminium. General practice across the family is high surface speed, sharp polished high-rake tooling, generous chip clearance, and a lubricant rather than plain coolant to prevent built-up edge; uncoated carbide or polished-flute tooling is usual, and aluminium-specific geometry matters more than cutting speed.

Forming: aluminium cold forms well in the annealed and low tempers and poorly in the hard ones, and the relationship is direct — the higher the temper, the lower the formability. Parts are therefore normally formed in O, T4 or a low H temper and then aged or work hardened to the final condition. Cold heading and thread rolling are the preferred routes for aluminium fasteners, both for the grain flow and because rolled threads are significantly stronger than cut ones in a material this soft. The heat-treatable alloys in the naturally ageing T4 condition have a limited working window after solution treatment, which is why aircraft rivets in 2024 are stored refrigerated to suppress ageing until they are driven.

Weldability splits along the same lines as everything else in aluminium. The 1xxx, 3xxx, 5xxx and 6xxx alloys are readily arc weldable by GTAW and GMAW. The 2xxx and 7xxx alloys, with the notable exception of 2219, are generally considered unweldable by fusion processes — they are highly susceptible to hot cracking in the weld and heat-affected zone, and welded joints in 2024 or 7075 lose a large fraction of their strength besides. Those alloys are joined mechanically, by riveting, bolting or adhesive bonding, or by friction stir welding where the geometry allows it. Filler selection matters: 4043 or 5356 for the 6xxx alloys, 5356 or 5183 for the 5xxx.

Heat-affected zone softening is the issue even on the weldable alloys. Welding a 6061-T6 part locally destroys the T6 temper and leaves the heat-affected zone at something closer to T4 strength, and a welded 6061 structure must be designed on that reduced value rather than on parent-metal properties unless the whole assembly is re-solution-treated and re-aged. In the strain-hardened 5xxx and 3xxx alloys the weld zone reverts towards the annealed O condition for the same reason, and cannot be restored by heat treatment at all. Aluminium's high thermal conductivity also means welding demands much more heat input than the equivalent steel joint, and the tenacious oxide film — which melts at around 2050 °C against the metal's 650 °C — must be removed by AC cleaning action or mechanical means or it will trap inclusions in the weld.

Heat treatment: this alloy is not heat treatable. No precipitation reaction is available, so strength comes only from cold work and is set by the H temper; the only thermal treatment that changes properties is annealing, carried out at approximately 345 °C for a full anneal to the O temper, with partial anneals used to establish the intermediate H2x tempers and stabilising treatments for the H3x tempers. The important practical consequence is that cold-worked strength is removed permanently by heat — a weld, a brazing cycle or prolonged warm service will locally anneal the material back towards the O condition, and no subsequent heat treatment will restore it. Design welded structures in these alloys on annealed properties in the heat-affected zone.

The single most important division in aluminium is heat-treatable against non-heat-treatable. The 1xxx, 3xxx and 5xxx series are non-heat-treatable: they contain no element that will precipitation harden, so the only way to strengthen them is cold work, and the only way to soften them is annealing. Their strength is set by the H temper. The 2xxx, 6xxx and 7xxx series are heat-treatable: copper, magnesium-silicide and zinc-magnesium respectively form coherent precipitates when the alloy is solution treated, quenched and then aged, and that precipitation is what produces the strength. Their strength is set by the T temper. The practical consequences run right through fabrication: a non-heat-treatable alloy cannot be restored to full strength after welding, because its strength came from cold work that the weld heat removed; a heat-treatable alloy can be re-solution-treated and re-aged, though rarely economically on a large weldment.

Aluminium is protected by a tough, instantly self-healing oxide film, and it is at its best in the neutral range. The film forms in milliseconds on exposed metal and is what gives aluminium its genuinely excellent atmospheric and marine durability — architectural and marine aluminium lasts decades with no coating. The film is stable from roughly pH 4 to pH 9, and outside that window aluminium is amphoteric: it is attacked by strong acids and, more aggressively still, by strong alkalis. Sodium hydroxide dissolves it rapidly, which is why aluminium must never be used for caustic service and why alkaline cleaners attack aluminium parts. Wet cement, lime and uncured concrete are alkaline enough to etch it. It resists most organic compounds, dry gases and the great majority of foodstuffs, and it is non-toxic and non-sparking.

Corrosion resistance varies enormously across the series, and it tracks copper content. The 1xxx, 3xxx, 5xxx and 6xxx alloys have good to excellent resistance, with the 5xxx magnesium alloys the best of all in seawater. The 2xxx and 7xxx alloys are the problem: the copper that gives them their strength also makes them markedly less corrosion resistant than any other aluminium, prone to pitting and to intergranular attack. That is precisely why Alclad exists — a thin layer of pure or 7072 aluminium roll-bonded to each face of a 2024 or 7075 core, which is anodic to the core and protects it sacrificially. Where a 2xxx or 7xxx part will see a corrosive environment, specify Alclad material, anodising, or a primer and paint system; bare 2024 and 7075 should not be left exposed.

5083 is the premier marine structural aluminium, with exceptional resistance to seawater, salt spray and industrial atmospheres, and it retains that resistance in the as-welded condition. It is the standard material for aluminium hulls, superstructures and offshore accommodation modules.

5xxx alloys with more than about 3% magnesium sensitise, and this is the limit that catches out marine designers. Above roughly 65 °C in sustained service, magnesium in excess of its solubility precipitates as the β-phase Al₃Mg₂ along the grain boundaries. That phase is strongly anodic to the surrounding metal, so the sensitised alloy becomes susceptible to intergranular corrosion and intergranular stress-corrosion cracking, and the damage accumulates with time at temperature. It is a well-documented cause of cracking in aluminium hulls and superstructures that have spent years in warm service. The practical rule is that 5083 and the other high-magnesium 5xxx alloys must not be used in sustained service above 65 °C. Where elevated temperature is unavoidable, specify a lower-magnesium alloy such as 5052, or the H116 and H321 tempers, which are produced and tested specifically for exfoliation-resistant marine service under ASTM G66 and G67.

Aluminium is anodic, and this reverses everything that applies to the other corrosion-resistant metals. Copper, titanium, zirconium and tantalum fasteners are all galvanically noble — they survive and drive corrosion of whatever they are bolted into. Aluminium is the opposite. It sits near the active end of the galvanic series, below carbon steel and far below stainless steel, copper and the nickel alloys, so in a mixed-metal joint the aluminium is the part that dissolves. The geometry makes it worse rather than better: a small aluminium fastener clamping a large stainless or steel assembly is a small anode against a large cathode, which is the most damaging configuration there is, and the fastener can be consumed while the structure around it is untouched.

An aluminium bolt in a stainless or steel joint, wet, will fail. Copper is the worst partner of all — even trace copper dissolved in water and redeposited on aluminium will initiate pitting, which is why aluminium should not be plumbed downstream of copper. The mitigations are insulating washers, sleeves and gaskets so no electrical circuit exists; a barrier coating or sealant at the faying surface; cadmium, zinc or aluminium-pigmented coatings on the steel part to bring it closer to aluminium's potential; and anodising, which is particularly effective here because the anodic film is an electrical insulator as well as a corrosion barrier. Where a steel fastener must be used in aluminium structure, specify it hot-dip galvanised, aluminium-coated or 300-series stainless with an isolating washer — never bare carbon steel.

Aluminium loses strength quickly with temperature and has essentially no useful creep strength above about 150 °C. This is a hard limit on the whole family and it is often underestimated, because the loss is not linear: a 6061-T6 part retains most of its strength to 100 °C, has lost a substantial fraction by 200 °C, and is structurally useless by 300 °C. Worse, the loss in the heat-treatable alloys is permanent, because time at temperature over-ages the precipitate structure that was providing the strength — the part does not recover when it cools. Aluminium bolting in anything that runs warm must be assessed at service temperature and not at room temperature, and prolonged exposure above roughly 120 °C should be treated as a design issue rather than a detail. Conversely aluminium is excellent at low temperature: it has a face-centred-cubic structure with no ductile-to-brittle transition, and both strength and toughness increase as temperature falls, which is why 5083 is a standard cryogenic tank material down to liquid-helium temperatures.

With aluminium the temper matters as much as the alloy, and quoting one without the other is meaningless. The same alloy can differ in strength by a factor of three between tempers, so “6061” on a drawing is an incomplete specification — it must be 6061-T6, or 6061-T4, or 6061-O. The designation system under ANSI H35.1 runs as follows. F is as-fabricated and O is annealed, the softest and most formable condition. H tempers are strain hardened and apply to the non-heat-treatable alloys: H1x is strain hardened only, H2x is strain hardened then partially annealed, H3x is strain hardened then stabilised, and the second digit gives the degree — 2 is quarter hard, 4 half hard, 6 three-quarter hard, 8 full hard and 9 extra hard. T tempers are thermally treated and apply to the heat-treatable alloys: T4 is solution heat treated and naturally aged, T6 solution heat treated and artificially aged to peak strength, T3 solution treated, cold worked and naturally aged, and T8 solution treated, cold worked and artificially aged. The T7x series is deliberately over-aged past peak strength — T73, T7351 and T76 exist specifically to buy stress-corrosion resistance at the cost of about 10 to 15% of the strength, which is why they dominate thick-section 7xxx work. A trailing 51, as in T351, T651 and T7351, means the product was stress relieved by controlled stretching after solution treatment, which matters greatly for parts that will be heavily machined.

ASTM F468 and F467 cover exactly three aluminium alloys: 2024-T4, 6061-T6 and 7075-T73. Those are the only aluminium alloys for which a certified nonferrous bolt, hex cap screw, stud or nut standard exists, and the specified conditions are part of the designation — F468 will not accept 7075-T6 for the stress-corrosion reasons described below. The F468 strength requirements put aluminium fasteners in perspective: 6061-T6 is 255–359 MPa full-size tensile, 2024-T4 is 379–483 MPa and 7075-T73 is 421–524 MPa, against 830 MPa for an ordinary ASTM A325 structural steel bolt and 1040 MPa for property class 10.9. Even the strongest aluminium bolt is roughly half the strength of a plain structural steel one, at about a third of the density.

Aluminium is chosen for weight, conductivity, non-magnetic behaviour and corrosion resistance — not for load. Three further practical points follow. Aluminium threads gall and seize readily, so an anti-seize compound or dry-film lubricant is standard practice and an aluminium nut on an aluminium bolt is poor practice. Aluminium threads also strip easily — a tapped hole in aluminium needs roughly twice the thread engagement of a steel one, or a steel threaded insert. And aluminium has low bearing strength under the head, so wide flange heads or large washers are needed to avoid embedment and the preload loss that follows. Torque figures for steel fasteners must never be carried across to aluminium ones.

Anodising is the standard surface treatment and it does several jobs at once. The process grows a controlled, thick, integral aluminium oxide layer that is far more protective than the natural film: sulfuric acid anodising for general corrosion protection and for colour, and hard anodising for a thick, very wear-resistant layer. For fasteners three points matter. First, the anodic film is an electrical insulator, which makes anodising an effective galvanic isolation measure in its own right — but by the same token an anodised fastener will not provide an earth path or electrical bonding, which is a common and awkward surprise. Second, the film grows outward as well as inward and adds meaningfully to thread dimensions, so anodised threads must be cut or rolled to allow for the coating thickness or they will not assemble. Third, anodising quality is alloy-dependent: the 5xxx and 6xxx alloys anodise beautifully and give clear, consistent films, while the high-copper 2xxx alloys anodise poorly and give patchy, less protective and discoloured coatings. Chromate and chromate-free conversion coatings are the alternative where electrical conductivity must be retained.

How the series divide. The first digit of the designation names the principal alloying element, and it tells you most of what you need to know. 1xxx — 1050, 1060, 1070, 1080, 1100 and 1145 — is 99% or purer aluminium, bought for electrical and thermal conductivity, corrosion resistance and formability, not strength. 2xxx is aluminium-copper, heat treatable to high strength with poor corrosion resistance and generally no weldability: 2014, 2017 and 2024 are the aerospace alloys, 2011 is the free-machining one and 2090 the aluminium-lithium. 3xxx — 3003 — is aluminium-manganese, the general-purpose sheet alloy. 5xxx is aluminium-magnesium, the marine and cryogenic family: 5052 for general service and 5083 for the highest strength available without heat treatment. 6xxx is aluminium-magnesium-silicide, the structural and extrusion workhorse combining moderate heat-treatable strength with good corrosion resistance and weldability: 6061, 6063, 6066 and 6082. 7xxx is aluminium-zinc, the highest strength of all and the most SCC-sensitive: 7075 and 7050.
Key Characteristics

  • 4.0–4.9% magnesium — the highest on this hub.
  • Strongest aluminium available without heat treatment.
  • 275–350 MPa specified even in the annealed O temper.
  • Exceptional seawater and marine atmosphere resistance.
  • Retains strength well as welded — no heat treatment to lose.
  • Standard cryogenic alloy — toughness increases as temperature falls.
  • Must not be used above 65 °C sustained — sensitisation risk.
  • Density 2.66 g/cm³ — the lightest alloy on this hub.

Typical Applications

  • Marine structural fasteners and hull fixings.
  • Ship hulls, superstructures and offshore modules.
  • Cryogenic tanks and LNG containment.
  • Pressure vessels and storage tanks.
  • Armoured and ballistic vehicle structure.
  • Rail car and transport structural panels.
  • Chemical and desalination plant equipment.
  • Welded structural fabrications in marine service.