+91 97734 41022 sales@exoticalloy.com
Material Specification

Alloy 28

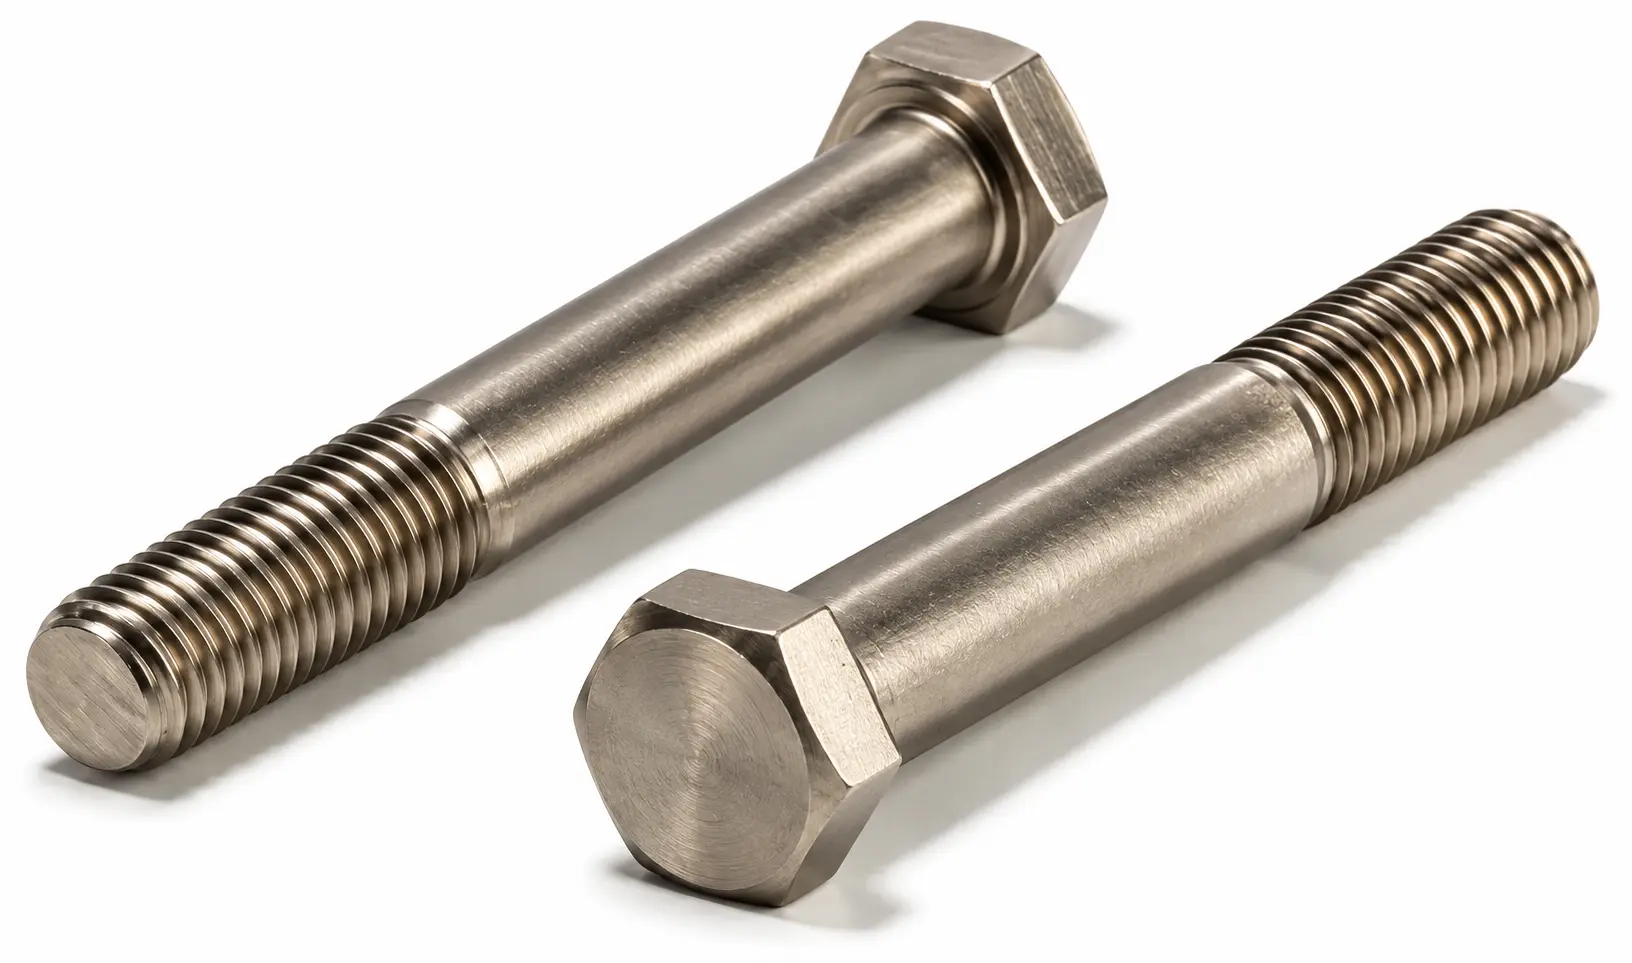
Alloy 28 Fasteners
27Cr-31Ni-3.5Mo-Cu High Alloy Austenitic Stainless Steel – Strong Acid Service

S Alloy 28 (Sanicro 28) Fasteners

Buy S Alloy 28 (Sanicro 28 / Alloy 28 / UNS N08028 / EN 1.4563) bolts, stud bolts, heavy hex nuts, tube, pipe, fittings and custom CNC fasteners from Exotic Alloy. Alloy 28 is a high-alloy multi-purpose austenitic stainless steel carrying nominally 27% chromium, 31% nickel, 3.5% molybdenum and 1% copper with carbon held to 0.020% maximum, giving very high corrosion resistance in strong acids together with excellent resistance to stress-corrosion cracking and intergranular attack.

Exotic Alloy supplies Alloy 28 to ASTM B668 for seamless tube and pipe, ASTM B709 for plate and sheet, EN 10088-3 and EN 10272 for bar and ASTM A403 for fittings, with ASME Boiler and Pressure Vessel Code acceptance under Sections I, III and VIII Division 1, VdTÜV Werkstoffblatt 483, and NACE MR0103 and NACE MR0175 / ISO 15156 qualification for sour service. All material carries EN 10204 3.1 certification.

Request a Quote
Product Range

Alloy 28 Fasteners Available

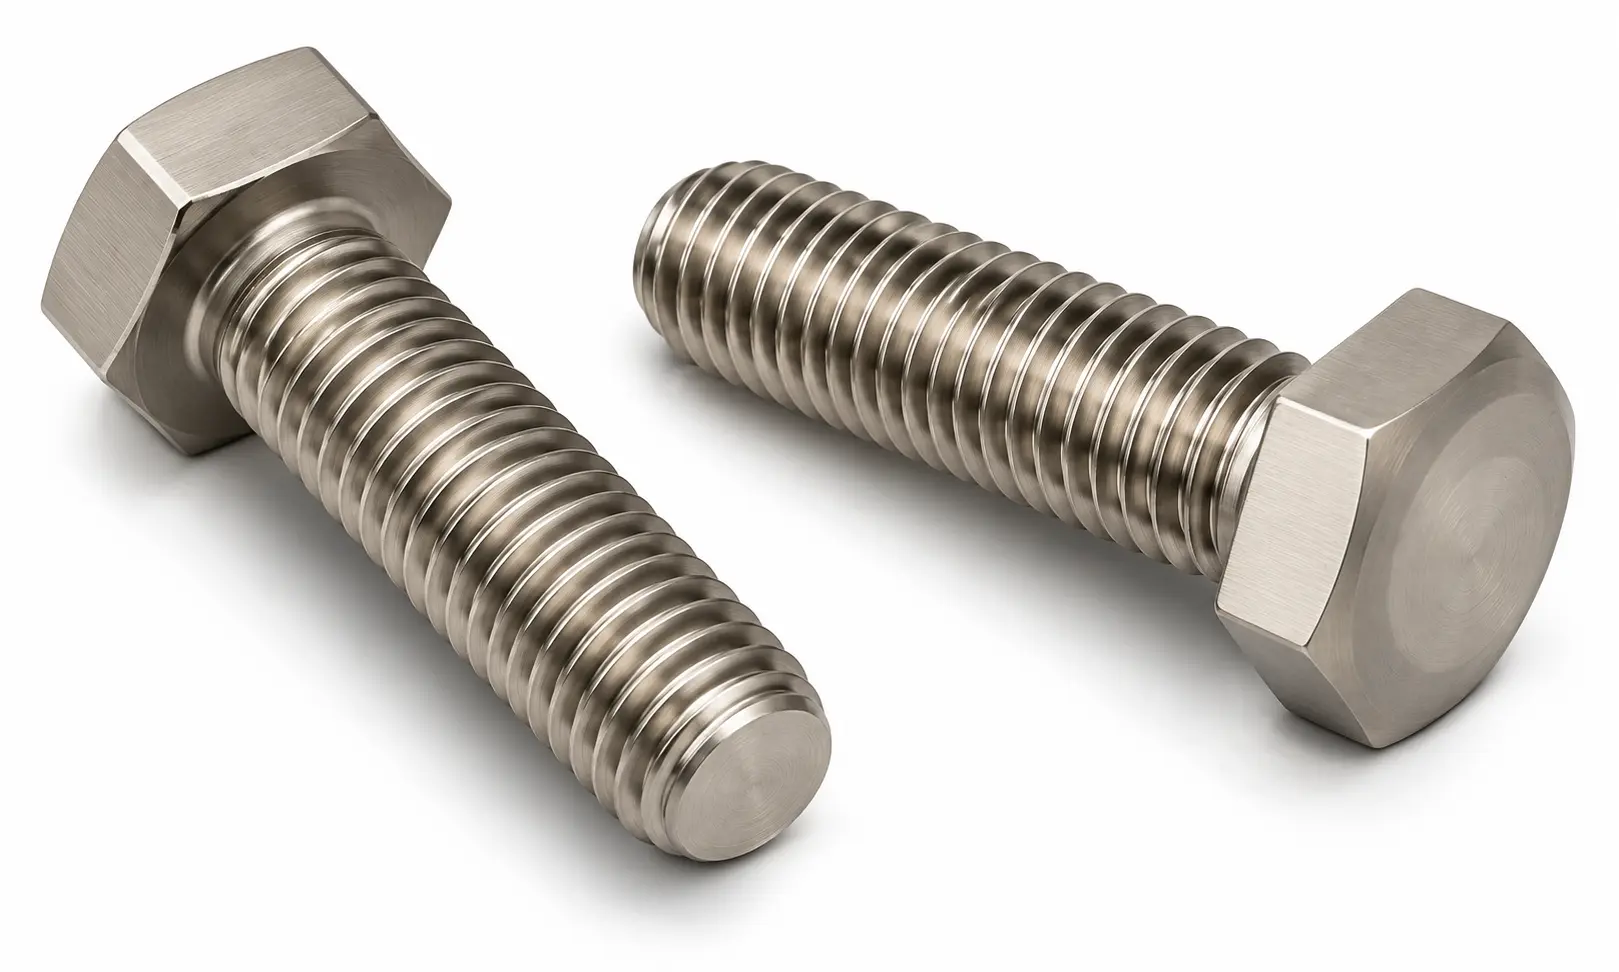
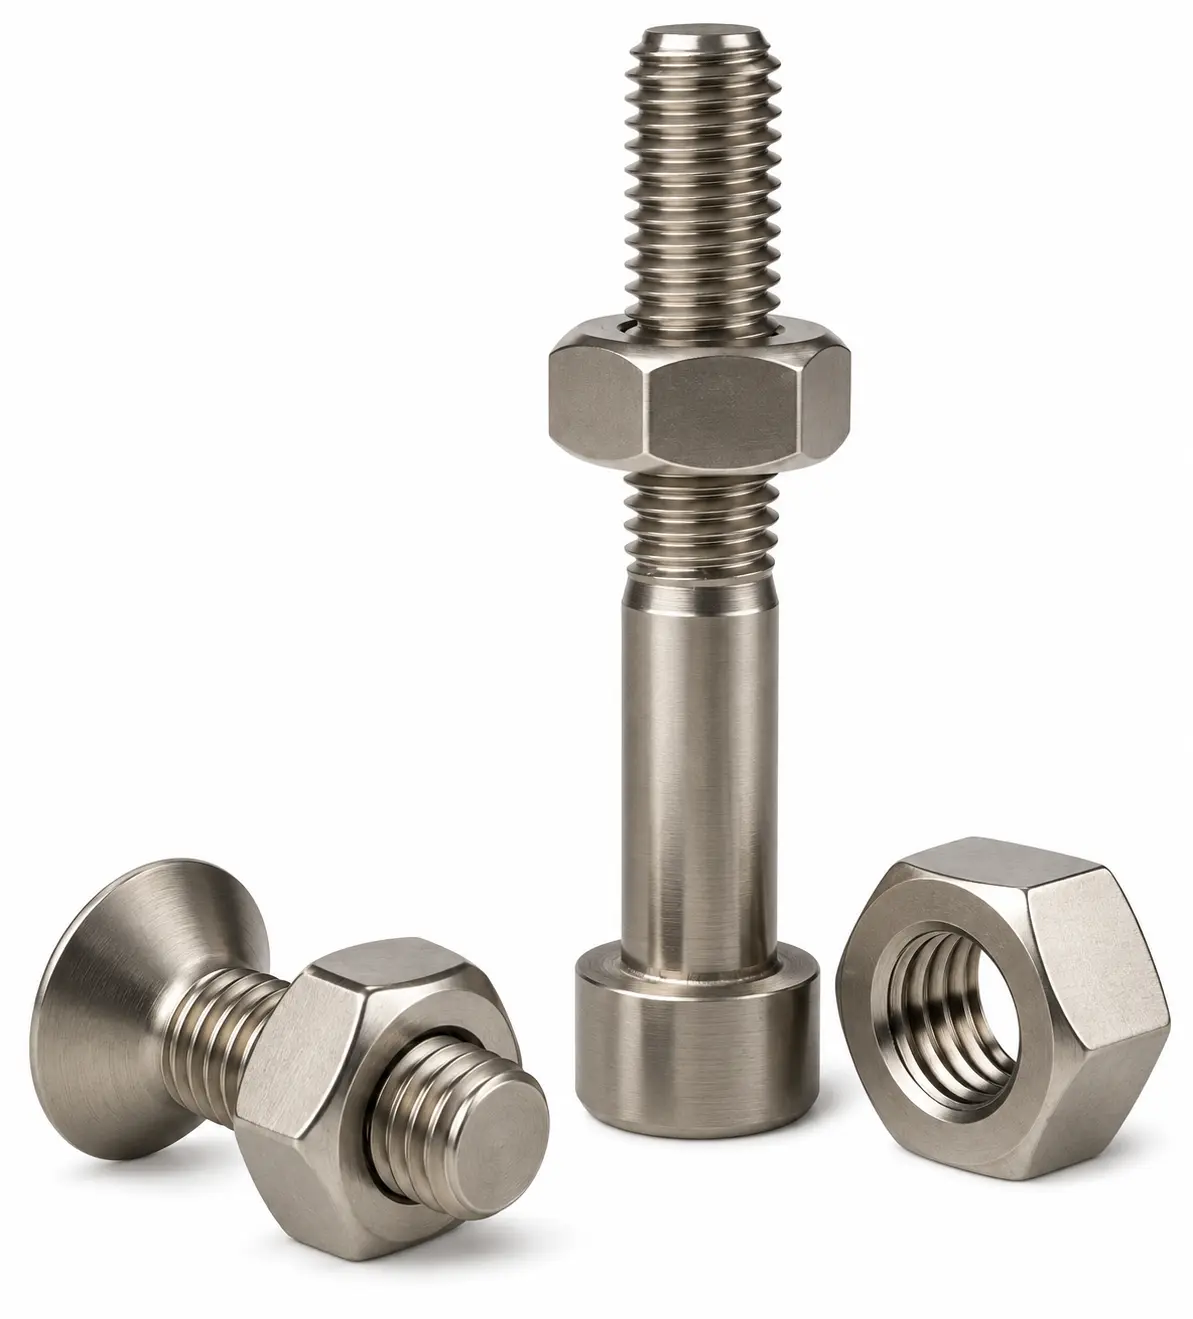
Alloy 28 Hex Bolts
Alloy 28
Hex Bolts
Alloy 28 Heavy Hex Bolts
Alloy 28
Heavy Hex Bolts
Alloy 28 Stud Bolts
Alloy 28
Stud Bolts
Alloy 28 Threaded Rods
Alloy 28
Threaded Rods
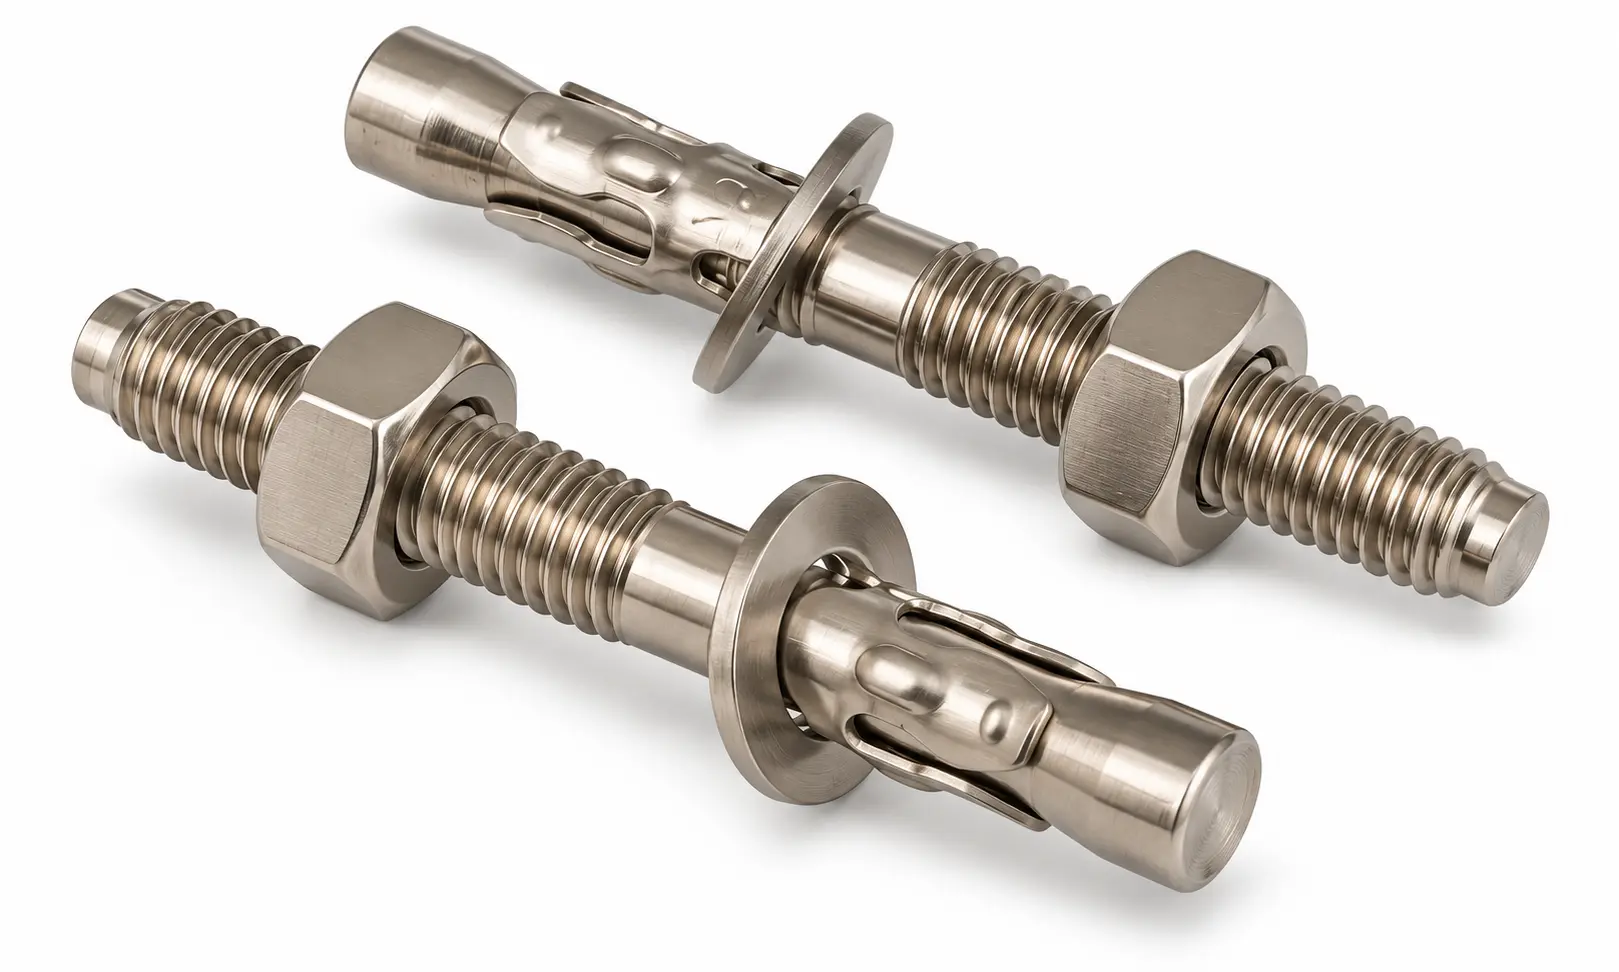
Alloy 28 Anchor Bolts
Alloy 28
Anchor Bolts
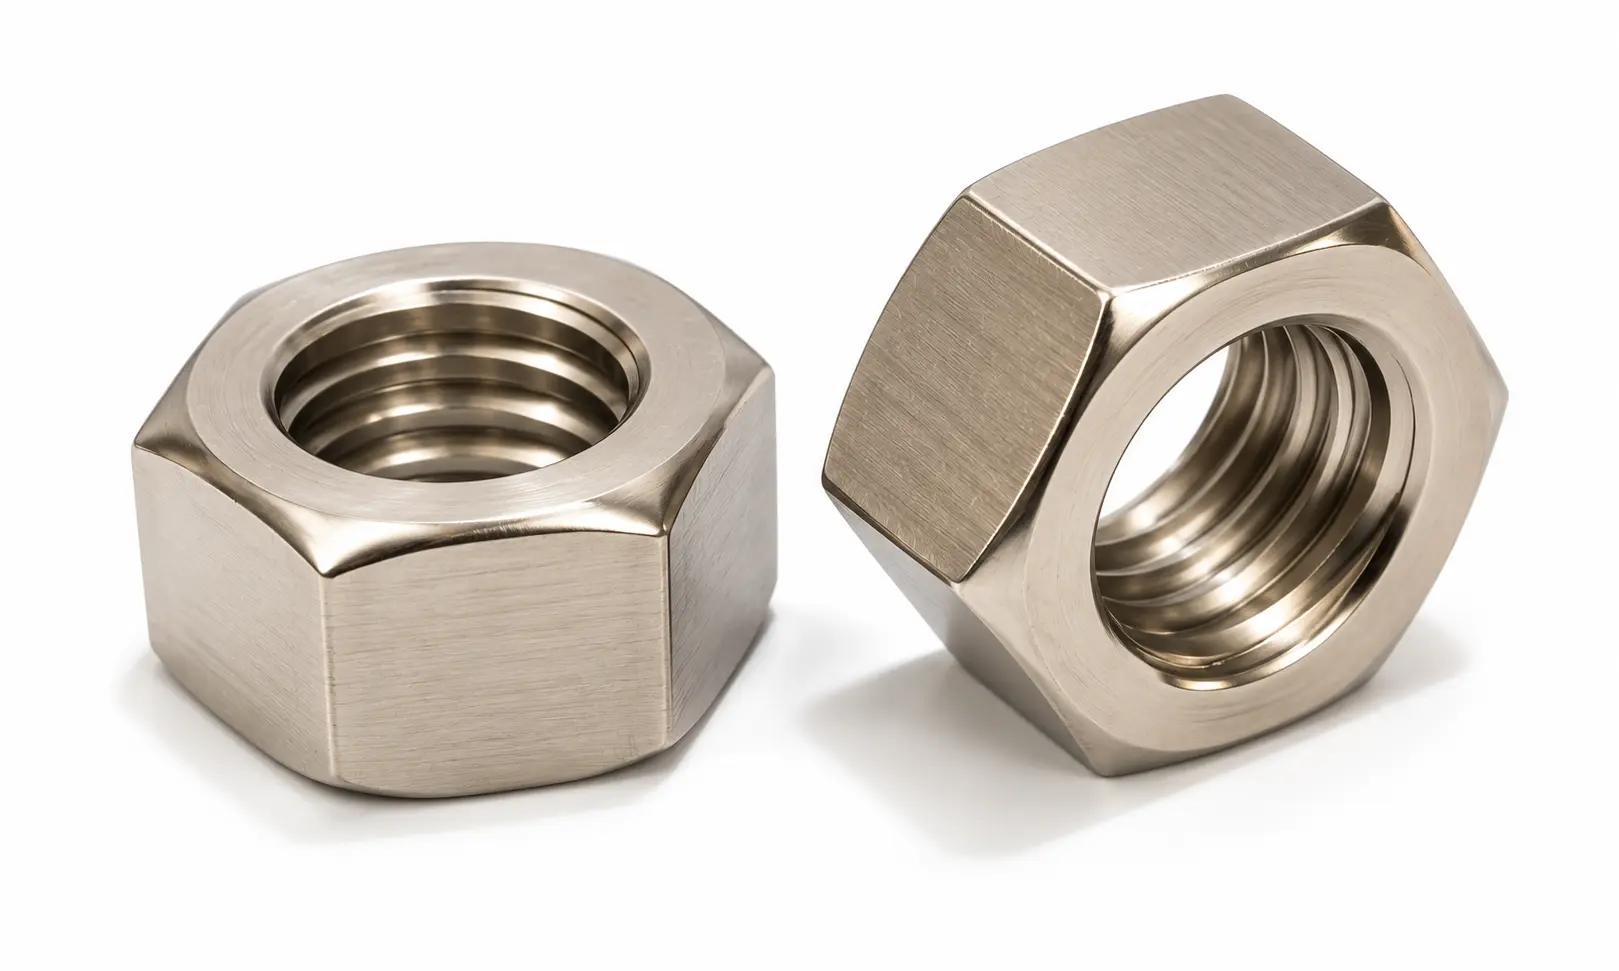
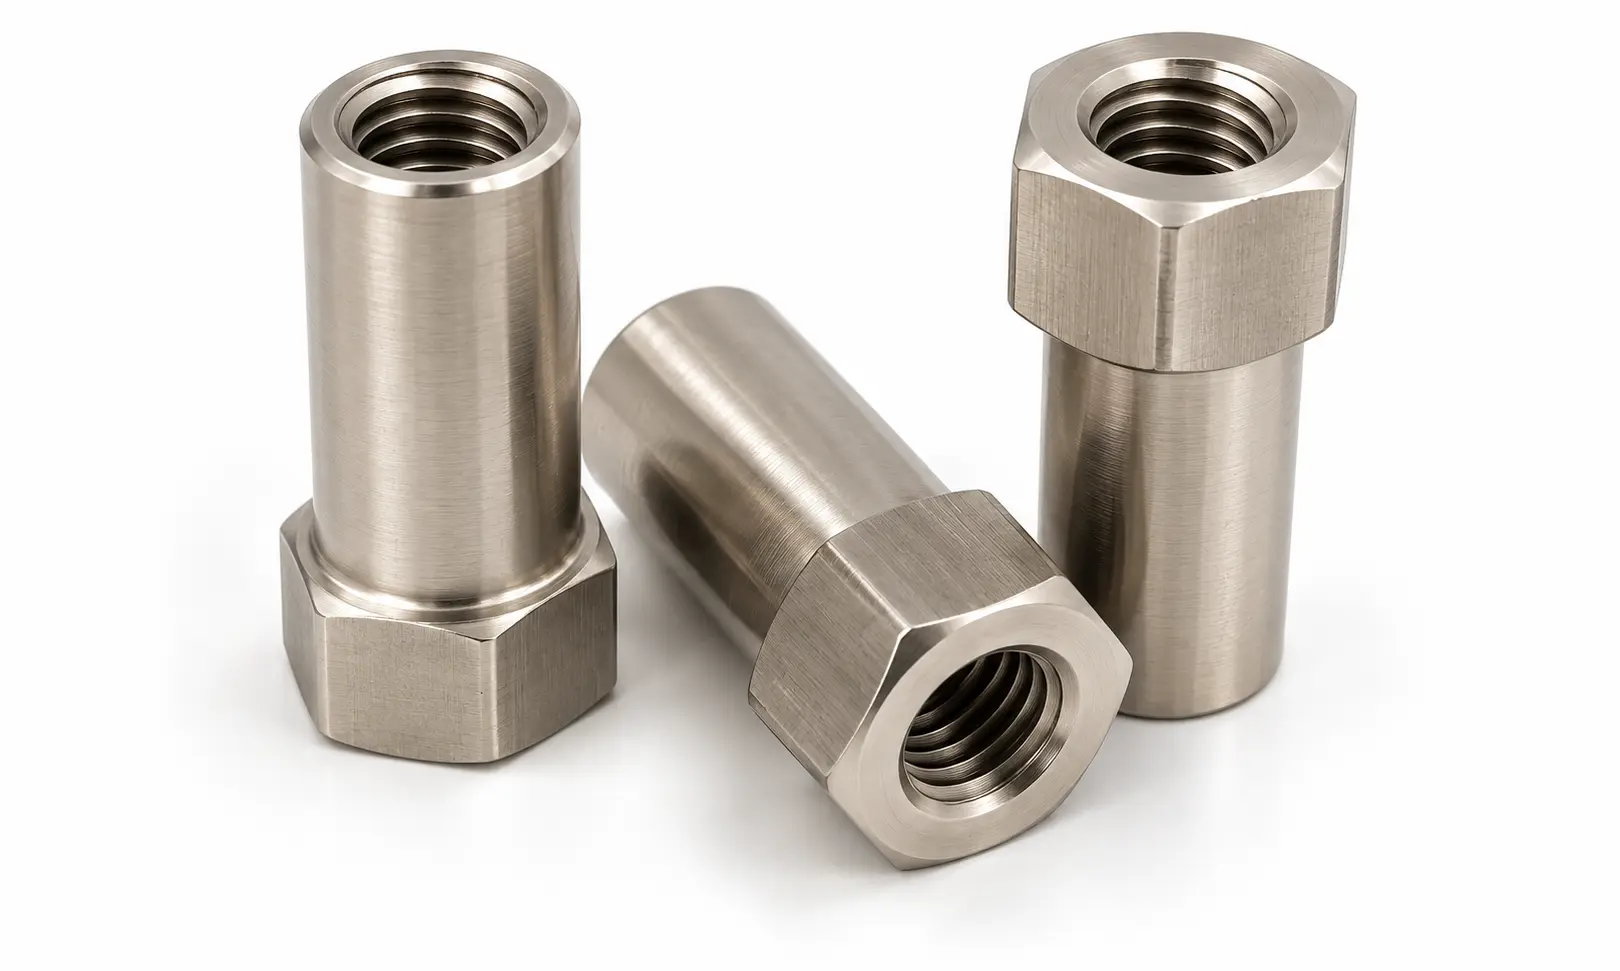
Alloy 28 Hex Nuts
Alloy 28
Hex Nuts
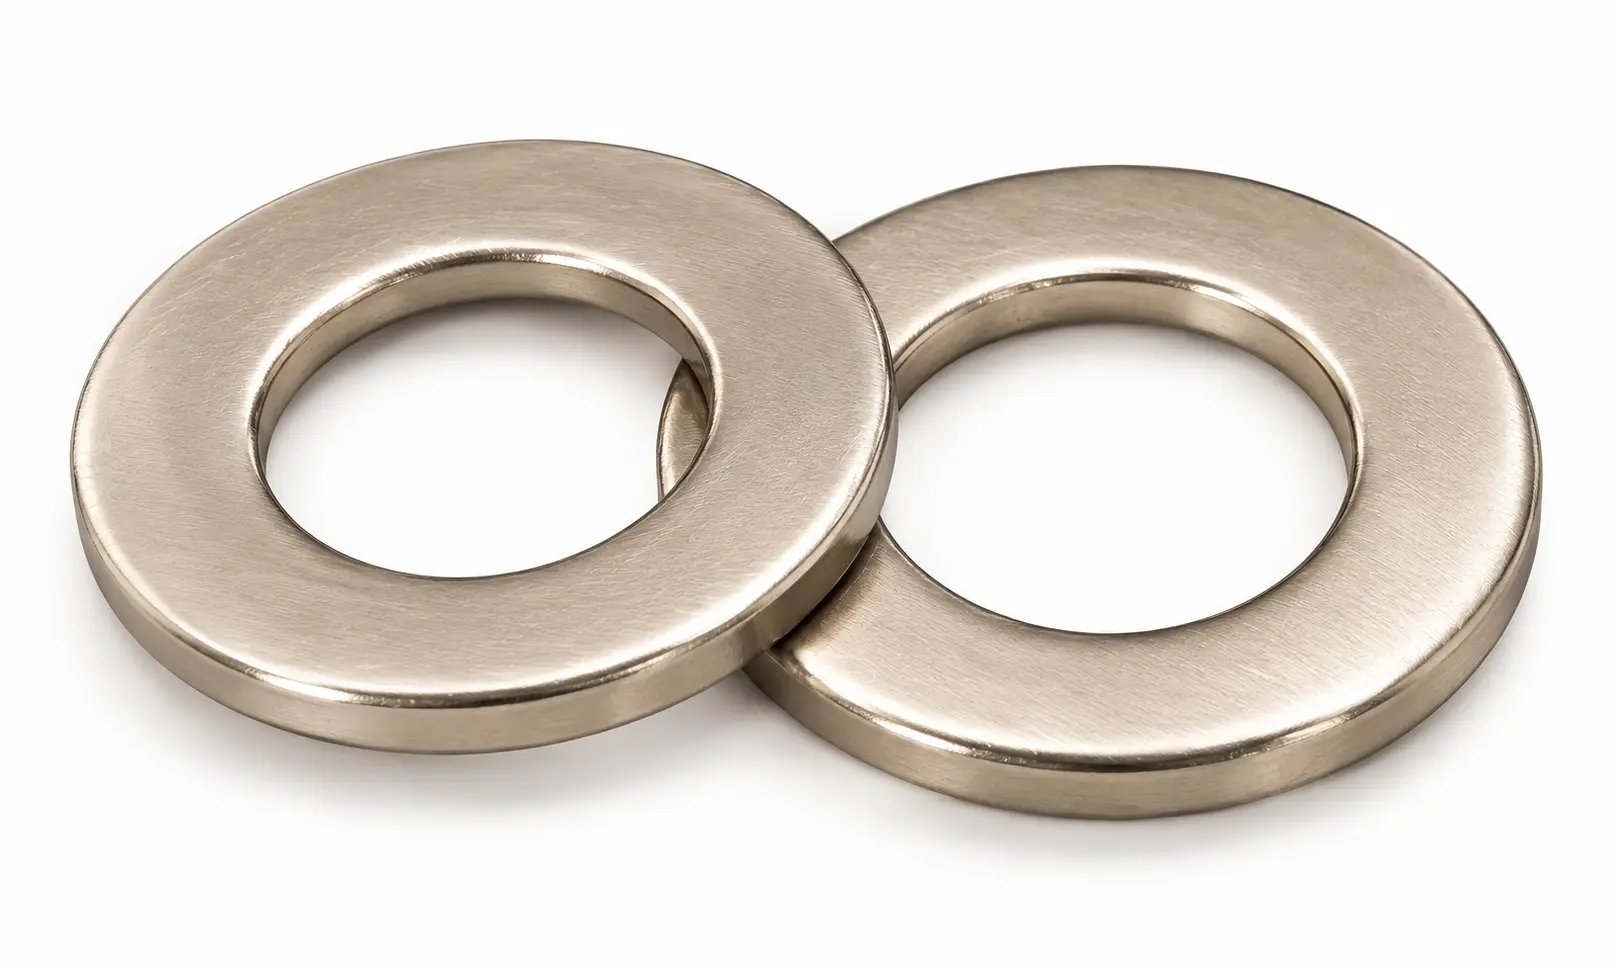
Alloy 28 Washers
Alloy 28
Washers
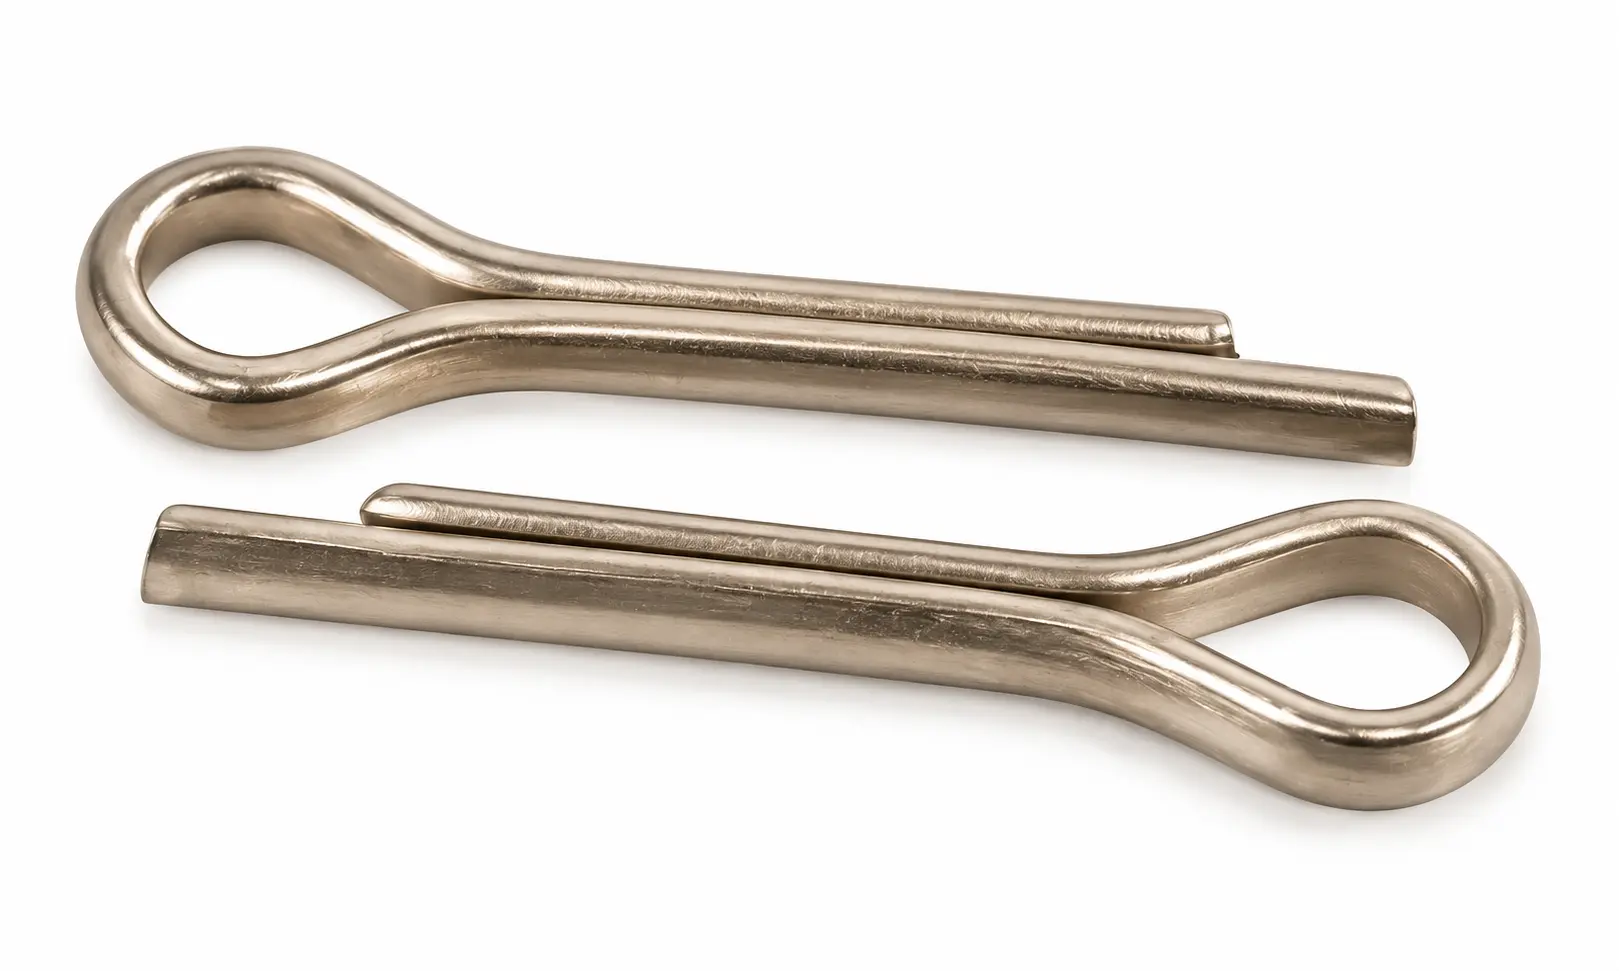
Alloy 28 Cotter Pins
Alloy 28
Cotter Pins
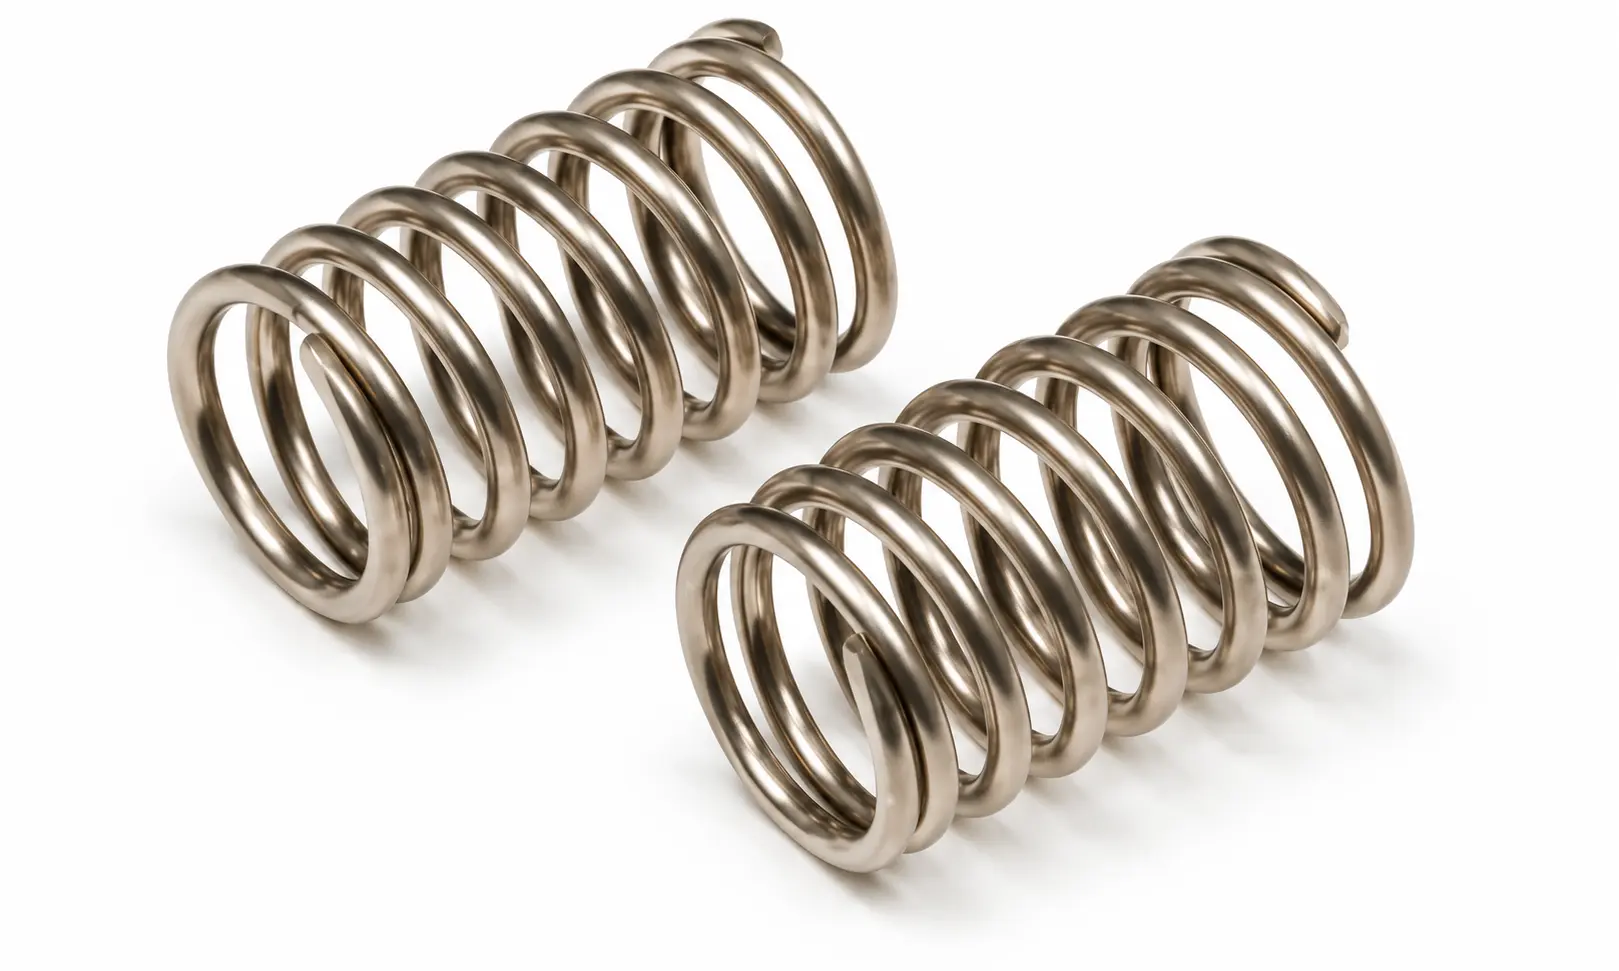
Alloy 28 Springs
Alloy 28
Springs
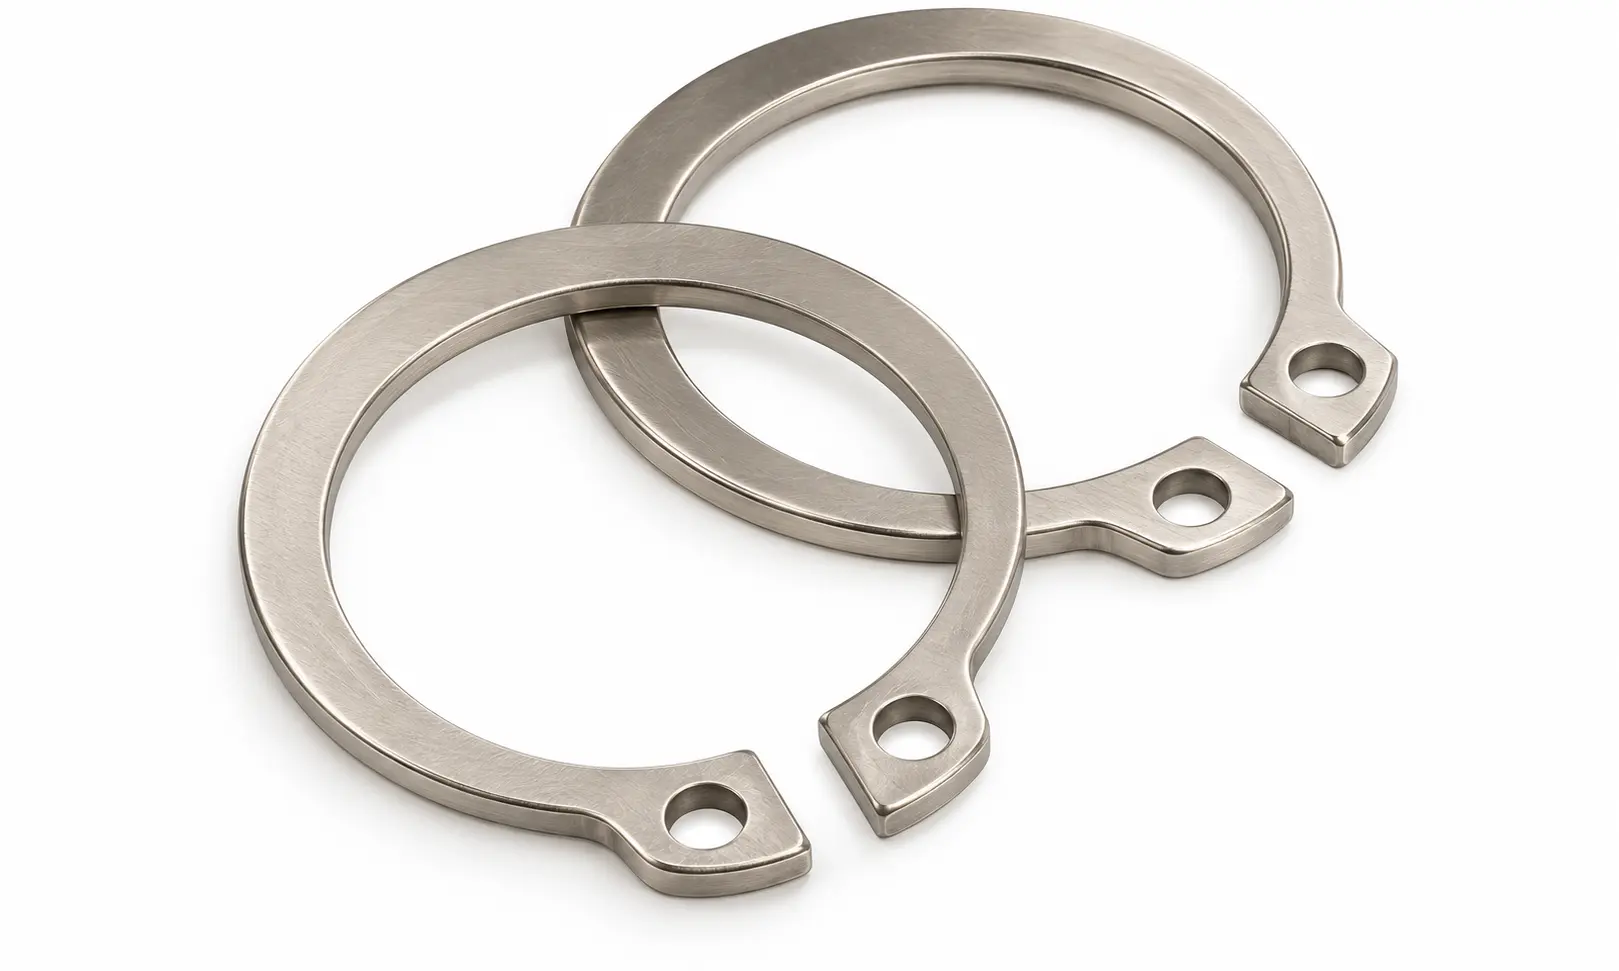
Alloy 28 Circlips
Alloy 28
Circlips
Alloy 28 Coated Fasteners
Alloy 28
Coated Fasteners
Alloy 28 Custom Spacers
Alloy 28
Custom Spacers
Technical Data

Alloy 28 Specifications

Chemical Composition — S Alloy 28 (Sanicro 28) (wt. %)
ElementFeCrNiMoCuMnSiNC
Nominal %Balance27.031.03.51.0≤ 2.0≤ 0.7≤ 0.1≤ 0.020
Mechanical Properties — S Alloy 28 (Sanicro 28)
ConditionUTS (MPa)YS 0.2% (MPa)Elongation (%)Hardness
Solution Annealed at 20°C (Rp0.2 / Rp1.0 Minimum)550–750≥ 220 / ≥ 250≥ 40≤ 90 HRB
Thick Section — over 20 mm, Bar over 100 mm550–750≥ 200 / ≥ 230≥ 40≤ 90 HRB
Cold Worked Tube for Oil & Gas ProductionHigher strength — certified per order––Per order
Physical Properties
Density8.0 g/cm³ (0.29 lb/in³)
Modulus of Elasticity195 GPa at 20°C
Specific Heat Capacity460 J/kg·°C at 20°C
Thermal Conductivity10 W/m·°C at 20°C
Thermal Expansion15 × 10−⁶/°C (30–100°C)
Electrical Resistivity0.99 µΩ·m at 20°C
Equivalent Grades & Standards
UNSEN NumberEN NameCommon Name
N08028 1.4563 X 1 NiCrMoCu 31-27-4 Sanicro 28 / Alloy 28

Key Specifications: ASTM B668 (Seamless Tube & Pipe) / ASTM B709 (Plate, Sheet & Strip) / EN 10216-5 / EN 10088-2 and 10088-3 / EN 10272 (Bar) / ASTM A403 (Fittings) / ISO 4563-080-28-I / SS 2584 / AFNOR Z1NCDU31-27-03. Approved under the ASME Boiler and Pressure Vessel Code Sections I (Code Case 1325-18), III and VIII Division 1; VdTÜV Werkstoffblatt 483; NACE MR0103 and NACE MR0175 / ISO 15156.

Machinability: Alloy 28 is fully austenitic and work-hardens readily, with a thermal conductivity of only 10 W/m·°C that concentrates heat at the cutting edge. Use rigid setups, sharp positive-rake carbide tooling at moderate speeds, heavy positive feeds and generous depth of cut with continuous flood coolant. Cold-worked stock machines more freely than solution-annealed material and is preferred for high-volume screw machining of nuts and small fasteners. Thread rolling is preferred to thread cutting wherever the section size permits.

Welding: weldability is good. Suitable processes are TIG/GTAW as first choice, with MMA/SMAW and gas-shielded arc welding also usable. Recommended heat input is below 1.0 kJ/mm with interpass temperature below 150°C, using a string bead technique. As with all fully austenitic grades, low thermal conductivity and high thermal expansion mean the welding sequence should be planned to limit distortion, and solution annealing after welding is available where residual stress is a concern. Fillers are ISO 14343 S 27 31 4 Cu L / AWS A5.9 ER383 for TIG and MIG, and ISO 3581 E 27 31 4 Cu L R / AWS A5.4 E383-16 for MMA.

Forming: material is delivered in the heat-treated condition. The alloy is readily cold formed, and cold-worked high-strength tube is produced specifically for oil and gas production service.

Heat Treatment: solution anneal at 1100–1160°C for 10 to 30 minutes followed by water quenching; thin-walled sections can be cooled rapidly in air instead. The very low 0.020% maximum carbon content is what allows the alloy to resist intergranular attack after welding without stabilising additions.

Alloy 28 was originally developed for wet-process phosphoric acid and is today the most widely used metallic material for evaporator tubes in that duty, with units in service for over ten years where graphite heat exchangers previously suffered repeated tube failures. Laboratory testing in wet-process phosphoric acid shows it to be far more resistant to the chloride and free fluoride impurities derived from phosphate rock than other high-alloy materials. In sulphuric acid it suits piping and heat exchangers particularly between 40 and 70% deaerated acid and above 85%, with approximately the same resistance as the nickel-base C-type alloys in concentrated 98% acid. It is used for production tubing, casing and liners in deep sour gas wells under NACE MR0175, for fluoride-bearing off-gas handling, for nuclear plant heat exchangers on the strength of its stress-corrosion cracking resistance, and for seawater and chloride-bearing cooling water service.

One honest limit: the manufacturer's own datasheet states that super duplex SAF 2507 is more resistant than Alloy 28 in seawater, so for a pure seawater duty a super duplex grade may be the better and cheaper answer; Alloy 28 earns its place where seawater is combined with an aggressive cooled medium, or where acid resistance governs.

The S alloy numbers are brand designations, not UNS numbers, and they do not map onto the alloy numbers used elsewhere in this catalogue. Alloy 41 in this family is UNS N08825 — the alloy sold generically as 825 — not the Rene 41 superalloy. Alloy 60 is UNS N06625, which is alloy 625, while Alloy 70 is UNS N06600, which is alloy 600. Alloy 31HT is UNS N08810/N08811, the 800H and 800HT chemistry. Always confirm the UNS number rather than ordering against the brand number alone; the S Alloys cross-reference table sets out the full mapping.

Sanicro is a trademark of Alleima, the former Sandvik Materials Technology business. Exotic Alloy is an independent manufacturer and is not affiliated with or endorsed by Alleima or Sandvik; the designation is used here solely to identify the alloy chemistry, which is defined by the UNS and EN numbers given above.
Key Characteristics

  • Very high corrosion resistance in strong phosphoric and sulphuric acids.
  • The most widely used metallic material for wet-process phosphoric acid evaporators.
  • Very good resistance to stress-corrosion cracking and intergranular attack.
  • High resistance to chloride pitting and crevice corrosion.
  • NACE MR0103 and NACE MR0175 / ISO 15156 qualified for sour service.

Typical Applications

  • Phosphoric acid plants: evaporator tube and heat exchanger bolting.
  • Sulphuric acid service: piping, flange and heat exchanger fasteners.
  • Sour oil and gas: production tubing, casing and liner components.
  • Nuclear power: heat exchanger fastener and tube support hardware.
  • Seawater and chloride-bearing cooling water system fasteners.