+91 97734 41022 sales@exoticalloy.com
Material Specification

Alloy 825

Alloy 825 Fasteners
Titanium-Stabilised Ni-Fe-Cr-Mo-Cu Alloy – Sulfuric Acid & Sour Service

Incoloy 825 Fasteners

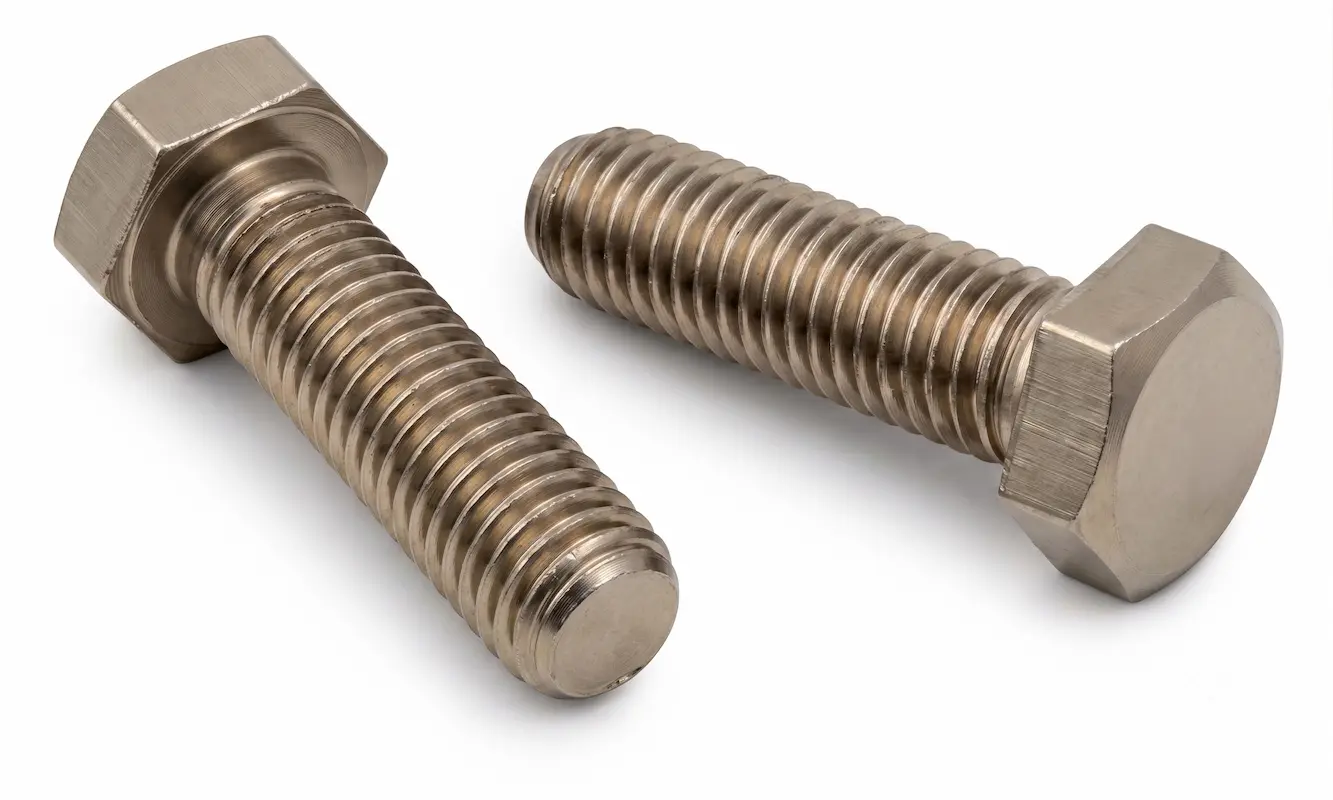
Buy Incoloy Alloy 825 (UNS N08825 / Werkstoff 2.4858 / ASTM B425) bolts, stud bolts, heavy hex nuts, socket cap screws, and custom CNC fasteners from Exotic Alloy. Incoloy 825 is a titanium-stabilised nickel-iron-chromium alloy with molybdenum and copper additions, giving it excellent resistance to both reducing and oxidising acids, to chloride-induced stress-corrosion cracking, and to pitting and crevice corrosion.

Exotic Alloy manufactures Incoloy 825 fasteners conforming to ASTM B425, ASME SB-425, DIN 17750 and NACE MR0175 / ISO 15156-3 in metric M6–M100 and imperial ¼"–4" sizes with full EN 10204 3.1 material test certificates for sour gas, sulfuric acid, pickling, nuclear fuel reprocessing and marine applications.

Request a Quote
Product Range

Alloy 825 Fasteners Available

Alloy 825 Hex Bolts
Alloy 825
Hex Bolts
Alloy 825 Heavy Hex Bolts
Alloy 825
Heavy Hex Bolts
Alloy 825 Stud Bolts
Alloy 825
Stud Bolts
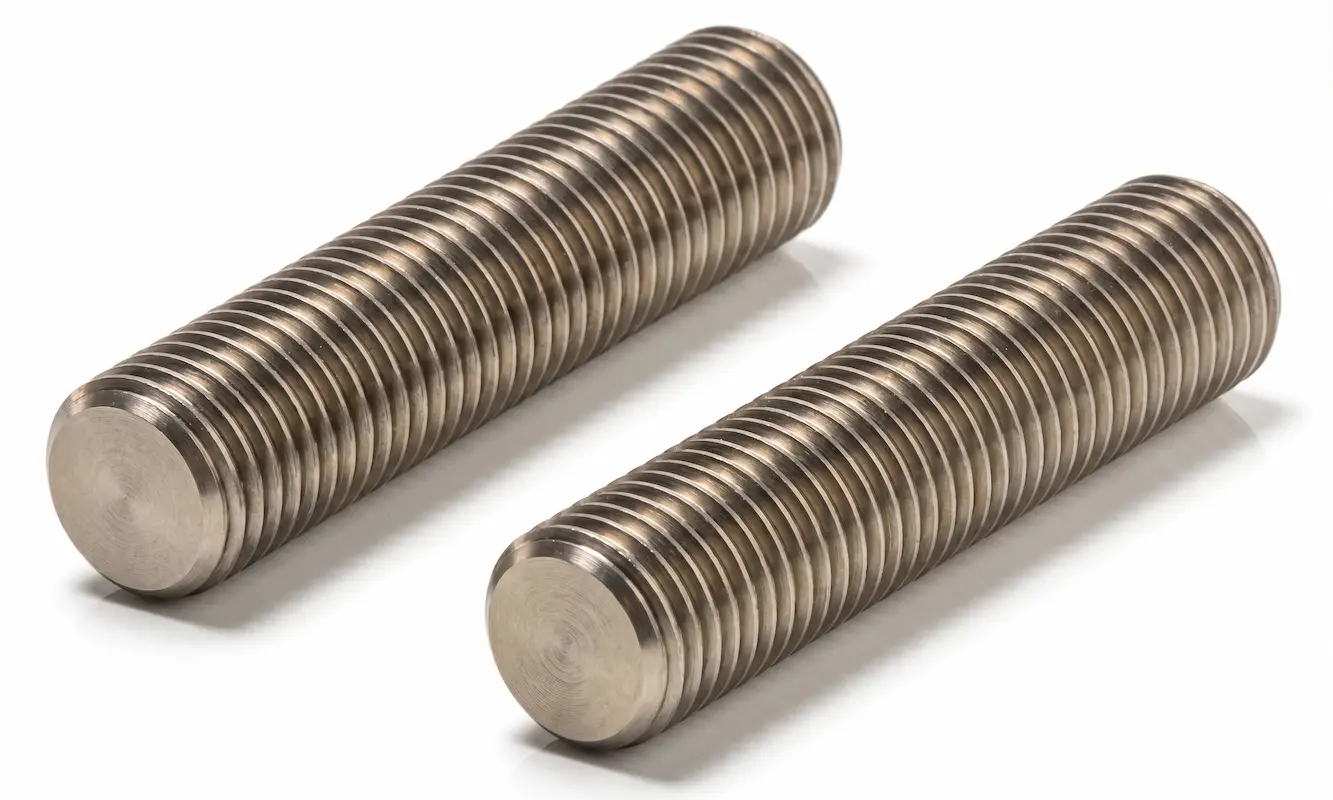
Alloy 825 Threaded Rods
Alloy 825
Threaded Rods
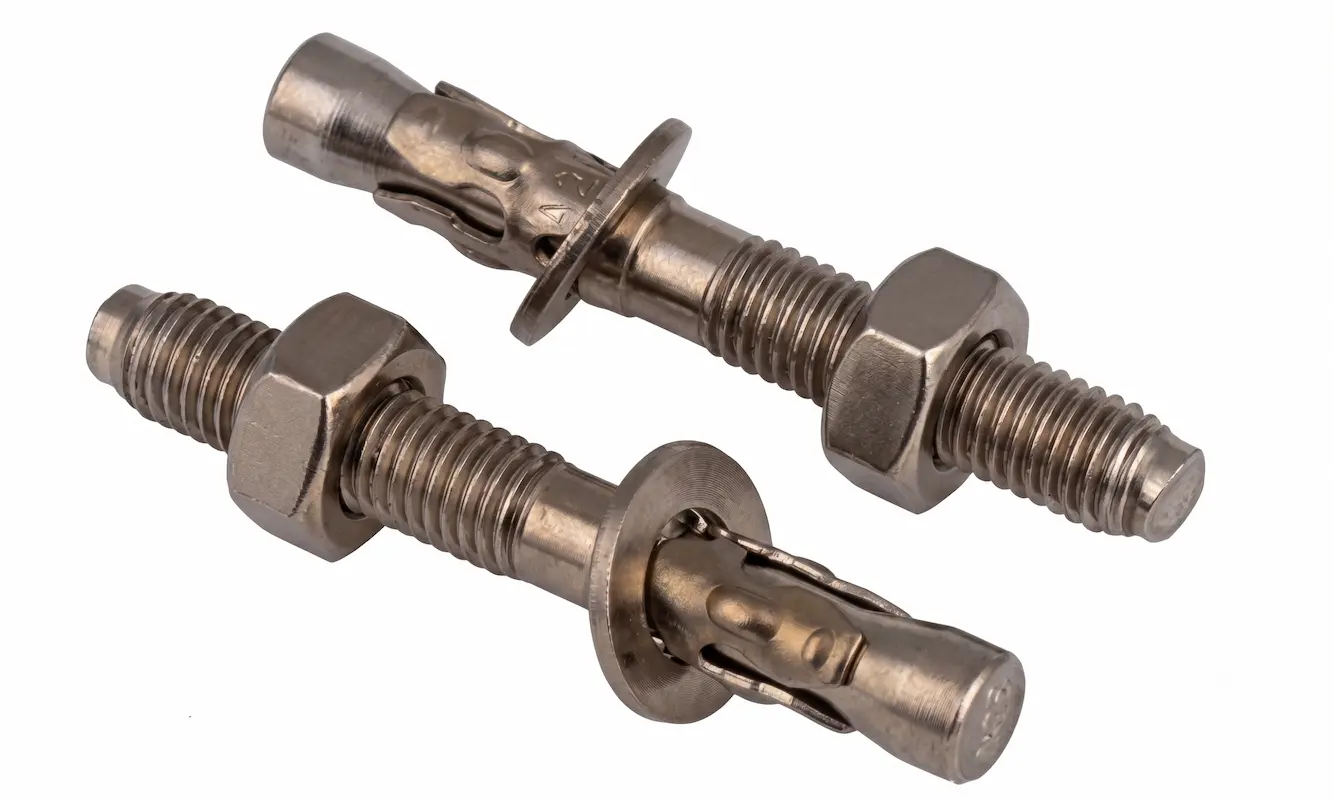
Alloy 825 Anchor Bolts
Alloy 825
Anchor Bolts
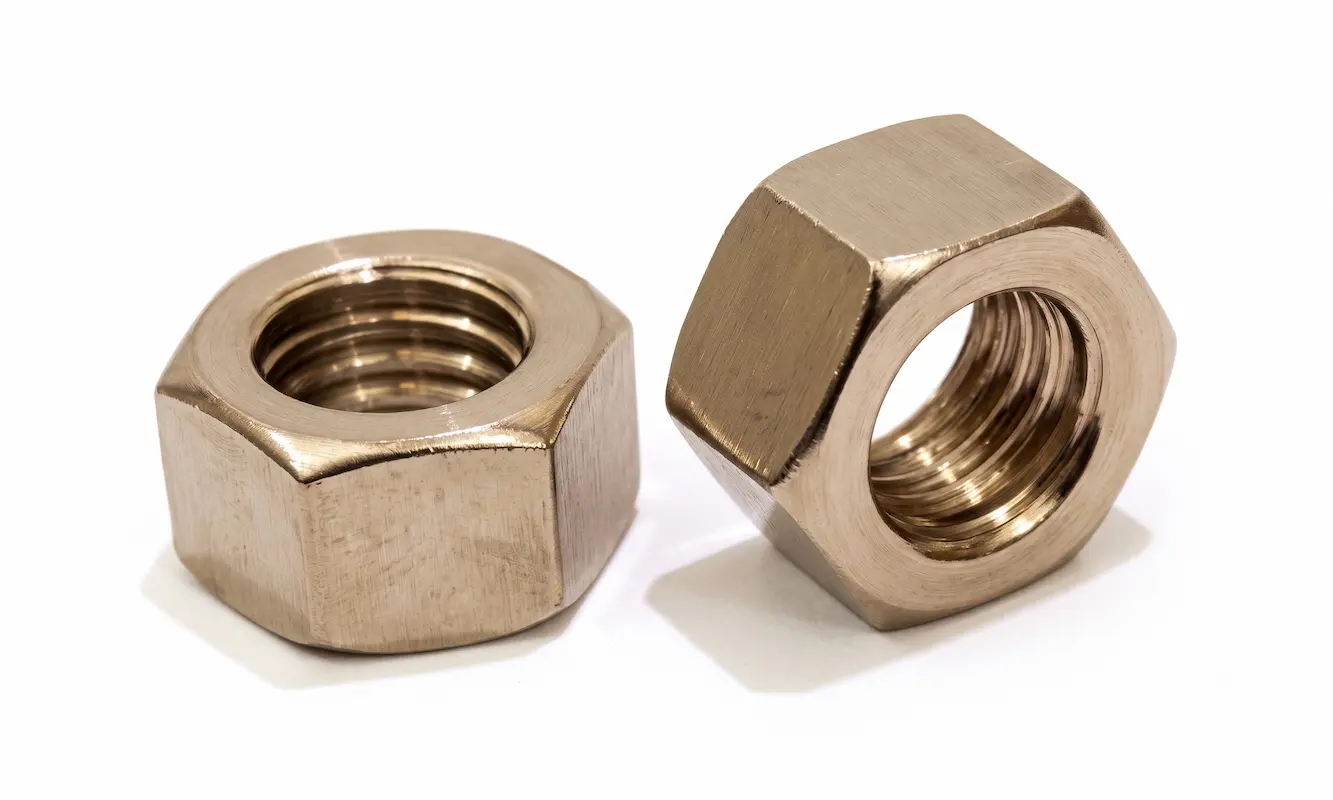
Alloy 825 Hex Nuts
Alloy 825
Hex Nuts
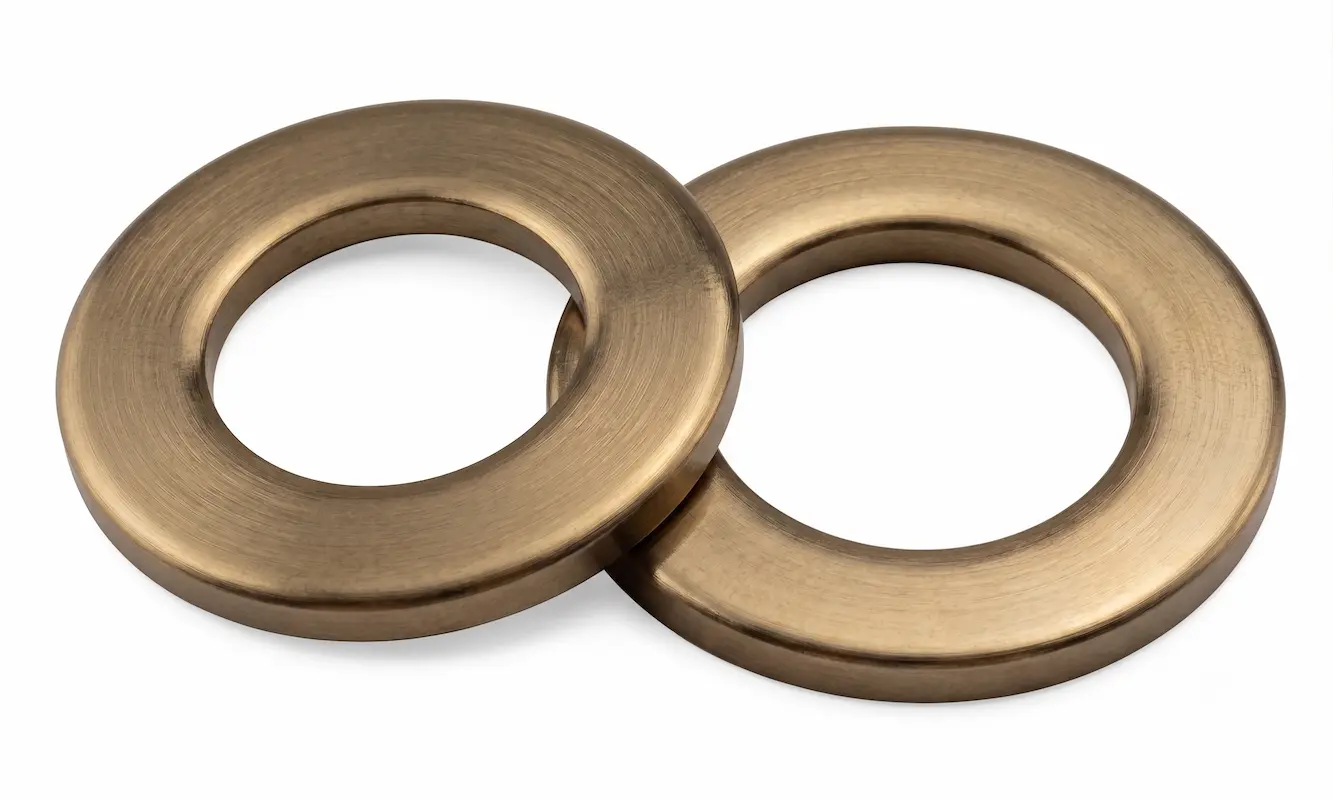
Alloy 825 Washers
Alloy 825
Washers
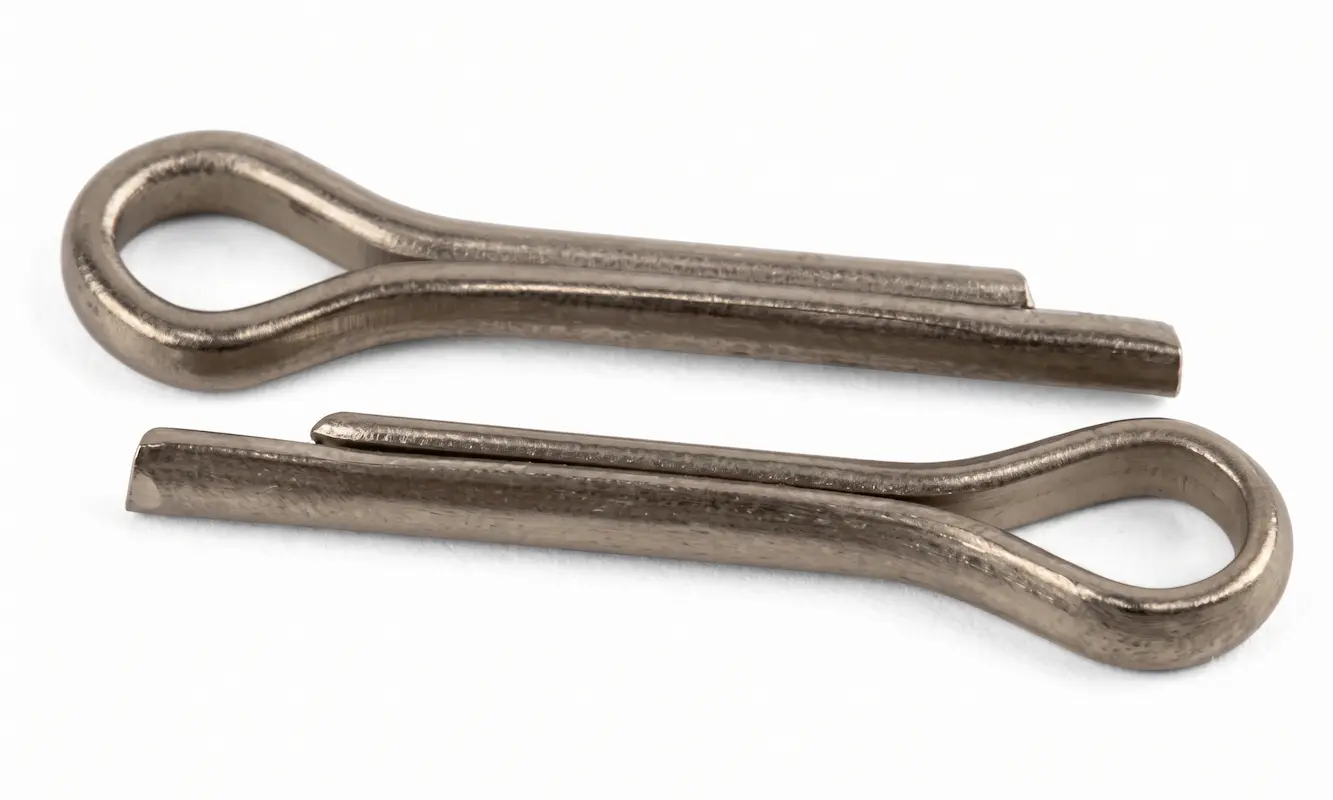
Alloy 825 Cotter Pins
Alloy 825
Cotter Pins
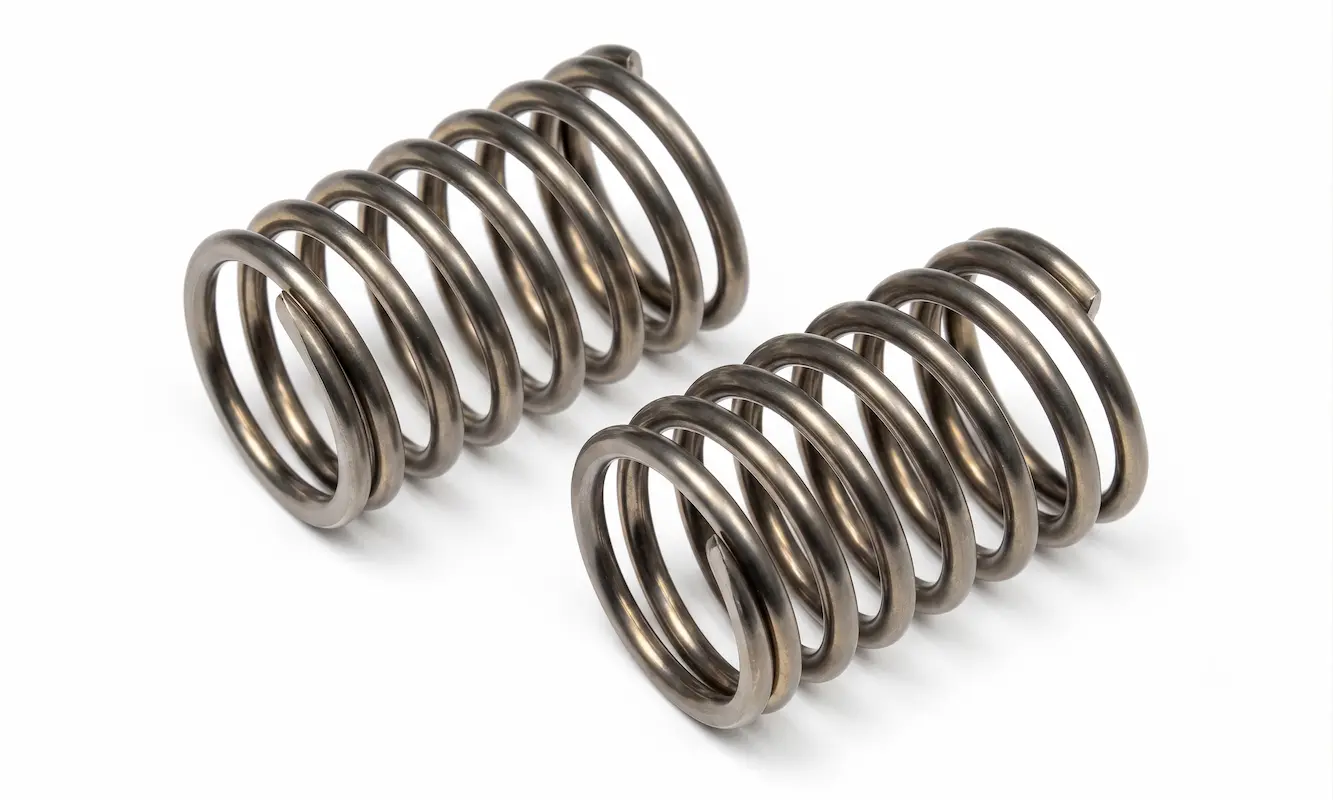
Alloy 825 Springs
Alloy 825
Springs
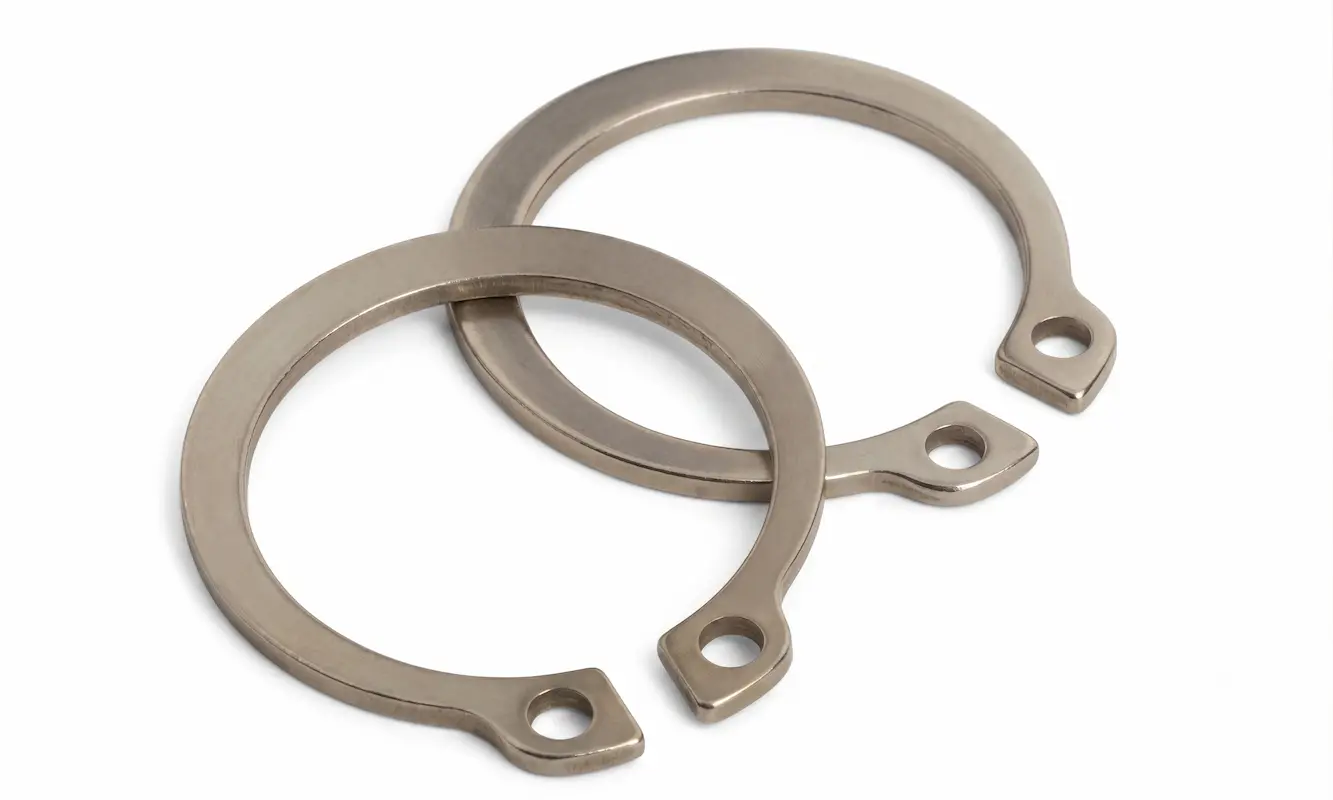
Alloy 825 Circlips
Alloy 825
Circlips
Alloy 825 Coated Fasteners
Alloy 825
Coated Fasteners
Alloy 825 Custom Spacers
Alloy 825
Custom Spacers
Technical Data

Alloy 825 Specifications

Chemical Composition — Incoloy 825 (wt. %)
ElementNiFeCrMoCuTiMnSiC
Min %38.0022.0019.502.501.500.60–––
Max %46.00Balance23.503.503.001.201.000.500.05
Mechanical Properties — Incoloy 825
ConditionUTS (MPa)YS 0.2% (MPa)Elongation (%)Hardness
Annealed (ASTM B425 Minimum)≥ 586≥ 241≥ 30≤ 100 HRB
Annealed (Typical Bar)69031045150 HB
Cold Drawn / Stress Relieved760–930550–76015–2522–30 HRC
Hot Finished Forged Bar620–720260–34540–50≤ 180 HB
Physical Properties
Density8.14 g/cm³
Melting Range1370–1400°C (2500–2550°F)
Specific Heat Capacity440 J/kg·K
Thermal Conductivity11.1 W/m·K at 26°C
Thermal Expansion14.0 µm/m·°C (20–100°C)
Electrical Resistivity1.13 µΩ·m
Equivalent Grades & Standards
UNSWerkstoff / DINEN DesignationCommon Name
N08825 2.4858 NiCr21Mo Incoloy 825

Key Specifications: ASTM B425 (Rod & Bar) / ASTM B424 (Plate & Sheet) / ASTM B423 (Tube) / ASTM B564 (Forgings) / ASTM B366 (Fittings) / NACE MR0175 / ISO 15156-3

Machinability: Incoloy 825 work-hardens appreciably and is gummy in the annealed condition. Use rigid setups, sharp positive-rake carbide tooling at 25–45 SFM, heavy positive feeds and generous depth of cut so the tool cuts beneath the previously hardened layer. Continuous flood coolant is essential. Cold-drawn stock machines more freely than annealed material and is preferred for high-volume screw machining.

Welding: Incoloy 825 is readily welded by GTAW, GMAW and SMAW using INCONEL Filler Metal 65 (ERNiFeCr-1) or INCO-WELD A electrodes. The titanium stabilisation ties up carbon and suppresses sensitisation, so weld heat-affected zones retain corrosion resistance without post-weld solution annealing. Pre-heat is not required; keep interpass temperature below 150°C.

Forging: Hot forge between 1040–1180°C (1900–2150°F) and finish above 900°C (1650°F). Soaking above 1180°C risks grain coarsening. Cold forging and cold heading are practicable in smaller diameters with intermediate anneals to restore ductility.

Heat Treatment: Anneal at 940–1010°C (1725–1850°F) followed by rapid cooling. Incoloy 825 is not age-hardenable; where higher strength is required in the same corrosion-resistant chemistry, specify the age-hardenable Incoloy 925. For NACE MR0175 sour service, cold-worked fasteners must be supplied within the hardness limits stated in ISO 15156-3.

Incoloy 825 resists sulfuric and phosphoric acids, nitric acid, and both oxidising and reducing chemical media. The nickel base gives freedom from chloride-induced stress-corrosion cracking, molybdenum and copper handle reducing acids and pitting attack, and chromium provides resistance in oxidising conditions. Titanium stabilisation prevents sensitisation during welding so intergranular attack is avoided in the as-welded condition. Typical duties include sulfuric acid pickling, phosphoric acid production, nuclear fuel reprocessing, radioactive waste handling, and sour oil and gas service under NACE MR0175. Applications broadly overlap those of Alloy 20.

Key Characteristics

  • Titanium stabilised — resists sensitisation and intergranular attack after welding.
  • Molybdenum and copper give strong resistance to sulfuric and phosphoric acids.
  • Excellent freedom from chloride-induced stress-corrosion cracking.
  • Good resistance to pitting and crevice corrosion in chloride media.
  • NACE MR0175 / ISO 15156-3 qualified for sour hydrocarbon service.

Typical Applications

  • Sour oil and gas: wellhead, flange and downhole fastener assemblies.
  • Sulfuric and phosphoric acid plants: reactor and pump bolting.
  • Pickling plants: acid tank, rack and heating coil hardware.
  • Nuclear fuel reprocessing and radioactive waste handling fasteners.
  • Marine and pollution control: scrubber and seawater system bolting.