+91 97734 41022 sales@exoticalloy.com
Material Specification

Grade 7

Grade 7 Fasteners
Palladium-Bearing CP Titanium – Best Crevice & Reducing Acid Resistance

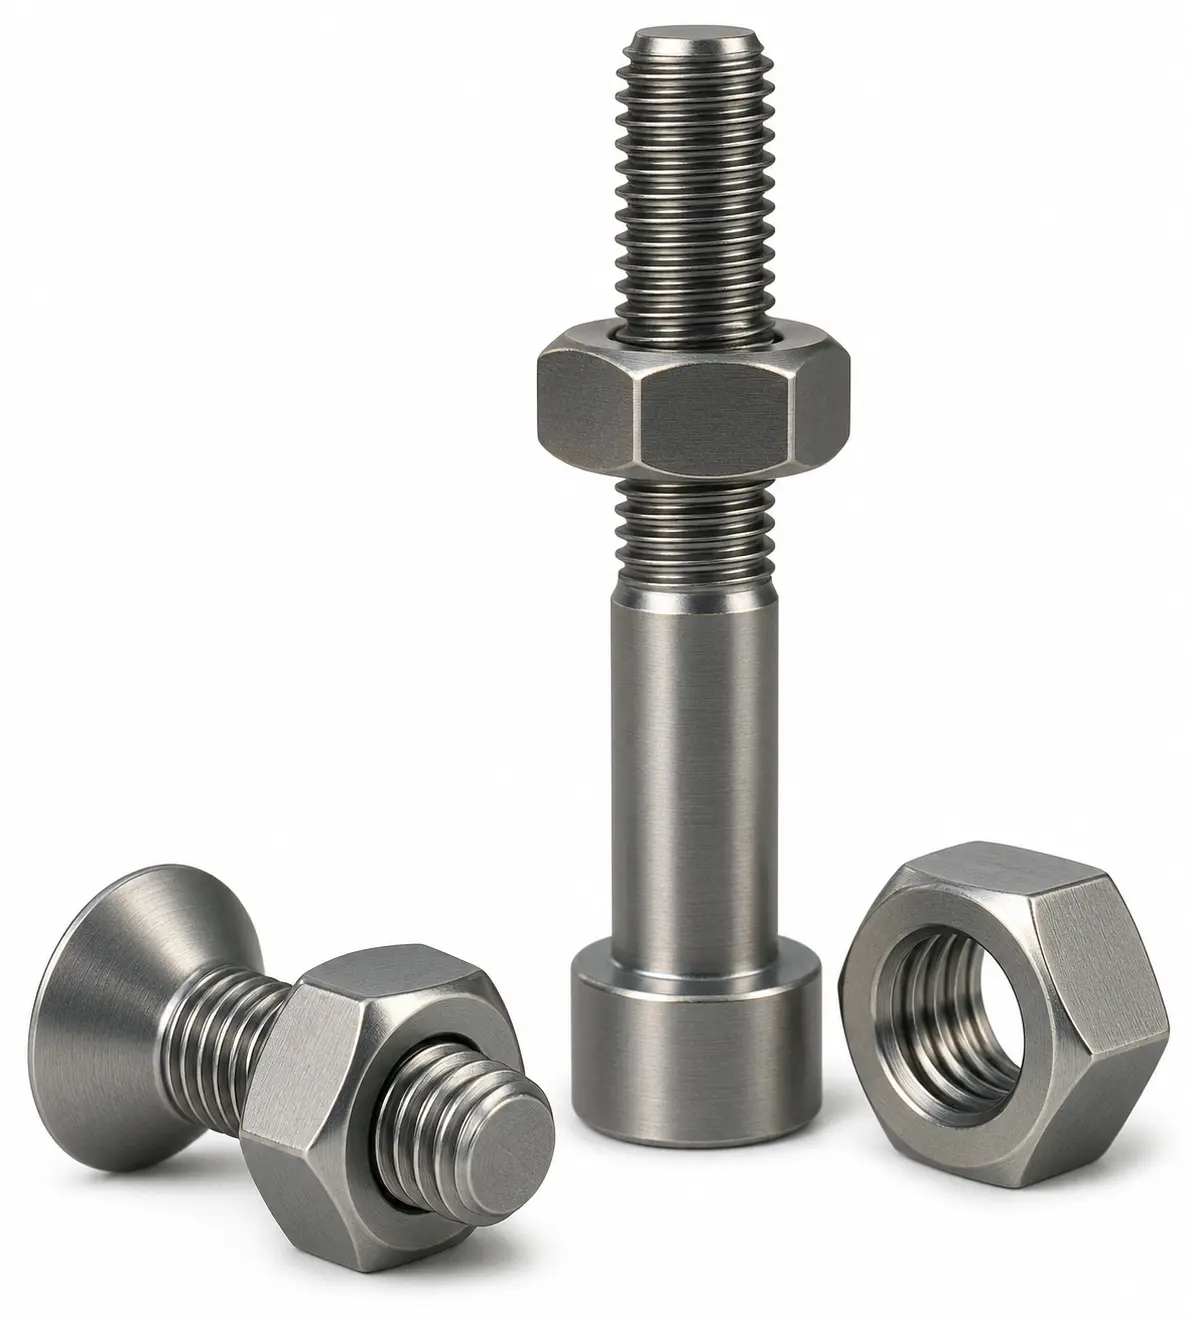
Titanium Grade 7 Fasteners

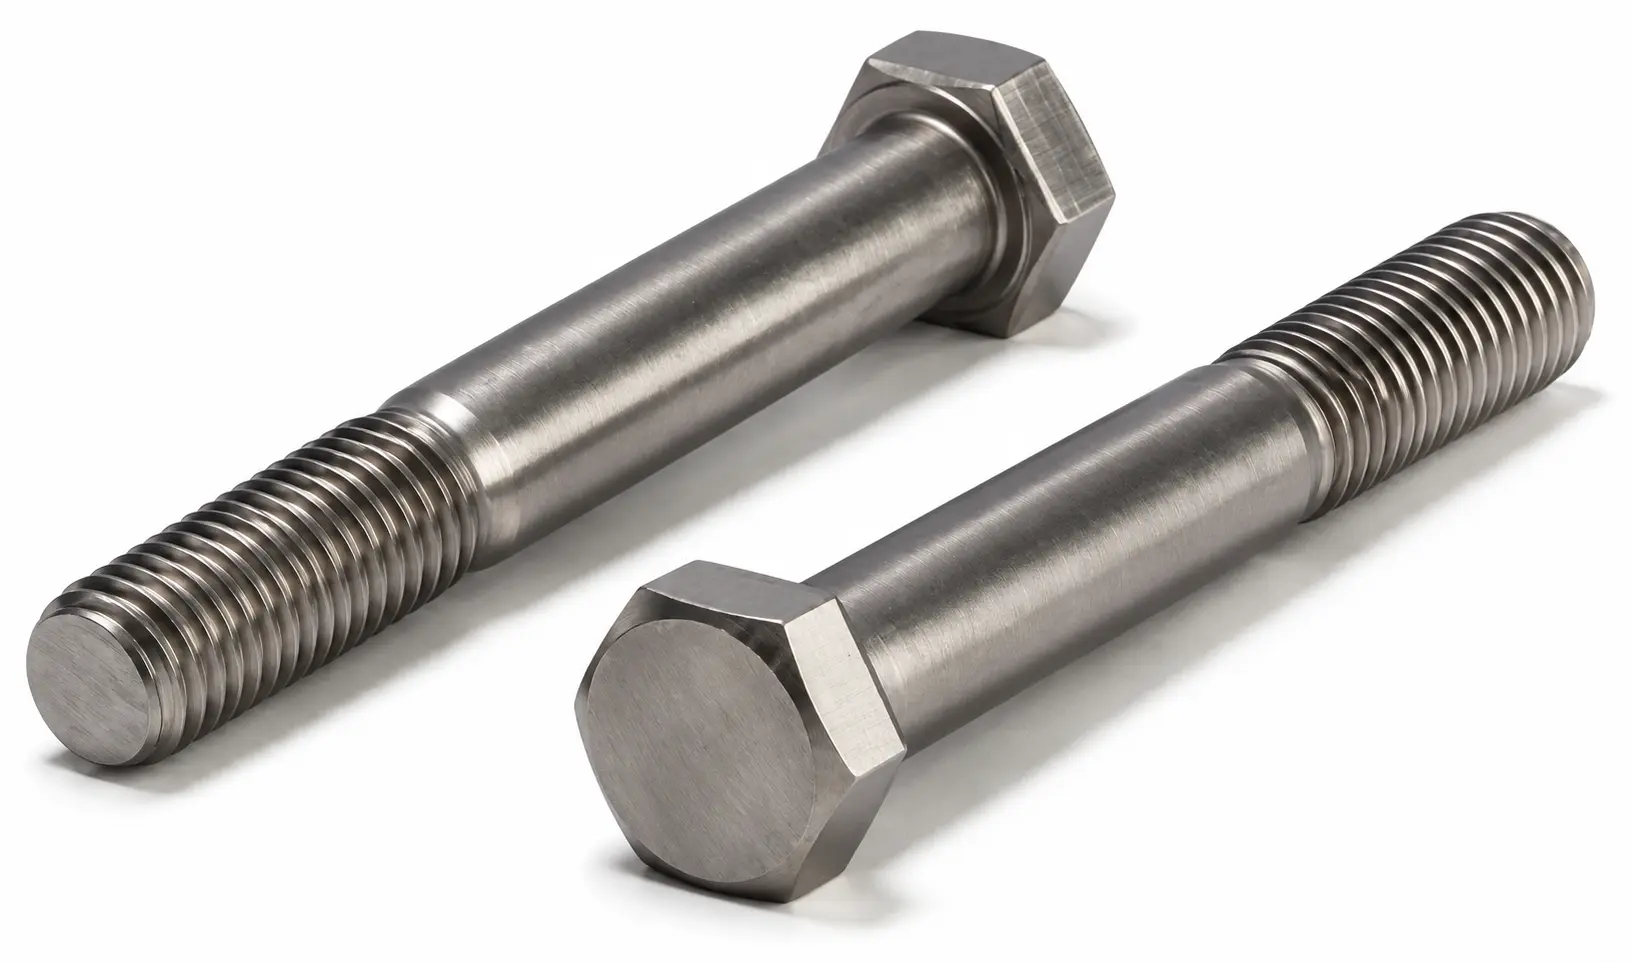
Buy Titanium Grade 7 (Ti-0.15Pd / UNS R52400 / Werkstoff 3.7235 / ASTM B348 Grade 7) bolts, stud bolts, hex nuts, washers and custom CNC fasteners from Exotic Alloy. Grade 7 is commercially pure titanium of Grade 2 chemistry with a deliberate 0.12 to 0.25% palladium addition. Mechanically it is identical to Grade 2; the palladium exists solely to transform its behaviour in hot chlorides and reducing acids, where it gives the best crevice corrosion resistance of any grade in this family.

Exotic Alloy manufactures Grade 7 titanium fasteners to ASTM B348, ASTM B265, ASTM B381 and ASTM F467 and F468, in metric M3–M48 and imperial #6–2" sizes, with full EN 10204 3.1 material test certificates for wet-process chemical plant, hot brine, sour service and acid-handling applications where Grade 2 would be at risk of crevice attack.

Request a Quote
Product Range

Grade 7 Fasteners Available

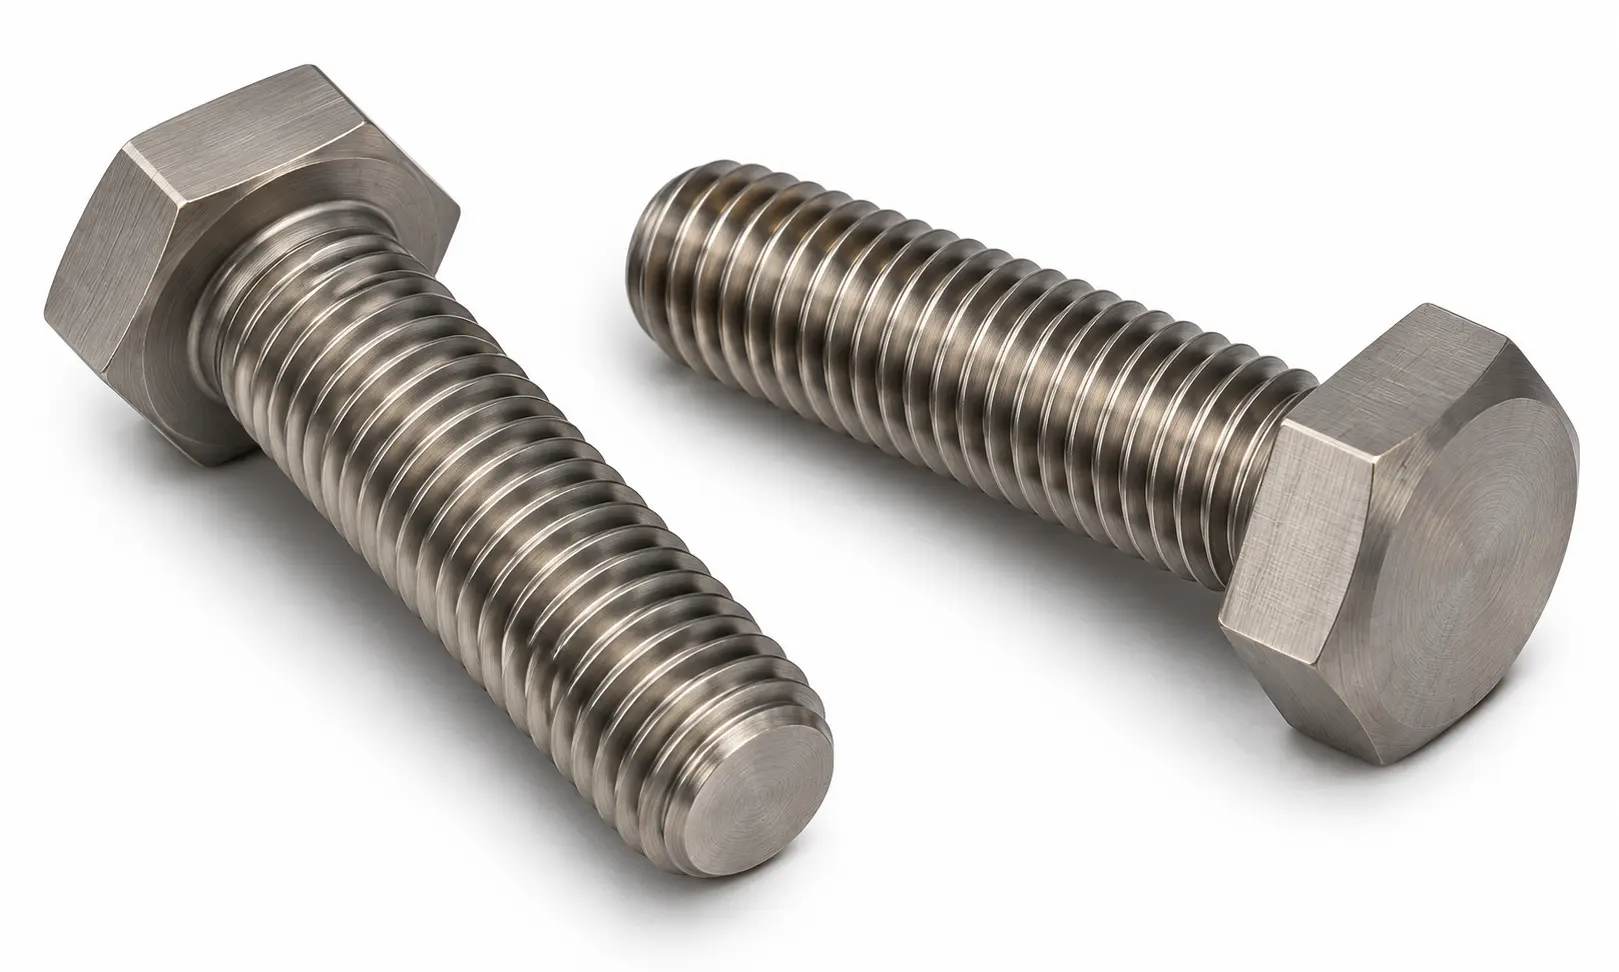
Grade 7 Hex Bolts
Grade 7
Hex Bolts
Grade 7 Heavy Hex Bolts
Grade 7
Heavy Hex Bolts
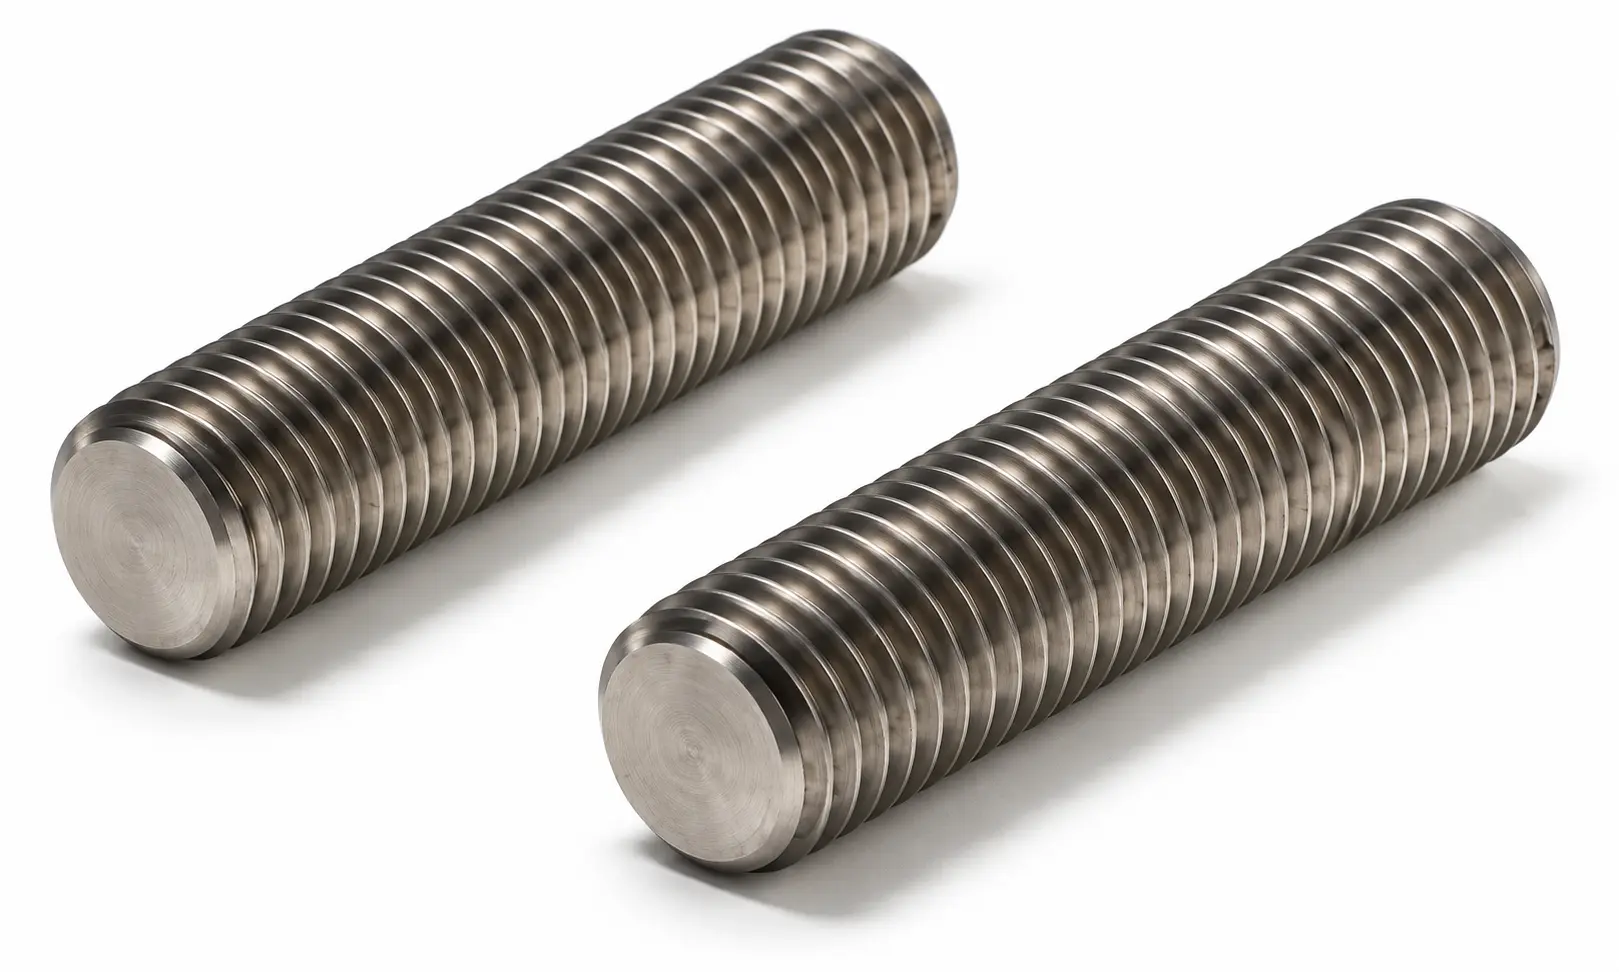
Grade 7 Stud Bolts
Grade 7
Stud Bolts
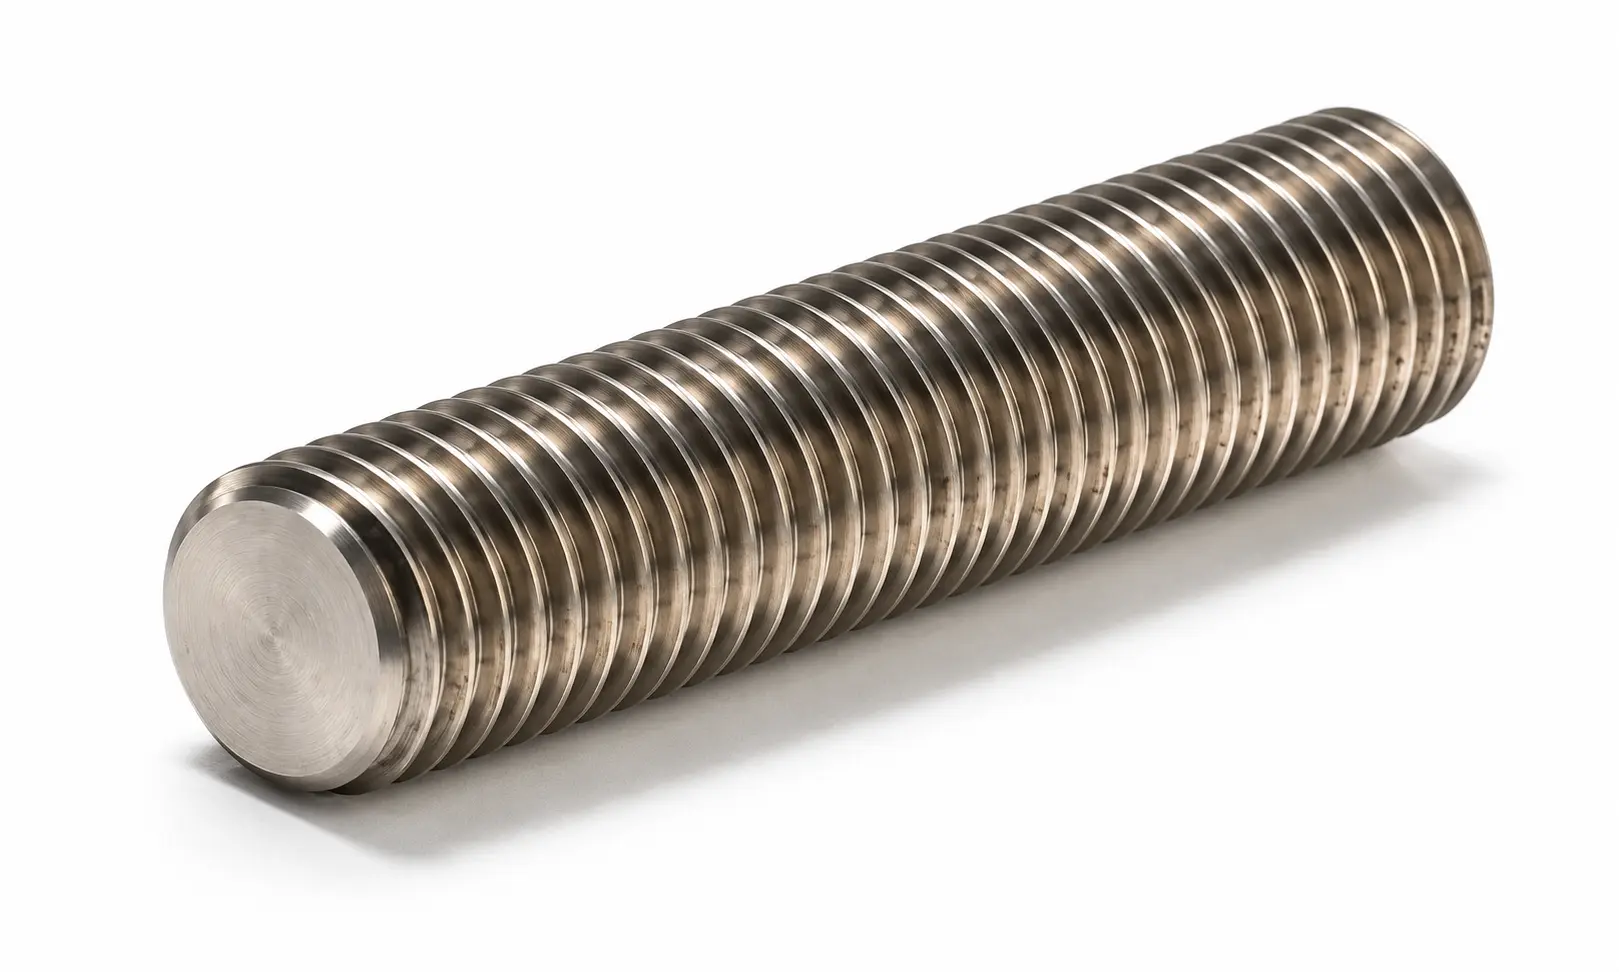
Grade 7 Threaded Rods
Grade 7
Threaded Rods
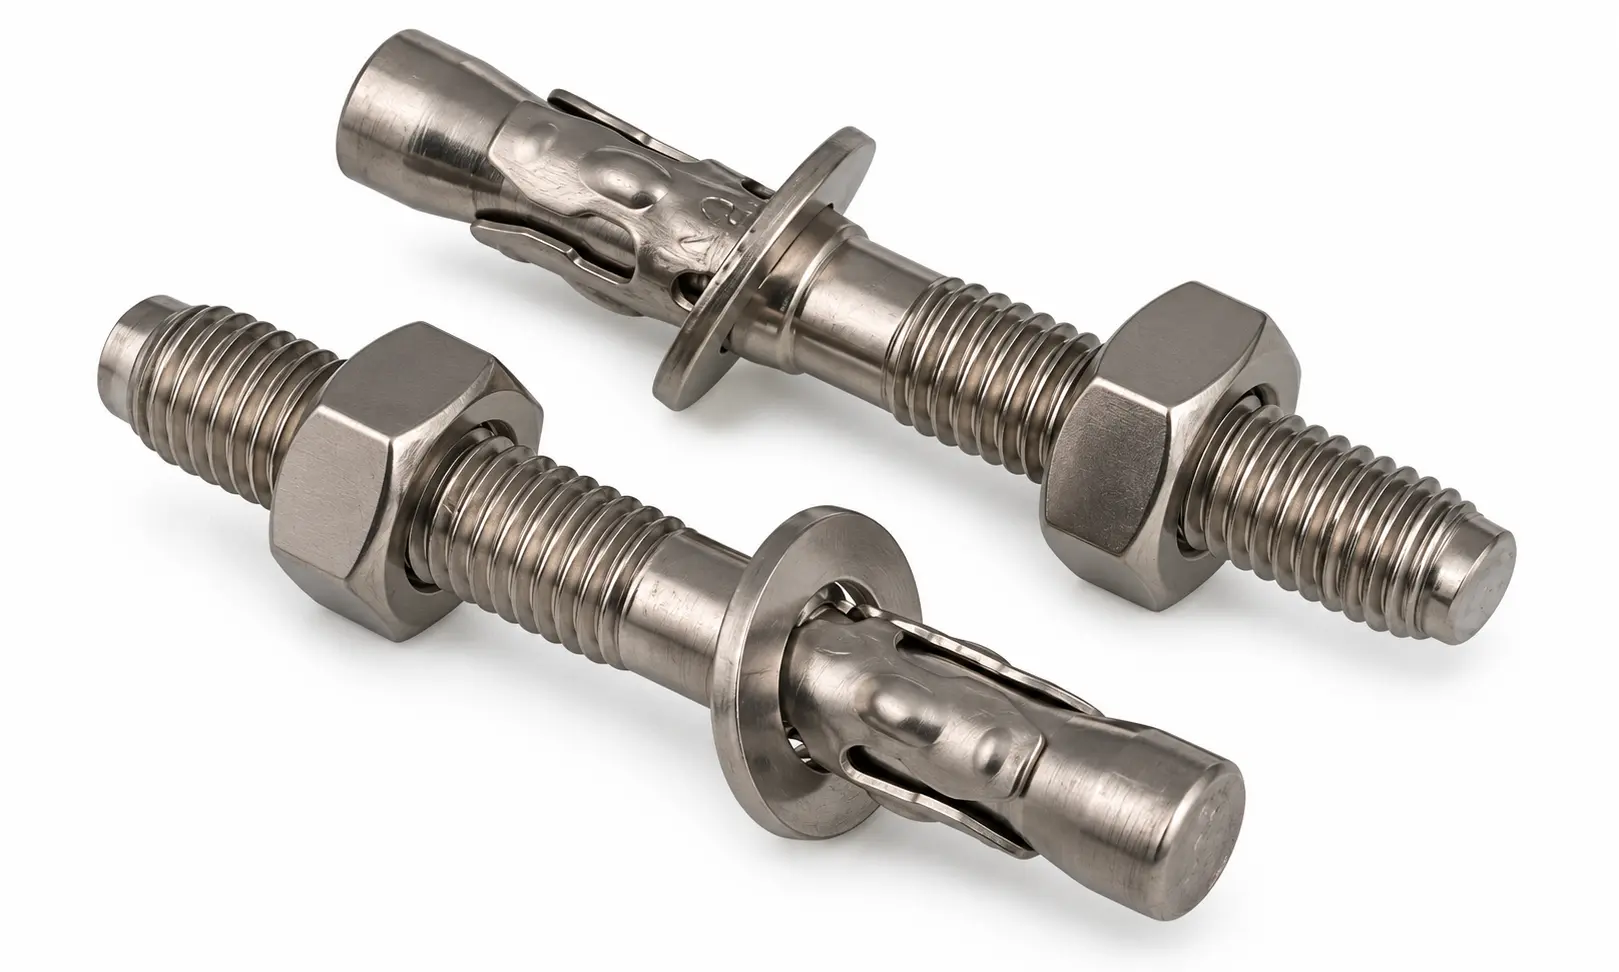
Grade 7 Anchor Bolts
Grade 7
Anchor Bolts
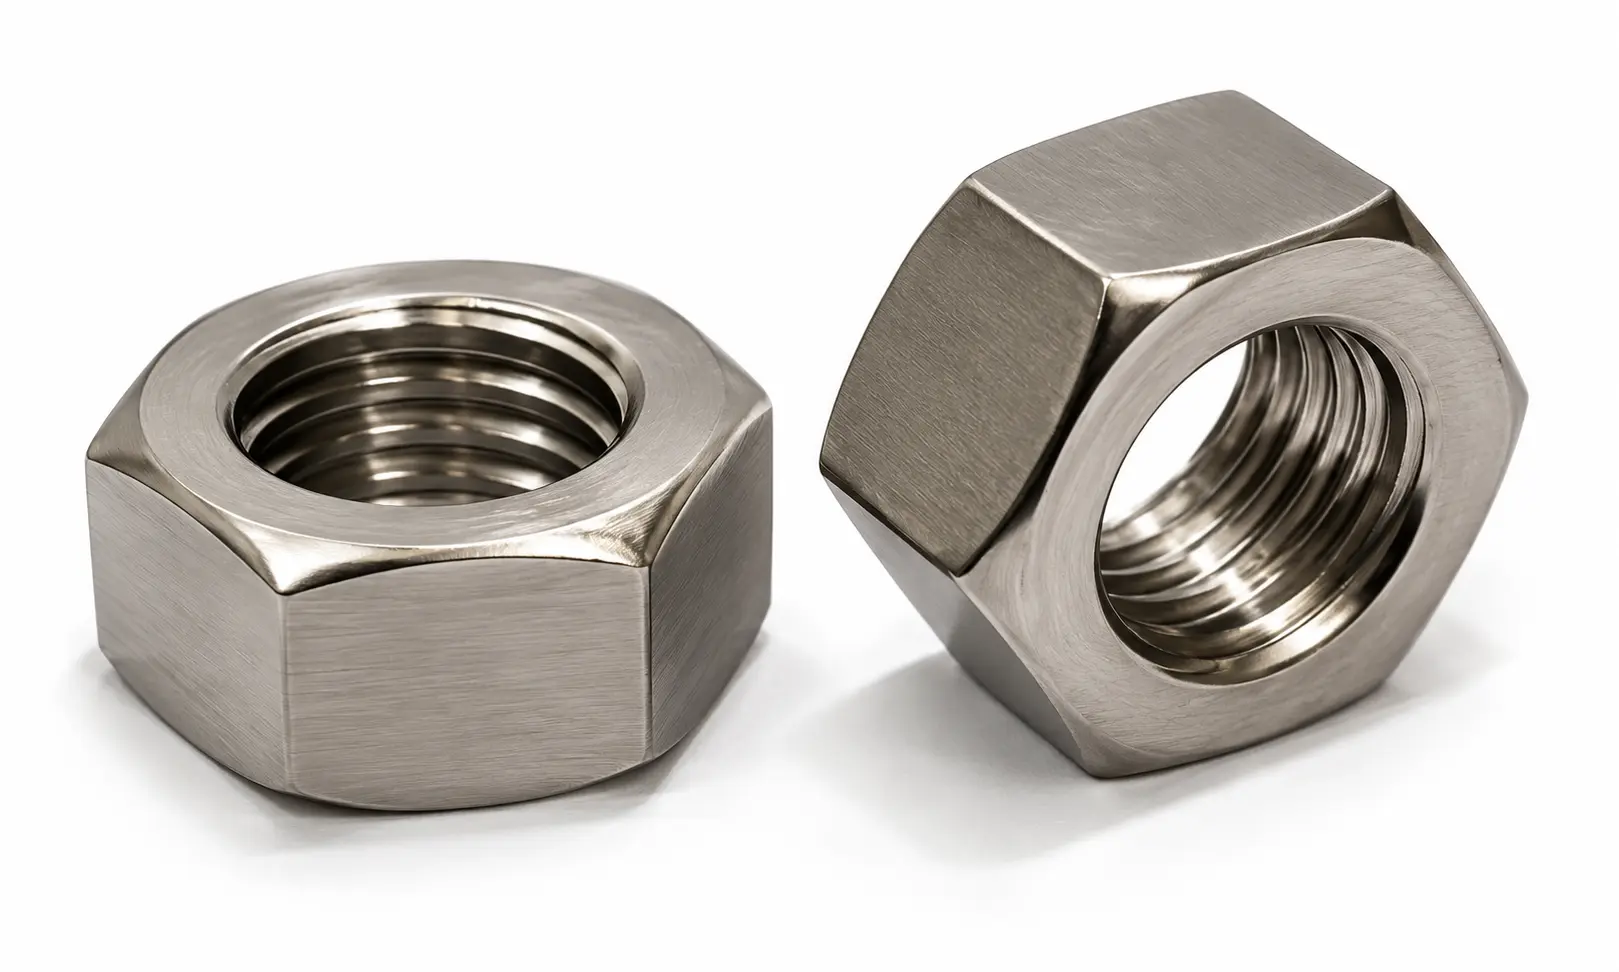
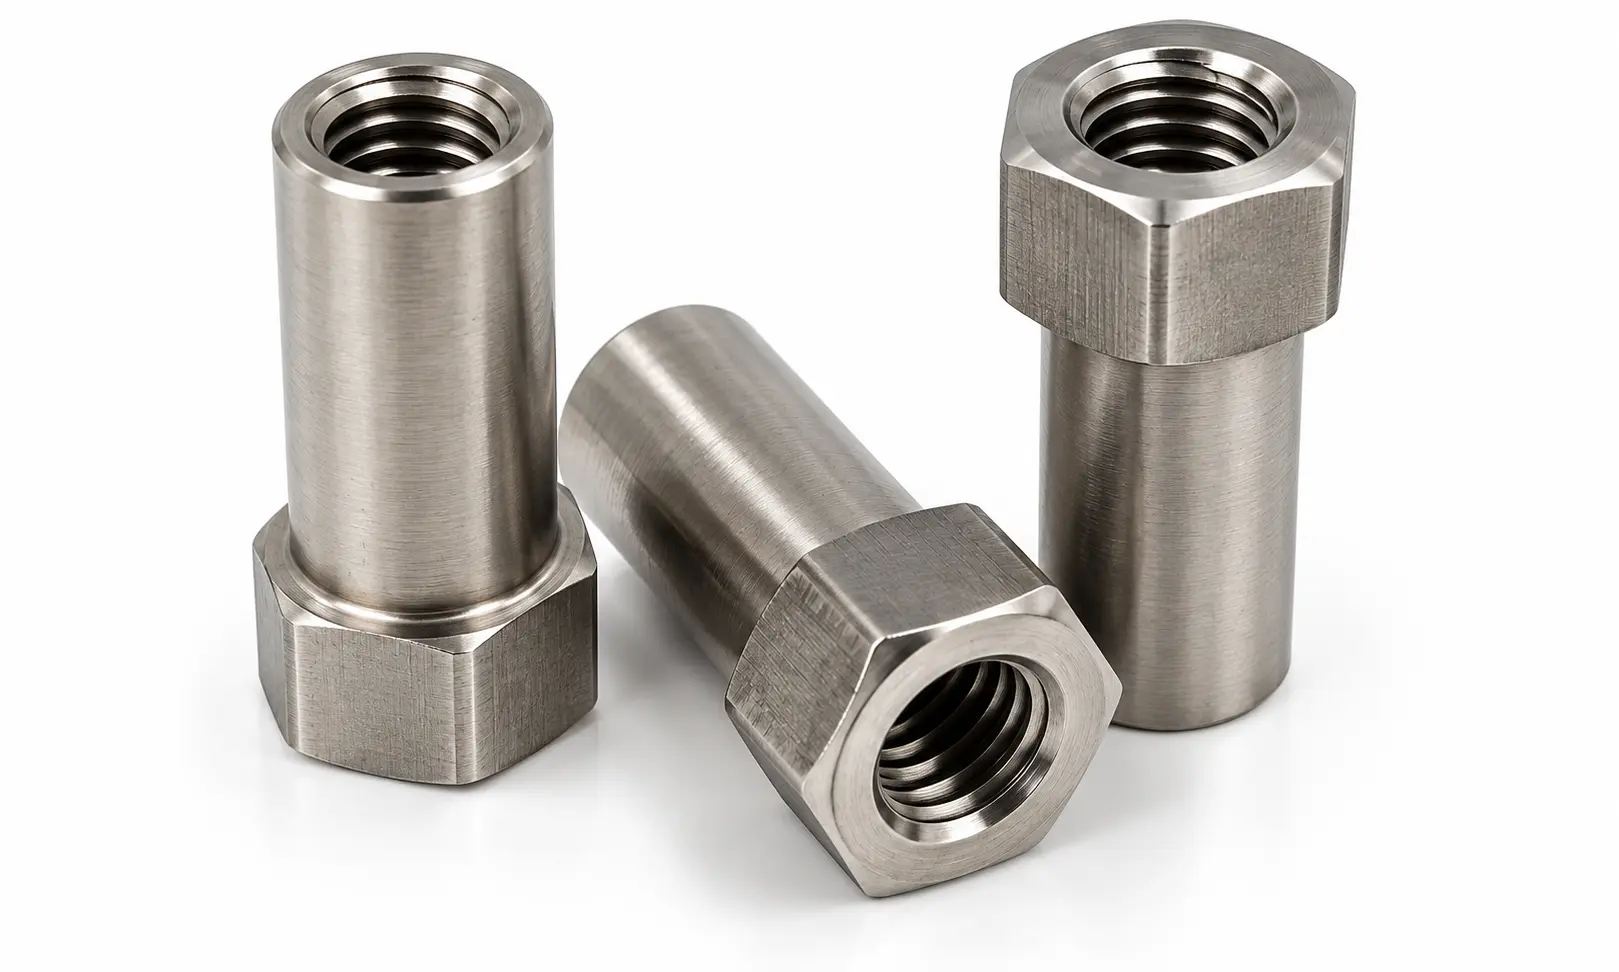
Grade 7 Hex Nuts
Grade 7
Hex Nuts
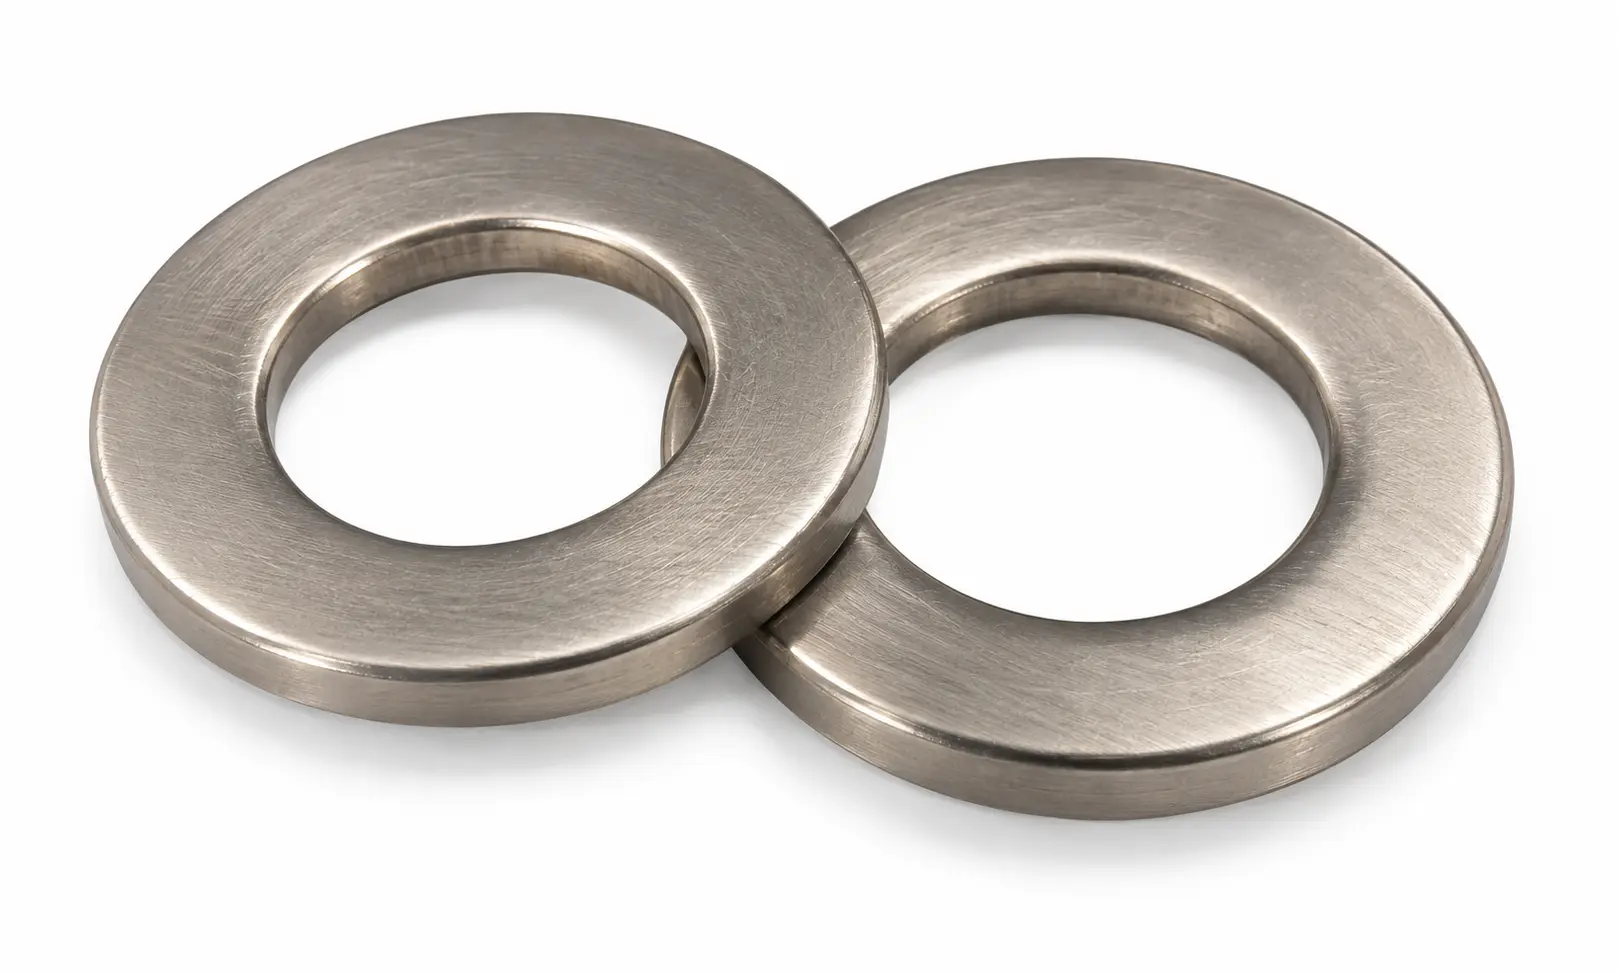
Grade 7 Washers
Grade 7
Washers
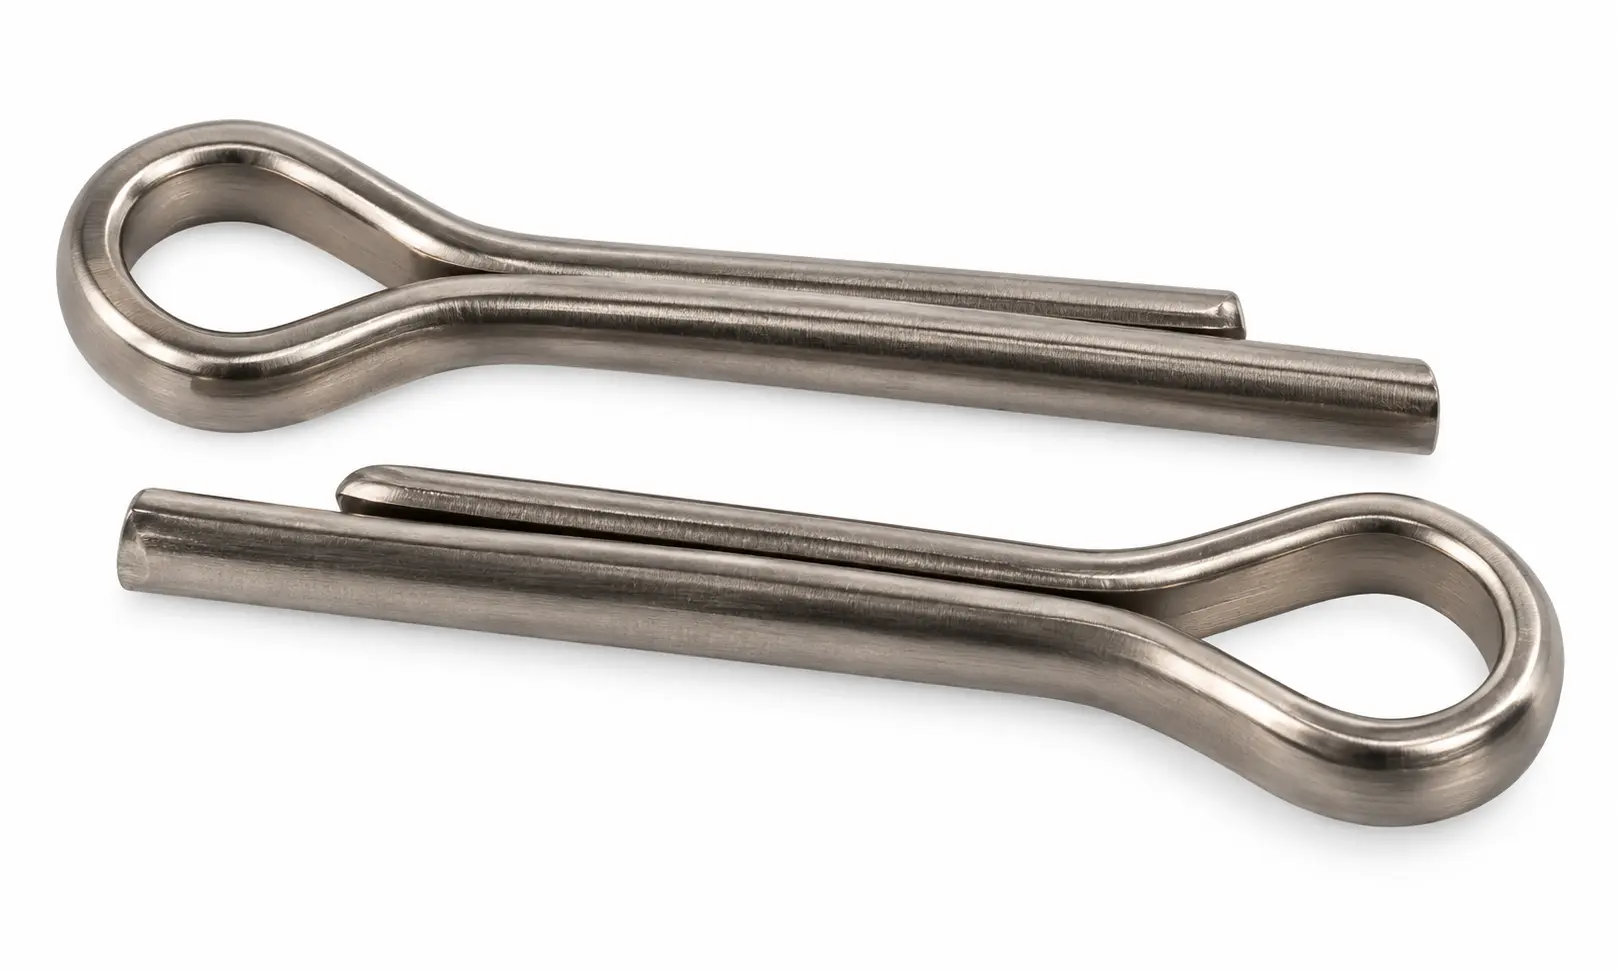
Grade 7 Cotter Pins
Grade 7
Cotter Pins
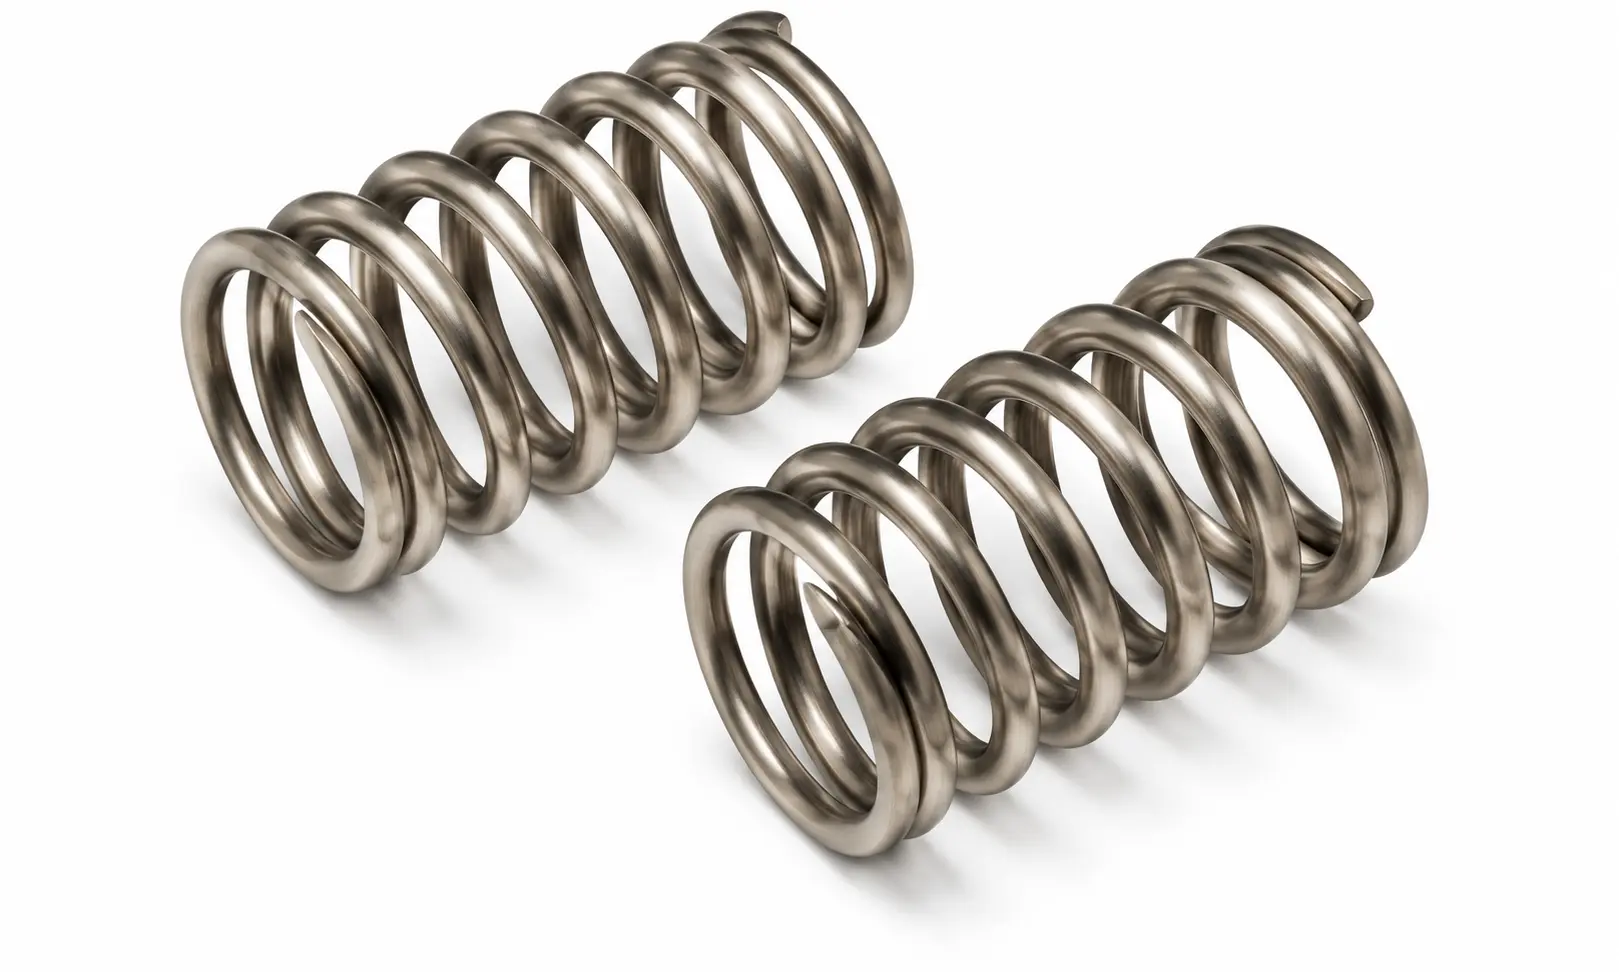
Grade 7 Springs
Grade 7
Springs
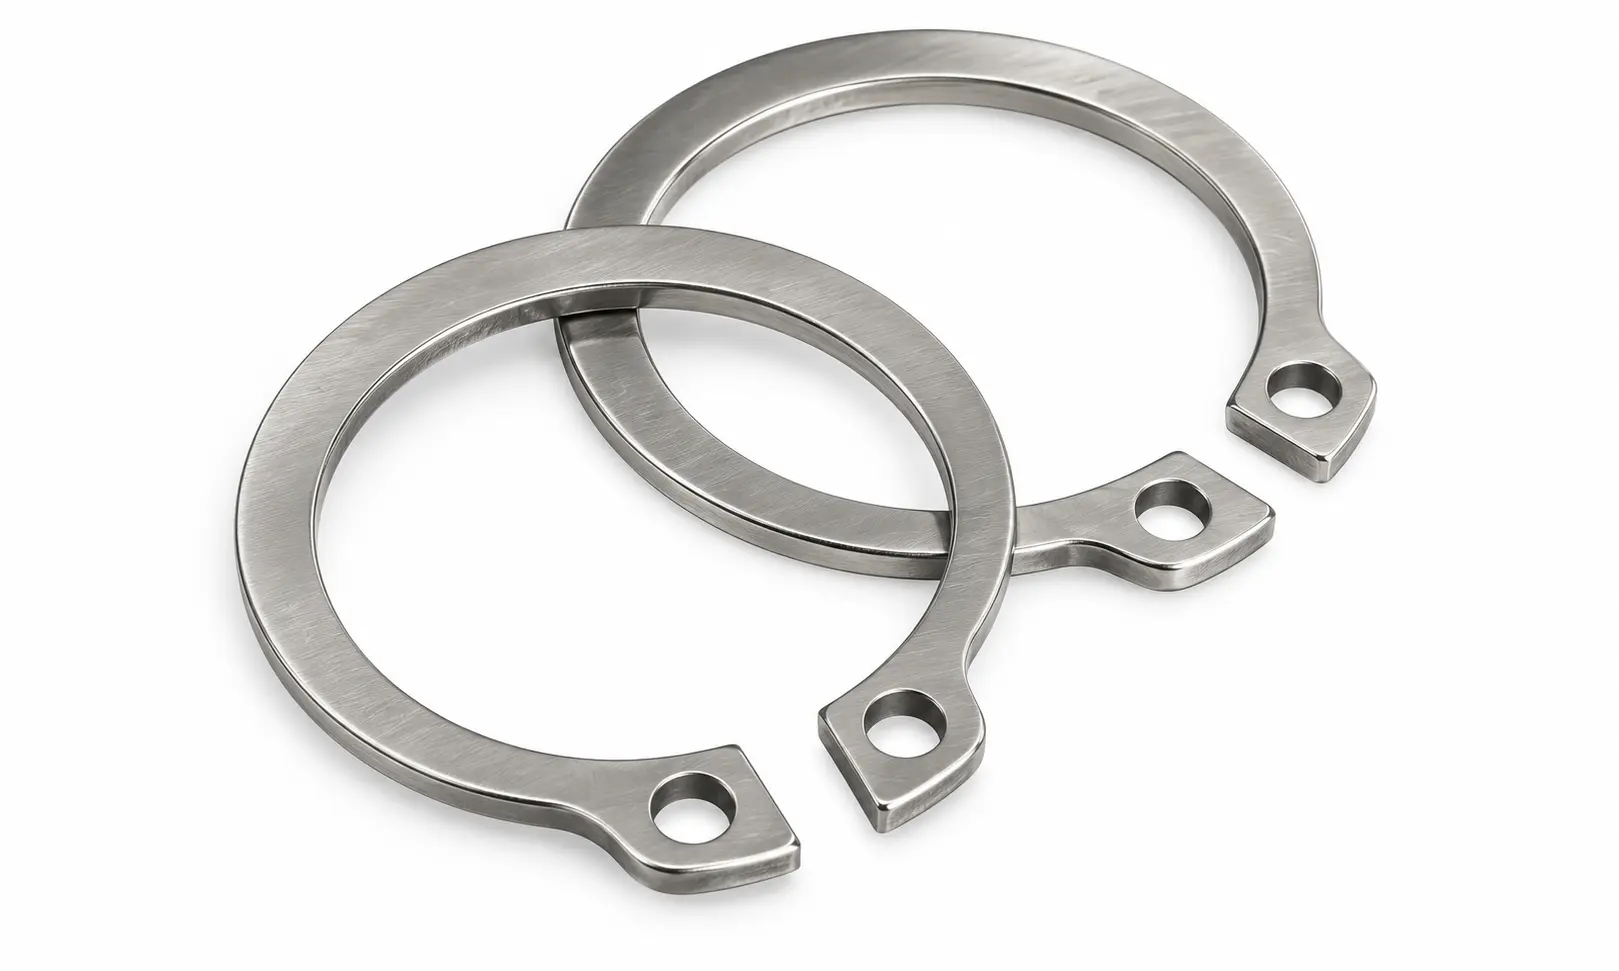
Grade 7 Circlips
Grade 7
Circlips
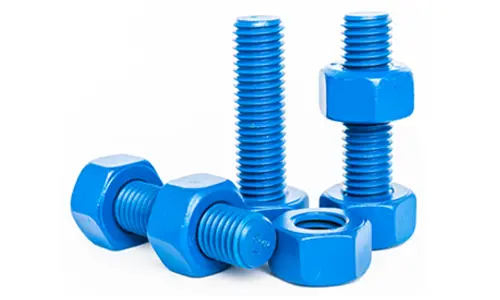
Grade 7 Coated Fasteners
Grade 7
Coated Fasteners
Grade 7 Custom Spacers
Grade 7
Custom Spacers
Technical Data

Grade 7 Specifications

Chemical Composition — Titanium Grade 7 (wt. %)
ElementTiPdOFeNCH
Min %Balance0.12–––––
Max %Balance0.250.250.300.030.080.015
Mechanical Properties — Titanium Grade 7
ConditionUTS (MPa)YS 0.2% (MPa)Elongation (%)Hardness
ASTM B348 Minimum≥ 345 (50 ksi)≥ 275 (40 ksi)≥ 20 in 4D–
Reduction of Area, Minimum–––≥ 30%
Grade 7H — Same Material, Higher UTS Minimum≥ 400 (58 ksi)≥ 275 (40 ksi)≥ 20 in 4D–
Annealed (Typical)400–480300–38025–30–
Physical Properties
Density4.51 g/cm³
Melting PointApproximately 1668°C
Modulus of ElasticityApproximately 105 GPa
Thermal ConductivityApproximately 16 W/m·K at 20°C
Thermal Expansion8.6 µm/m·°C (20–100°C)
Palladium Content0.12–0.25% — the reason for the grade
Equivalent Grades & Standards
UNSWerkstoff / DINASTM DesignationCommon Name
R52400 3.7235 ASTM B348 Grade 7 / 7H Ti-0.15Pd / Ti-Pd

Key Specifications: ASTM B348 (Bar & Billet) / ASTM B265 (Plate, Sheet & Strip) / ASTM B381 (Forgings) / ASTM B337 and B338 (Tube) / ASTM F467 and F468 (Nonferrous Nuts and Bolts). Grade 7H is identical material certified to a 400 MPa (58 ksi) minimum tensile strength. Grade 11 is the equivalent palladium-bearing version of Grade 1 chemistry, and Grades 16 and 17 carry a reduced 0.04 to 0.08% palladium addition at lower cost where the full benefit is not required.

Machinability: titanium’s low thermal conductivity is the governing problem — the heat generated at the cut is not carried away into the workpiece or the chip but stays at the cutting edge. Use rigid setups, sharp tooling, low surface speeds, heavy positive feeds and high-volume flood coolant directed at the cutting zone, and never allow the tool to dwell. Titanium also work-hardens and galls against tooling, so sharp edges matter more than high speeds. Fine chips and grinding dust are a fire hazard and are handled wet. Grade 7 machines identically to Grade 2 — the palladium addition is too small to affect cutting behaviour.

Welding: Grade 7 is readily weldable by GTAW, GMAW, plasma and resistance processes, exactly as Grade 2. Full inert gas shielding of weld, heat-affected zone and root is essential. Matching Grade 7 filler should be used rather than Grade 2 filler, because a Grade 2 weld bead in a Grade 7 assembly becomes the crevice-susceptible weak point and defeats the reason for selecting the alloy in the first place.

Forming: forming behaviour matches Grade 2 — good cold formability, hot work in the 760–870°C range. Thread rolling is preferred to thread cutting.

Heat Treatment: not hardenable by heat treatment. Mill anneal at approximately 650–760°C, stress relieve at 480–595°C. Treatment above about 500°C should be in vacuum or inert gas, or the alpha case removed. The palladium remains in solid solution and is unaffected by normal thermal processing.

Grade 7 exists for one reason, and it is a good one. In a tight, oxygen-starved crevice — under a gasket, inside a threaded joint, beneath a deposit — commercially pure titanium cannot repassivate and will eventually suffer crevice attack in hot chloride service above roughly 70 to 80°C. The 0.12 to 0.25% palladium addition changes the cathodic behaviour of the surface so that repassivation occurs even under those conditions, which extends useful service into hot brines, wet-process acid plant and reducing acid chloride environments where Grade 2 would fail.

Because a bolted joint is by its nature a collection of crevices, this benefit matters more for fasteners than for almost any other product form. Grade 7 is mechanically identical to Grade 2 — same 345 MPa minimum tensile, same 20% elongation — so specifying it costs nothing in strength or formability; the premium is purely the palladium. Where the cost of palladium is the obstacle, Grade 12 delivers much of the same crevice benefit through molybdenum and nickel instead, and is stronger into the bargain.

Three absolute exclusions. Titanium must not be used in dry chlorine, with which it reacts violently; it must not be used with red fuming nitric acid; and it is rapidly attacked by hydrofluoric acid at any concentration. Fine titanium swarf and grinding dust are also a genuine fire hazard and must be handled wet and stored separately. These limits apply to every grade on this page, including the palladium and molybdenum-nickel modified grades — the alloying additions improve crevice and reducing-acid performance, they do not change these exclusions.

Titanium galls, and for a threaded fastener this is the single most important practical fact about the material. Titanium’s protective oxide is thin and the metal beneath it is adhesive, so a titanium thread run against another titanium thread will cold-weld and seize — often badly enough that the fastener has to be cut off. Every titanium bolted joint needs one of three mitigations: an anti-seize compound or dry-film lubricant such as molybdenum disulphide on the thread; a plated or coated thread, commonly silver or a solid-film lubricant; or a nut in a dissimilar material rather than titanium. Exotic Alloy supplies titanium fasteners with a lubricant or coating specified at order stage, and will advise on the combination if you tell us the mating material.

Titanium is galvanically noble, which makes it a hazard to what it is bolted into. It sits close to the passive stainless steels and the nickel alloys on the galvanic series and well above carbon steel, aluminium, zinc and magnesium. A titanium fastener in an aluminium or carbon steel structure will not itself corrode, but it will drive accelerated corrosion of the structure around it, and the small-anode-large-cathode geometry of a bolted joint is the worst case. Where titanium fasteners are used in a less noble assembly, an insulating washer and sleeve or a barrier coating on the mating faces should be specified.

Note on section size: the ASTM B348 tensile requirements apply to longitudinal sections up to 76 mm (3 in.) thick with a maximum area of 64.5 cm² (10 in.²). Mechanical properties for larger sections are negotiated between manufacturer and purchaser, so for large-diameter bolting the acceptance values must be agreed on the order rather than assumed from the table.
Key Characteristics

  • Best crevice corrosion resistance of the five grades on this page.
  • Palladium addition enables repassivation in oxygen-starved crevices.
  • Mechanically identical to Grade 2 — no strength or formability penalty.
  • Extends useful service into hot brines and reducing acid chlorides.
  • Grade 7H variant available at a 400 MPa minimum tensile.

Typical Applications

  • Wet-process chemical plant: acid-service flange and vessel bolting.
  • Hot brine and concentrated chloride systems.
  • Sour service and oil and gas production hardware.
  • Heat exchangers and gasketed joints where crevices are unavoidable.
  • Pulp and paper bleach plant fastener assemblies.