+91 97734 41022 sales@exoticalloy.com
Material Specification

Grade 5

Grade 5 Fasteners
Ti-6Al-4V Alpha-Beta Alloy – 895 MPa Minimum at 4.42 g/cm³

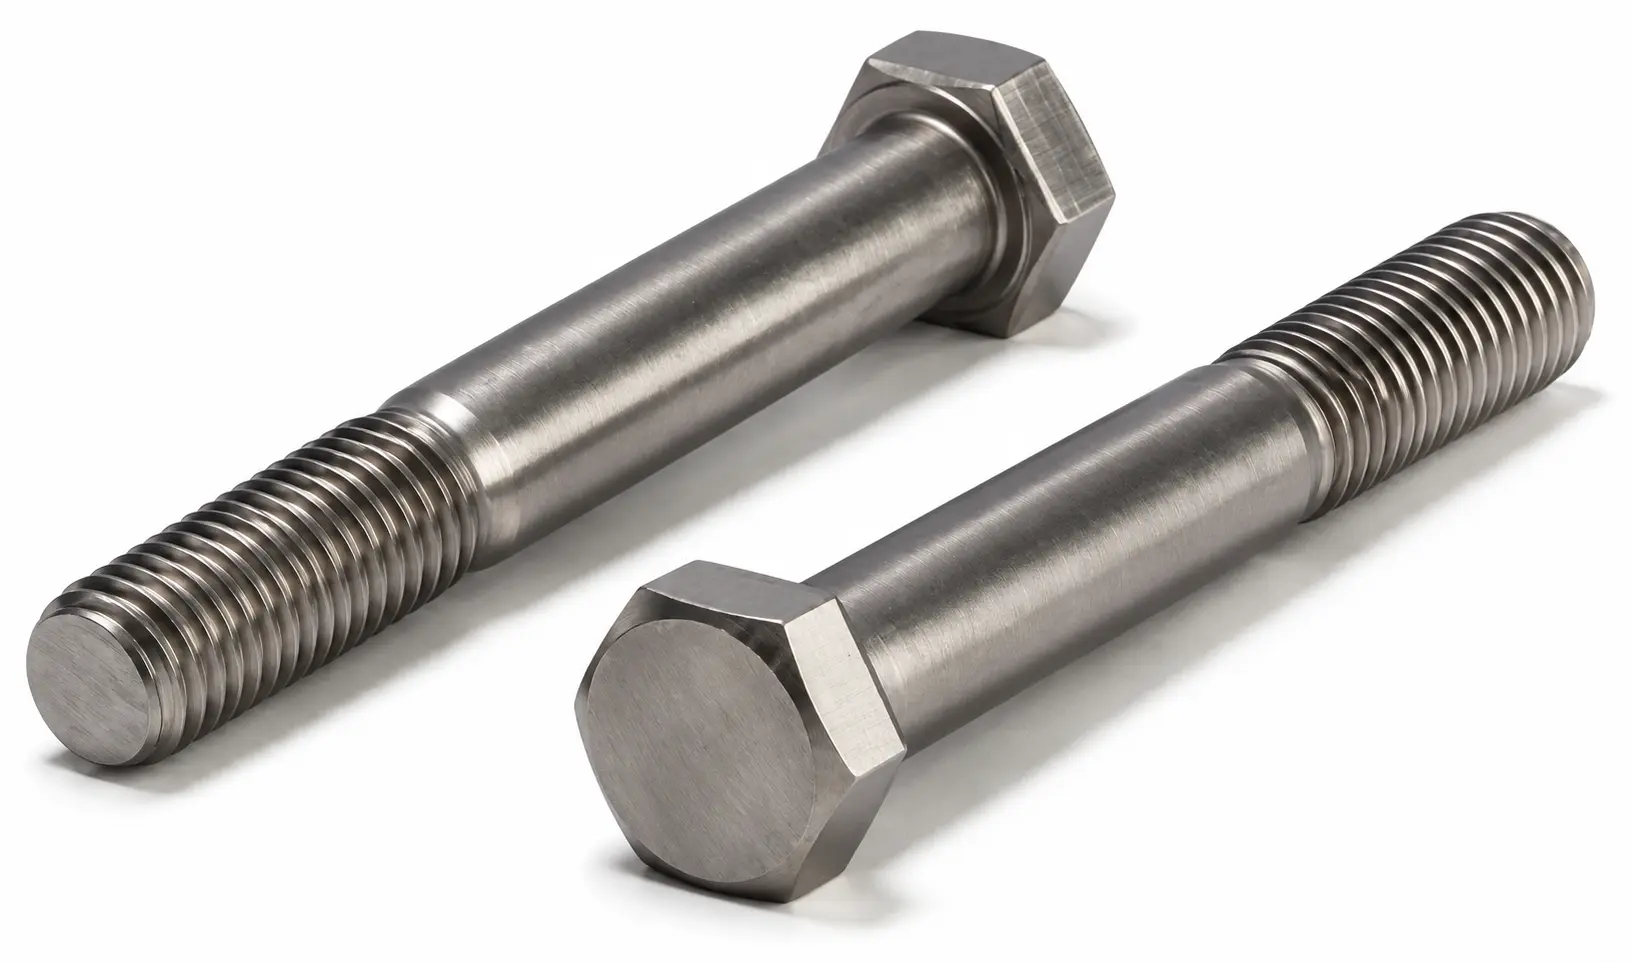
Titanium Grade 5 (Ti-6Al-4V) Fasteners

Buy Titanium Grade 5 (Ti-6Al-4V / UNS R56400 / Werkstoff 3.7165 / ASTM B348 Grade 5) bolts, stud bolts, hex nuts, socket cap screws, threaded rods and custom CNC fasteners from Exotic Alloy. Grade 5 is the most widely used of all the high-strength titanium alloys — an alpha-beta alloy carrying 5.5–6.75% aluminium and 3.5–4.5% vanadium that combines a specified minimum 895 MPa tensile strength with a density of only 4.42 g/cm³.

Exotic Alloy manufactures Grade 5 titanium fasteners to ASTM B348, ASTM B265, ASTM B381, AMS 4928, AMS 4911, BS TA11 and MIL-STD-2154, and to ASTM F467 and F468 for nonferrous nuts and bolts, in metric M3–M48 and imperial #6–2" sizes, with full EN 10204 3.1 material test certificates for aerospace, motorsport, offshore and medical applications. The alloy is fully heat treatable in sections up to 25 mm and can be employed up to around 400°C.

Request a Quote
Product Range

Grade 5 Fasteners Available

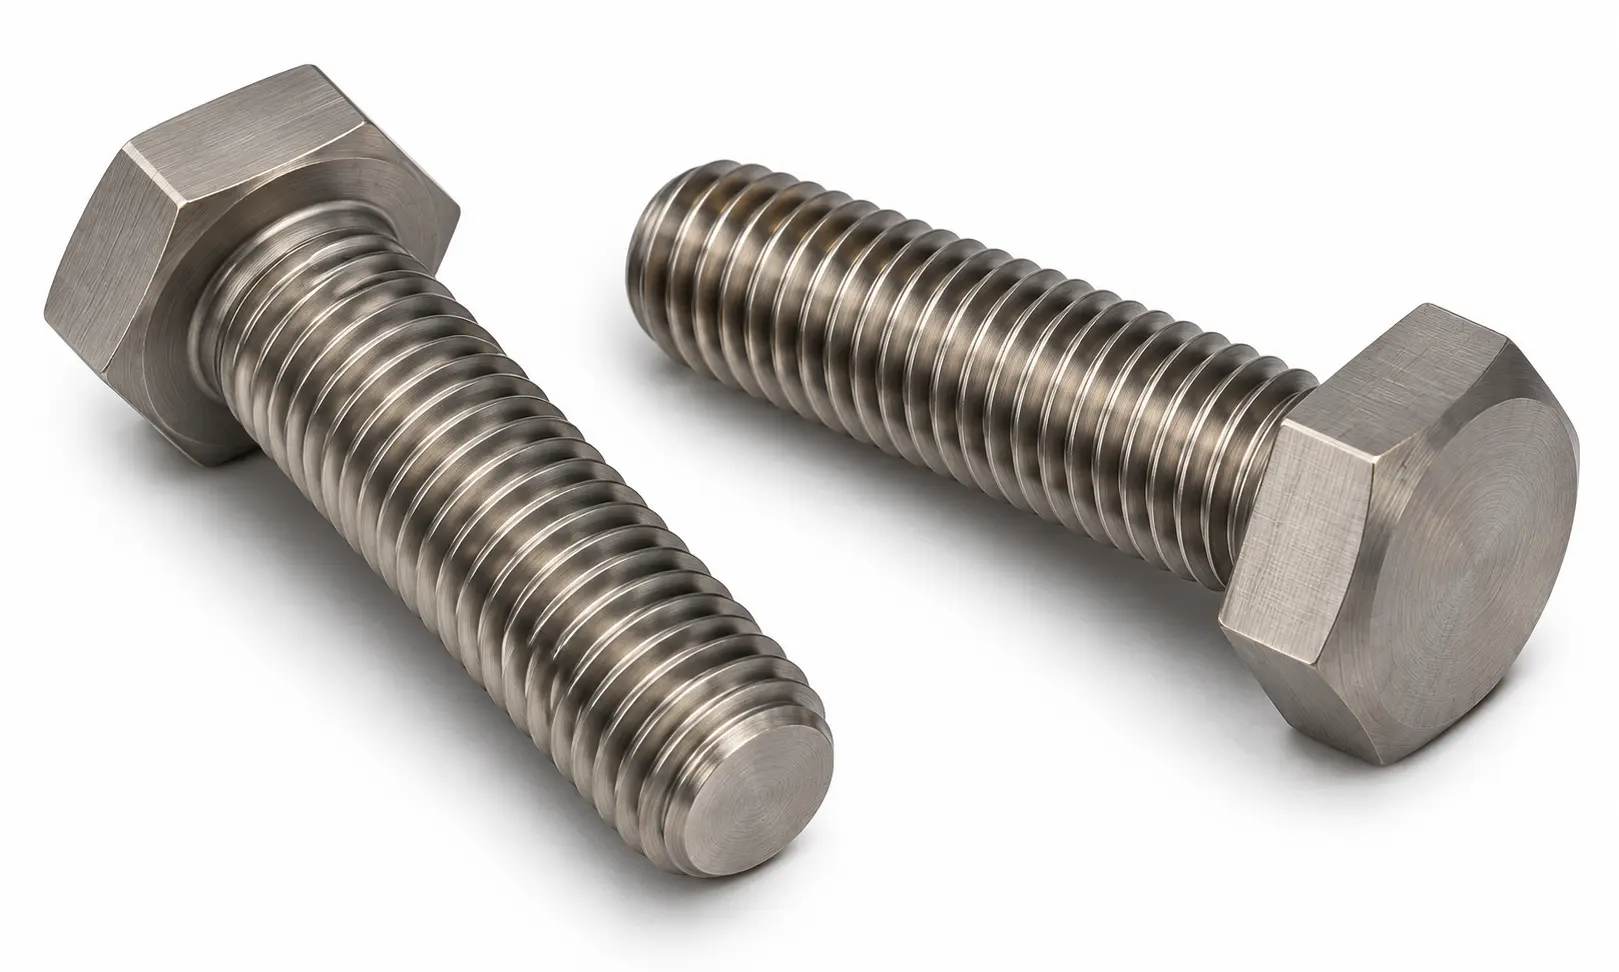
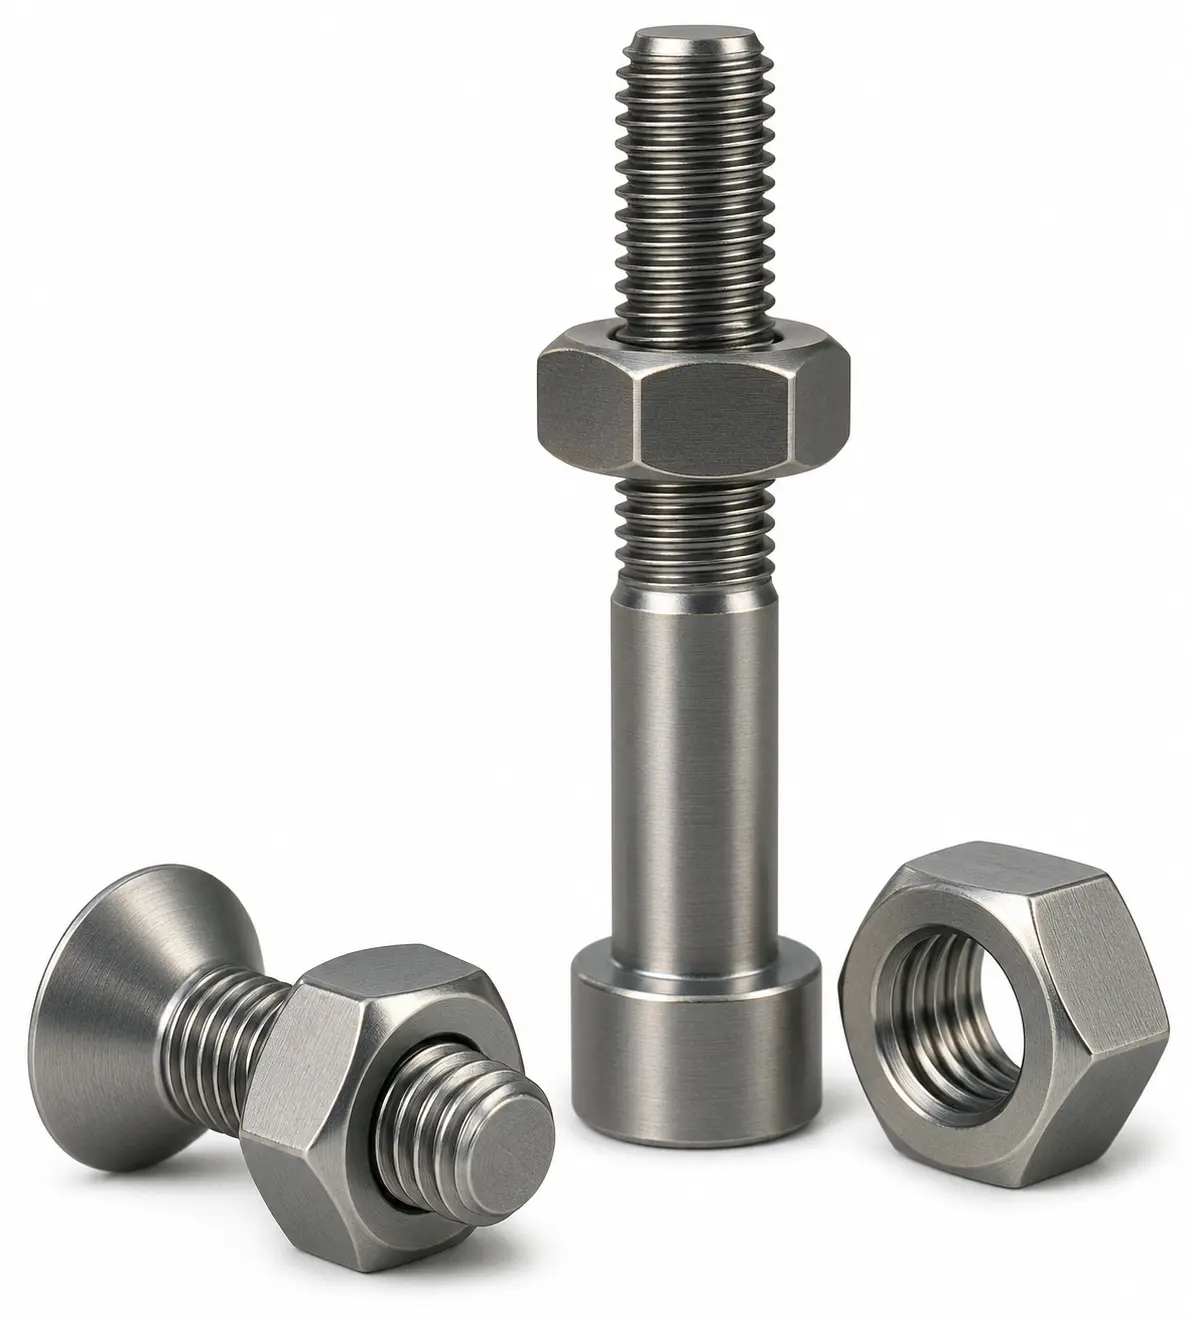
Grade 5 Hex Bolts
Grade 5
Hex Bolts
Grade 5 Heavy Hex Bolts
Grade 5
Heavy Hex Bolts
Grade 5 Stud Bolts
Grade 5
Stud Bolts
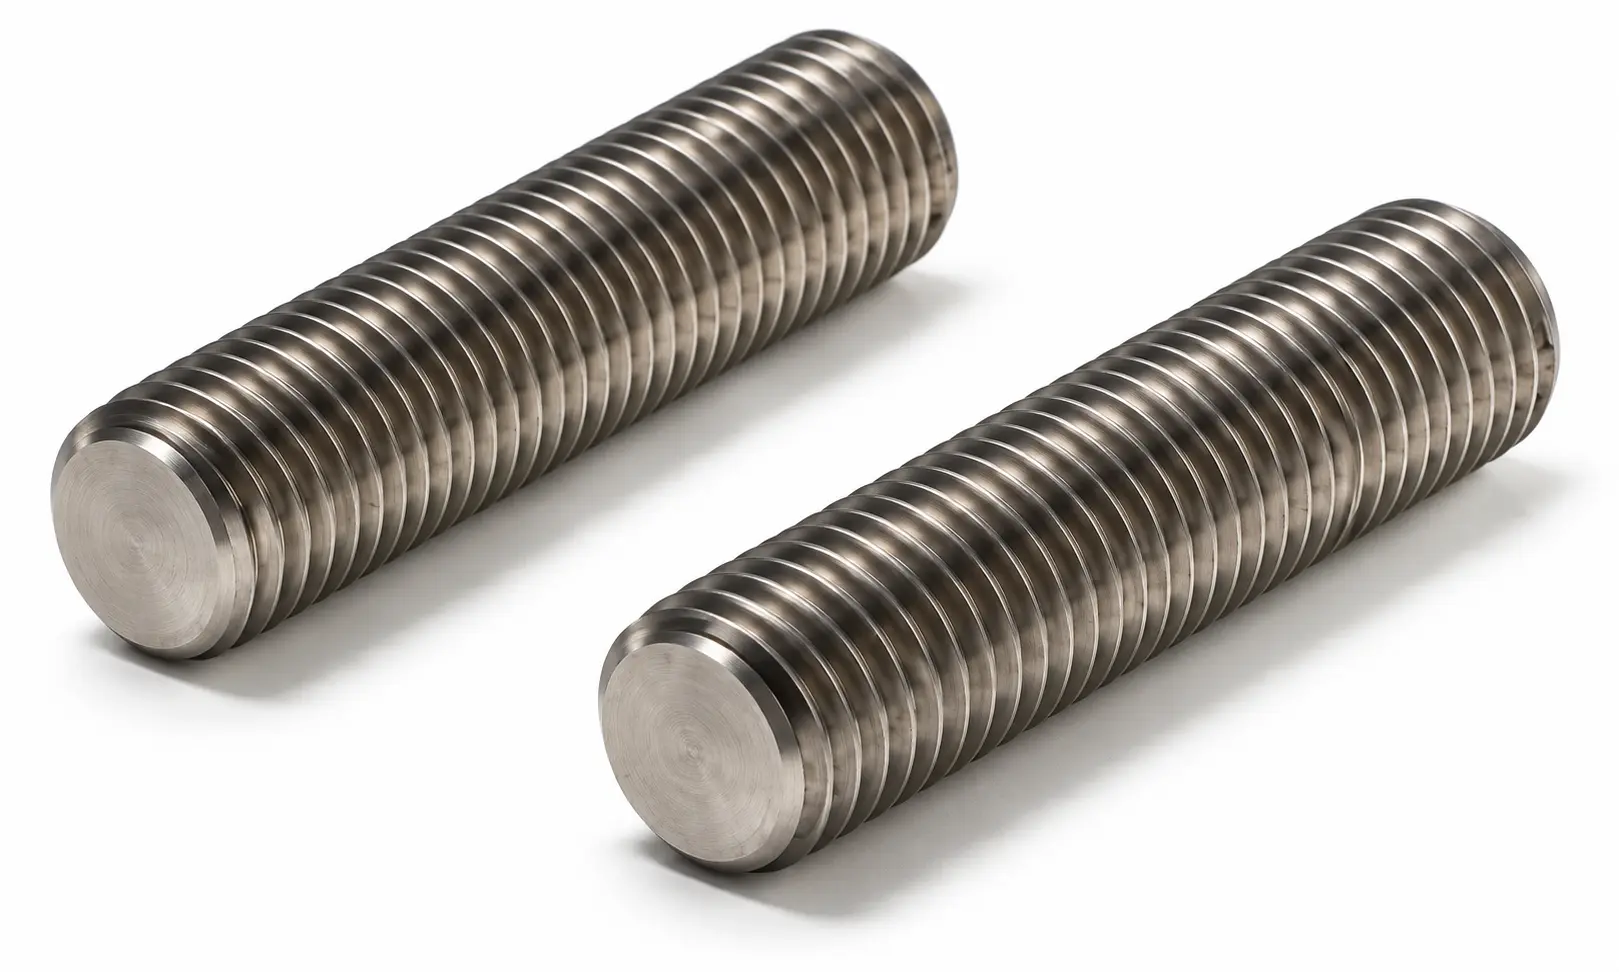
Grade 5 Threaded Rods
Grade 5
Threaded Rods
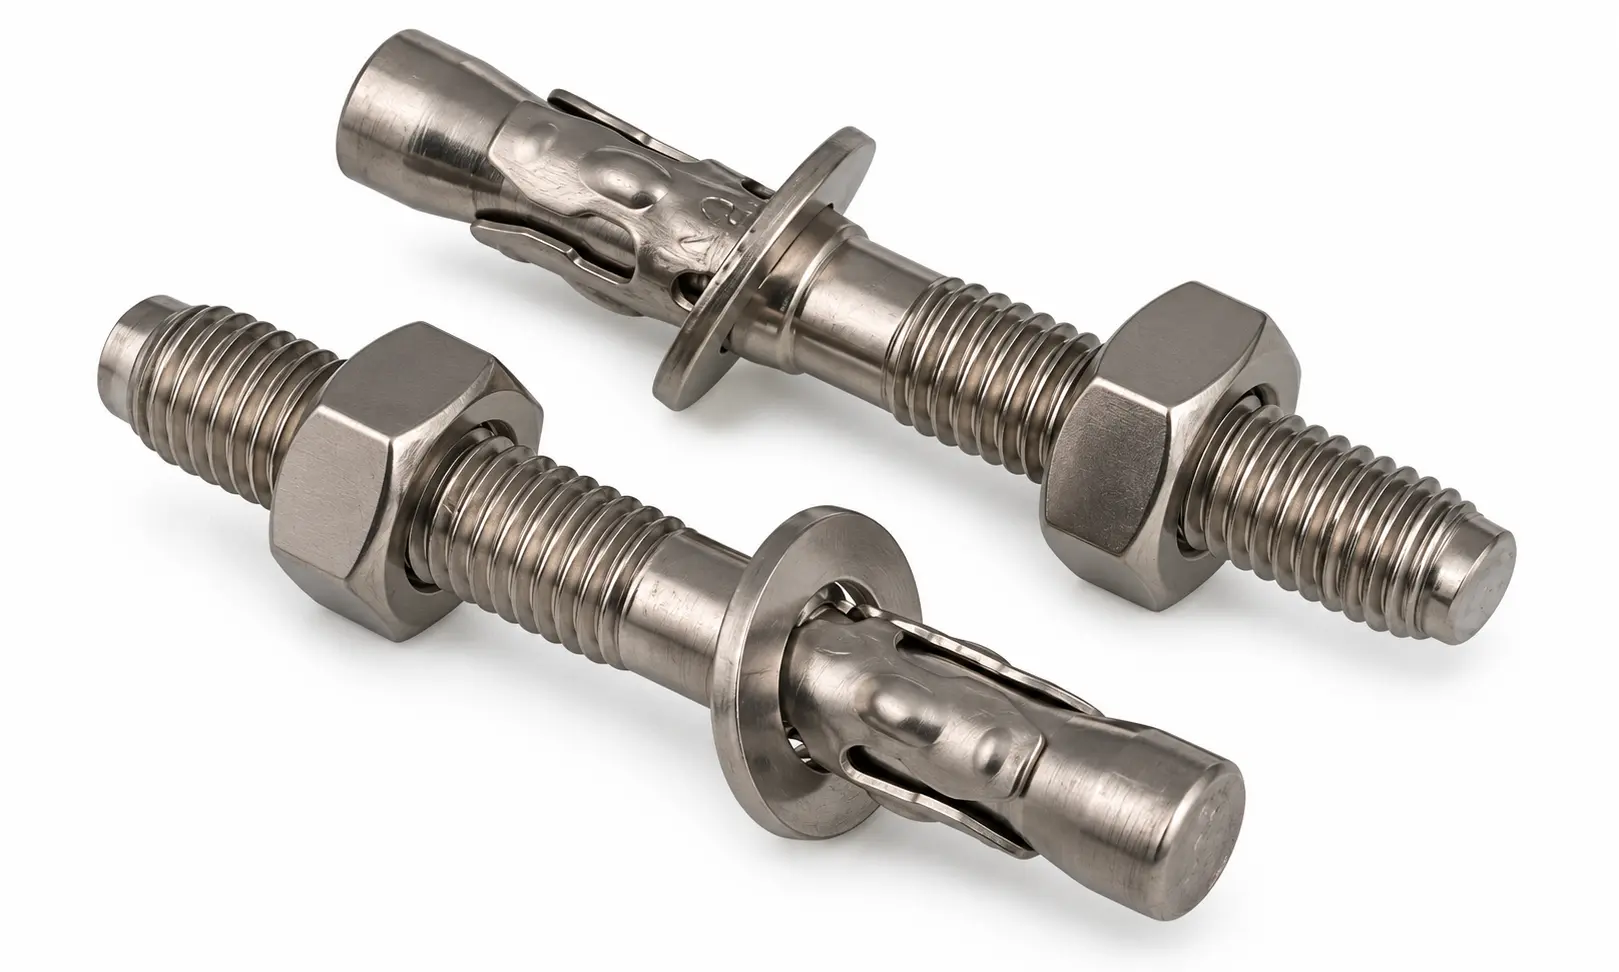
Grade 5 Anchor Bolts
Grade 5
Anchor Bolts
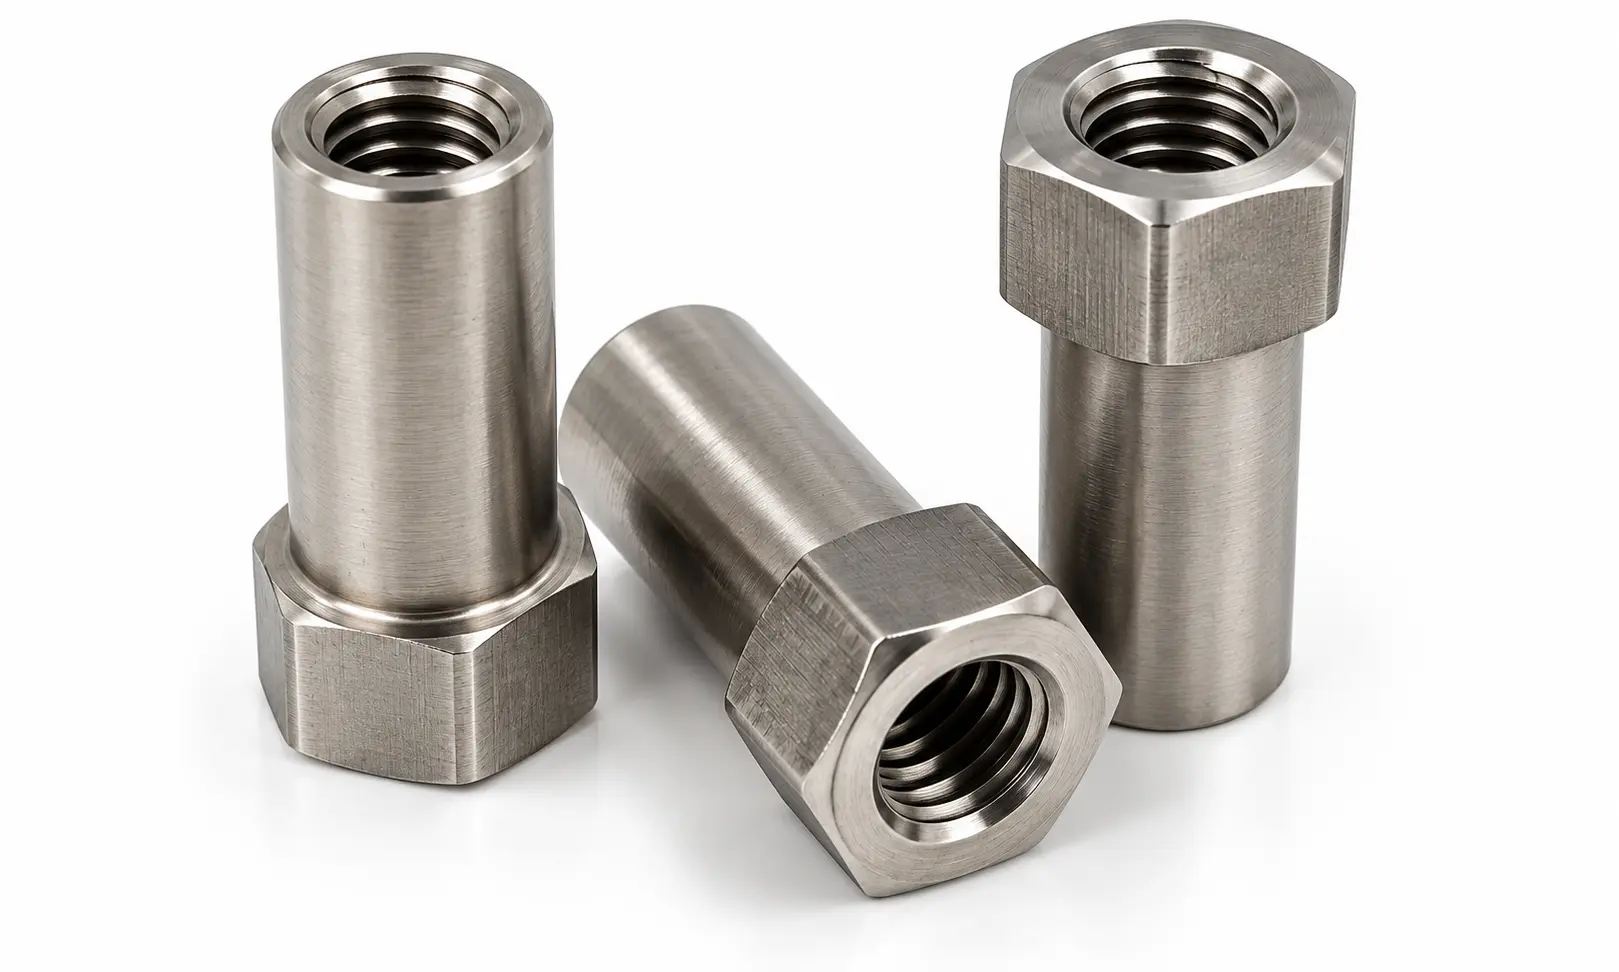
Grade 5 Hex Nuts
Grade 5
Hex Nuts
Grade 5 Washers
Grade 5
Washers
Grade 5 Cotter Pins
Grade 5
Cotter Pins
Grade 5 Springs
Grade 5
Springs
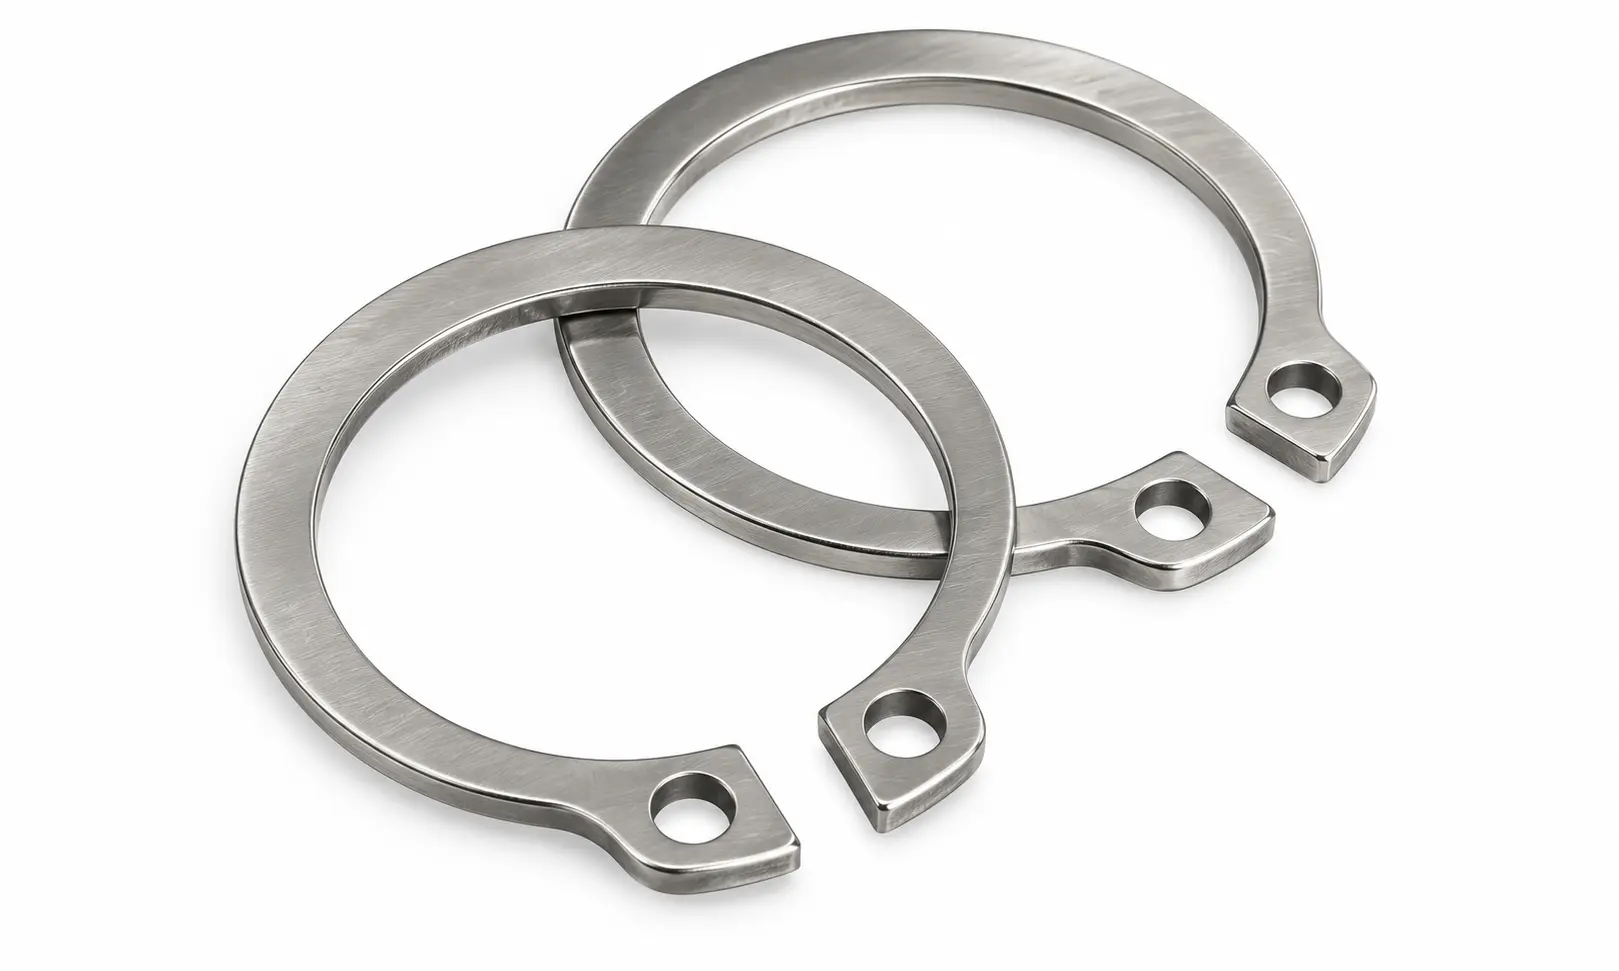
Grade 5 Circlips
Grade 5
Circlips
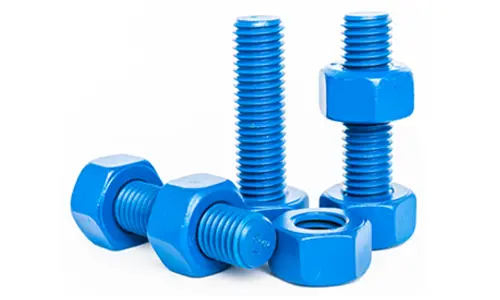
Grade 5 Coated Fasteners
Grade 5
Coated Fasteners
Grade 5 Custom Spacers
Grade 5
Custom Spacers
Technical Data

Grade 5 Specifications

Chemical Composition — Titanium Grade 5 (Ti-6Al-4V) (wt. %)
ElementTiAlVOFeNCH
Min %Balance5.503.50–––––
Max %Balance6.754.500.200.400.050.080.015
Mechanical Properties — Titanium Grade 5 (Ti-6Al-4V)
ConditionUTS (MPa)YS 0.2% (MPa)Elongation (%)Hardness
ASTM B348 Minimum≥ 895 (130 ksi)≥ 828 (120 ksi)≥ 10 in 4D–
Reduction of Area, Minimum–––≥ 25%
Annealed Bar (Typical)100091018Approx. 36 HRC
Charpy V-Notch Impact (Typical)–––24 J
Physical Properties
Density4.42 g/cm³
Melting RangeApproximately 1604–1660°C
Modulus of Elasticity114 GPa (typical)
Thermal ConductivityApproximately 6.7 W/m·K at 20°C
Thermal Expansion8.6 µm/m·°C (20–100°C)
Maximum Service TemperatureApproximately 400°C
Equivalent Grades & Standards
UNSWerkstoff / DINASTM DesignationCommon Name
R56400 3.7165 ASTM B348 Grade 5 Ti-6Al-4V / BS TA11

Key Specifications: ASTM B348 (Bar & Billet) / ASTM B265 (Plate, Sheet & Strip) / ASTM B381 (Forgings) / AMS 4928 (Bar) / AMS 4911 (Sheet) / BS TA11 / MIL-STD-2154 / ASTM F467 and F468 (Nonferrous Nuts and Bolts). For fracture-critical and implant work, Grade 23 (Ti-6Al-4V ELI) is the extra-low-interstitial version with oxygen restricted to 0.13% maximum, giving improved ductility and fracture toughness at some cost in strength; it is covered by ASTM F136 for surgical implants.

Machinability: titanium’s low thermal conductivity is the governing problem — the heat generated at the cut is not carried away into the workpiece or the chip but stays at the cutting edge. Use rigid setups, sharp tooling, low surface speeds, heavy positive feeds and high-volume flood coolant directed at the cutting zone, and never allow the tool to dwell. Titanium also work-hardens and galls against tooling, so sharp edges matter more than high speeds. Fine chips and grinding dust are a fire hazard and are handled wet. Grade 5 is the most demanding of these five to machine because its thermal conductivity is only about 6.7 W/m·K — roughly 40% that of the CP grades — so almost all the cutting heat goes into the tool. Surface speeds must come down accordingly and coolant volume up.

Welding: weldability is rated fair rather than good. The alloy can be welded by GTAW, plasma and electron beam under full inert gas shielding or in vacuum, but the weld and heat-affected zone lose ductility relative to the parent metal and post-weld stress relief is normally required. Where a joint must carry fatigue loading, mechanical fastening is preferable to welding — which is part of why Grade 5 fasteners exist.

Forming: Grade 5 is considerably less formable than the CP grades and most forming is done hot, in the 870–955°C range. Specified minimum bend radii are 4.5 times thickness below 1.8 mm and 5.0 times thickness above it. Thread rolling is practicable and strongly preferred to cutting.

Heat Treatment: unlike the CP grades, Grade 5 is fully heat treatable — solution heat treatment followed by ageing — in sections up to 25 mm. Most fasteners are supplied in the annealed condition at the ASTM B348 minimums; solution treated and aged material reaches higher strength but with reduced ductility and is specified where the drawing calls for it. Mill annealing is at approximately 705–790°C. Treatment above about 500°C must be in vacuum or inert gas, or the alpha case removed afterwards.

Grade 5 offers excellent resistance in marine and offshore oil and gas environments and is highly resistant to oxidising acids, with useful resistance to reducing acids and good resistance to most organic acids at lower concentrations and temperatures. It is not, however, a substitute for the commercially pure grades on corrosion duty — the aluminium and vanadium additions that give it its strength reduce its resistance in reducing media relative to Grades 2, 7 and 12. Where corrosion rather than strength governs, use a CP grade; where both matter, the palladium and ruthenium modified versions of this chemistry (Grades 24, 25 and 29) raise the useful threshold temperature in reducing acid chloride and sour environments to well over 200°C.

Three absolute exclusions. Titanium must not be used in dry chlorine, with which it reacts violently; it must not be used with red fuming nitric acid; and it is rapidly attacked by hydrofluoric acid at any concentration. Fine titanium swarf and grinding dust are also a genuine fire hazard and must be handled wet and stored separately. These limits apply to every grade on this page, including the palladium and molybdenum-nickel modified grades — the alloying additions improve crevice and reducing-acid performance, they do not change these exclusions.

Titanium galls, and for a threaded fastener this is the single most important practical fact about the material. Titanium’s protective oxide is thin and the metal beneath it is adhesive, so a titanium thread run against another titanium thread will cold-weld and seize — often badly enough that the fastener has to be cut off. Every titanium bolted joint needs one of three mitigations: an anti-seize compound or dry-film lubricant such as molybdenum disulphide on the thread; a plated or coated thread, commonly silver or a solid-film lubricant; or a nut in a dissimilar material rather than titanium. Exotic Alloy supplies titanium fasteners with a lubricant or coating specified at order stage, and will advise on the combination if you tell us the mating material. Grade 5 is the grade most often used for weight-critical bolted joints, so galling mitigation is routinely specified on it.

Titanium is galvanically noble, which makes it a hazard to what it is bolted into. It sits close to the passive stainless steels and the nickel alloys on the galvanic series and well above carbon steel, aluminium, zinc and magnesium. A titanium fastener in an aluminium or carbon steel structure will not itself corrode, but it will drive accelerated corrosion of the structure around it, and the small-anode-large-cathode geometry of a bolted joint is the worst case. Where titanium fasteners are used in a less noble assembly, an insulating washer and sleeve or a barrier coating on the mating faces should be specified.

Note on section size: the ASTM B348 tensile requirements apply to longitudinal sections up to 76 mm (3 in.) thick with a maximum area of 64.5 cm² (10 in.²). Mechanical properties for larger sections are negotiated between manufacturer and purchaser, so for large-diameter bolting the acceptance values must be agreed on the order rather than assumed from the table.

How the five grades divide up: Grades 1, 2, 7 and 12 are commercially pure or lean alloys selected for corrosion resistance; Grade 5 is the structural alloy selected for strength-to-weight. Within the corrosion grades, Grade 1 is the softest and most formable, Grade 2 is the general-purpose workhorse, Grade 7 adds palladium for the best crevice and reducing-acid resistance in the family, and Grade 12 adds molybdenum and nickel to get much of Grade 7’s crevice performance without the palladium cost while also being 40% stronger than Grade 2. Grade 5 is a different proposition entirely — 895 MPa minimum tensile at 4.42 g/cm³ — but its aluminium and vanadium make it less corrosion resistant than the CP grades in reducing media, so it should not be substituted for them on corrosion duty.
Key Characteristics

  • The most widely used high-strength titanium alloy in the world.
  • Specified minimum 895 MPa tensile at a density of only 4.42 g/cm³.
  • Fully heat treatable by solution treatment and ageing to 25 mm sections.
  • Service capability to approximately 400°C.
  • Excellent resistance in marine and offshore oil and gas environments.

Typical Applications

  • Aerospace: airframe and aero-engine component fastener assemblies.
  • Motorsport: weight-critical driveline, suspension and chassis bolting.
  • Offshore oil and gas: riser, manifold and subsea fastener applications.
  • Marine equipment and high-performance fixings.
  • Medical equipment and instrument hardware.